
2026-10-30
CNC Machining for Industrial Hydraulic and Pneumatic Equipment: Valve Bodies, Manifold Blocks, Cylinder Components and Sealing Interfaces
Introduction: Precision Requirements in Hydraulic and Pneumatic Equipment
Hydraulic and pneumatic systems are widely used in industrial machinery, automated production lines, mobile equipment, material handling systems, and process-control applications. Their performance depends on the reliable movement and control of fluids or compressed air through interconnected valves, cylinders, manifolds, fittings, and actuators.
Many of these systems contain precision-machined metal components. A valve body must provide accurately positioned ports and internal passages. A manifold block may connect several hydraulic circuits through intersecting drilled holes. A cylinder component must maintain the required relationship between its bore, rod, seals, and mounting interfaces.
Although these components may appear to be simple blocks, sleeves, shafts, or housings, their functional requirements can be demanding. Incorrect hole positions, poor surface conditions, dimensional variation, or inadequate sealing geometry may lead to leakage, assembly difficulties, pressure loss, or inconsistent operation.
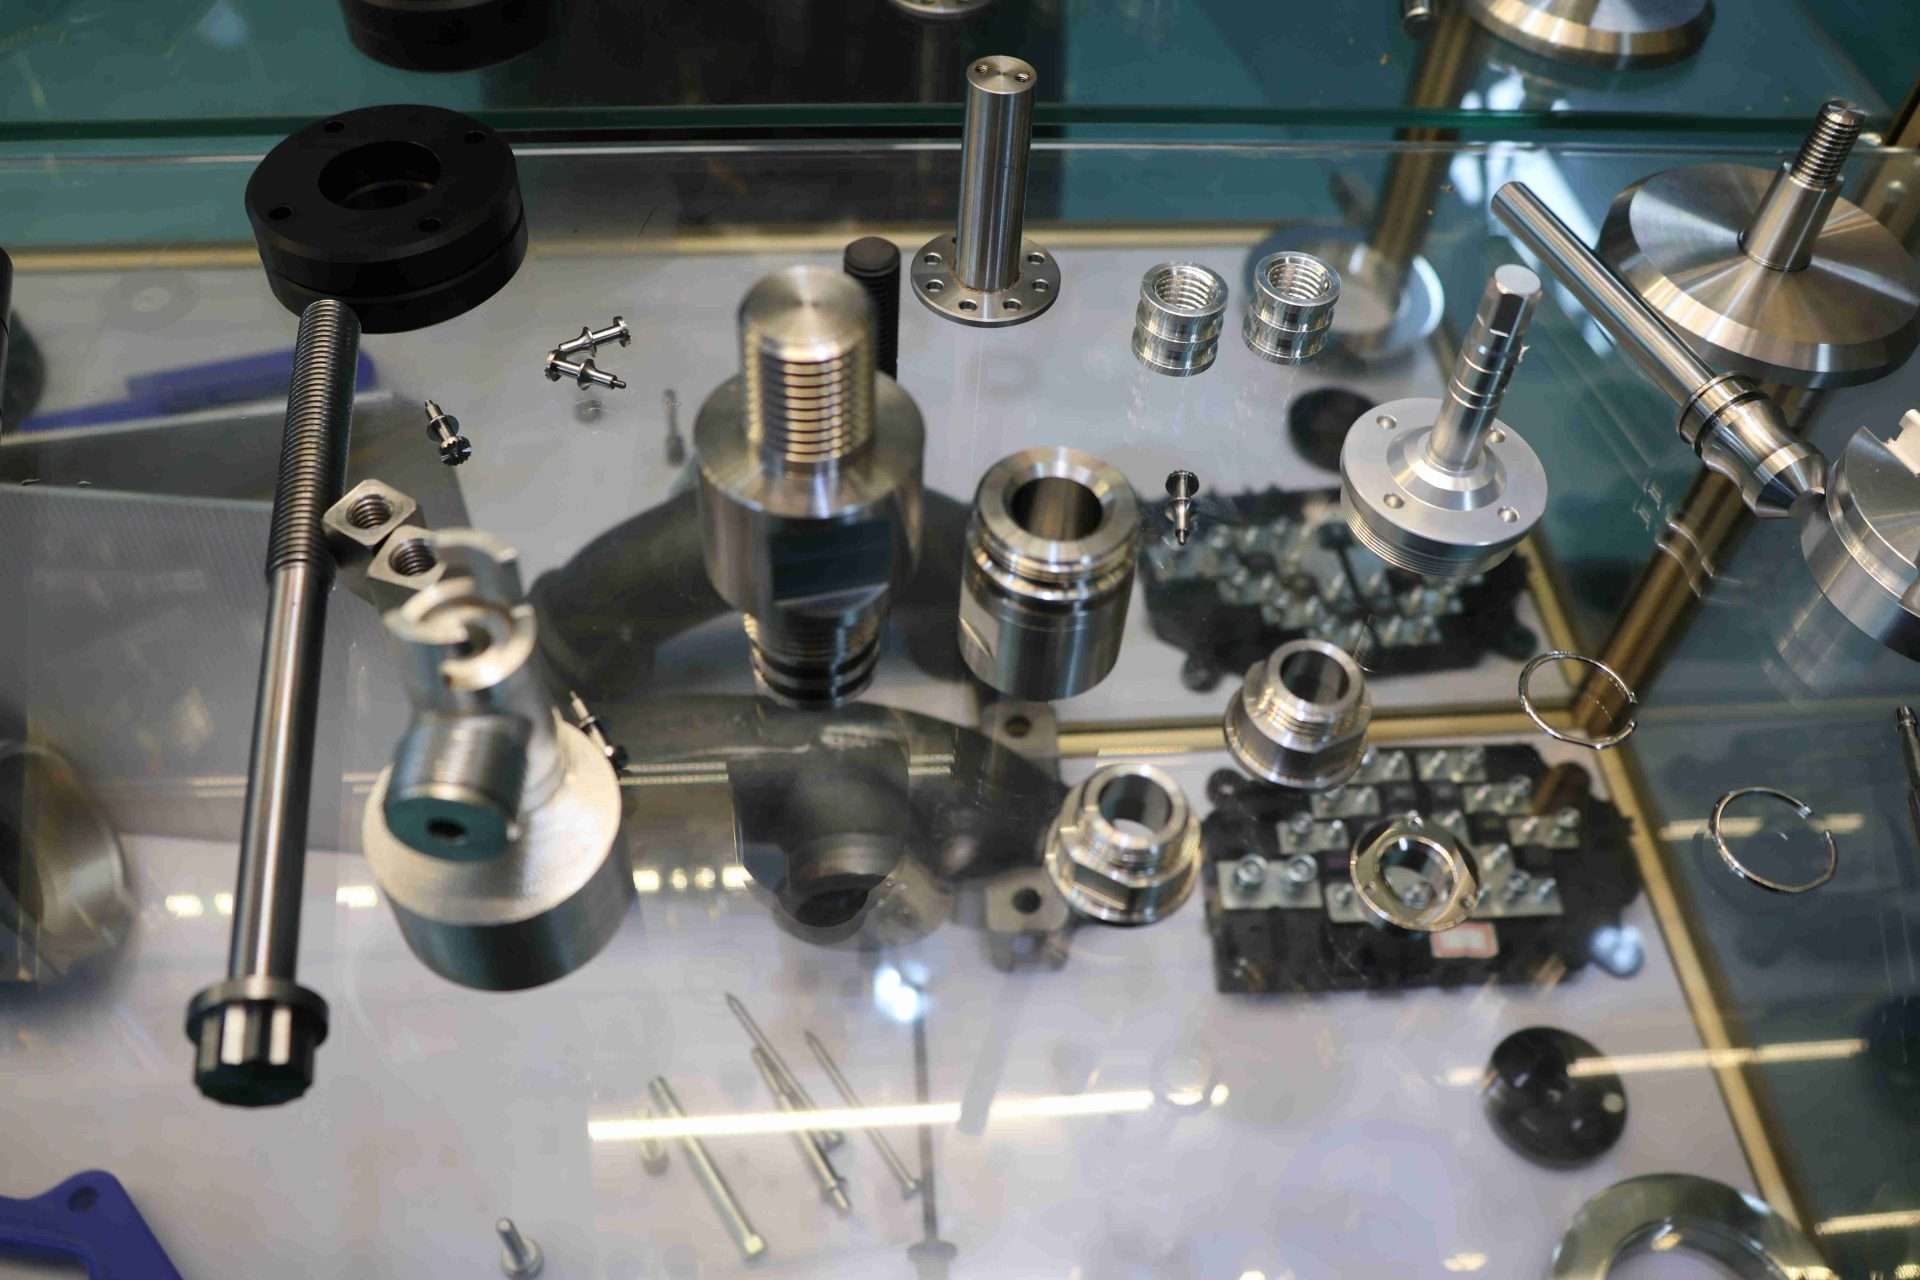
CNC machining provides a flexible manufacturing solution for producing custom hydraulic and pneumatic components from aluminum, stainless steel, carbon steel, brass, and engineering plastics. Depending on the geometry, manufacturers may combine CNC milling, turning, drilling, boring, tapping, and finishing operations to create the required features.
However, successful production involves more than selecting a machine. Engineers and buyers need to consider material compatibility, pressure-related design requirements, port geometry, sealing interfaces, dimensional tolerances, internal cleanliness, inspection, and production quantity.
MFG SOLUTION provides CNC machining services for custom industrial components. This guide explains how to plan the manufacturing of hydraulic and pneumatic equipment parts, with particular attention to valve bodies, manifold blocks, cylinder components, precision ports, sealing surfaces, and quality control.
1. Common CNC-Machined Components in Hydraulic and Pneumatic Systems
Hydraulic and pneumatic equipment contains components with different mechanical and fluid-control functions. Identifying the purpose of each part helps determine its machining requirements.
1.1 Hydraulic Valve Bodies
Valve bodies provide the housing and internal passages for controlling fluid direction, pressure, and flow. Depending on the valve design, a body may contain precision bores, threaded ports, cross-drilled passages, mounting faces, plug interfaces, and sealing grooves.
The location and relationship of these features are important. A port that is correctly sized but incorrectly positioned may interfere with an adjacent passage or prevent the valve from connecting properly to the surrounding circuit.
Valve bodies may be manufactured from aluminum alloys, steel, stainless steel, or other materials selected according to operating pressure, environment, weight, and application requirements.
CNC milling is commonly used for external profiles, mounting surfaces, and pockets. Drilling, boring, tapping, and other operations create the internal and external features required by the design.
1.2 Hydraulic Manifold Blocks
Manifold blocks distribute fluid between multiple valves, pumps, cylinders, and other hydraulic components. They often contain several intersecting passages and connection ports within a relatively compact block.
Their manufacturing challenges include:
- Accurate positioning of intersecting passages.
- Correct port dimensions and thread specifications.
- Adequate wall thickness between internal passages.
- Controlled sealing surfaces.
- Removal of burrs and machining debris.
- Reliable inspection of critical features.
Manifold blocks may require multiple machining orientations to access all ports and passages. The manufacturing plan should establish datums that maintain the relationship between the different faces and internal features.
For complex parts, multi-axis machining may reduce the number of setups. The appropriate configuration depends on the geometry, machine capability, production volume, and required accuracy.
1.3 Pneumatic Valve and Actuator Components
Pneumatic systems use compressed air to operate cylinders, valves, grippers, and other mechanisms. Their machined components may include valve housings, actuator end caps, mounting blocks, piston supports, and connector adapters.
Pneumatic components may have different pressure and sealing requirements from hydraulic components. Buyers should provide the actual operating conditions rather than assuming that a generic machining tolerance or surface finish will be sufficient.
Aluminum is often considered for lightweight pneumatic housings and mounting components. Stainless steel and engineering plastics may be appropriate for selected applications depending on environmental and mechanical requirements.
1.4 Cylinder Components: Pistons, Rods, and End Caps
Cylinder assemblies convert fluid or compressed-air pressure into mechanical movement.
Common machined components include piston bodies, piston rods, end caps, guide sleeves, rod glands, mounting brackets, and threaded connectors.
The functional dimensions vary by component:
- Piston bodies require appropriate dimensional relationships with the cylinder bore and sealing elements.
- Piston rods may require controlled diameters, straightness, and surface condition.
- End caps need suitable mounting and sealing interfaces.
- Guide sleeves require appropriate bore geometry and fit.
- Rod glands may contain grooves and locating features for sealing components.
These requirements should be reviewed as part of the complete cylinder assembly rather than treated as unrelated dimensions.
For rotational components, CNC turning services can produce shafts, rods, sleeves, and cylindrical interfaces. Milling and drilling can then create additional flats, holes, and mounting features where required.
2. Material Selection for Hydraulic and Pneumatic Components
Material selection affects strength, weight, corrosion resistance, machinability, dimensional stability, and compatibility with the working environment.
The correct material depends on the actual system requirements, including operating pressure, temperature, fluid type, external exposure, and expected service conditions.
Aluminum Alloys
Aluminum alloys are frequently considered for valve housings, pneumatic components, mounting blocks, and selected manifold designs where weight reduction and machinability are important.
Their relatively low density can help reduce equipment weight. Aluminum can also be machined into complex shapes and finished through processes such as anodizing.
However, the selected alloy must be appropriate for the component’s mechanical loading and environment. Not every aluminum alloy is suitable for every pressure-containing application.
Learn more about aluminum machining and material options.
Stainless Steel
Stainless steel may be appropriate for components exposed to moisture, corrosive environments, certain chemicals, or demanding operating conditions.
It can be used for selected fittings, connectors, valve components, shafts, and other precision parts.
The exact grade should be determined according to corrosion exposure, mechanical requirements, machinability, and compatibility with the working fluid. Machining parameters should also account for the material’s cutting behavior and potential work hardening.
See the stainless steel machining guide for additional material considerations.
Carbon and Alloy Steels
Carbon and alloy steels may be selected for components requiring specific strength, hardness, or wear properties.
Applications may include shafts, mechanical interfaces, actuator components, and structural parts. Heat treatment may be required depending on the component’s function.
When heat treatment is involved, engineers should consider its potential effects on dimensional stability and the subsequent machining or finishing sequence.
MFG SOLUTION also provides information about 1045 steel turned parts and general material selection.
Brass and Engineering Plastics
Brass may be considered for selected fittings, connectors, and components where its machinability and application-specific properties are suitable.
Engineering plastics such as POM, nylon, and PTFE may be used for selected guide components, spacers, insulating parts, and other nonstructural applications.
Plastic materials can behave differently from metals under sustained loading, temperature variation, and fluid exposure. Their suitability should be confirmed against the operating environment and component function.
3. Precision Ports, Internal Passages, and Hole Geometry
Hydraulic and pneumatic components frequently contain multiple holes and intersecting passages. Their accuracy and quality influence assembly, flow paths, and the integrity of the component.
Define Port Specifications Clearly
Port requirements should identify the thread standard, nominal size, thread depth, sealing arrangement, and location.
For example, metric threads, BSP threads, and NPT threads are not interchangeable simply because their nominal sizes appear similar. The drawing or technical specification should state the required standard.
The manufacturer should also understand whether the connection uses a tapered thread, parallel thread with a sealing element, O-ring interface, or another arrangement.
Ambiguous port specifications can create problems during production and final assembly.
Control Intersecting Passages
Manifold blocks often contain drilled passages that intersect at different angles. Their position and depth must be planned carefully to achieve the intended internal connection.
The machining process should account for drill access, tool length, chip evacuation, and the possibility of burr formation at intersections.
For complex internal geometries, the manufacturer may need to review the drawing and machining sequence before confirming feasibility.
Choose Between Drilling, Reaming, and Boring
Not every hole requires the same operation.
Standard drilling may be suitable for general passages and clearance holes. Reaming can be considered when a more controlled finished diameter is required. Boring may be appropriate for larger holes or features requiring specific geometric control.
The decision depends on diameter, depth, tolerance, surface condition, and the function of the hole.
For more detail, review the CNC hole tolerance guide.
Prevent Burrs and Internal Contamination
Burrs inside cross-drilled passages can interfere with assembly, restrict flow, or become loose during operation.
Deburring is therefore an important part of manufacturing manifold blocks and other fluid-control components.
However, internal passage geometry can make deburring difficult. Tool access, intersecting-hole locations, and cleaning methods should be considered during design and process planning.
The drawing or purchase specification should identify any special internal cleanliness requirements. A general deburring note should not be treated as a substitute for a defined cleanliness standard when the application requires one.
4. Sealing Interfaces, O-Ring Grooves, and Surface Finish
Sealing features are among the most important functional areas of hydraulic and pneumatic components.
A component may meet its overall dimensions but still fail to seal properly if the relevant groove, mating face, or surface condition is incorrect.
O-Ring Groove Geometry
O-ring grooves require dimensions that are compatible with the specified seal and installation arrangement.
Important considerations include groove width, depth, corner geometry, surface condition, and the relationship between the groove and adjacent features.
The correct design depends on the seal type, material, pressure conditions, and whether the seal is used in a static or dynamic application.
Manufacturers should work from the approved drawing and seal specification rather than estimating groove dimensions from a sample component.
Sealing Faces and Mating Surfaces
Mating faces may require controlled flatness, surface finish, and positional relationships.
For example, a valve mounting surface may need to align with a corresponding manifold face. A cylinder end cap may need to seat consistently against its housing.
These requirements should be clearly specified and inspected according to their function.
Surface Finish Requirements
Surface roughness can influence sealing performance, friction, wear, and the behavior of mating components.
However, different surfaces require different levels of control. A seal-running surface may have more demanding requirements than an external protective face.
Avoid applying one extremely fine surface-finish specification to every feature unless the application genuinely requires it.
For more information, see the CNC machining surface finish guide.
Surface Treatment and Dimensional Changes
Some components may require anodizing, plating, coating, or another surface treatment to meet environmental or functional requirements.
Finishing processes can affect final dimensions, especially at threads, grooves, bores, and mating interfaces.
The manufacturer and buyer should clarify whether dimensions refer to the condition before or after finishing. Critical sealing surfaces may require masking or a specific finishing sequence.
Explore the surface treatment information when comparing finishing requirements for different materials.
5. Selecting CNC Machining Processes for Different Components
The best manufacturing route depends on geometry, material, quantity, tolerance, and the complete production sequence.
CNC Milling for Valve Bodies and Manifold Blocks
CNC milling is suitable for producing external profiles, mounting faces, pockets, slots, and port-related features.
A manifold block may require machining on several faces. The process plan should establish repeatable workholding and preserve the relationship between the different ports.
For complex geometry, four-axis or five-axis machining may help reduce setups. However, additional machine-axis capability should be justified by the actual part requirements.
Review 5-axis CNC machining when evaluating parts with multiple angled features or machining orientations.
CNC Turning for Rods, Sleeves, and Cylindrical Parts
Turning is appropriate for piston rods, guide sleeves, collars, spacers, and cylindrical adapters.
It can produce external diameters, internal bores, shoulders, grooves, and threads. Some parts may require secondary milling or drilling operations to complete flats, cross-holes, or other nonrotational features.
For small precision components with complex rotational geometry, Swiss turning may be worth evaluating.
Workholding and Fixture Design
Hydraulic blocks and valve bodies may contain multiple machined faces and deep features. Proper workholding is essential to maintain stability and provide tool access.
Clamping forces should be appropriate for the material and geometry. Thin sections and irregular shapes may require additional support to prevent movement or distortion.
For practical guidance, read the CNC workholding fixtures guide.
Design for Manufacturability
Some design changes can reduce machining time without affecting the component’s function.
Examples include:
- Using practical internal corner radii.
- Avoiding unnecessarily deep and narrow pockets.
- Providing adequate tool access to ports and holes.
- Clarifying which dimensions are functionally critical.
- Reducing unnecessary setups where possible.
- Considering material utilization during the design stage.
The CNC part geometry optimization guide provides further ideas for improving manufacturability.
6. Quality Inspection and Functional Verification
Inspection should focus on the characteristics that affect assembly, sealing, and component function.
Dimensional Inspection
Depending on the component, inspection may include:
- External dimensions and overall geometry.
- Bore diameters and depths.
- Thread size and thread condition.
- Hole position and spacing.
- Groove width and depth.
- Flatness and parallelism of mating surfaces.
- Critical geometric relationships.
Suitable instruments may include micrometers, bore gauges, thread gauges, height gauges, and coordinate measuring machines.
The inspection method should match the dimension and tolerance being evaluated.
First-Article Inspection
First-article inspection verifies that an initial production part conforms to the approved drawing and specifications.
It can be useful for new components, revised designs, and projects involving multiple machining operations.
The inspection report should identify the relevant drawing revision and measured characteristics so that the buyer can evaluate the result against the approved requirements.
Material and Process Traceability
Some industrial customers require material certificates, heat-treatment records, finishing documentation, or batch traceability.
These requirements should be confirmed before production because they may influence supplier selection, material sourcing, and documentation costs.
MFG SOLUTION provides additional guidance through its quality assurance standards for CNC machining and ISO 9001 precision machining guide.
Any certification or specific inspection capability should be confirmed for the actual manufacturing project.
Cleanliness and Internal Passage Inspection
For fluid-control components, machining debris and residual contamination should be addressed before delivery.
The required cleaning method depends on the component design, fluid system, operating environment, and customer specification.
Where internal passages are difficult to inspect visually, the buyer and manufacturer should agree on appropriate verification and documentation methods.
7. Cost Control and Production Planning
Hydraulic and pneumatic components can contain several precision features, but not every feature needs the same level of manufacturing effort.
A practical cost-control strategy begins with understanding which characteristics are essential to the component’s function.
Allocate Tolerances According to Function
Tight tolerances may be necessary for sealing interfaces, locating bores, or specific mating features.
Other dimensions may only need standard machining tolerances.
Applying unnecessarily tight tolerances to all dimensions can increase cycle time, inspection effort, and rejection risk.
See why CNC machining tolerance drives part price and the machining tolerances guide.
Reduce Unnecessary Machining Operations
Designs with excessive pockets, complicated internal corners, or difficult tool access may require additional operations.
Where engineering requirements permit, simplifying these features can reduce machining time and improve inspection accessibility.
Consider Material and Stock Size
Material cost can be significant for components machined from solid blocks.
The selected stock size should provide sufficient machining allowance without creating unnecessary material waste.
For some components, alternative stock forms may be worth discussing with the manufacturer, provided the material and process remain suitable for the application.
Evaluate Prototype and Production Quantities
Prototype manufacturing may prioritize flexibility and design validation. Repeated production may justify dedicated fixtures, standardized inspection procedures, and documented machining programs.
The quotation should reflect actual order quantity, expected repeat demand, finishing, inspection, and packaging requirements.
For a broader cost-planning perspective, review the CNC machining cost analysis guide.
8. What to Include in an RFQ for Hydraulic and Pneumatic Components
A complete RFQ helps the manufacturer evaluate technical feasibility and prepare a more reliable quotation.
Buyers should provide the following information wherever applicable:
- 2D engineering drawings: Include dimensions, tolerances, datum references, thread specifications, and geometric controls.
- 3D CAD files: Supply STEP or another agreed format to clarify the component geometry.
- Material specification: State the exact alloy, grade, temper, or engineering plastic.
- Operating conditions: Provide relevant pressure, temperature, fluid, and environmental information.
- Port and thread details: Identify the thread standard, nominal size, depth, and sealing arrangement.
- Critical sealing features: Highlight O-ring grooves, mating faces, bore surfaces, and other functional interfaces.
- Surface treatment: Specify coating, plating, anodizing, masking, or other finishing requirements.
- Inspection requirements: Identify dimensional reports, material certificates, first-article inspection, and traceability requirements.
- Quantity and delivery: State prototype quantity, production volume, expected repeat orders, and target delivery schedule.
If a component has special internal passage or cleanliness requirements, include these details in the RFQ instead of relying on a general note.
MFG SOLUTION can review drawings and manufacturing requirements for custom components. Start through the online quotation page or contact the team through the MFG SOLUTION contact page.
You can also review the company’s manufacturing capabilities before preparing a project inquiry.
9. Frequently Asked Questions
1. Which materials are commonly used for CNC-machined hydraulic components?
Aluminum, stainless steel, carbon steel, alloy steel, and brass may be used depending on the component’s function. Material selection should consider operating pressure, mechanical loading, corrosion exposure, fluid compatibility, and manufacturing requirements.
2. What is the difference between machining a hydraulic manifold and a valve body?
A hydraulic manifold primarily distributes fluid through a network of interconnected passages and ports. A valve body houses valve mechanisms and related control features. Both may require precision bores, ports, threads, and sealing interfaces, but their functional geometry and inspection priorities can differ.
3. Why are internal burrs a concern in hydraulic manifold blocks?
Burrs may restrict passages, interfere with assembly, or become loose during operation. They should be considered during machining and deburring planning, especially where several drilled passages intersect.
4. Does every hydraulic component require a tight surface finish?
No. Surface-finish requirements depend on the function of each surface. Sealing faces, seal-running areas, and selected bores may require controlled finishes, while nonfunctional exterior surfaces may use less demanding specifications.
5. Can CNC machining produce custom pneumatic valve components?
Yes. CNC milling and turning can produce custom valve housings, actuator components, mounting blocks, connectors, and other pneumatic parts. The process depends on the geometry, material, quantity, and dimensional requirements.
6. What thread information should be included in a hydraulic component drawing?
Specify the thread standard, nominal size, pitch where applicable, depth, and sealing arrangement. Clearly distinguish between thread standards such as metric, BSP, and NPT to avoid connection and assembly problems.
7. What inspection documents should buyers request?
Depending on the project, buyers may request dimensional inspection reports, first-article inspection results, material certificates, finishing records, and batch traceability documents. Requirements should be agreed before production.
8. How can buyers reduce the cost of custom hydraulic and pneumatic parts?
Provide complete drawings, identify critical dimensions, avoid unnecessary tolerance tightening, simplify difficult-to-machine features where possible, and confirm material, quantity, finishing, and inspection requirements before production.
Conclusion: Reliable Hydraulic and Pneumatic Components Start with Manufacturing Planning
CNC machining plays an important role in producing custom hydraulic and pneumatic equipment components, including valve bodies, manifold blocks, cylinder parts, piston rods, end caps, fittings, and mounting interfaces.
Reliable production requires careful attention to material selection, port geometry, intersecting passages, sealing surfaces, dimensional relationships, deburring, cleanliness, and inspection.
The most effective manufacturing strategy begins with the component’s actual operating requirements. By identifying functional features and communicating them clearly in the engineering drawing and RFQ, buyers can help manufacturers select suitable processes, reduce avoidable production risks, and control machining costs.
MFG SOLUTION supports custom CNC-machined components for industrial equipment and engineering applications.
If you are sourcing hydraulic or pneumatic components, send your drawings, material requirements, quantities, and technical specifications for manufacturing review.
Request a quotation: https://mfg-solution.com/online-quote/
Contact MFG SOLUTION: https://mfg-solution.com/contact-mfg-solution/
Explore CNC machining services: https://mfg-solution.com/cnc-machining/