
2026-07-17
1045 Steel Turned Parts: Guide & Applications

1045 steel turned parts are CNC-machined components produced from medium-carbon steel (0.43–0.50% carbon) prized for its balance of strength, machinability, and cost. With a tensile strength of roughly 570–700 MPa in the as-rolled condition and excellent response to heat treatment, 1045 is a go-to material for shafts, pins, studs, and bushings across automotive, industrial, and general engineering applications. It machines cleanly on CNC lathes and automatic lathes, holding tight tolerances without excessive tool wear.
What Makes 1045 Steel Turned Parts the Default Choice for Medium-Duty Components
1045 steel dominates medium-duty CNC turning because it delivers tensile strength between 570–700 MPa as-rolled, machines without rapid tool wear, and costs 15–25% less per kg than alloy alternatives.
The 0.43–0.50% carbon content sits in a practical sweet spot. Below that range, steels like 1018 top out near 400 MPa tensile strength, adequate for light brackets but undersized for shafts or hydraulic cylinder rods under cyclic load. Above it, grades like 4140 reach 655–1020 MPa depending on condition, but carry a price premium and require tighter process control during machining. 1045 occupies the middle ground most mechanical engineers reach for first.
A normalized Brinell hardness of 163–179 HB keeps cutting forces manageable on CNC lathes and automatic lathes. That hardness range allows consistent chip formation and predictable tool life across long production runs, a practical advantage when batch sizes reach the hundreds or thousands.
“Medium-carbon steels like 1045 represent the workhorse of the turned parts industry — they offer a compelling combination of strength, ductility, and machinability that alloy steels simply cannot match at the same price point.” — Dr. James R. Davis, Senior Editor, Metals Handbook, ASM International
According to ASM International, the world’s largest association of materials engineers and scientists, medium-carbon steels in the 1040–1050 range consistently rank among the most widely specified grades for machined mechanical components due to their predictable heat treatment response and broad availability in bar stock form.
1045 vs. 1018 vs. 4140: Choosing the Right Grade for Your Turned Part
The selection comes down to load, surface requirement, and budget. The following comparison highlights the key differences between the three most common grades for turned parts:
- 1018 steel: Low carbon (0.15–0.20%), tensile strength ~400 MPa, excellent weldability, best for light-duty brackets, pins, and non-structural components where strength is not critical.
- 1045 steel: Medium carbon (0.43–0.50%), tensile strength 570–700 MPa as-rolled, good machinability, ideal for shafts, coupling pins, hydraulic rods, and general mechanical components.
- 4140 steel: Alloy steel with chromium and molybdenum, tensile strength 655–1020 MPa depending on heat treatment condition, superior fatigue resistance, suited for high-stress drivetrain and tooling applications at a 15–25% cost premium.
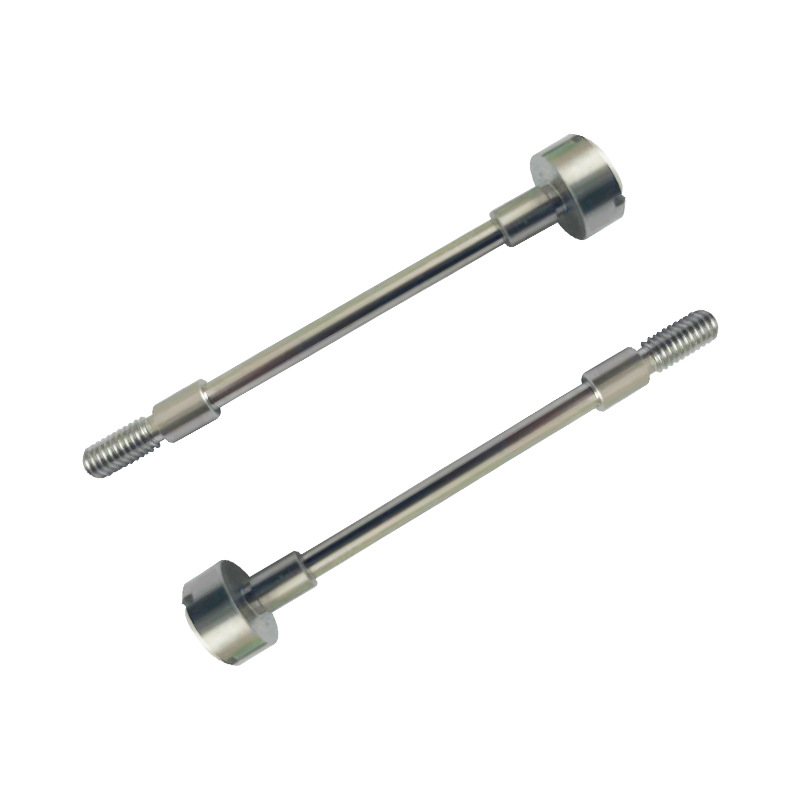
Drive shafts and coupling pins in industrial gearboxes are classic 1045 applications — the material handles torsional and bending loads that would plastically deform 1018, while avoiding the alloy surcharge of 4140. Hydraulic cylinder rods are another common fit: 1045 steel turned parts hold the dimensional tolerances required for seal interfaces, and the material’s response to induction hardening protects the rod surface from wear without through-hardening the entire cross-section.
When a part demands surface hardness above 50 HRC across a thin case, such as a precision spindle or a heavily loaded bushing, 4140 or 4340 may justify the added cost. For the majority of medium-duty applications, 1045 bar stock at 15–25% lower cost per kg makes the economic case clearly.
How Heat Treatment Changes 1045 Turned Part Performance
Heat treatment is where 1045 earns its specification in wear-critical components. Induction hardening, through hardening, and case hardening all apply, and surface hardness can reach 54–60 HRC, sufficient for pins, studs, and shaft journals running against bearing surfaces. After quench and temper, tensile strength climbs to roughly 850 MPa, closing much of the gap with as-heat-treated 4140 at the lower end of that grade’s range.
The key trade-off is core toughness. 1045 through-hardened to full depth becomes more brittle than 4140 at equivalent hardness, so engineers typically specify induction hardening to preserve a tough core while protecting the surface. That combination — hard case, ductile core — is why 1045 remains the standard material for turned shafts and spindles in automotive and industrial drive systems.
“Induction hardening of medium-carbon steels produces a hard, wear-resistant surface layer while retaining a tough, ductile core — a combination that is difficult and expensive to replicate with through-hardened alloy steels.” — George E. Totten, Editor, Steel Heat Treatment Handbook, Taylor & Francis
CNC Turning Process for 1045 Steel: Speeds, Feeds, and Tolerances
CNC turning 1045 steel runs efficiently at 180–250 m/min with carbide tooling, holding diameter tolerances of ±0.01 mm in standard production.
For roughing passes, a feed rate of 0.15–0.35 mm/rev removes material quickly without overloading the insert. Finishing passes drop to 0.05–0.10 mm/rev to achieve the surface quality that bearing fits and sealing surfaces require. Treat these as practical starting points — actual parameters shift with part geometry, machine rigidity, and batch size.
Tooling and Insert Selection for High-Volume 1045 Turning Runs
ISO P20–P30 grade carbide inserts outperform high-speed steel for 1045 at production volumes, handling the material’s moderate hardness without rapid edge wear. Coated inserts — TiN or TiAlN coatings — extend tool life by 30–50% on long-run jobs, which directly reduces per-part cost when producing 1045 steel turned parts in the thousands.
Coolant selection is equally critical. Water-soluble cutting fluid at 8–10% concentration controls thermal expansion at the cutting zone, keeping the workpiece dimensionally stable across an entire batch. Without adequate coolant, heat buildup shifts diameter readings by several microns, enough to push parts outside tolerance on tight-fit applications. For a full breakdown of fluid types and application methods, refer to the CNC coolants and lubricants reference on the MFG SOLUTION site.
Holding Tight Tolerances on 1045 Turned Shafts and Pins
Standard CNC turning holds ±0.01 mm on diameter for most shaft and pin geometries. On small-diameter parts under 20 mm, Swiss lathe and automatic lathe setups — both available at MFG SOLUTION across 20 dedicated machines — achieve ±0.005 mm, which matters for precision pins, needle rollers, and close-clearance bores. For more information, see Thegoodcode.
Surface finish follows the same tiered logic. A single turning pass delivers Ra 1.6 µm, adequate for most functional surfaces. Adding a dedicated finishing pass brings Ra down to 0.8 µm, the threshold for sealing surfaces and interference-fit bearing journals where roughness directly affects performance life.
Secondary Operations That Add Value to 1045 Steel Turned Parts
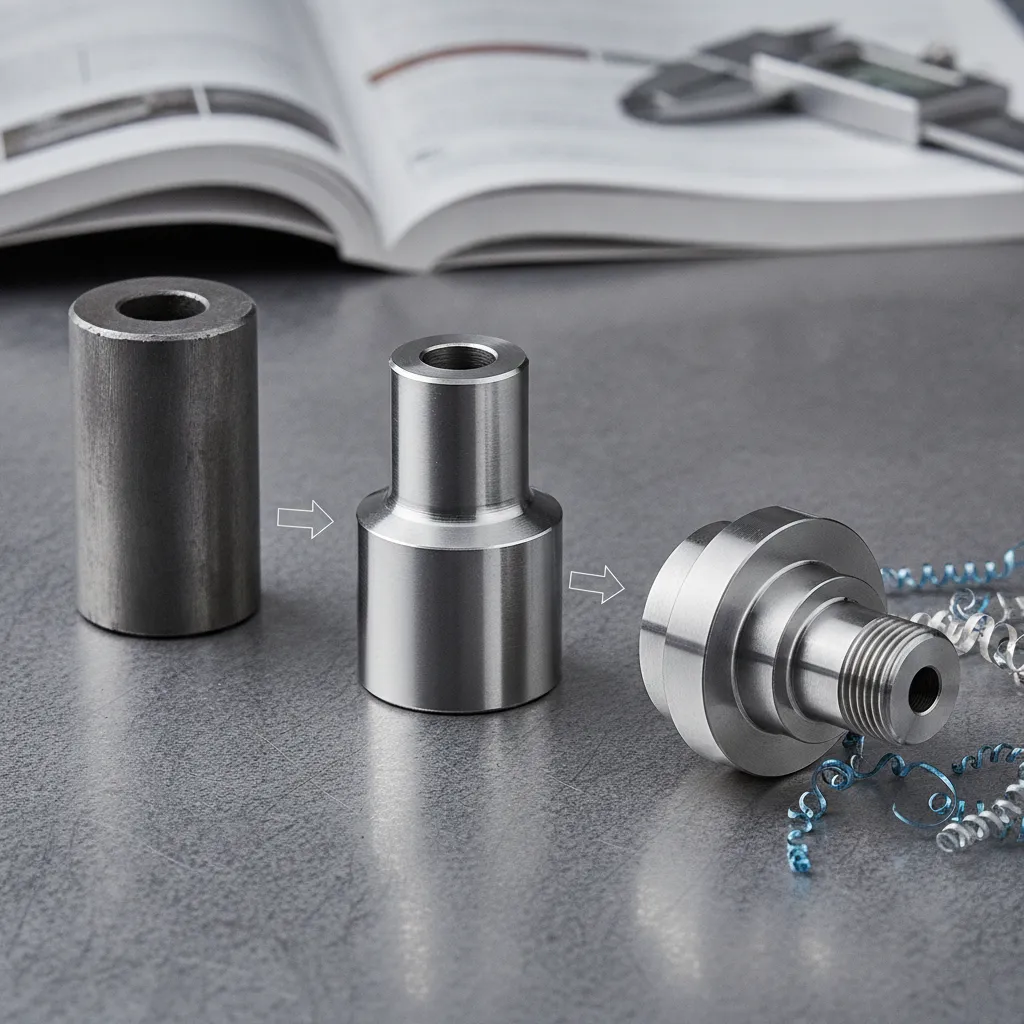
Threading, drilling, heat treatment, and surface finishing are the four secondary operations that most directly affect the performance and cost of 1045 steel turned parts.
Threading and Cross-Drilling 1045 Turned Parts in a Single Setup
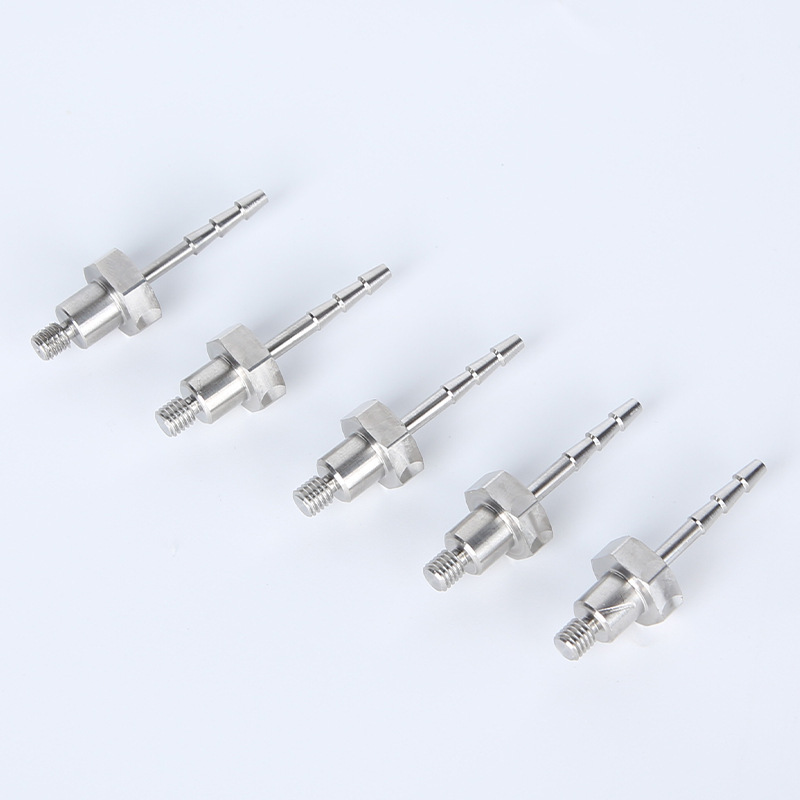
CNC threading is the most common secondary operation on 1045 turned parts. The material cuts cleanly with standard tooling across the M6 through M64 thread range, using either single-point threading or thread milling depending on thread depth and tolerance class. MFG SOLUTION’s CNC threading services cover both methods within the same production run.
Cross-drilling and axial hole drilling performed on a mill-turn center eliminate a separate fixture setup entirely. That single-setup approach removes positioning error and reduces cycle time. For process specifics on hole geometry and depth control, MFG SOLUTION’s CNC hole drilling technology page covers the parameters in detail.
Heat treatment sequencing is where dimensional discipline matters most. The standard sequence — rough turn, heat treat, finish turn — exists because skipping the final pass after heat treatment risks dimensional drift of 0.02–0.05 mm, which puts tight-tolerance features outside spec. The finish pass corrects that drift before the part ships.
Surface finishing adds 1–3 days to lead time regardless of the process chosen. The most common surface finishing options for 1045 steel turned parts, ranked by dimensional impact, are:
- Black oxide: Corrosion protection with dimensional change under 0.001 mm — the default choice when tolerances are tight.
- Zinc plating: Greater corrosion resistance than black oxide, adds 5–15 µm per side — must be accounted for in design tolerances.
- Electroless nickel: Excellent corrosion and wear resistance, adds 15–25 µm per side with very uniform coverage on complex geometries.
- Hard chrome: Maximum wear resistance, adds 25–75 µm per side — typically specified for hydraulic rod surfaces and high-wear journals.
Deburring is non-negotiable on any threaded or drilled 1045 part. Sharp edges on threads cause assembly failures; burrs in drilled holes trap contaminants. MFG SOLUTION’s CNC deburring process is integrated into the production flow rather than treated as an afterthought.
Quality Standards and Inspection for 1045 Turned Parts
Qualified suppliers of 1045 steel turned parts hold ISO 9001:2015 and IATF 16949 certification and back every shipment with documented dimensional and material records.
ISO 9001:2015 requires documented process control, full traceability from raw material to finished part, and a corrective action system when nonconformances occur. IATF 16949 adds automotive-specific requirements: production part approval, measurement system analysis, and statistical process monitoring. Together, they give buyers auditable evidence that each batch was made and inspected to a controlled procedure.
Dimensional verification on turned parts centers on CMM (coordinate measuring machine) inspection. For a 1045 steel shaft, acceptable runout is typically ≤0.02 mm TIR for general industrial fits and ≤0.005 mm TIR where precision bearing seats are involved. CMM reports capture critical diameters, concentricity, and surface finish against the drawing callout, not just a spot check.
According to the National Institute of Standards and Technology (NIST) Manufacturing Program, dimensional traceability and documented measurement uncertainty are foundational requirements for any precision machined component entering a regulated or safety-critical supply chain. Buyers should verify that their supplier’s CMM equipment carries current NIST-traceable calibration certificates.
Tolerance stackup is a real risk when multiple turned parts assemble into a single mechanism. Engineers managing fit and function across a component stack should review the precision tolerance stackup resource before finalizing drawings.
What to Ask Your Supplier for Material and Dimensional Traceability
Always request a material test report (MTR), sometimes called a mill cert, confirming carbon content (0.43–0.50%), tensile strength, and yield strength for every heat lot. For safety-critical parts, no MTR means no shipment.
First Article Inspection (FAI) is required on any new part number before production quantities release. FAI covers a full dimensional layout, material verification, and functional check against the drawing. It protects the buyer from tooling errors and protects the supplier from disputes over whether the approved sample matched the production run.
“First Article Inspection is not a bureaucratic formality — it is the single most effective tool for catching tooling and process errors before they propagate across an entire production batch.” — Mark A. Schmitt, Quality Systems Director, Society of Manufacturing Engineers (SME)
MFG SOLUTION, certified to ISO 9001:2015 and IATF 16949, provides CMM reports, MTRs, and FAI packages as standard documentation, with quotes returned within 8 hours of specification submission.
Industries and Applications Where 1045 Turned Parts Deliver the Best ROI
1045 steel turned parts deliver the strongest return in automotive, industrial machinery, and general engineering, where moderate-to-high strength, machinability, and volume economics align.
Automotive
Transmission shafts, steering column pins, and brake anchor bolts are three of the highest-volume applications. 1045 meets SAE J403 grade requirements for medium-carbon steel and fits directly into IATF 16949-compliant supply chains, the same standard MFG SOLUTION holds, which simplifies supplier qualification for automotive OEMs.
Industrial Machinery
Hydraulic cylinder rods, conveyor drive shafts, and gearbox studs all benefit from 1045’s fatigue resistance. Under R.R. Moore fully reversed testing, 1045 sustains a fatigue limit of approximately 300 MPa, enough for most cyclic-load applications in pumps, conveyors, and power transmission assemblies. According to SME (Society of Manufacturing Engineers), medium-carbon steels remain the dominant material choice for power transmission shafts in North American industrial machinery due to their predictable fatigue behavior and broad machinability across standard CNC turning platforms.
Medical Device Adjacent
1045 is not implant-grade and should never be specified for in-body components. It does appear in non-implant equipment frames, jigs, and fixturing where corrosion is controlled. For implant-grade work, 316L stainless or titanium is the correct call, and MFG SOLUTION’s ISO 13485:2016-certified CNC machining service covers both.
Volume Economics
Bar stock runs from 6 mm to 300 mm in standard diameters, which suits automatic bar-feed lathes for uninterrupted production. On runs of 1,000–50,000 pieces, cost per part drops sharply because setup amortizes across the batch and material waste stays low.
When 1045 Is the Wrong Choice
Two situations disqualify it. Thin-wall parts with less than 3 mm wall thickness risk distortion during quench-and-temper heat treatment. Corrosive environments — salt spray, chemical wash, or outdoor exposure — require either a coated alternative or a stainless grade from the start.
Frequently Asked Questions
What is the difference between 1045 steel and 4140 steel for turned parts?
1045 steel offers good machinability and moderate strength, while 4140 steel delivers higher tensile strength and better hardenability for demanding applications. 1045 has a carbon content of roughly 0.43–0.50%, making it easier to machine and weld at lower cost. 4140 contains chromium and molybdenum, which improve fatigue resistance and toughness under cyclic loading. For shafts, pins, and structural components where cost matters more than extreme strength, 1045 is the practical choice. High-stress drivetrain or tooling parts typically warrant 4140.
Can 1045 steel turned parts be welded after machining?
Yes, 1045 steel can be welded after machining, but preheating to 150–260°C is recommended to reduce the risk of heat-affected zone cracking. The medium carbon content raises hardenability in the weld zone, so post-weld stress relief at around 595°C helps restore ductility. Use low-hydrogen electrodes and follow established AWS D1.1 structural welding guidelines for best results.
What surface finish is achievable on 1045 CNC turned parts without grinding?
CNC turning on 1045 steel can achieve a surface finish of Ra 0.8–1.6 µm as a standard result, with Ra 0.4 µm reachable using fine finishing passes and sharp tooling. Swiss lathe machining can push tolerances tighter still on small-diameter parts. Grinding is only necessary when the application demands Ra values below 0.4 µm or very tight dimensional tolerances beyond ±0.005 mm.
How long does it take to get a quote and lead time for 1045 steel turned parts?
At MFG SOLUTION, you receive a quote within 8 hours of submitting your part specifications, and approved orders ship within 3 days. That turnaround applies to batch production runs on parts up to 38mm in diameter. Submit your drawing at mfg-solution.com to start the process today.
What certifications should a supplier of 1045 steel turned parts hold?
At minimum, look for ISO 9001:2015 certification, which ensures documented process control and full material traceability. For automotive supply chains, IATF 16949 is required and covers production part approval, statistical process monitoring, and measurement system analysis. Suppliers serving medical-adjacent or aerospace markets should additionally hold ISO 13485:2016 or AS9100D. Always request current certification documents and verify expiry dates before placing production orders.
Conclusion
1045 steel hits a practical balance point that most turned-part applications actually need: enough strength for structural and mechanical duty, carbon content that machines cleanly, and a cost profile that holds up across production volumes. The key decisions are heat treatment timing, tolerance allocation between turning and finishing, and matching the production method — CNC turning, Swiss lathe, or automatic lathe — to your part geometry.
If your parts fall under 38mm in diameter and you need certified quality backed by ISO 9001:2015, ISO 13485:2016, or IATF 16949, submit your drawing to MFG SOLUTION at mfg-solution.com and get a detailed quote within 8 hours.
Recommended Articles
Explore more from our content library: