
2026-04-30
CNC Machining Surface Finish: A Complete Guide

| Key Insight | Explanation |
|---|---|
| Ra is the universal roughness metric | Ra (arithmetic mean roughness) is the most widely used parameter to specify and compare surface finish in CNC machining, measured in micrometers (μm) or microinches (μin). |
| Ra 3.2 μm is the default standard | Most standard milling and turning operations produce Ra 3.2 μm (125 μin) without additional post-processing, making it the baseline for general-purpose machined parts. |
| Finish affects function, not just looks | Surface finish directly impacts fatigue strength, friction, corrosion resistance, sealing capability, and dimensional fit — especially critical for medical and automotive components. |
| Cutting parameters drive roughness outcomes | Feed rate, spindle speed, tool nose radius, and depth of cut are the four primary variables that machinists adjust to achieve a target surface finish specification. |
| Post-process finishing expands the range | Anodizing, electropolishing, bead blasting, and vibratory finishing can push surface quality from Ra 3.2 μm down to Ra 0.1 μm or better for demanding applications. |
| Certifications validate finish compliance | ISO 9001:2015, ISO 13485:2016, and IATF 16949 frameworks require documented surface finish verification, ensuring traceability and repeatability across production runs. |
Surface finish CNC machining is the process of controlling and refining the texture of a machined part’s outer layer to meet functional and aesthetic requirements. It is defined by measurable parameters such as Ra (arithmetic mean roughness), Rz (mean peak-to-valley height), and Rq (root mean square roughness). Getting it right determines whether a part seals properly, survives fatigue loading, or passes a regulatory inspection.
Most engineers encounter surface finish as a callout on a drawing: a small triangle symbol followed by a number like Ra 1.6 or Ra 3.2. But the topic runs much deeper than that. The finish you specify affects your machining time, your cost, your part’s corrosion resistance, and — in medical or automotive applications — your compliance status under ISO 13485:2016 or IATF 16949. This is particularly relevant for surface finish CNC machining.
This guide covers everything you need: the measurement parameters, the finish types available, the variables that drive roughness outcomes, common mistakes teams make, and the best practices that separate average parts from precision-grade components.

What Is Surface Finish in CNC Machining?
Surface finish in CNC machining refers to the measurable texture of a part’s surface after cutting, defined by parameters like Ra (roughness average) and Rz. It directly affects part performance, longevity, and compliance with industry standards.
According to Wikipedia’s entry on surface finish, surface texture is defined by three characteristics: lay (the predominant direction of surface pattern), waviness (the wider spaced component of surface texture), and roughness (the finer, closely spaced irregularities) [1]. All three matter, but roughness is the parameter most commonly specified in manufacturing drawings.
The Core Measurement Parameters
Ra is the arithmetic mean of the absolute values of the surface profile deviations from the mean line, measured in micrometers (μm) or microinches (μin). It’s the most universally used parameter because it’s easy to measure and interpret [2]. When considering surface finish CNC machining, this point stands out.
- Ra (Roughness Average): The mean deviation across the measured length. The most common callout on engineering drawings.
- Rz (Mean Roughness Depth): The average of the five highest peak-to-valley distances. More sensitive to extreme surface events like scratches or burrs.
- Rq (RMS Roughness): The root mean square of profile deviations. Slightly higher than Ra numerically; preferred in optics and electronics applications.
- Rt (Total Roughness): The maximum peak-to-valley height across the entire measurement length. Used where a single defect could cause failure.
Why the Definition Matters for Engineers
Specifying the wrong parameter — or the wrong value — creates real problems. A part designed for a dynamic sealing application needs a tight Ra specification (typically Ra 0.8 μm or better) to prevent leakage. Calling out Ra 3.2 μm on that same drawing is a design error, not a machining error. Understanding what each parameter measures prevents those costly mismatches.
Research published in IOP Conference Series: Materials Science and Engineering confirms that surface roughness Ra is the most critical output variable in determining the functional quality of machined components across industries [3]. Getting this parameter right from the design stage is far cheaper than correcting it after parts are made.
How Surface Finish CNC Machining Works
Surface finish in CNC machining is produced by the interaction of the cutting tool, workpiece material, and machine parameters — each variable leaving a measurable signature on the part surface.
Every pass of a cutting tool leaves a pattern of peaks and valleys on the workpiece. The height and spacing of those features are what roughness instruments measure. Four variables control this outcome more than any others [4]. For those exploring surface finish CNC machining, this matters.
The Four Primary Variables
- Feed rate: The distance the tool advances per spindle revolution. Lower feed rates produce finer finishes. This is typically the single most impactful variable.
- Cutting speed (SFM/RPM): Higher speeds generally reduce built-up edge on the tool and produce smoother cuts, especially with carbide tooling.
- Tool nose radius: A larger nose radius spreads the feed mark over a wider area, reducing peak height and improving Ra. The theoretical minimum Ra from turning is directly calculable from feed and nose radius.
- Depth of cut: Shallower finishing passes reduce cutting forces and vibration, improving surface consistency.
According to research from the National Institutes of Health’s PubMed Central, optimizing cutting temperature alongside these parameters significantly enhances surface finish outcomes, particularly when machining harder alloys where thermal effects accelerate tool wear and surface degradation [5].
The Role of Machine Rigidity and Toolpath Strategy
Machine stiffness matters just as much as cutting parameters. Vibration (chatter) creates periodic surface errors that no parameter adjustment can fully eliminate if the machine or fixturing is inadequate. At MFG SOLUTION, we’ve found that 5-axis CNC machining allows shorter tool overhangs and more favorable cutting angles, which directly reduces chatter and produces more consistent surface finishes across complex geometries.
Toolpath strategy also plays a role. Climb milling (where the cutter engages the workpiece in the direction of feed) typically produces better finishes than conventional milling because chip thickness decreases as the tool exits the cut, reducing rubbing and heat buildup [6].
Pro Tip: For CNC turning operations, use the theoretical Ra formula: Ra ≈ (f² / 8r) × 1000 μm, where f is feed per revolution in mm and r is tool nose radius in mm. This gives you a target starting point before cutting the first chip.
Types of Surface Finishes for CNC Parts
CNC machined parts can receive a wide range of surface finishes, from the as-machined texture left by the cutting tool to highly refined post-process treatments that achieve mirror-quality surfaces. This directly impacts surface finish CNC machining outcomes.
As detailed by Hubs’ knowledge base on CNC surface finishes, the finishing options broadly split into two categories: as-machined finishes produced during the cutting process itself, and secondary finishing processes applied after machining [7].
As-Machined and Mechanical Finishes
| Finish Type | Typical Ra Range | Common Applications | Relative Cost |
|---|---|---|---|
| As-machined (standard) | Ra 1.6–3.2 μm | General structural parts, brackets, housings | Lowest |
| Bead blasting | Ra 1.6–3.2 μm | Cosmetic parts, uniform matte appearance | Low |
| Vibratory / tumble finishing | Ra 0.4–1.6 μm | Small batch deburring, edge rounding | Low–Medium |
| Anodizing (Type II / Type III) | Preserves machined Ra; adds 5–25 μm layer | Aluminum aerospace, electronics enclosures | Medium |
| Electropolishing | Ra 0.1–0.4 μm | Medical implants, food-grade stainless parts | High |
| Grinding / lapping | Ra 0.025–0.4 μm | Bearing surfaces, precision gauges, sealing faces | Highest |
Choosing the Right Finish for Your Application
The right finish isn’t always the smoothest finish. Overly smooth surfaces can actually reduce lubrication retention in sliding applications, where a controlled Ra 0.8–1.6 μm texture helps oil film adhere. Fictiv’s finishing guide notes that matching the finish to the functional requirement is more important than chasing the lowest Ra number [8].
- Sealing surfaces: Ra 0.4–0.8 μm, with lay direction perpendicular to the seal
- Sliding/bearing surfaces: Ra 0.4–1.6 μm depending on lubrication type
- Cosmetic/exterior surfaces: Bead blast or anodize to Ra 1.6–3.2 μm
- Medical implants: Electropolish to Ra ≤ 0.4 μm per ISO 13485:2016 requirements
- Structural, non-contact surfaces: As-machined Ra 3.2 μm is typically sufficient

Key Benefits: Why Surface Finish Matters in 2026
Surface finish directly affects a part’s mechanical performance, service life, and regulatory compliance — making it a functional specification, not just a cosmetic preference.
As of 2026, supply chain quality requirements from automotive and medical OEMs have tightened considerably. IATF 16949 surveillance audits now routinely include surface finish verification as part of the Production Part Approval Process (PPAP), and ISO 13485:2016 auditors increasingly flag inadequate surface documentation as a nonconformance. Getting surface finish right isn’t optional for suppliers in these sectors. This is particularly relevant for surface finish CNC machining.
Functional Performance Advantages
- Fatigue life: Smoother surfaces reduce stress concentration at surface irregularities. Research indicates that reducing Ra from 3.2 μm to 0.8 μm can improve fatigue strength by 15–30% in steel components [3].
- Corrosion resistance: Rougher surfaces have greater exposed area and more crevices for corrosive media to accumulate. Electropolishing stainless steel to Ra ≤ 0.4 μm measurably improves its passive oxide layer integrity.
- Friction and wear: Controlled surface texture reduces the running-in period for mating parts and stabilizes the coefficient of friction over the component’s service life.
- Sealing effectiveness: Gasket and O-ring interfaces require specific Ra ranges. Too rough and the seal leaks; too smooth and the gasket can’t conform and micro-leak under pressure cycling.
- Dimensional accuracy: Post-process finishes like hard anodizing add measurable material to the surface. Accounting for coating thickness in the design stage prevents out-of-tolerance assemblies.
Commercial and Compliance Benefits
Beyond performance, surface finish has direct commercial implications. Parts rejected for surface quality at incoming inspection are expensive: they require rework or replacement, delay assembly schedules, and damage supplier relationships. Industry analysts note that surface-finish-related rework accounts for a disproportionate share of quality costs in high-mix, low-volume precision machining environments.
Our team at MFG SOLUTION recommends documenting surface finish requirements explicitly in the purchase order and drawing package — not leaving them to default assumptions. When your drawing specifies Ra 1.6 μm and the supplier defaults to Ra 3.2 μm, the resulting nonconformance is avoidable with a single line of specification text.
Pro Tip: For medical device components, always specify both Ra and Rz on your drawings. Ra alone doesn’t capture isolated deep scratches or burrs that Rz will flag. ISO 13485:2016 auditors expect both parameters to be controlled and recorded.
Common Challenges and Mistakes to Avoid
The most common surface finish failures in CNC machining stem from specification errors, tool wear, vibration, and inadequate process control — all of which are preventable with the right approach.
A precision machining client recently faced a batch rejection from their automotive customer because connector housings arrived with Ra 2.8 μm on a sealing face specified at Ra 0.8 μm. The root cause wasn’t a machining error. It was a drawing that omitted the surface finish callout entirely, leaving the machine shop to apply a default standard finish. One missing symbol cost three weeks of rework time. When considering surface finish CNC machining, this point stands out.
Specification and Design Mistakes
- No finish callout on the drawing: Suppliers default to Ra 3.2 μm (or whatever their shop standard is) when nothing is specified. Always call out critical surfaces explicitly.
- Specifying tighter finishes than necessary: Calling Ra 0.4 μm on a non-contact structural surface adds cost with no functional benefit. Over-specification is as problematic as under-specification.
- Ignoring lay direction: For sealing surfaces, the direction of surface texture relative to the seal path matters. A circumferential lay on a shaft seal is very different from an axial lay.
- Not accounting for coating thickness: Hard anodizing adds 12–25 μm per surface. If you don’t account for this, bores and external diameters will be out of tolerance after coating.
Process and Machining Mistakes
- Running worn tooling too long: Tool wear is the single most common cause of surface finish degradation in production runs. A worn tool nose radius increases Ra dramatically. The Precision Machined Products Association recommends proactive tool change intervals based on cut count, not just visual inspection [4].
- Inadequate chip evacuation: Chips re-cutting the workpiece surface create random deep scratches that no parameter setting can prevent. Proper coolant direction and chip clearance are essential.
- Chatter from poor fixturing: Vibration during cutting creates periodic waviness that shows up as a characteristic pattern under magnification and degrades Ra significantly.
- Inconsistent coolant application: Thermal gradients from inconsistent coolant cause workpiece expansion and contraction during cutting, producing variable surface texture across the part length.
According to DATRON’s CNC surface finish guide, one of the most overlooked factors is spindle runout — even 0.005 mm of runout can degrade surface finish by a full Ra grade in high-speed finishing operations [6].
Best Practices for Surface Finish in 2026
Achieving consistent, specification-compliant surface finish in CNC machining requires a systematic approach covering drawing specification, process parameter selection, tooling management, and in-process measurement.
In practice, the shops that consistently hit surface finish specs aren’t doing anything exotic. They’re disciplined about the fundamentals: clear specifications, calibrated tooling, and measurement at the right points in the process.
Drawing and Specification Best Practices
- Use ISO 1302 surface texture symbols on all engineering drawings. This standard defines how to call out Ra, Rz, lay, and machining method requirements unambiguously.
- Specify the measurement parameter and value (e.g., Ra 1.6 μm, not just “smooth finish”). Vague callouts create supplier interpretation gaps.
- Identify critical surfaces explicitly. Use a general note for non-critical surfaces (e.g., “all surfaces Ra 3.2 μm unless otherwise noted”) and call out tighter requirements on individual features.
- Include finish requirements in your RFQ package. If you submit drawings without surface finish callouts, you’ll get default finishes that may not meet your application needs.
Process and Production Best Practices
- Optimize feed rate first. For a given tool nose radius, halving the feed rate reduces theoretical Ra by approximately 75%. This is the highest-leverage parameter adjustment available [4].
- Use the largest practical tool nose radius for finishing passes. A 0.8 mm nose radius produces significantly better finish than a 0.4 mm radius at the same feed rate.
- Separate roughing and finishing passes. Don’t try to achieve final surface finish in the same pass that removes bulk material. Dedicated finishing passes with lower feed and depth of cut produce consistent results.
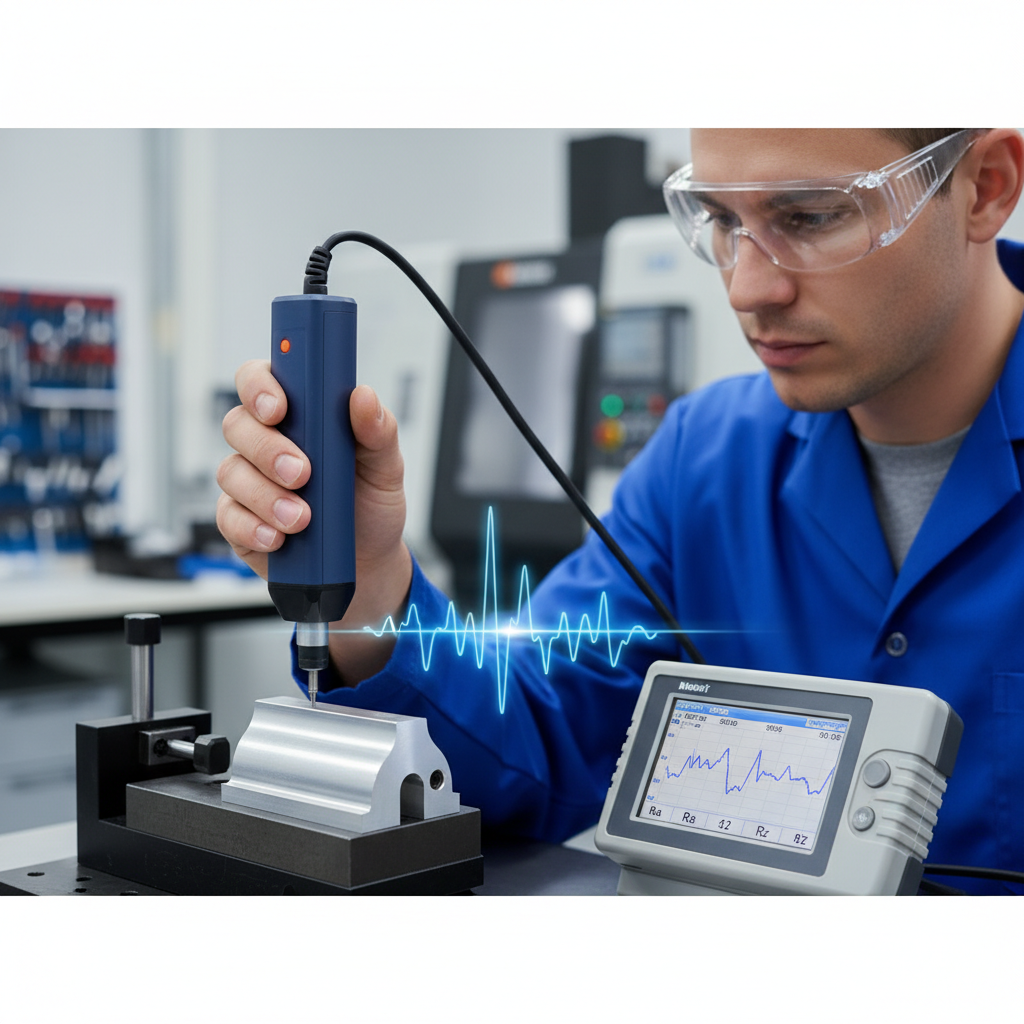
- Measure in-process, not just at final inspection. Profilometer checks after the first finishing pass allow parameter adjustments before the entire batch is run. Geomiq’s surface roughness guide recommends first-article surface verification as a standard quality gate [2].
- Document tool change intervals and enforce them. Proactive replacement based on cut count prevents the gradual Ra drift that causes end-of-batch nonconformances.
Pro Tip: When quoting surface finish CNC machining jobs, always ask your supplier for a first-article inspection report (FAIR) that includes profilometer data. Any ISO 9001:2015-certified shop should be able to provide this as standard documentation — if they can’t, that’s a red flag about their process control capability.
As of 2026, digital profilometers with Bluetooth data logging are increasingly standard in precision machine shops, enabling real-time SPC (Statistical Process Control) charting of surface roughness data. This means surface finish variation can be caught and corrected within a production run rather than discovered at final inspection. Shops operating under IATF 16949 are expected to have this capability for critical surface characteristics. For those exploring surface finish CNC machining, this matters.
From experience, the combination of documented tool change intervals, dedicated finishing passes, and first-article profilometer verification eliminates the vast majority of surface finish nonconformances in high-volume small-part production. These aren’t advanced techniques — they’re disciplined fundamentals that separate reliable suppliers from inconsistent ones.
Sources & References
- Wikipedia, “Surface Finish,” 2026
- Geomiq, “Surface Roughness Guide for CNC Machining (Ra, Rz),” 2026
- IOP Science, “Effect of Machining Parameters on the Surface Roughness,” 2019
- Precision Machined Products Association (PMPA), “5 Tips to Improve Surface Finish On Your Precision Machined Parts,” 2026
- PubMed Central / NIH, “Optimization of Cutting Temperature and Surface Roughness in CNC Machining,” 2025
- DATRON, “Achieve The Perfect CNC Machining Surface Finish,” 2026
- Hubs, “What Are the Types of Surface Finishes for CNC Machining?” 2026
- Fictiv, “The Ultimate Guide to Finishing CNC Machined Parts,” 2026
- RapidDirect, “The Ultimate Guide to CNC Machining Surface Finish,” 2026
- HPPI, “Technical Guide: Surface Finishes | Precision CNC Machining,” 2026
Frequently Asked Questions
1. What is the standard surface finish for CNC machining?
The standard default surface finish for CNC machining is Ra 3.2 μm (125 μin), which is the typical result of a basic milling or turning operation without additional grinding, polishing, or post-processing. This finish is adequate for non-critical structural surfaces and general-purpose parts. However, applications involving sealing, sliding contact, or medical/automotive compliance typically require tighter specifications: Ra 1.6 μm for general precision surfaces, Ra 0.8 μm for sealing interfaces, and Ra 0.4 μm or better for medical implants and high-precision bearing surfaces. Always specify the required Ra value explicitly on your drawing rather than relying on a shop default.
2. How do you get a better surface finish on a CNC lathe?
Improving surface finish on a CNC lathe involves a combination of parameter adjustments and tooling choices. The most effective single change is reducing feed rate — halving the feed per revolution reduces theoretical surface roughness by approximately 75% for a given tool nose radius. Simultaneously, increasing cutting speed (especially with carbide inserts), using the largest practical tool nose radius, switching to wiper inserts for finishing passes, ensuring thorough chip evacuation to prevent re-cutting, and eliminating any dwell or pause in the toolpath all contribute to measurably better Ra values. For surface finish CNC machining on lathes, separating roughing and finishing passes is essential: don’t attempt to achieve your final Ra specification in a combined roughing cut.
3. What does Ra 3.2 surface finish mean?
Ra 3.2 μm (also expressed as 125 μin in imperial units) means the arithmetic mean of the absolute surface profile deviations from the mean centerline, measured over a standard sampling length, equals 3.2 micrometers. In practical terms, this is a visible machining mark finish — you can see and feel the tool path marks under normal lighting. It’s the standard as-machined result from conventional milling or turning and is suitable for non-contact structural surfaces. It is not appropriate for sealing faces, sliding surfaces, or medical-grade components, which typically require Ra 0.8 μm or finer.
4. What is the difference between Ra and Rz in surface finish?
Ra is the arithmetic mean roughness — the average deviation of the surface profile from its mean line across the measurement length. Rz is the mean roughness depth — the average of the five highest peak-to-valley distances within the measurement length. Ra gives a general picture of overall texture smoothness, while Rz is more sensitive to isolated deep scratches, burrs, or surface defects. For most general engineering drawings, Ra is sufficient. For critical applications like medical devices, hydraulic sealing surfaces, or optical components, specifying both Ra and Rz provides more complete control over surface quality.
5. How does surface finish affect the cost of CNC machined parts?
Surface finish has a direct and significant impact on CNC machining cost. Achieving Ra 3.2 μm requires no additional operations beyond standard cutting. Moving to Ra 1.6 μm typically requires a dedicated finishing pass with reduced feed, adding 10–20% to cycle time. Ra 0.8 μm or better often requires additional passes, specialized tooling, or post-process operations like vibratory finishing or electropolishing, which can add 30–100% to part cost depending on geometry and batch size. Specifying tighter finishes than your application actually requires is a common and avoidable cost driver. Always match the finish specification to the functional requirement.
6. What surface finish is required for medical device components?
Medical device components manufactured under ISO 13485:2016 typically require Ra ≤ 0.8 μm for non-implant contact surfaces and Ra ≤ 0.4 μm for implant-grade or fluid-contact surfaces. Electropolishing is the preferred post-process for stainless steel medical parts, as it both improves Ra and enhances the passive oxide layer that provides corrosion resistance. All surface finish measurements must be documented and traceable as part of the device history record (DHR). Surface finish CNC machining for medical applications should always be performed by a supplier with active ISO 13485:2016 certification and documented measurement capability.
Conclusion
Surface finish CNC machining is one of the most consequential — and most frequently mismanaged — aspects of precision part production. Get it right and you have components that seal reliably, resist fatigue, meet regulatory audits, and fit their assemblies on the first attempt. Get it wrong and you’re looking at rework, delays, and customer rejections that could have been prevented with a single Ra callout on a drawing.
The fundamentals are clear: understand your measurement parameters (Ra, Rz, Rq), specify them explicitly on your drawings, match the finish to the functional requirement rather than defaulting to the tightest tolerance you can imagine, and work with a supplier who measures and documents surface finish as part of their standard process control.
At MFG SOLUTION, surface finish verification is built into our quality process for every order — not an optional add-on. With ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, 60+ engineering professionals, and 5-axis CNC capability, we machine precision small parts up to 38mm diameter with documented surface finish compliance. You’ll have a quote within 8 hours and your parts shipped within 3 days, backed by the inspection data to prove they meet spec.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: