
2026-07-12
Validate Coolant CNC Performance in High-Speed Ops

To validate coolant CNC performance, measure four core metrics before and after any coolant change: tool life (target ≥15% extension), surface finish (Ra values), cutting temperature, and chip formation consistency. Run a minimum of three identical machining cycles per condition to establish a statistically reliable baseline. Document concentration levels (typically 5–10% for semi-synthetics), pH (8.5–9.5 range), and tramp oil percentage at each interval. These benchmarks catch degradation early and confirm whether a coolant is actually earning its place in your process.
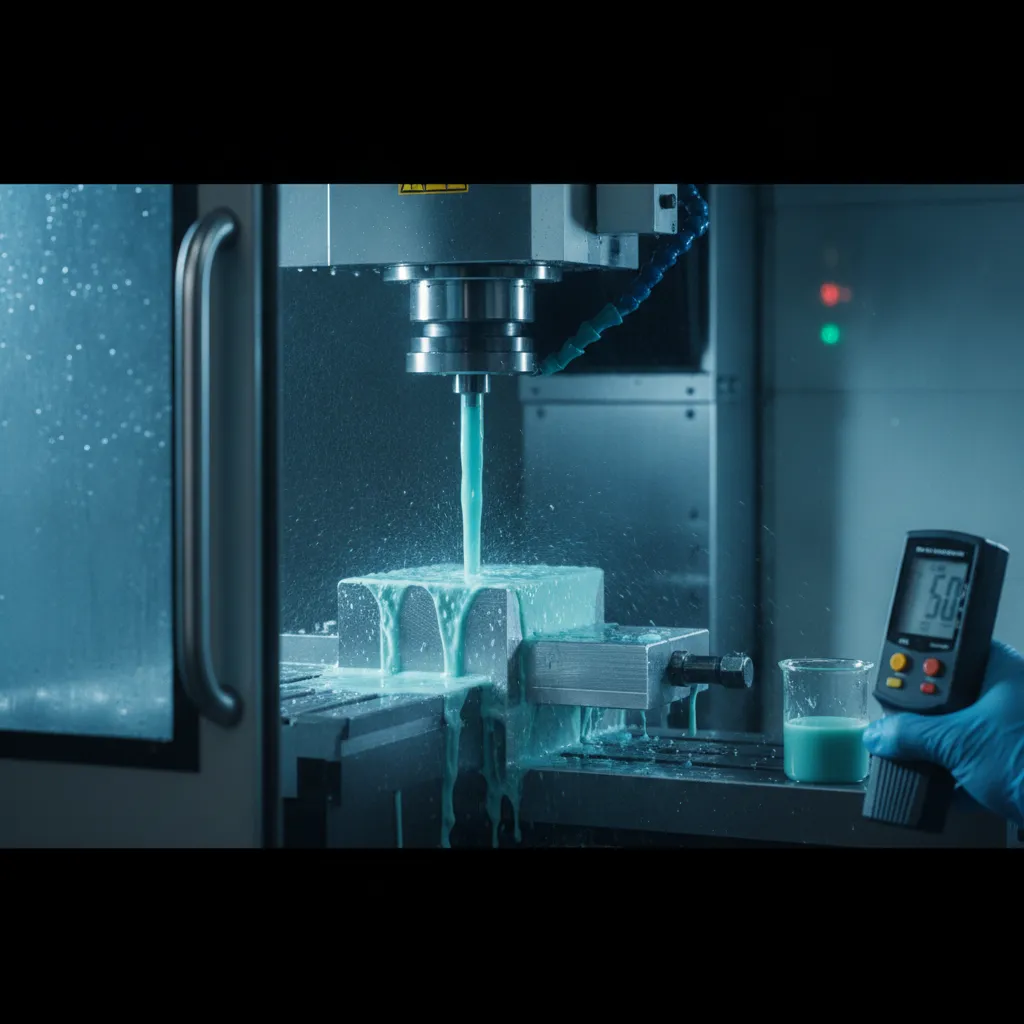
What You’ll Need to Validate Coolant CNC Performance
Gather five instrument categories and three documentation sets before you run a single validation cycle, missing any one will leave gaps in your data.
Instruments and Measurement Tools
A refractometer is your first instrument. Use one rated to ±0.5% accuracy or better to confirm concentration at every interval, semi-synthetic fluids typically run 5–10%, and a reading outside that band immediately flags a mixing or evaporation problem.
Pair it with a digital pH meter calibrated to ±0.1 units. pH strips are acceptable for a quick field check, but a calibrated digital meter gives you the precision to catch early bacterial growth before it destabilizes the emulsion.
To validate coolant CNC performance across surface finish, you need a contact stylus profilometer that captures both Ra and Rz values. Log readings on the same feature before and after any coolant change, a single Ra measurement without a pre-change baseline tells you nothing.
Position a thermocouple or infrared pyrometer directly at the cutting zone, not at the sump. Cutting-zone temperature deltas across runs expose whether a coolant is actually transferring heat away from the insert, or just recirculating warm fluid.
A belt or disk tramp oil skimmer should be running before validation starts, not after. Pair it with a turbidity meter, or a calibrated visual standard, to document contamination level at day zero. Tramp oil above 2% distorts every downstream measurement.
Baseline Documentation Checklist
- Tool life records: Pull the number of parts machined per insert edge from your current production logs. This is your control figure, without it, any claimed tool life improvement is anecdotal.
- Part print surface finish specs: Note the Ra/Rz tolerance called out on the drawing. At MFG SOLUTION, every job runs against documented surface finish specs tied to ISO 9001:2015 process control records, giving engineers a fixed reference point for before-and-after comparison.
- Coolant SDS and TDS sheets: Obtain both the Safety Data Sheet and the Technical Data Sheet for the fluid under test. The TDS lists the manufacturer’s recommended concentration range and pH window, your acceptance criteria come directly from these values.
Define the Key Performance Criteria Before You Run a Single Part
To validate coolant CNC performance accurately, define nine measurable criteria and set numeric pass/fail thresholds before any test part is cut.
The nine criteria are: lubricity (tool wear rate), cooling capacity (cutting zone temperature), corrosion protection on part and machine surfaces, foam index, biological stability (bacterial and fungal colony counts), tramp oil rejection, concentration stability over time, pH drift rate, and chip flushing efficiency. Each criterion needs a defined measurement method and an acceptable range, not a vague target. If you haven’t selected your coolant type yet, review the CNC coolants and lubricants guide first; this article covers validation once the fluid is chosen.
Concentration drift is a common test-killer. Any reading above ±1% from your target concentration, measured by refractometer at shift start, invalidates that run’s data. Log the corrected value and restart the measurement window before recording results.
Why Biological Stability Belongs in Every Validation Protocol
Slime and “goo” formation in the sump is a direct sign of bacterial or fungal growth, not a housekeeping issue. Include a weekly colony-forming unit (CFU) count as a hard validation criterion. A sump showing visible biological buildup has already compromised lubricity, pH, and odor control, all of which corrupt your other nine measurements simultaneously.
Poorly maintained sumps accelerate biological instability. Schedule CFU counts on the same day each week and set a rejection threshold, typically above 106 CFU/mL, before the test begins, not after results disappoint.
Setting Numeric Pass/Fail Thresholds
Thresholds must be written down before machining starts. Three practical benchmarks to use as starting points:
- Tool life must not drop below 85% of your established baseline across the test batch.
- Surface roughness (Ra) must stay within ±10% of the specified value throughout the run.
- pH must not drift more than 0.5 units per week from the initial reading.
At MFG SOLUTION, parts up to 38mm diameter are held to documented process control standards under ISO 9001:2015 and IATF 16949, which means coolant performance criteria are treated as process variables, not afterthoughts. Any threshold breach triggers a corrective action before the next shift, not after the batch ships. For more information, see Boxer Performance.
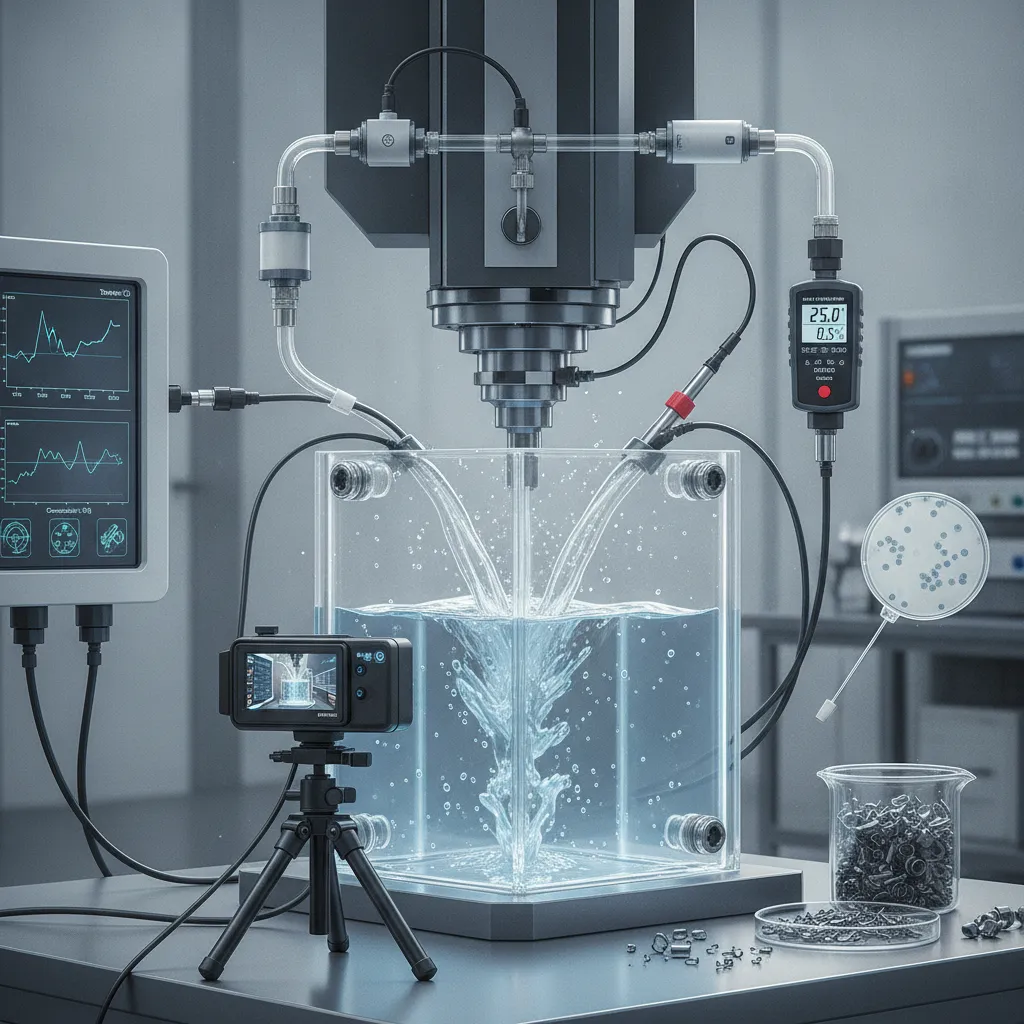
Run the Structured Test Protocol Across Machine Types
To validate coolant CNC performance, run a minimum of three identical machining cycles per test condition and log tool wear, surface finish, and temperature at each cycle’s end.
Each cycle must hold all variables constant, same material grade, feed rate, spindle speed, and depth of cut. At the end of every cycle, record flank wear (VB in mm) using a tool microscope, surface roughness (Ra in µm) with a contact profilometer, and cutting zone temperature via thermocouple or infrared pyrometer. Three cycles give you enough data points to identify trends without running a full design-of-experiments study.
Use ISO 6743-7 for classifying your metalworking fluid type and ASTM E2523 as the framework for your management and documentation procedures. Both standards define what your data sheet must capture: date, operator name, machine ID, coolant batch number, concentration at cycle start and end, pH at cycle start and end, tool ID, parts produced per cycle, Ra readings, and any anomalies such as foam, discoloration, or odor. A structured log like this makes your validation auditable, critical if your production runs under ISO 9001:2015 or IATF 16949 requirements.
Mills vs. Lathes vs. Multi-Axis: What Changes in the Protocol
Each machine type exposes a different coolant failure mode, so the test focus shifts accordingly.
- Mills: Run flood coolant and through-spindle delivery as two separate test conditions. Through-spindle pressure should fall in the 500–1,000 PSI range. Record whether chip evacuation clears the pocket fully at each pressure setting, and compare Ra and VB results between delivery modes.
- Lathes: Prioritize chip evacuation efficiency and insert nose wear. Long, stringy chips that wrap the insert signal inadequate coolant flow or pressure at the cutting zone, log chip morphology alongside VB measurements at each cycle end.
- Multi-axis machines: Confirm coolant reaches every cutting zone during simultaneous axis movement. Run the test cycle at the most complex tool path in your program, not a simplified proxy, and inspect each cutting zone for dry spots or heat discoloration after each cycle.
High-Speed and High-Precision Machining Scenarios
At spindle speeds above 10,000 RPM, flood coolant, minimum-quantity lubrication (MQL), and high-pressure coolant (HPC) produce measurably different temperature and tool life results, validate each delivery method as a separate test condition, not a single combined run.
MQL typically delivers 10–50 mL/hour of lubricant directly to the cutting edge, which reduces thermal shock on carbide tools but may leave chips in the cut zone. HPC at 500–1,000 PSI evacuates chips more aggressively and drops cutting temperatures further. Log the delivery method as a discrete variable on every data sheet row so post-test analysis can isolate its effect on Ra and VB independently of coolant chemistry.
MFG SOLUTION runs 5-axis CNC machines and 20 automatic lathes across production, which means coolant validation protocols must account for both high-speed milling paths and continuous turning operations, two scenarios where delivery method choice directly affects part surface finish and insert life on the same shift.
Troubleshoot Common Coolant Performance Failures
Three signals demand immediate investigation: tool life drops more than 15% from baseline, surface Ra rises more than 10% above spec, or pH moves outside the 8.5–9.5 window.
Any single trigger is enough to validate coolant CNC performance against your established baseline and open a formal diagnostic. Waiting for multiple failures to stack up costs more in scrapped parts and worn tooling than the investigation itself.
How to Diagnose Coolant Degradation Step by Step
Work through the degradation sequence in order, concentration, pH, tramp oil, then bacterial count, before concluding the coolant formula is at fault.
- Check concentration with a refractometer. Compare the reading against your target range. A drift here often explains both tool wear and surface finish problems before anything else does.
- Measure pH. A reading below 8.5 or above 9.5 signals either contamination or additive depletion. Log the value against your baseline.
- Assess tramp oil level. Tramp oil above 2% accelerates bacterial growth and degrades lubricity. If you see a visible oil layer or a sheen on the sump surface, run a skimmer before moving to the next step.
- Run a CFU count. Bacterial counts above 106 CFU/mL indicate the sump is biologically compromised. At that point, treatment options narrow quickly.
Foam failures on high-speed spindles deserve a separate note. Excessive foam is usually caused by air entrainment from an incorrect nozzle angle or too much agitation, not a coolant chemistry problem. Adjust the nozzle position first. Adding defoamer without fixing the root cause masks the symptom and shortens fluid life.
Corrective Actions When Performance Drops Below Threshold
Match each failure mode to a specific corrective action before escalating to full sump replacement.
- Concentration out of range: Top up with fresh concentrate or dilute with deionized water to bring the refractometer reading back within spec.
- pH drift: Add a pH buffer or biocide appropriate to your coolant formulation. Retest within four hours.
- Tramp oil above 2%: Run the skimmer continuously for 24 hours, then retest tramp oil level before any other intervention.
- Bacterial count above 106 CFU/mL: Dump and recharge the sump. Biocide treatment at this count rarely achieves a lasting result.
The replacement-versus-remediation decision follows one rule: if two or more parameters fail simultaneously and corrective action does not restore all of them within 48 hours, full sump replacement is more cost-effective than continued treatment. At MFG SOLUTION, process control documentation, required under ISO 9001:2015 and IATF 16949, captures every corrective action and retest result, so the decision to replace is data-driven rather than reactive.
Common Mistakes to Avoid When Validating CNC Coolant Performance
Five errors account for most failed or inconclusive coolant validation efforts: missing baselines, mixed variables, concentration drift, cross-machine assumptions, and skipped biology checks.
1. Testing Without a Documented Baseline
If you start a validation without pre-existing tool life and surface roughness (Ra) data, you have no reference point to measure against. Pull at least 10 production runs of historical data before you begin, anything less leaves your results statistically indefensible.
2. Changing More Than One Variable per Test Cycle
Swapping coolant and insert grade at the same time makes it impossible to attribute any performance change to the coolant specifically. Run one variable per cycle. If you need to evaluate a new insert, complete that test first, then introduce the new fluid.
3. Ignoring Concentration Drift Mid-Test
A single refractometer reading at shift start misses evaporation-driven concentration increases that can inflate apparent performance gains by 5–8%. Check concentration at the start, midpoint, and end of every shift during the validation window.
4. Applying Mill Data to Lathe or Multi-Axis Operations
Chip load, heat generation, and coolant delivery geometry differ enough between machine types to invalidate cross-machine extrapolation. When you validate coolant CNC performance on a vertical mill, that data does not transfer to a Swiss lathe or multi-axis turn-mill without re-running the full protocol, a point especially relevant when qualifying coolants across mixed-equipment cells like those MFG SOLUTION operates, which include CNC turning, Swiss lathe, and CNC mill & turn platforms.
5. Skipping the Biological Stability Check
Slime-forming bacteria can reach harmful concentrations before any visible contamination appears, so a coolant that “looks clean” is not necessarily safe. A sump that tests at acceptable concentration but harbors bacterial growth will compromise part surface quality and create occupational health exposure for operators. Run a dip-slide or ATP test at every scheduled validation interval, not just when odor or discoloration prompts concern.
Frequently Asked Questions
Which ISO and ASTM standards apply to CNC coolant performance testing?
ASTM E1687 covers biocide efficacy in metalworking fluids, and ASTM D1384 tests corrosion inhibition in coolant solutions. ISO 6743-7 classifies metalworking fluids by type and application. For shops operating under automotive or medical quality systems, IATF 16949 and ISO 13485 require documented process control over cutting fluid parameters, meaning coolant validation data must be traceable, auditable, and tied to specific part numbers and production runs, not just recorded informally.
What quantitative metrics should you track to measure coolant performance improvement?
Track tool life (number of parts per edge), surface roughness (Ra values in µm), coolant concentration (refractometer reading vs. target), pH (target range 8.5–9.5 for most semi-synthetics), and bacterial count (colony-forming units per mL). Baseline each metric before changing coolant type or concentration. A validated improvement shows tool life increasing by at least 10–15% or Ra values holding within drawing tolerance across consecutive production runs without process adjustments.
How often should you validate coolant performance in a production CNC environment?
Validate coolant concentration and pH daily on active sumps; run full performance checks, tool life, surface finish, and bacterial count, weekly. Trigger an unscheduled validation after any sump top-up exceeding 10% of total volume, a material change, or a tool failure rate spike. High-volume shops running three shifts should treat weekly validation as a minimum, not a target.
How do you compare coolant performance data across multiple machining runs?
Normalize your data to a common baseline, parts per tool edge, Ra per material type, and concentration drift per shift, then log each run in a structured format that ties coolant batch, machine ID, operator, and part number together. A simple spreadsheet works for shops running fewer than five machines. Larger operations benefit from SPC (statistical process control) charts that flag when tool life or surface finish trends outside two standard deviations of the established mean.
Conclusion
Validating coolant CNC performance comes down to three actions: establish a numeric baseline before you change anything, track tool life and surface finish Ra values as your primary output metrics, and run structured comparisons across batches using normalized data tied to specific machine and material combinations.
Coolant management is process control, the same discipline that governs every other variable in precision machining. Shops certified to ISO 9001:2015 or IATF 16949 already have the documentation framework; coolant validation slots directly into it.
As a concrete next step, pull your last 30 days of tool change logs and calculate average parts per edge by machine. That single number gives you an honest baseline to measure every coolant change against going forward.
Recommended Articles
Explore more from our content library: