
2026-08-24
Understanding Surface Finish Specifications in CNC Machining

Understanding surface finish specifications CNC is essential. Surface finish specifications in CNC machining define the allowable texture and roughness of a machined surface, typically expressed as Ra (average roughness) in micrometers or microinches. These specifications directly affect part performance, influencing friction, wear resistance, fatigue life, and sealing capability. Choosing the wrong finish can cause premature failure or unnecessary production cost, so matching the specification to the functional requirement is as critical as dimensional tolerance.
Surface Finish Specifications in CNC Machining: What They Are and Why They Matter: surface finish specifications CNC
Surface finish specifications in CNC machining define the complete texture of a machined surface, covering roughness, waviness, and lay, not just a single roughness number. This is particularly relevant for surface finish specifications CNC.
What Is the Difference Between Surface Finish and Surface Roughness?
Engineers frequently use “surface finish” and “surface roughness” as interchangeable terms, but the distinction matters when you write a drawing callout or plan an inspection. Surface finish is the broader condition of a surface, encompassing three measurable characteristics: lay (the dominant direction of the surface pattern), waviness (longer-wavelength undulations from machine vibration or deflection), and roughness (the fine, short-interval irregularities left by the cutting tool).
Surface roughness, most commonly expressed as Ra, the arithmetic average of peak-to-valley deviations, is one component of surface finish, not the whole picture. Specifying only Ra on a drawing leaves waviness and lay undefined, which can create inspection disagreements and assembly problems even when the Ra value passes.
Ra is the dominant parameter in CNC surface finish specifications because it is easy to measure and widely supported by profilometers. Rz (average maximum peak-to-valley height over multiple sampling lengths) and Rmax (the single deepest peak-to-valley measurement) serve as supplementary parameters when peak depth, not average roughness, drives the functional risk, such as in sealing surfaces or fatigue-sensitive components.
Why Surface Finish Specifications Impact Part Performance and Failure Rates
A surface that is too rough increases friction at contact interfaces, accelerates adhesive and abrasive wear, and creates stress concentration points where fatigue cracks initiate. These are mechanical consequences of peak geometry, sharp asperities on mating surfaces interlock and shear under load, removing material with every cycle.
The opposite error carries its own cost. An unnecessarily fine finish requires additional machining passes, slower feed rates, and sometimes secondary operations like grinding or lapping, adding time and cost without improving function for applications where moderate roughness is perfectly adequate.
Surface finish also interacts directly with dimensional tolerance. A shaft specified to a tight diameter tolerance but machined with a coarse finish can still fail to assemble correctly: the roughness peaks effectively increase the functional diameter, consuming tolerance budget before the part even enters the assembly. Finish is a companion specification to dimensional tolerancing, not an afterthought.
For a broader overview of how CNC processes produce different surface conditions, see our related resource on surface finish CNC machining, this article focuses specifically on how to read, write, and apply surface finish specifications CNC drawings require.
How to Read Standard Surface Finish Specifications: Ra Values, Symbols, and Drawing Callouts
Surface finish specifications on CNC drawings use Ra values, ISO or ASME symbols, and unit conventions that must all be read together to avoid costly production errors.
What Does a 3.2 Surface Finish Mean and What Are the Standard Ra Values?
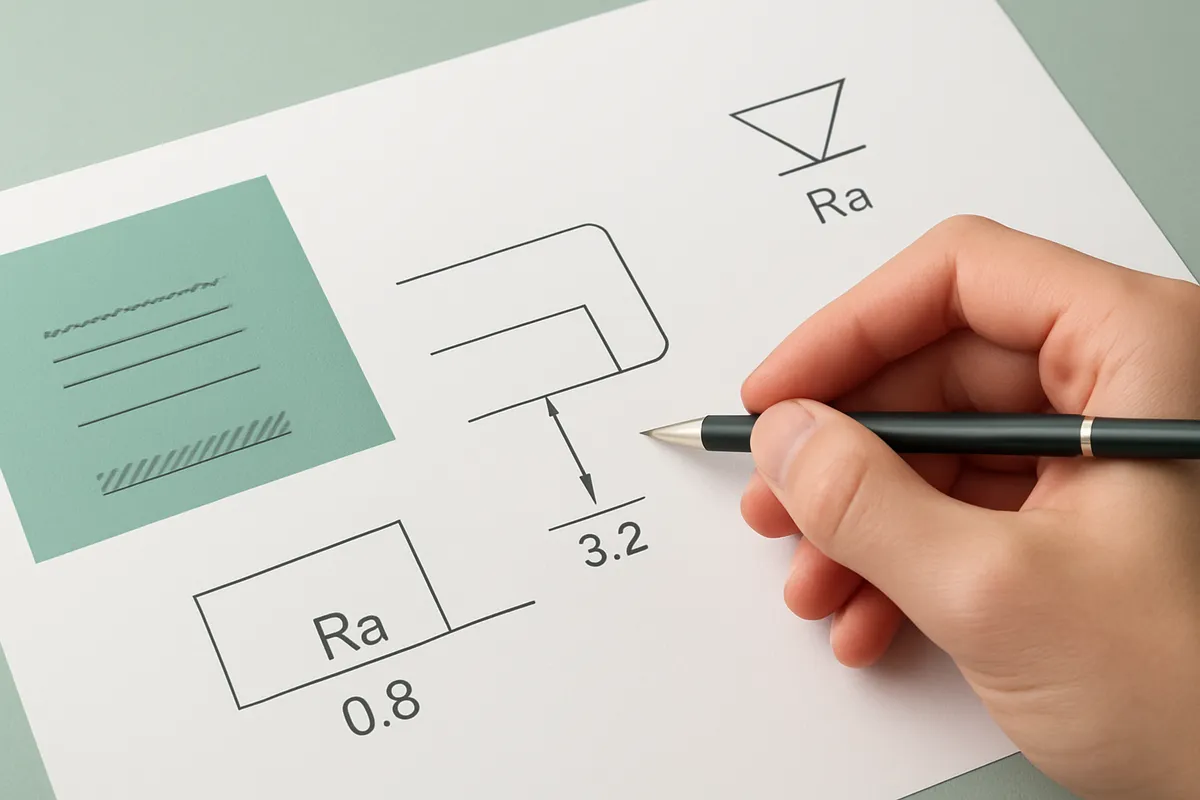
Ra, arithmetic mean roughness, measures the average deviation of a surface profile from its centerline. A 3.2 Ra surface (roughly 125 µin) feels slightly grainy to the fingertip and is visible under direct light; it represents a general-purpose machined finish. A 0.8 Ra surface (about 32 µin) feels smooth and uniform, typical of precision fits. A 6.3 Ra surface (approximately 250 µin) is noticeably rough and acceptable only where appearance and tight tolerances are irrelevant.
Different CNC operations occupy distinct Ra bands. Standard turning and milling typically produce surfaces in the 1.6–6.3 Ra range. Grinding brings parts down to 0.4–1.6 Ra. Honing and lapping reach 0.1–0.8 Ra for bearing bores and sealing surfaces.
In practice, drawings use a standard Ra ladder: 0.4, 0.8, 1.6, 3.2, 6.3, and 12.5 µm. These values align with achievable process windows. Specifying a non-standard value, say, 2.5 Ra, forces a custom process setup, additional inspection steps, and higher unit cost. Staying on the ladder keeps surface finish specifications CNC-compatible with standard tooling and cycle times.
What Symbols and Standards Govern Surface Finish Callouts?
ISO 1302 and ASME Y14.36M are the two governing standards, and both use a check-mark base symbol placed on the surface line of a drawing. Under ISO 1302, the Ra value sits in the upper-left position of the symbol, a lay direction indicator (such as “=” for parallel or “X” for crossed) appears to the right, and a machining allowance value can be added above the horizontal bar. Each element has a fixed location, misplacing any one of them changes the specification’s meaning. When considering surface finish specifications CNC, this point stands out.
ASME Y14.36M follows the same base symbol but differs in how it encodes waviness, lay, and cutoff values within the callout. ISO drawings typically express roughness in micrometers (µm); North American drawings using ASME conventions often use microinches (µin). The conversion is direct, 1 µm equals approximately 40 µin, but the unit label is frequently omitted on older drawings. Reading a 3.2 µm callout as 3.2 µin produces a surface 40 times smoother than intended, a specification error that can invalidate an entire batch.
Engineers working across international supply chains should confirm which standard governs a drawing before quoting or machining. At MFG SOLUTION, our 60+ engineering professionals review drawing callouts during the quoting process, catching unit and symbol conflicts before they reach the shop floor. For more information, see How Long Dental Implant Process Start Finish.
How to Measure and Achieve Target Ra Values Across CNC Mills, Lathes, and 5-Axis Machines
Measuring surface roughness accurately and adjusting the right process variables lets you hit a target Ra value systematically rather than by repeated trial and error.
Practical Differences in Achieving Surface Finish on Mills Versus Lathes Versus 5-Axis Machines
Contact profilometry uses a diamond stylus dragged across the surface to record peak-and-valley data. It suits hard metals and flat or gently curved surfaces where the stylus can track a consistent path. Non-contact optical methods, white-light interferometry and confocal microscopy, are better for soft materials like copper or PTFE-coated parts, and for micro-features where stylus contact would itself deform or damage the surface.
On a CNC mill, four variables control Ra directly. Feed rate sets the distance the cutter advances per revolution; a higher feed leaves taller cusps. Stepover determines the spacing between adjacent passes; reducing it lowers scallop height but extends cycle time. Insert nose radius smooths the cusp geometry, a larger nose radius produces a flatter cusp at the same feed. Spindle speed affects chip load and heat; running too slow generates built-up edge that tears rather than shears the surface.
Lathe-turned surfaces carry a helical lay pattern, a continuous spiral groove running around the part’s circumference. Milled surfaces produce a crossed lay from overlapping cutter paths. This distinction matters when specifying surface finish specifications CNC engineers apply to dynamic seals or bearing fits: a helical lay can channel fluid along the groove under a lip seal, increasing leak risk, while a crossed lay tends to retain lubricant more uniformly. For sealing applications, a superfinished or ground lay-free surface is often required rather than a standard turned finish.
On 5-axis machines, tool tilt angle changes the effective cutting geometry as the tool follows a curved surface. Scallop height, the residual ridge between adjacent passes, rises when tilt angle pulls the cutter contact point away from the tool tip. Ra measurement on a curved surface requires careful stylus path selection: measuring across the lay direction captures peak-to-valley height correctly, but a path that follows the curvature will blend form error into the roughness reading and produce a misleadingly low Ra value.
Troubleshooting Steps When You Cannot Achieve a Specified Ra Value
Work through this sequence in order, each step targets a specific failure mechanism rather than a generic parameter adjustment.
- Check tool condition first. A worn insert or chipped edge tears material instead of shearing it cleanly, raising Ra regardless of other settings. Inspect under magnification and replace before changing any parameter.
- Adjust cutting parameters. Reduce feed rate to lower cusp height, increase nose radius if the insert geometry allows, and verify spindle speed is within the material’s recommended surface footage range to prevent built-up edge.
- Check machine rigidity and vibration. Chatter from tool overhang, a loose spindle bearing, or an unsupported workpiece introduces periodic waviness that appears as improved Ra. Shorten tool stick-out and confirm all fixturing is rigid.
- Verify coolant delivery. Insufficient coolant causes thermal expansion at the cutting zone, which shifts the tool path and introduces dimensional and surface variation. Confirm nozzle position and flow rate match the operation.
MFG SOLUTION’s 60+ engineering professionals apply this same structured diagnostic approach across CNC turning, Swiss lathe, and 5-axis mill-turn operations, catching surface finish deviations before parts reach inspection, not after.
How Surface Finish Requirements Vary by Material and Industry
Material hardness, microstructure, and end-use function each drive distinct surface finish specifications CNC engineers must account for before selecting a process or tolerancing a drawing.
Surface Finish Specifications for Aluminum Versus Steel Versus Composites
Aluminum’s lower hardness means tool marks are shallower at equivalent feed rates compared to steel, but that advantage is deceptive. Dull tooling causes aluminum to smear rather than shear cleanly, producing a surface that measures a low Ra yet has poor functional properties because the material has been plastically displaced rather than cut. The mechanism matters more than the number alone.
Steel hardness and alloy composition set the achievable Ra floor differently. Soft carbon steels turned on a lathe typically reach Ra 1.6–3.2 µm. Hardened tool steels ground after heat treatment can reach Ra 0.2 µm or finer, a finish that turning alone cannot produce. This means a tight finish spec on a hardened steel part almost always requires a secondary grinding or honing operation, which affects both lead time and cost planning. For those exploring surface finish specifications CNC, this matters.
Fiber-reinforced composites present a different problem entirely. Surface texture in these materials is driven by fiber pull-out and delamination rather than plastic deformation, so a standard Ra measurement captures profile height but misses the structural damage that governs functional quality. Inspecting composite surfaces with Ra alone can be misleading; additional methods such as optical microscopy are typically needed.
Thread surfaces are a related sub-case, CNC threading optimization covers how thread flank finish interacts with material type and load-bearing requirements.
How Aerospace, Automotive, and Medical Industries Specify Surface Finish Differently
Each industry ties its finish specifications directly to a failure mode it cannot tolerate.
Aerospace structural components prioritize fatigue life. Surface cracks initiate at peaks and valleys left by machining, so Ra specifications on flight-critical parts target crack initiation prevention, typically Ra 0.8 µm or finer on high-stress zones. A rougher surface in this context is not a cosmetic issue; it is a fatigue life reduction.
Medical implants, bone screws, joint components, spinal hardware, specify Ra ranges tuned to tissue response and osseointegration. Too smooth and bone cells struggle to anchor; too rough and bacterial colonization risk increases. MFG SOLUTION machines implant-grade components under ISO 13485:2016 certification, where process control documentation supports the traceability that medical OEMs require.
Automotive sealing surfaces, gaskets, valve seats, hydraulic fittings, prioritize Rz over Ra because peak height governs whether a leak path exists, not average roughness. A surface with a low Ra but high Rz can still allow fluid to bypass a seal under pressure.
Selecting the Right Surface Finish Specification: Cost Trade-offs and Design-Phase Decisions
Choose your CNC surface finish specification during design, not after production, over-specifying finish is one of the most common and avoidable cost drivers in precision machining.
How to Select the Right Surface Finish Specification During the Design Phase
Start from the functional requirement: sealing, wear resistance, fatigue strength, aesthetics, or assembly fit. Map that requirement to the minimum finish quality it demands, then select the coarsest Ra value that satisfies it. Specifying a tighter finish than the function requires adds cost with no performance return.
The cost increase between Ra values is not linear. Moving from Ra 3.2 µm to Ra 1.6 µm often requires only a parameter change, slower feed rate, sharper tool, adjusted depth of cut. Moving from Ra 1.6 µm to Ra 0.4 µm typically demands an additional operation: grinding, honing, or lapping. Each added setup introduces fixturing time, machine allocation, and process validation, which is where the cost step-change occurs.
Coolant selection is a practical first adjustment before committing to a secondary finishing operation. The right CNC coolants and lubricants reduce tool-workpiece friction and thermal deformation, directly improving achievable surface finish without adding setups, a cost-effective lever that engineers often overlook at the design stage. This directly impacts surface finish specifications CNC outcomes.
Cost-Benefit Trade-offs Between Surface Finish Quality Levels and Production Time
Surface finish specifications CNC engineers select fall into three broad cost tiers. An as-machined finish is budget-friendly and appropriate for non-critical, non-mating surfaces. A controlled Ra finish with documented inspection is mid-range and suits functional mating surfaces where fit and wear matter. A ground or lapped finish with full measurement traceability is premium and applies to safety-critical or high-precision applications, medical implant bores and automotive sealing faces being typical examples.
Tighter Ra specifications also compound inspection overhead. Ra values below 0.8 µm require calibrated contact profilometers or non-contact optical systems, more frequent measurement intervals, and documented records, all of which add time and cost per part, particularly in high-volume production runs where inspection frequency scales with batch size.
At MFG SOLUTION, parts certified under ISO 9001:2015, ISO 13485:2016, and IATF 16949 carry full process documentation, so inspection traceability is built into production rather than bolted on, keeping the overhead of tighter finish specs from becoming a surprise at the quality gate.
Frequently Asked Questions
What is the most common surface finish specification used in CNC machining?
Ra (arithmetic average roughness) is the most widely used surface finish parameter in CNC machining. It averages the absolute deviations of a surface profile from its mean line over a measured length, giving a single number that most machine shops, inspection labs, and engineering drawings already reference. Ra 1.6 µm (63 µin) is the default general-purpose callout for turned and milled parts where no tighter finish is required.
Can CNC machining alone achieve a mirror finish, or is a secondary process always required?
CNC machining alone can reach Ra values as low as 0.2–0.4 µm under optimized conditions, but a true mirror finish (Ra below 0.1 µm) typically requires a secondary process. Diamond turning on specialized equipment is one exception. For most production parts, lapping, polishing, or superfinishing follows the CNC operation to reach optical-grade surfaces. The choice of secondary process depends on part geometry, material, and the functional reason the mirror finish is required.
How does surface finish specification affect fatigue life in structural parts?
Rougher surfaces create stress concentration points where fatigue cracks initiate, directly reducing the number of load cycles a part can survive. Specifying a finer finish on high-stress zones, such as fillet radii, thread roots, or bearing seats, reduces those initiation sites. For rotating or cyclically loaded components in automotive and aerospace applications, tightening the Ra callout in critical zones is one of the most cost-effective ways to extend service life.
What is the difference between Ra and Rz, and when should you specify Rz instead?
Ra measures the average roughness across an entire sample length, while Rz measures the average of the five highest peak-to-valley distances within that length. Rz is more sensitive to isolated surface defects, scratches, pits, or tool marks, that Ra can statistically mask. Specify Rz when a single deep defect would cause functional failure, such as on sealing surfaces, optical components, or parts subject to high-cycle fatigue where peak asperities drive crack initiation.
Conclusion
Surface finish specifications are engineering decisions, not afterthoughts. Three things are worth acting on immediately: first, match your Ra or Rz callout to the function of each surface, not to a blanket drawing standard. Second, confirm that your machining process can actually hit the specified value before the part goes to production; a Swiss lathe and a standard CNC mill produce very different achievable ranges. Third, treat finish and tolerance as a pair, one without the other leaves functional performance undefined.
If you’re preparing a drawing for a precision small part, submit it to MFG SOLUTION for an 8-hour quote that includes process selection across CNC turning, Swiss lathe, and mill & turn, so you know which method hits your finish spec at the lowest cost before you commit to a production run.
Recommended Articles
Explore more from our content library: