2026-05-01
Swiss Machining Technology: A Complete Guide

| Key Insight | Explanation |
|---|---|
| What Swiss machining is | A CNC bar-fed turning process using a sliding headstock and guide bushing to machine small, complex parts with exceptional precision. |
| Tolerances achieved | Swiss-type lathes routinely hold tolerances of ±0.0002″ (±0.005mm), making them ideal for medical, automotive, and electronics components. |
| Key advantage over conventional CNC | The guide bushing supports the workpiece right at the cutting zone, virtually eliminating deflection and enabling long, slender part production. |
| Industry applications | Medical device implants, automotive fuel injectors, electronics connectors, and watch components are all produced with Swiss machining technology. |
| Certifications that matter | ISO 9001:2015, ISO 13485:2016, and IATF 16949 are the quality standards buyers should require from any Swiss machining supplier. |
| Speed benchmark | Modern Swiss-type lathes can perform milling, drilling, threading, and turning in a single setup, drastically cutting cycle times and lead times. |
You need 50,000 stainless steel bone screws, each 2mm in diameter, with a tolerance of ±0.003mm. Your current supplier says six weeks. Swiss machining technology can do it faster, more accurately, and at a lower per-unit cost than almost any other process available. Swiss machining technology is a precision bar-fed CNC turning method that uses a sliding headstock and a guide bushing to support the workpiece right at the point of cutting, enabling the production of small, complex, high-tolerance parts that conventional lathes simply cannot match. Originally developed in Switzerland’s 19th-century watchmaking industry, this process now drives precision manufacturing across medical devices, automotive systems, and electronics globally. In this guide, you’ll learn exactly how it works, why it outperforms conventional CNC turning for small parts, what pitfalls to avoid, and what best practices separate good outcomes from great ones.
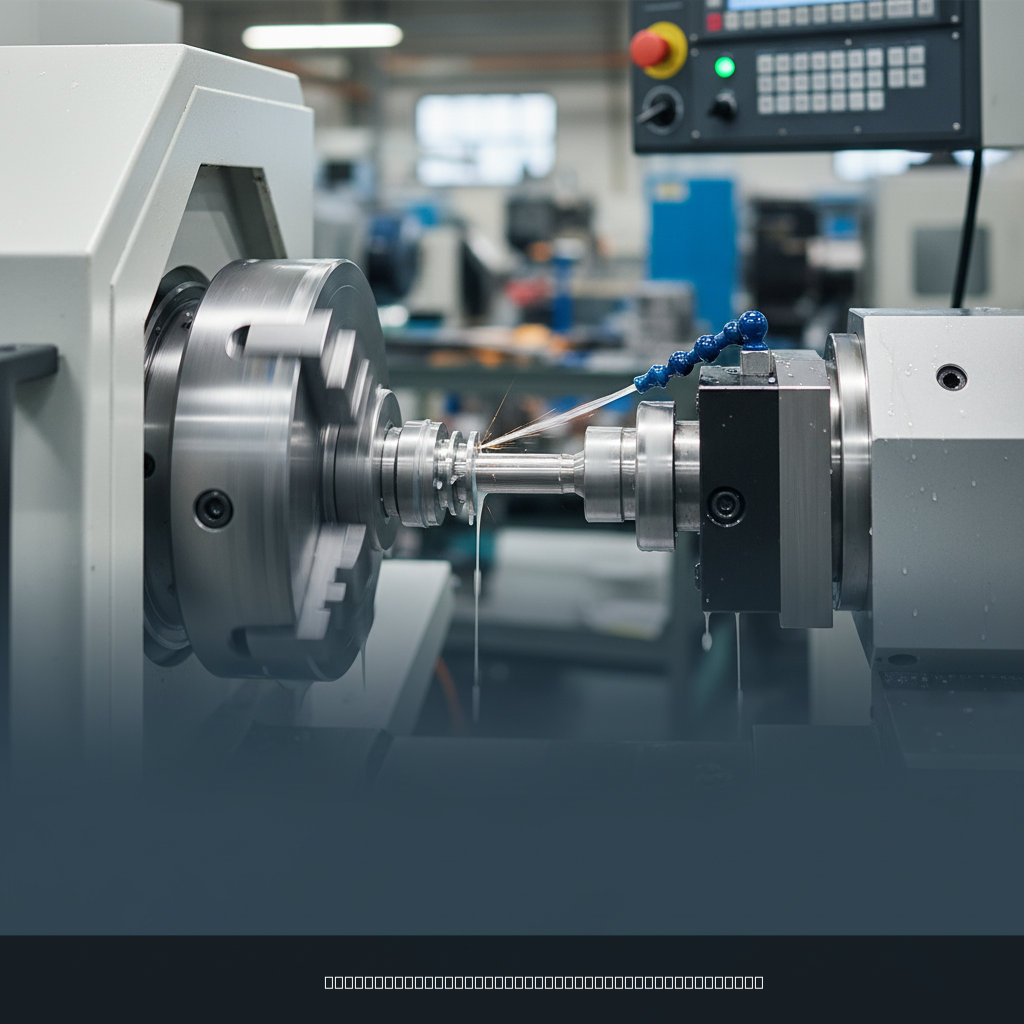
What Is Swiss Machining Technology?
Swiss machining technology is a CNC bar-fed turning process where a sliding headstock moves the bar stock axially through a fixed guide bushing, positioning the cutting tool within millimeters of the bushing’s support point to achieve extreme rigidity and precision. This design eliminates the workpiece deflection that plagues conventional lathes when machining long, slender parts.
Origins and Modern Evolution
The process originated in the Jura region of Switzerland in the 1870s, designed specifically to produce the tiny, intricate shafts and pins required by the Swiss watch industry [1]. Early Swiss screw machines were purely mechanical, driven by cams and levers. CNC control arrived in the 1980s, and by the 2000s, multi-axis Swiss-type lathes with live tooling had transformed the technology into a full machining center capable of milling, drilling, threading, and turning in a single uninterrupted cycle [2].
As of 2026, modern Swiss-type lathes routinely feature 7 to 13 axes of simultaneous motion. Some configurations integrate secondary spindles, gang tool slides, and back-working attachments that allow complete part machining without any manual intervention between operations.
What Swiss Machining Technology Produces
Swiss machining excels at parts that share a specific profile: small diameter, high complexity, and tight tolerances. Typical applications include:
- Medical implants and surgical instruments (bone screws, cannulas, dental implants)
- Automotive fuel system components (injector nozzles, valve stems, sensor housings)
- Electronics connectors, contact pins, and micro-shafts
- Watch and instrument components (gears, pinions, arbors)
- Aerospace fasteners and hydraulic fittings
According to Xometry’s technical resource library, Swiss machining is particularly suited to parts under 38mm in diameter, where the guide bushing’s support advantage is most pronounced [3]. Parts beyond that diameter are better served by conventional turning or mill-turn centers.
Pro Tip: If your part has a length-to-diameter (L/D) ratio greater than 3:1, Swiss machining technology is almost certainly your best option. The guide bushing prevents the deflection that makes long, slender parts nearly impossible to hold to tolerance on a conventional lathe.
How Swiss Machining Technology Works
Swiss machining technology works by feeding a bar of raw material through a collet and guide bushing, then advancing the headstock axially so that cutting tools always engage the stock within 1-2mm of the bushing’s support point, maintaining rigidity throughout the cut regardless of part length.
The Mechanics: Step by Step
Understanding the process sequence clarifies why Swiss machining achieves tolerances that conventional turning cannot. Here’s how a typical cycle runs:
- Bar loading: A bar of raw material (stainless steel, titanium, brass, aluminum, or engineering plastics) is loaded into the bar feeder and fed through the machine’s collet and guide bushing.
- Headstock advance: The sliding headstock moves the bar axially (Z-axis) through the stationary guide bushing, exposing only the length of material needed for the current cut.
- Outer diameter turning: Gang tool slides or turret tools engage the bar to turn the OD profile. Because the cutting point is always within millimeters of the bushing, the workpiece has virtually no unsupported length during cutting.
- Live tooling operations: Milling cutters, drills, and tapping tools mounted on live spindles machine cross-holes, flats, slots, and threads simultaneously or in rapid succession.
- Secondary spindle pickup: Once the primary features are complete, a secondary (sub) spindle grips the part, and the cut-off tool separates it from the bar. The sub-spindle then presents the back end of the part to additional tools for back-working operations.
- Part ejection and inspection: The finished part is ejected into a parts catcher. In-process gauging systems can measure critical dimensions on every cycle.
As AdvancedManufacturing.org explains, the guide bushing is the defining element of this architecture. The tool cuts the stock near the bushing, which is the support point, so the effective cutting length is always minimal, no matter how long the finished part ultimately becomes [4].
Key Machine Components
| Component | Function | Why It Matters |
|---|---|---|
| Sliding headstock | Moves bar stock axially through the guide bushing | Controls Z-axis positioning with sub-micron accuracy |
| Guide bushing | Supports bar stock at the cutting zone | Eliminates deflection; enables long slender parts |
| Gang tool slide | Holds multiple turning tools in a fixed array | Rapid tool engagement without turret indexing time |
| Live tooling spindles | Power rotating tools for milling, drilling, tapping | Enables complete machining in one setup |
| Secondary spindle | Grips part after cutoff for back-working | Machines the back face without a second setup |
| Bar feeder | Automatically loads and advances bar stock | Enables lights-out, unattended production |
Mastercam’s technical blog notes that the difference between Swiss and conventional turning lies fundamentally in how the stock material is moved and supported during cutting, not merely in the number of axes available [5].
Key Benefits of Swiss Machining Technology
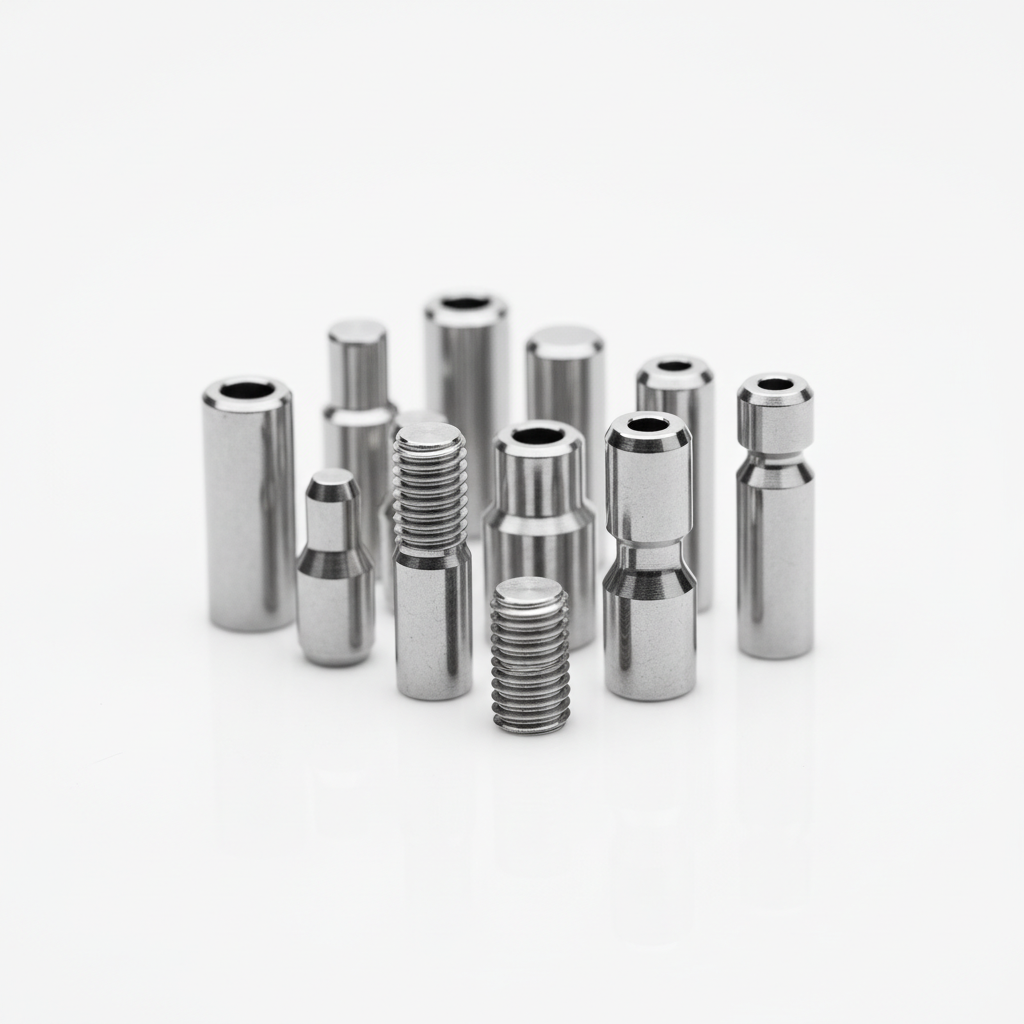
Swiss machining technology delivers a combination of precision, speed, and part complexity that no other single-setup process can match for small-diameter components, making it the preferred choice for medical, automotive, and electronics manufacturers worldwide.
Precision and Repeatability
The guide bushing architecture allows Swiss-type lathes to hold tolerances of ±0.0002″ (±0.005mm) routinely in production, with some specialized machines achieving ±0.0001″ [6]. That’s not prototype-level performance. That’s repeatable, lot-after-lot consistency that quality-critical industries depend on.
- Dimensional accuracy: Tolerances tighter than ±0.005mm are achievable in production runs
- Surface finish: Ra values below 0.4μm are routinely achieved without secondary finishing operations
- Concentricity: The continuous bar support ensures excellent concentricity between features machined in the same setup
- Repeatability: CNC control eliminates operator-to-operator variation across thousands of parts
Efficiency and Cost Advantages
Swiss machining technology’s single-setup capability is a major cost driver. Parts that once required three or four separate operations (turning, milling, drilling, threading) on different machines are completed in one continuous cycle. According to the National Tooling and Machining Association (NTMA), shops transitioning to Swiss-type machining report that time savings from single-operation production represent the most immediate and significant throughput benefit [7].
Additional cost benefits include:
- Reduced fixturing costs: No custom fixtures needed for multiple setups
- Lower scrap rates: Fewer handling steps mean fewer opportunities for damage or error
- Lights-out production: Bar feeders enable unattended overnight runs, maximizing machine utilization
- Material efficiency: Bar stock is consumed progressively with minimal waste
Pro Tip: When evaluating whether Swiss machining technology is cost-effective for your part, calculate total cost across all operations, not just the machining rate. A Swiss lathe’s higher hourly rate almost always delivers a lower total cost per part when you factor in eliminated setups, reduced scrap, and faster throughput.
Swiss Machining vs. Conventional CNC Turning
Swiss machining technology and conventional CNC turning are both bar-fed rotational processes, but they differ fundamentally in workpiece support, axis count, and the complexity of parts they can produce economically in a single operation.
A Direct Comparison
Choosing the wrong process for your part geometry is one of the most common and costly mistakes in precision machining procurement. Here’s how the two processes compare across the factors that matter most:
| Factor | Swiss Machining | Conventional CNC Turning |
|---|---|---|
| Workpiece support | Guide bushing at cutting zone | Chuck or collet at headstock only |
| Axis count | 5 to 13+ axes | 2 to 4 axes typical |
| Best part diameter | Up to 38mm | 10mm to 300mm+ |
| L/D ratio capability | Excellent (up to 20:1+) | Limited (typically under 4:1) |
| Tolerances | ±0.005mm routinely | ±0.01–0.05mm typical |
| Setup complexity | Higher initial setup time | Faster setup for simple parts |
| Best for | High-volume, complex, small parts | Larger, simpler parts; lower volumes |
| Live tooling | Standard on most machines | Available but less integrated |
In practice, the decision often comes down to part diameter and L/D ratio. Fractory’s technical analysis confirms that Swiss turning is specifically designed to produce small, complex parts where the sliding headstock and guide bushing combination provides rigidity that a conventional chuck simply cannot offer at small diameters [8].
When to Choose Each Process
From experience, the right process depends on your part’s specific geometry and volume requirements:
- Choose Swiss machining when your part is under 38mm diameter, has an L/D ratio above 3:1, requires multiple features (threads, cross-holes, milled flats), or demands tolerances tighter than ±0.01mm
- Choose conventional CNC turning when your part is larger than 38mm, relatively simple in geometry, or you’re running very low volumes where Swiss setup time isn’t justified
- Consider CNC mill-turn when your part combines significant prismatic features with rotational geometry and doesn’t require the extreme L/D capability of Swiss
Common Challenges and Mistakes in Swiss Machining
Swiss machining technology delivers outstanding results when set up correctly, but several common mistakes can undermine precision, increase scrap rates, and drive up costs for buyers and machinists alike.
Design and Material Mistakes
A common mistake is designing parts without considering the bar stock diameter constraint. Swiss machines feed bar stock through the guide bushing, so your part’s maximum diameter must fit within the machine’s bar capacity (typically up to 38mm). Designing a part that exceeds this requires either a different process or a re-design.
Material selection errors also cause problems. Guide bushings require consistent bar stock diameter and surface quality. Bars with excessive diameter variation or rough surface finish cause the bushing to wear prematurely and compromise part accuracy. Industry professionals recommend using precision-ground bar stock with h6 or h7 diameter tolerances for Swiss machining applications.
- Avoid: Designing undercuts or features that require the guide bushing to be removed mid-cycle
- Avoid: Specifying tolerances tighter than the process can hold without discussing feasibility with your machinist first
- Avoid: Using free-machining alloys with lead content in medical or food-contact applications, even when they offer better machinability
Process and Programming Pitfalls
One pitfall to watch for is guide bushing clearance. The bushing must be set with the correct clearance for the bar diameter. Too tight, and friction heats the bar and causes dimensional drift. Too loose, and the bar chatters, leaving poor surface finish and out-of-tolerance dimensions.
The Society of Manufacturing Engineers (SME) has documented that improper guide bushing setup is among the leading causes of dimensional inconsistency in Swiss machining production [9]. Shops transitioning from conventional turning often underestimate the skill required to set up and maintain guide bushings correctly.
Pro Tip: When sourcing Swiss-machined parts, ask your supplier specifically about their guide bushing maintenance schedule and in-process gauging capability. A supplier who can’t answer both questions clearly is a quality risk, regardless of their price.
Best Practices for Swiss Machining in 2026
Swiss machining technology in 2026 is more capable than ever, but getting the best results requires deliberate choices in design, supplier selection, and quality verification throughout the production process.
Design for Swiss Machining (DfSM)
Design for manufacturability principles applied specifically to Swiss machining (DfSM) can cut part costs by 20-40% without sacrificing function. Key guidelines include:
- Minimize diameter steps: Each diameter change requires a separate tool pass. Reducing the number of distinct diameters shortens cycle time.
- Standardize thread forms: Use standard thread pitches and forms (UNC, UNF, M-series metric) rather than custom profiles whenever possible.
- Specify surface finish only where needed: Applying a tight Ra requirement across the entire part surface adds cost. Specify Ra values only on functional surfaces.
- Avoid deep blind holes: Blind holes in small-diameter parts require specialized tooling and slow cycle times. Through holes are almost always faster and cheaper.
- Design for bar stock diameters: Size your part’s maximum OD to align with standard bar stock diameters (e.g., 6mm, 8mm, 10mm, 12mm) to minimize material waste.
Supplier Selection and Quality Verification
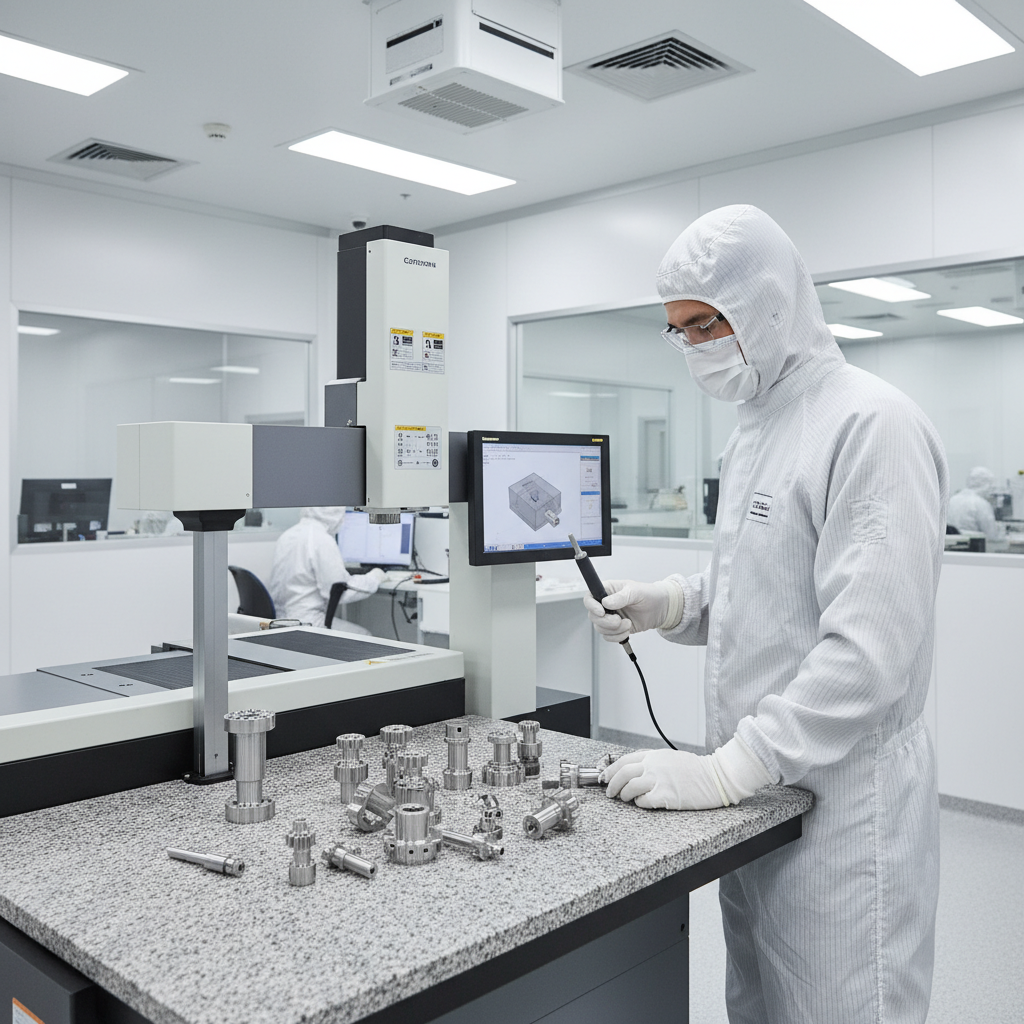
At MFG SOLUTION, we’ve found that the three certifications that most reliably predict supplier quality for Swiss machining are ISO 9001:2015 (general quality management), ISO 13485:2016 (medical device manufacturing), and IATF 16949 (automotive quality). A supplier holding all three has demonstrated documented process control, traceability, and corrective action capability across the most demanding industries.
A medical device client recently faced a supply chain disruption when their existing Swiss machining supplier failed an ISO 13485 audit. Switching to a certified supplier with full process documentation resolved the compliance gap within two weeks and restored production continuity without a single rejected lot.
When evaluating Swiss machining suppliers, verify these capabilities:
- In-process gauging and statistical process control (SPC) implementation
- Material traceability from bar stock certificate to finished part
- First article inspection (FAI) reports with full dimensional layout
- Capacity to quote within 8 hours and ship within 3 days for standard geometries
- Engineering support for DfSM review before production begins
Industry analysis from Nomura DS confirms that Swiss machining’s precision advantage is fully realized only when paired with rigorous quality systems, since the process’s capability to hold tight tolerances means that any systematic error in setup or tooling will replicate consistently across thousands of parts [10].
As of 2026, leading Swiss machining suppliers are also integrating IoT-enabled machine monitoring and digital twin simulation into their production workflows. These tools allow real-time detection of tool wear, thermal drift, and dimensional deviation before scrap is produced, not after.
Sources & References
- Dynamic Machine, “Swiss CNC Machining: The Most Impressive Precision Manufacturing Technology,” 2026
- Criterion Precision, “Swiss Machining Explained: Precision Capabilities and Benefits,” 2026
- Xometry, “What Is Swiss Machining? How It Works and Uses,” 2026
- AdvancedManufacturing.org, “Swiss Machining Made Simpler,” 2026
- Mastercam, “What is Swiss Machining?,” 2026
- Eagle Stainless Tube, “What is Swiss Machining?,” 2026
- National Tooling and Machining Association (NTMA), “Transitioning to CNC Swiss-Type Machining,” 2026
- Fractory, “Swiss Machining Explained: What Is a Swiss Lathe?,” 2026
- Society of Manufacturing Engineers (SME), “Swiss-Style Machines Simplified,” 2021
- Nomura DS, “What is Swiss Machining? The Ins and Outs of Swiss-Type Lathes,” 2026
Frequently Asked Questions
1. How much does a Swiss CNC programmer make?
As of 2026, Swiss CNC programmers in the United States earn an average of approximately $64,000-$72,000 per year, depending on experience level, geographic location, and the complexity of parts they program. Senior programmers with multi-axis experience on 9-13 axis Swiss-type lathes, particularly in medical device or aerospace environments, can command $85,000-$100,000 annually. Demand for qualified Swiss CNC programmers continues to outpace supply, which is driving wages upward across most manufacturing regions. Certifications from institutions like the Milwaukee Area Technical College’s CNC Swiss Multi-Axis Machining program are increasingly valued by employers.
2. What is the difference between CNC and Swiss machining?
Conventional CNC turning supports the workpiece only at the headstock chuck or collet, which limits rigidity for small-diameter or long parts. Swiss machining technology adds a guide bushing that supports the bar stock within millimeters of the cutting tool, virtually eliminating deflection and enabling tolerances of ±0.005mm or tighter. Swiss-type machines also typically operate on 5 to 13 axes simultaneously, compared to 2-4 axes on standard CNC lathes, allowing complete part machining, including milling, drilling, and threading, in a single uninterrupted setup. This combination of rigidity, axis count, and single-setup capability is what makes it the clear choice for high-precision small-diameter parts.
3. What does a Swiss machinist do?
A Swiss machinist sets up, programs, operates, and maintains Swiss-type CNC lathes (also called Swiss screw machines or sliding headstock lathes) to produce small, complex, high-precision parts from bar stock. Their responsibilities go well beyond simply running a machine: they select and set guide bushings to correct clearances, qualify bar stock for dimensional consistency, write or verify CNC programs for multi-axis simultaneous machining, perform first-article inspections, and monitor in-process gauging data to detect tool wear before it produces out-of-tolerance parts. In practice, a skilled Swiss machinist combines the knowledge of a CNC programmer, a quality technician, and a tooling specialist in a single role.
4. What materials can be machined with Swiss machining technology?
this method works with a wide range of materials, including stainless steel (303, 304, 316L), titanium alloys (Grade 5/Ti-6Al-4V), aluminum alloys (6061, 7075), brass, copper, carbon steel, and engineering plastics such as PEEK, Delrin, and PTFE. Material selection depends on the part’s end-use environment, regulatory requirements (medical applications often require 316L stainless or titanium), and machinability. Free-machining alloys like 303 stainless and C360 brass produce the shortest cycle times, while titanium and hardened steels require slower speeds and specialized tooling but are fully compatible with Swiss-type lathes.
5. Is Swiss machining technology suitable for high-volume production?
Yes. this strategy is one of the most efficient processes available for high-volume production of small, complex parts. Bar feeders enable lights-out, unattended production runs overnight or over weekends, and cycle times for typical Swiss-machined parts range from 15 seconds to 3 minutes per part depending on complexity. Production volumes from 500 to several million parts per year are all within the process’s economic range. The key economic threshold is setup time: Swiss-type lathes require more initial setup than simple CNC lathes, so the process becomes increasingly cost-effective as volume grows. For most parts above 500 pieces, Swiss machining delivers a lower total cost per part than any alternative single-setup process.
6. What certifications should I look for in a Swiss machining supplier?
The three certifications that matter most are ISO 9001:2015 (general quality management system), ISO 13485:2016 (medical device manufacturing), and IATF 16949 (automotive quality management). ISO 9001:2015 confirms that the supplier has documented processes and a systematic approach to quality. ISO 13485:2016 adds medical-specific requirements for traceability, risk management, and regulatory compliance. IATF 16949 adds automotive-specific requirements for process control, measurement system analysis, and production part approval. A supplier holding all three has demonstrated the highest level of quality system maturity and is equipped to serve the most demanding industries. Results may vary based on how rigorously a supplier implements these standards in practice, so always request audit records and recent inspection reports.
Conclusion
this approach remains the gold standard for producing small, complex, high-precision parts in 2026. Its unique combination of guide bushing support, multi-axis simultaneous machining, and single-setup capability delivers tolerances, surface finishes, and throughput rates that no other process can match for components under 38mm in diameter. The process isn’t right for every part, but for the parts it fits, it’s the most efficient and precise manufacturing method available.
Choosing the right Swiss machining partner is just as important as choosing the right process. Certifications, engineering depth, and turnaround speed all determine whether you get the precision you specified, on time, and within budget. At MFG SOLUTION, we operate Swiss lathe services alongside CNC turning, CNC mill-turn, automatic lathe, and cold forging capabilities, all under ISO 9001:2015, ISO 13485:2016, and IATF 16949 certification. Our 60+ engineering professionals can quote your Swiss-machined parts within 8 hours and ship your first batch within 3 days. If you’re sourcing precision small parts and need a supplier who understands the process from bar stock to final inspection, that’s exactly what we’re built for.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: