
2026-08-31
How to Machine Stainless Steel Precision Parts Successfully

Stainless steel precision parts are custom-machined or formed components held to tight dimensional tolerances, typically achieved through CNC turning, Swiss lathe machining, or milling, that go beyond what standard off-the-shelf metal parts can deliver. What sets them apart is the combination of corrosion resistance, mechanical strength, and repeatable accuracy required by industries like medical devices, aerospace, and automotive. Choosing the right stainless grade and machining process determines whether your part performs reliably or fails under load.
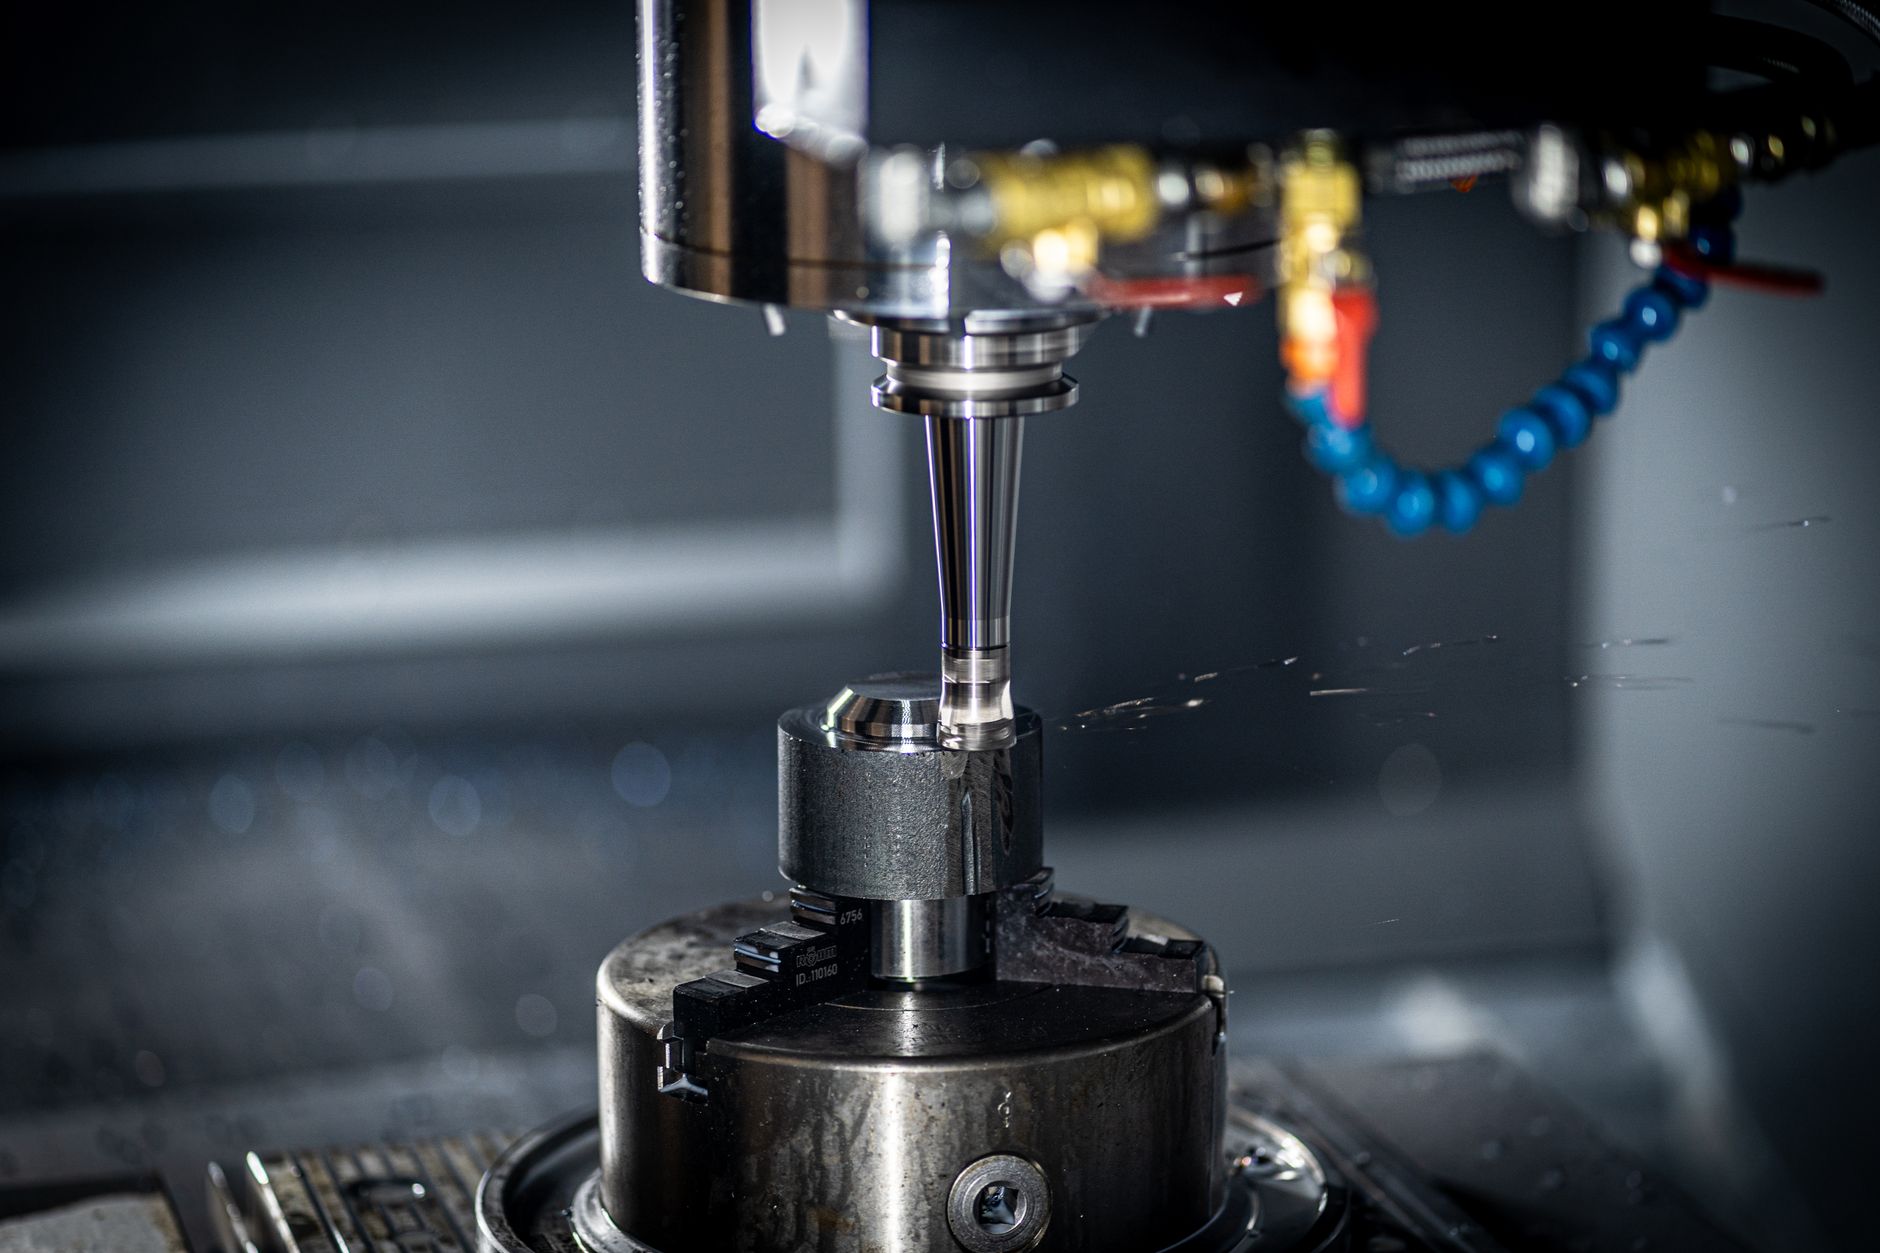
Understand What Stainless Steel Precision Parts Actually Require
Stainless steel precision parts demand tolerances, surface finishes, and process controls that standard machined components simply cannot meet.
The gap between a standard metal component and a precision part comes down to dimensional control. Standard machined parts typically hold tolerances in the ±0.1 mm to ±0.5 mm range. Precision parts, by contrast, routinely require ±0.005 mm or tighter, accuracy that conventional machining cannot reliably achieve. Hitting those thresholds requires purpose-built equipment and deliberate process design.
How Precision Metal Parts Are Manufactured
CNC turning, Swiss lathe machining, and 5-axis mill-turn centers are the primary methods for holding tight tolerances on small-diameter stainless components. Swiss lathe machines are particularly effective for slender parts under 38mm in diameter because the guide bushing supports the workpiece directly at the cutting zone, minimizing deflection. For high-volume runs of simpler geometries, automatic lathes reduce per-part cost while maintaining consistent output. Complex, low-volume parts, those with multiple features or compound angles, move to CNC mill-turn centers where a single setup handles turning and milling operations together, cutting cumulative error.
Why Stainless Steel Behaves Differently Under Cutting Conditions
Stainless steel work-hardens as the cutting tool passes through it, which accelerates tool wear and degrades surface finish faster than aluminum or mild steel does. Austenitic grades like 304 and 316 are especially prone to this, the cutting heat they generate demands tighter control of feed rates, tool geometry, and coolant application than softer metals require.
Full process documentation is not optional in this environment. Medical device buyers require traceability under ISO 13485:2016; automotive suppliers require it under IATF 16949. Every step, material certification, tooling records, in-process inspection data, final dimensional reports, must be tracked and auditable. Without that paper trail, a part that measures correctly still cannot ship to a regulated customer.
Key Industries That Rely on Stainless Steel Precision Parts
Understanding which industries drive demand for stainless precision components helps clarify why the requirements are so exacting. The following sectors represent the most common end-use environments:
- Medical devices: Surgical instruments, implant components, and fluid-handling assemblies require biocompatible grades, electropolished surfaces, and full lot traceability under ISO 13485:2016.
- Aerospace: Fasteners, actuator components, and hydraulic fittings must meet tight dimensional tolerances and pass rigorous material certification requirements.
- Automotive: Fuel system parts, sensor housings, and transmission components demand IATF 16949-compliant suppliers and statistical process control on critical dimensions.
- Food and beverage processing: Pumps, valves, and conveyor fittings require 304 or 316 grades with smooth, cleanable surfaces that resist bacterial adhesion.
- Electronics and semiconductor: Precision housings, connectors, and heat-sink components need tight flatness and parallelism tolerances to ensure reliable assembly.
Select the Right Stainless Steel Grade for Your Precision Parts
Match your grade to your environment: 303 for fast machining, 304 for food contact, 316 for chloride exposure, 17-4 PH for high strength, 440C for hardness.
Austenitic Grades: 303, 304, and 316 Compared
303 and 304 are the two most common starting points for stainless steel precision parts. The key difference is sulfur: 303 contains a sulfur addition that breaks chips cleanly and reduces tool wear, cutting machine time and cost. That same sulfur reduces corrosion resistance, so 303 is a poor choice anywhere moisture, cleaning agents, or food contact are present.
304 drops the sulfur and offers better corrosion resistance across a broader set of conditions. It machines slower than 303 but holds up in wet environments, food-processing equipment, and medical instrument housings where surface integrity matters.
316 goes further by adding molybdenum, typically 2–3% by composition, which closes the grain structure against chloride ion attack. That makes 316 the standard choice for marine hardware, pharmaceutical fluid-contact components, and chemical processing parts where pitting corrosion is a documented failure mode, not a theoretical one. From a cost standpoint, 303 is the most budget-friendly grade to machine; 304 sits slightly higher; 316’s molybdenum content pushes material cost into mid-range territory.
Precipitation-Hardening and Martensitic Grades for High-Strength Applications
17-4 PH achieves high tensile strength through an aging heat treatment process: after solution annealing, the alloy is held at a controlled temperature (commonly between 900°F and 1150°F depending on the H-condition specified) that causes copper-rich precipitates to form within the steel matrix. This raises strength without the corrosion resistance trade-off typical of fully martensitic grades. For detailed composition and mechanical property data, MFG SOLUTION’s material reference on 17-4 PH covers condition-specific tensile and yield values.
440C is the right call when hardness is the primary requirement, bearings, valve seats, and cutting tool components where surface wear resistance drives part life. Heat-treated 440C reaches Rockwell hardness levels that austenitic grades cannot approach. The trade-off is real: 440C’s high carbon content reduces corrosion resistance significantly compared to 304 or 316, so it belongs in dry or controlled environments, not in chemical or marine exposure. Material and machining costs for 17-4 PH and 440C fall into the mid-range to premium tier, reflecting both alloy content and the additional processing steps each grade requires.

Evaluate the Limitations of Stainless Steel Before Committing to a Grade
Stainless steel precision parts offer excellent corrosion resistance, but the material carries real machining and performance trade-offs that can affect cost, tool life, and dimensional accuracy.
Work hardening is the most common problem machinists encounter with austenitic grades like 304 and 316. These grades harden rapidly at the cutting zone during machining, which shortens tool life and can introduce residual stress into the part. That stress may cause dimensional drift in components with tight tolerances, a serious concern for medical implants or automotive fuel system parts where a few microns matter.
Galling is a separate risk in threaded or sliding stainless-on-stainless assemblies. When two stainless surfaces contact under load, they can seize and tear. Switching to grade 303, which contains added sulfur for lubricity, or applying a surface treatment such as PTFE coating or electropolishing, reduces this risk significantly.
Thermal conductivity is also lower in stainless than in aluminum, which concentrates heat at the tool tip rather than dissipating it through the workpiece. This requires a deliberate coolant strategy and slower feed rates to prevent tool failure and surface damage.
When to Consider Alternatives to Stainless Steel
Four factors should drive the decision to switch materials: load requirements, weight targets, thermal performance, and budget. Aluminum handles weight-sensitive electronics housings better; titanium outperforms stainless under high-stress, low-weight conditions; engineering plastics suit low-load, chemically aggressive environments where metal is unnecessary. If your part doesn’t need stainless-level corrosion resistance, defaulting to stainless adds cost without adding value.
Source Stainless Steel Precision Parts Without Compromising Quality or Lead Time
Qualify a supplier by checking three things: industry-specific certifications, realistic lead time drivers, and how fast they respond to a drawing.
Quality Certifications and Compliance Standards That Matter
Certifications tell you what a supplier is required to demonstrate, not just claim. ISO 9001:2015 requires documented process control, corrective action systems, and measurable quality objectives across general precision machining. Holding the certificate means an accredited third party audited those systems, not that a manager printed a policy document.
ISO 13485:2016 goes further for medical device components. It adds risk management, traceability to individual lot level, and design controls that link each part characteristic back to a clinical or functional requirement. IATF 16949 applies to automotive suppliers and mandates advanced product quality planning (APQP), production part approval process (PPAP), and statistical process control, all of which require the supplier to prove capability before a production run ships, not after.
Ask any candidate supplier to share their most recent audit summary, not just a certificate scan. A shop that holds ISO 9001:2015, ISO 13485:2016, and IATF 16949, as MFG SOLUTION does, has passed external audits across three separate requirement sets, which meaningfully reduces your supplier qualification burden.
In-House Machining vs. Outsourcing to a Precision Machining Service
In-house machining gives you direct process control over stainless steel precision parts, but it requires capital investment in Swiss lathes, 5-axis CNC machines, and metrology equipment, plus the engineering headcount to operate and maintain them. That fixed cost makes sense only when volumes are high and part families are stable.
Outsourcing to a certified shop shifts that overhead entirely. You access Swiss lathe, CNC turning, cold forging, and CNC mill & turn capacity without owning a single machine. The tradeoff is supplier dependency, which certifications and documented process controls directly mitigate.
Lead time depends on four variables: whether you need prototype or production quantities, grade availability (316L and 304 stock faster than 17-4 PH), secondary operations such as passivation or heat treatment, and inspection requirements like CMM reports or first-article inspection. Each adds time; knowing which apply to your part lets you build a realistic schedule.
Use quoting speed as a qualification signal. A shop that returns an 8-hour quote has engineers reading your drawing and identifying process constraints, not a sales rep estimating from a price list. MFG SOLUTION’s 8-hour quote window reflects that engineering review is built into the front end of every order. For a detailed look at inspection methods and metrology standards, see our CNC machining quality assurance page.
Avoid Common Mistakes When Specifying and Ordering Precision Stainless Parts
The four errors that most often cause rework or delays in stainless steel precision parts orders are over-tight tolerances, unauthorized grade substitution, missing surface finish callouts, and skipped passivation.
Over-Tightening Tolerances
Specifying tighter tolerances than your application requires forces slower feed rates, more inspection passes, and higher scrap rates, none of which improve part function. A bearing seat that needs ±0.05mm does not benefit from a ±0.01mm callout; it just costs more to produce and reject. Match tolerance to the actual assembly requirement, then hold that line.
Grade Substitution Without Engineering Review
A supplier swapping 304 for 316, or 303 for 304, changes corrosion resistance and machinability in ways that can cause field failures. Your purchase order should explicitly state the alloy designation, the applicable ASTM standard (e.g., ASTM A276 for bar stock), and a clause requiring written buyer approval before any material substitution.
Ignoring Surface Finish Callouts
Leaving Ra values unspecified invites shop-floor variation. A rougher surface than intended can break a seal, reduce fatigue life by creating stress-concentration sites, or accelerate crevice corrosion on stainless. Call out Ra in micrometers on every drawing where finish affects function.
Skipping Passivation
Machining embeds iron particles from cutting tools into the stainless surface, disrupting the chromium oxide layer that provides corrosion resistance. Passivation, typically a nitric or citric acid bath per ASTM A967, removes those particles and restores the passive film. For post-machining surface treatment context, see the CNC deburring process page. Treating passivation as optional on machined stainless parts is a specification gap that shows up as rust in the field.
Frequently Asked Questions
What is the difference between passivation and electropolishing for stainless steel precision parts?
Passivation removes free iron from the surface using a nitric or citric acid bath, restoring the chromium oxide layer without changing part dimensions. Electropolishing goes further, it removes a thin layer of metal through an electrochemical process, simultaneously deburring, brightening, and improving corrosion resistance beyond what passivation achieves. Medical and food-contact parts often specify electropolishing because it produces a microscopically smoother surface that resists bacterial adhesion. Passivation is the lower-cost option when dimensional tolerances are tight and surface removal is not acceptable.
Can stainless steel precision parts be welded without affecting their corrosion resistance?
Yes, but the heat-affected zone around a weld can deplete chromium and create sensitization, reducing local corrosion resistance. Using low-carbon grades such as 304L or 316L limits carbide precipitation during welding. Post-weld passivation or annealing restores the protective oxide layer. For parts where weld integrity is critical, such as medical device housings or automotive fluid fittings, specifying the correct filler material and post-weld treatment in your drawing notes is the most reliable way to protect corrosion performance.
What surface finishes are available for machined stainless steel parts?
Common finishes include as-machined, bead blasting, passivation, electropolishing, and vibratory tumbling. As-machined surfaces typically achieve Ra 1.6–3.2 µm; grinding or lapping can reach Ra 0.2 µm or finer for sealing surfaces. Bead blasting produces a uniform matte appearance without dimensional change. Electropolishing improves both aesthetics and corrosion resistance. The right finish depends on your functional requirements, sealing, biocompatibility, or cosmetic appearance, so specify surface roughness values (Ra) on your drawing rather than finish names alone.
How does tolerance stackup affect stainless steel precision assemblies?
Tolerance stackup occurs when individual part tolerances accumulate across an assembly, causing the final fit or function to fall outside acceptable limits. Stainless steel’s lower thermal conductivity compared to aluminum means parts can expand unevenly under heat, making stackup analysis more critical in temperature-variable environments. Worst-case and statistical stackup analysis during the design phase identifies which dimensions need tighter control. Communicating critical interface dimensions clearly on engineering drawings, and confirming your machining partner holds those tolerances consistently, prevents costly rework at the assembly stage.
What inspection methods are used to verify stainless steel precision parts meet drawing requirements?
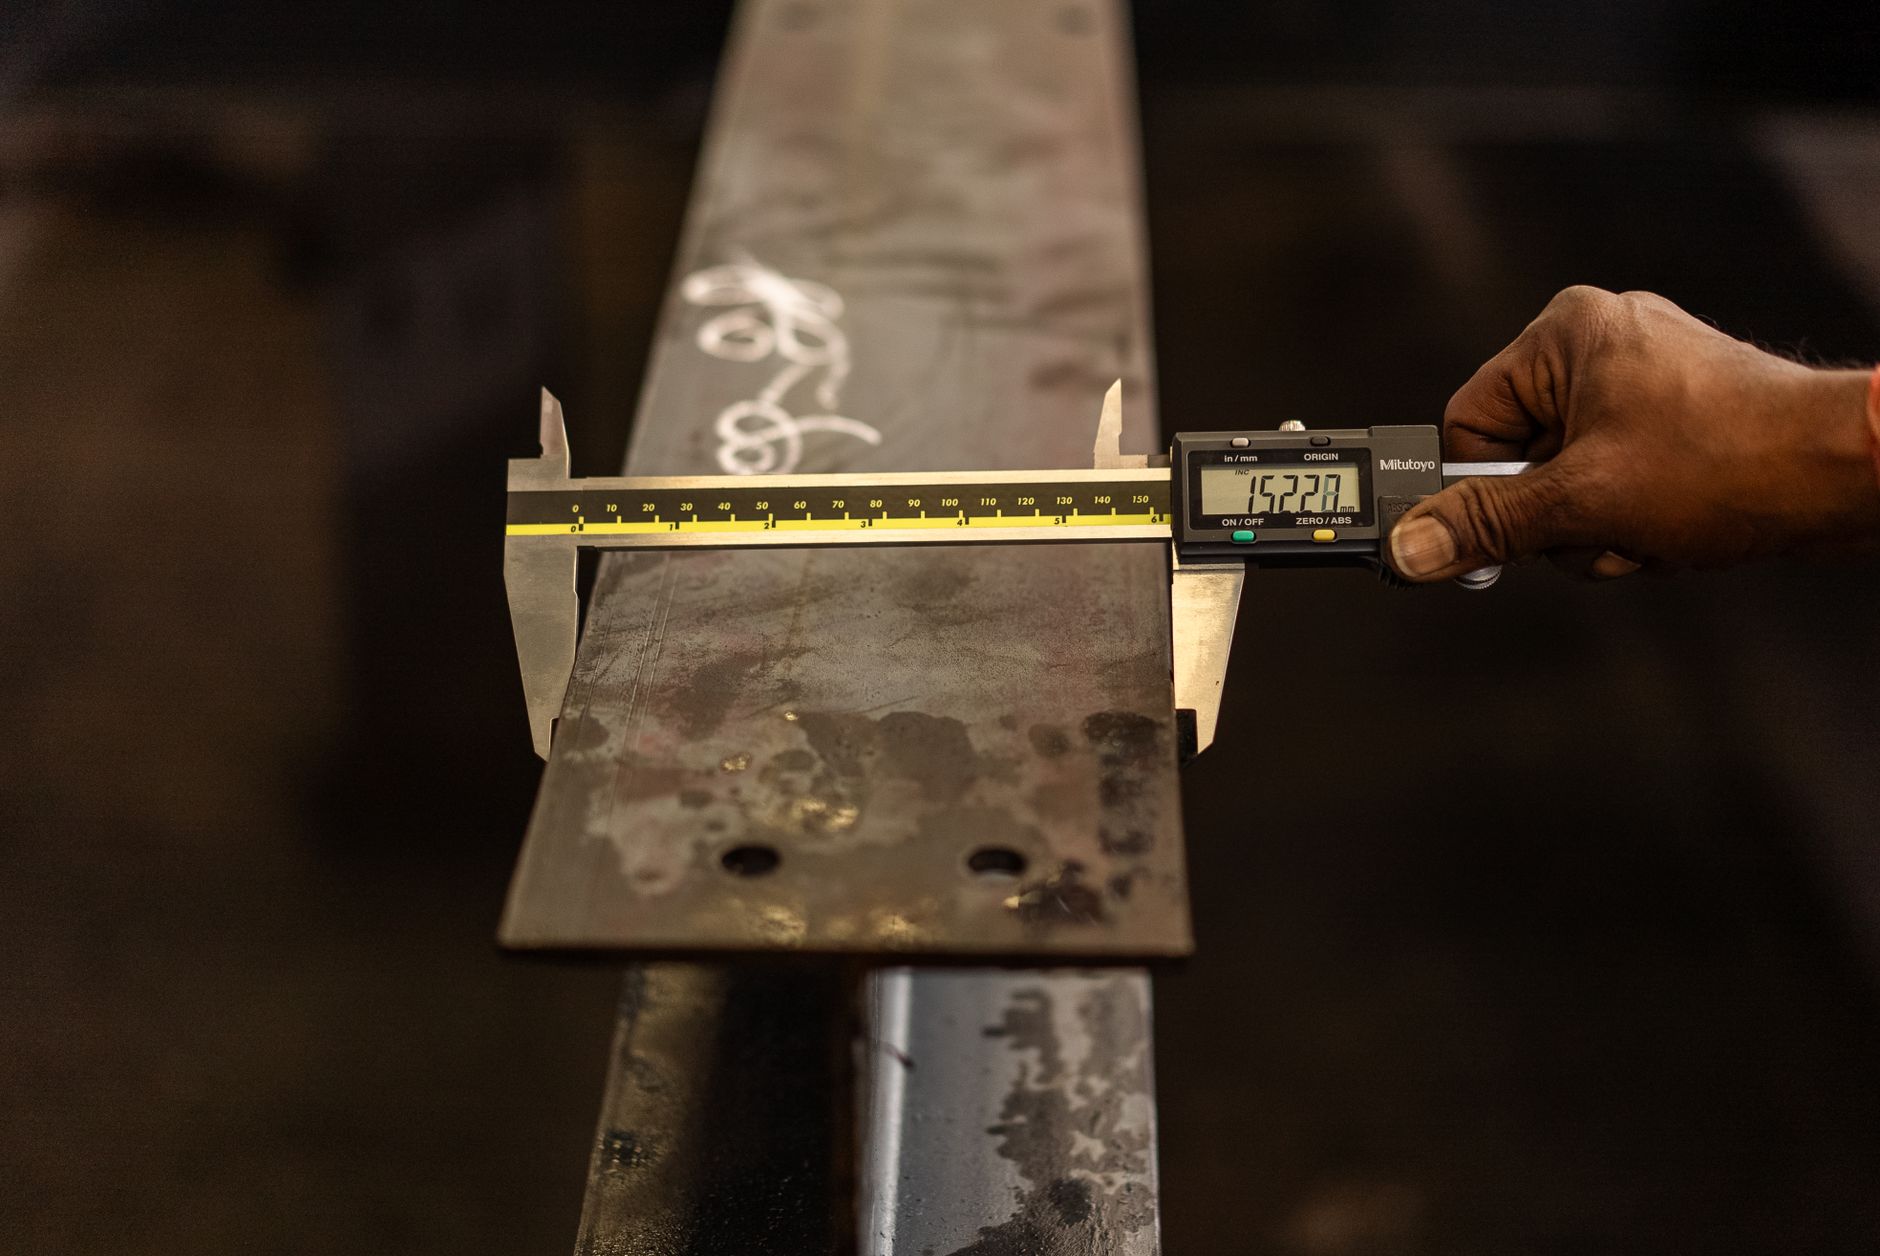
The most common verification methods are coordinate measuring machine (CMM) inspection, optical comparator measurement, surface profilometry for Ra values, and hardness testing where heat treatment is specified. First-article inspection (FAI) documents every critical dimension on the first production part before a full run begins. For high-volume production, statistical process control (SPC) tracks key dimensions across the run to catch drift before it produces out-of-tolerance parts. Requesting a CMM report or first-article inspection report with your initial order is a straightforward way to confirm your supplier’s measurement capability.
Conclusion
Producing reliable this approach comes down to three decisions made early: selecting the right alloy for your corrosion and strength requirements, specifying tolerances and surface finishes on the drawing rather than leaving them to interpretation, and choosing a manufacturing partner whose certifications match your industry’s compliance requirements.
If your parts serve automotive, medical, or electronics applications, verify that your supplier holds IATF 16949, ISO 13485, or ISO 9001:2015 certification before placing a production order, not after a quality escape.
Your concrete next step: submit your part drawing to MFG SOLUTION for a quote. You will receive a detailed response within 8 hours, including process recommendations for your specific geometry and material grade.
Recommended Articles
Explore more from our content library: