
2026-05-05
The CNC Deburring Process: Methods, Tips, and Best Practices

| Key Insight | Explanation |
|---|---|
| What deburring is | The CNC deburring process removes sharp burrs, fins, and micro-edges left after machining, ensuring parts meet dimensional and safety specifications. |
| Why it matters | Burrs can cause assembly failures, accelerate wear, and create safety hazards. Deburring is a non-negotiable step in precision manufacturing. |
| Main methods | CNC-integrated chamfering, robotic brushing, vibratory tumbling, high-pressure waterjet, and thermal/electrochemical deburring each suit different part geometries. |
| Automation advantage | Automated CNC deburring delivers consistent, repeatable results at scale, outperforming manual methods in throughput, accuracy, and cost-per-part. |
| Common mistakes | Over-deburring, wrong technique selection, and skipping post-deburr inspection are the top errors that cause rework and scrap. |
| Quality standards | ISO 9001:2015, ISO 13485:2016, and IATF 16949 all require documented finishing processes, including deburring, as part of full process control. |
Every machined part has a hidden enemy: the burr. The CNC deburring process is the systematic removal of these tiny, often razor-sharp projections that form whenever a cutting tool exits a workpiece. Burrs aren’t just cosmetic problems. They cause assembly failures, accelerate component wear, and in medical or automotive applications, they can create genuine safety hazards. This article explains what CNC deburring is, how each major method works, which technique fits which situation, and what separates a clean, production-ready finish from a costly rework cycle. Whether you’re sourcing small precision parts or running your own shop, you’ll leave with a clear, practical understanding of the entire process.

What Is the CNC Deburring Process?
The CNC deburring process is an automated or semi-automated finishing operation that removes burrs (raised metal edges, fins, or micro-projections) from workpieces produced by CNC machining, turning, milling, or drilling. It goes beyond manual filing: it integrates directly with CNC workflows to deliver burr-free parts that meet tight dimensional and surface specifications.
Defining Burrs and Why They Form
A burr is an unintended raised edge or projection of material left on a workpiece after a machining operation. They form at the exit point of a cutting tool, where the material deforms plastically rather than shearing cleanly. According to the U.S. Department of Energy’s Process Guide for Deburring Technologies [1], burrs are classified by their formation mechanism into rollover burrs, Poisson burrs, tear burrs, and cut-off burrs, each requiring a different removal strategy.
- Rollover burrs: The most common type, formed when material bends over the edge at tool exit.
- Poisson burrs: Caused by lateral material flow perpendicular to the cutting direction.
- Tear burrs: Result from material tearing rather than clean shearing, common in ductile metals.
- Cut-off burrs: Appear at the parting point during turning or sawing operations.
Why Deburring Is Non-Negotiable
Burrs create real downstream problems. In assemblies, they prevent mating surfaces from seating correctly, introducing gaps and misalignment. In moving parts, they accelerate wear and can break free to contaminate lubrication systems. In medical devices and automotive components, a single rogue burr can trigger a product recall or safety failure [2].
The financial stakes are significant: according to a study published by the National Institute of Standards and Technology (NIST), deburring and edge finishing account for up to 30% of total manufacturing costs for precision machined components in some industries, making it one of the largest controllable cost drivers in a machining operation [8].
Industry standards reflect this reality. The National Institute for Metalworking Skills (NIMS) CNC Operator standards explicitly list selecting appropriate deburring tools and determining appropriate deburring processes as core machinist competencies [3]. This isn’t optional finishing work. It’s a quality checkpoint built into the production flow.
How the CNC Deburring Process Works
CNC deburring works by applying controlled mechanical, thermal, chemical, or abrasive energy to targeted part edges, removing material precisely enough to eliminate burrs without altering part geometry or dimensional tolerances.
The Main CNC Deburring Methods
No single method handles every part geometry. The right choice depends on material, part complexity, batch size, and tolerance requirements. Here’s how the primary methods operate:
- CNC-integrated chamfering and contouring: A chamfering tool or deburring end mill is programmed directly into the CNC toolpath. The machine removes the burr in the same setup, eliminating a separate operation. According to Harvey Performance’s machinist blog, in-machine deburring is highly repeatable and reduces overall cycle times by consolidating finishing into the primary machining operation [4].
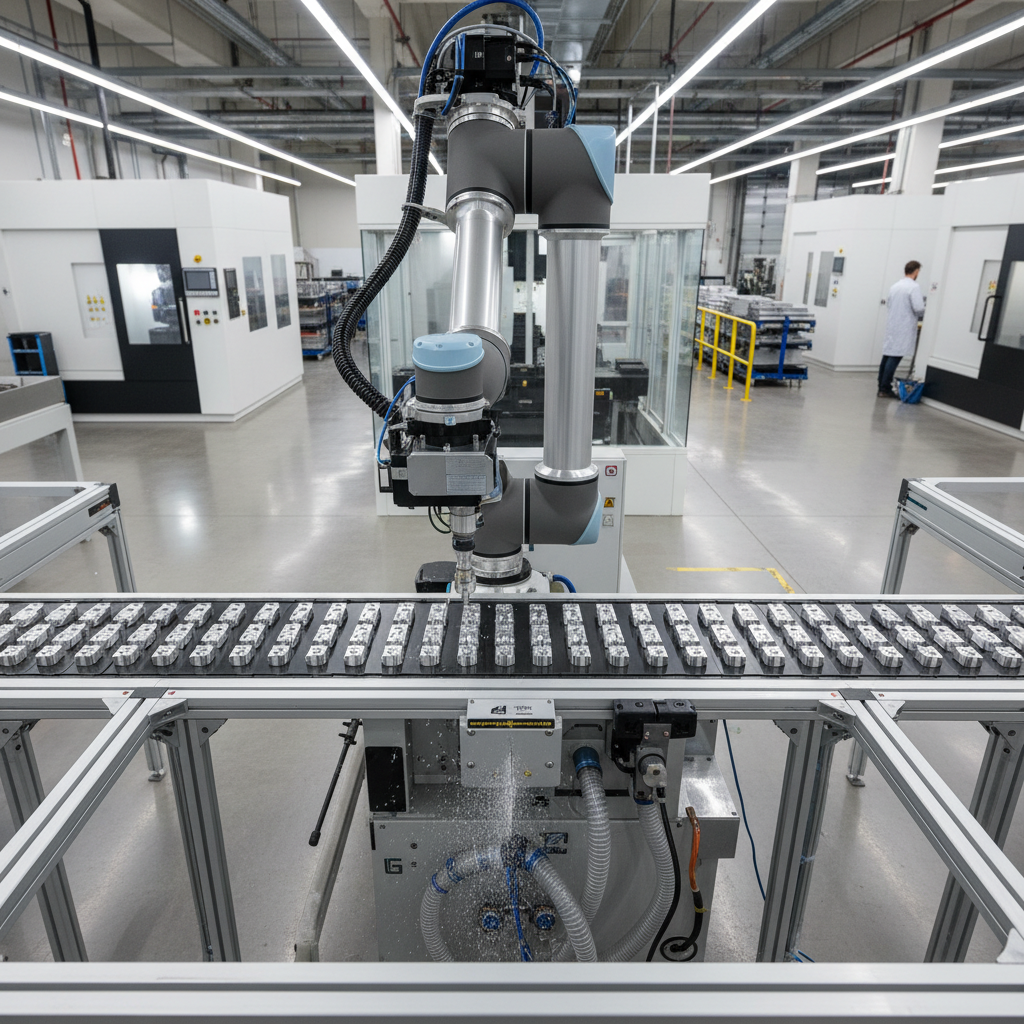
- Robotic brushing: A CNC robot or spindle-mounted brush (ceramic, nylon, or abrasive filament) follows a programmed path across part surfaces. This method excels on complex 3D contours where rigid tools can’t reach. Advanced Manufacturing reports that ceramic end brushes can cut cycle times significantly while maintaining precision in tight spaces [5].
- Vibratory tumbling: Parts are placed in a bowl or trough with abrasive media and vibrated. The media works all exposed surfaces simultaneously. It’s cost-effective for high volumes of small parts but doesn’t discriminate between surfaces, so it’s unsuitable for parts with tight tolerances on specific features.
- High-pressure waterjet deburring: CNC-controlled water jets at pressures up to 60,000 PSI blast burrs from internal passages, cross-drilled holes, and complex geometries. The Society of Manufacturing Engineers (SME) notes that waterjet deburring uses the kinetic energy of the jet to remove burrs with speed and effectiveness that mechanical methods can’t match in certain geometries [6].
- Electrochemical deburring (ECD): An electrolytic solution and electrical current dissolve burrs selectively from conductive metals. ECD is ideal for internal features, cross-holes, and areas physically inaccessible to tools.
- Thermal energy deburring (TEM): Parts are placed in a chamber filled with a combustible gas mixture. Ignition creates a brief, intense thermal pulse that burns off burrs (which have a high surface-area-to-mass ratio) without affecting the bulk part. It’s fast but requires specialized equipment and is best for high-volume production.
Pro Tip: For small turned parts under 38mm diameter, program a chamfering pass directly into your CNC toolpath before parting off. This eliminates the burr at the source rather than treating it downstream, saving handling time and reducing the risk of part damage during secondary operations.
| Method | Best For | Tolerance Impact | Volume Suitability |
|---|---|---|---|
| CNC Chamfering | Simple edges, turned parts | Minimal (controlled) | Low to high |
| Robotic Brushing | Complex 3D contours | Low | Medium to high |
| Vibratory Tumbling | High-volume small parts | Moderate (non-selective) | High |
| High-Pressure Waterjet | Internal passages, cross-holes | Very low | Medium to high |
| Electrochemical (ECD) | Inaccessible internal features | Very low | Medium |
| Thermal (TEM) | Complex multi-feature parts | Very low | High |
Key Benefits of CNC Deburring for Precision Parts
CNC deburring delivers measurable improvements in part quality, production efficiency, and downstream assembly performance, making it one of the highest-return finishing investments in precision manufacturing.
Quality, Safety, and Functional Performance
Clean edges aren’t just aesthetics. They’re a functional requirement. Parts with residual burrs fail dimensional inspections, create assembly interference, and in regulated industries, they trigger non-conformance reports that cost far more than the deburring operation itself.
- Dimensional conformance: Burrs can add measurable material to a feature, pushing it outside tolerance. Removing them restores the true dimension the drawing specifies.
- Surface integrity: Proper deburring preserves the surface finish Ra (average roughness) required for sealing surfaces, bearing fits, and fluid passages.
- Assembly reliability: Burr-free mating surfaces seat correctly, reducing torque scatter in threaded fasteners and improving seal integrity in hydraulic and pneumatic assemblies [7].
- Worker and end-user safety: Sharp burrs cause lacerations during handling and assembly. Removing them protects both factory workers and end users of the finished product.
- Extended component life: Burrs act as stress concentrators. Under cyclic loading, they initiate fatigue cracks. Deburring extends fatigue life, especially in aerospace and automotive structural parts.
Production Efficiency and Cost Savings
Automated CNC deburring reduces labor costs and cycle times compared to manual methods. A machinist spending 2-3 minutes hand-filing each part across a batch of 5,000 units represents significant labor cost. Integrating deburring into the CNC program or a post-process automated cell eliminates that entirely.
Research from NIST’s advanced deburring system technology program demonstrated that automated deburring systems incorporating expert planning modules could dramatically reduce the time and cost associated with post-machining finishing, particularly for complex geometries [8]. For manufacturers running batch production of small components, this translates directly to lower cost-per-part and faster delivery cycles.
Thinking about how automation integrates across your entire manufacturing workflow? The principles behind Automatisation Processus M Tier R Volutionnez Votre Org apply directly to how deburring can be folded into a broader, more efficient production architecture.
Common Challenges and Mistakes in the CNC Deburring Process
The most common failures in the CNC deburring process aren’t technical, they’re process decisions: choosing the wrong method, skipping inspection, or treating deburring as an afterthought rather than a planned production step.
Technique Mismatch and Over-Deburring
Choosing the wrong deburring technique for the part geometry is the single most common mistake. A vibratory tumbler that works perfectly for simple turned pins will round over the sharp corners of a milled slot that the drawing requires to be maintained. Conversely, using electrochemical deburring on a part that only needs a simple chamfer is expensive overkill.
Over-deburring is equally damaging. Applying too much abrasive pressure or running a part through a tumbler too long removes more material than intended, altering edge geometry and potentially pushing critical dimensions out of tolerance. DATRON’s finishing guide emphasizes that deburring should remove only the burr itself, not reshape the underlying part geometry [9].
- Mistake 1: Relying exclusively on manual deburring for production volumes. Manual filing is inconsistent between operators and unsustainable at scale. One operator removes 0.05mm of material; another removes 0.15mm. That variability shows up in assembly.
- Mistake 2: Not integrating deburring into the process plan. Treating it as a separate, informal step means it gets skipped under schedule pressure. It needs to be a documented, timed operation with defined acceptance criteria.
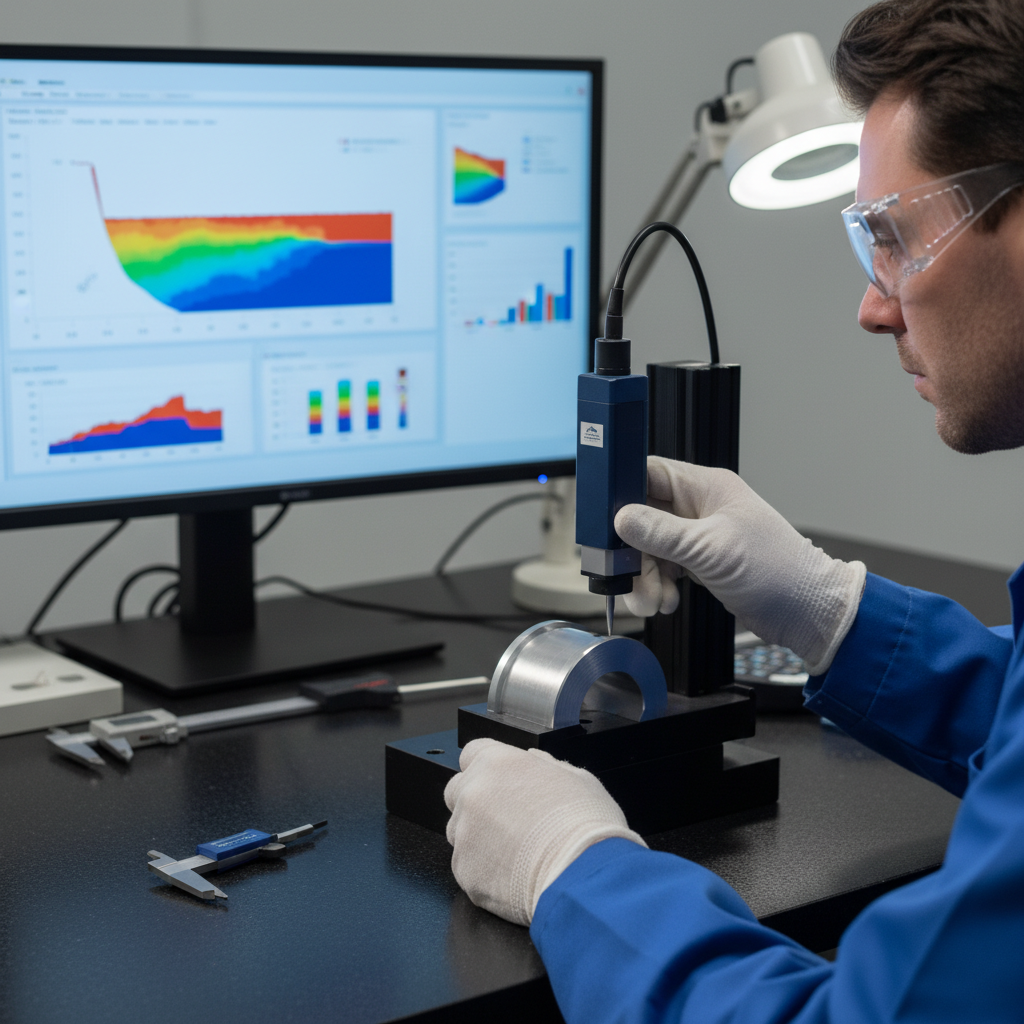
- Mistake 3: Skipping post-deburr inspection. Deburring without verification is incomplete. A part that looks clean to the naked eye may still have micro-burrs detectable under magnification that will cause problems in precision assemblies.
- Mistake 4: Ignoring burr direction. Burrs have a grain direction. Deburring against the grain can fold the burr over rather than removing it, creating a work-hardened flap that’s harder to remove in subsequent passes.
Material-Specific Pitfalls
Different materials behave differently during deburring. Aluminum is soft and deburrs easily but is prone to smearing. Stainless steel work-hardens quickly, so aggressive deburring can make subsequent passes harder. Titanium requires careful method selection to avoid introducing heat that alters the surface microstructure.
In practice, a precision machining client once submitted stainless steel medical components for vibratory tumbling without specifying the alloy grade. The 316L stainless work-hardened during tumbling, and the resulting surface condition failed the Ra specification for implant-adjacent parts. The fix required electrochemical finishing, doubling the processing time. Specifying the material and its work-hardening characteristics upfront would have prevented the issue entirely.
Pro Tip: Always specify your material’s alloy grade, hardness, and any surface finish requirements on your part drawing before requesting deburring. Vague material callouts lead to method mismatches that cost time and money to correct.
Best Practices for CNC Deburring in 2026
As of 2026, the best CNC deburring operations integrate deburring planning into the design and programming phase, not as an afterthought after parts come off the machine.
Design for Deburring (DfD)
The most effective deburring strategy starts before machining begins. Design for Deburring (DfD) is a methodology that considers how burrs will form and how they’ll be removed during the part design and process planning phase. Applying DfD principles consistently reduces deburring time and cost.
- Minimize sharp internal corners. Generous radii at pocket corners reduce the severity of burrs formed by end mills and make them easier to remove.
- Specify edge breaks on drawings. Explicitly calling out “break all sharp edges 0.1-0.2mm” gives the machinist a quantified target and prevents over-deburring.
- Orient cross-holes for accessibility. If a part requires cross-drilled holes, position them so a waterjet or brush can reach the intersection. Hidden cross-holes require expensive electrochemical or thermal methods.
- Choose machinable alloys where possible. Free-machining grades (e.g., 12L14 steel, 6061-T6 aluminum) produce smaller, more brittle burrs that are easier to remove than burrs from tough alloys like Inconel or titanium.
- Program chamfers into the CNC toolpath. A 0.2mm x 45° chamfer programmed on all exit edges costs seconds of machine time and eliminates the burr before it forms as a separate problem.
Inspection and Documentation Standards
Post-deburr inspection isn’t optional in regulated industries. Under ISO 9001:2015, ISO 13485:2016, and IATF 16949, finishing processes including deburring must be documented, controlled, and verified. This means:
- Defined acceptance criteria for edge condition (typically Ra, edge break size, or visual standard)
- Documented deburring method, media type, and process parameters for each part number
- First-article inspection after deburring to confirm dimensional conformance
- Traceability records linking each batch to its deburring parameters
At MFG SOLUTION, we’ve found that building deburring parameters into the part traveler (the document that follows a job through the shop) eliminates ambiguity and ensures every operator applies the same process regardless of shift or volume pressure. This is what “full process control” actually means in practice: every step tracked, documented, and auditable.
Industry analysts at MSC Industrial Supply’s knowledge center note that automation in deburring, from robotic cells to integrated CNC finishing cycles, is the clear direction for precision manufacturers in 2026, driven by labor cost pressures and the need for consistent, repeatable quality at scale [10].
Pro Tip: Use a go/no-go edge radius gauge or a profilometer to verify edge break dimensions after deburring. Visual inspection alone misses micro-burrs that cause assembly problems downstream, especially on parts destined for medical or automotive applications.
Sources & References
- U.S. Department of Energy / OSTI, “Process Guide for Deburring Technologies,” 2014
- AMP CNC, “Deburring Machined Parts: Effective Methods for Clean, Safe Finishes,” 2024
- National Institute for Metalworking Skills (NIMS), “ISV Interactive Smart Standards: CNC Operator,” 2026
- Harvey Performance Company, “Deburring End Mills,” In the Loupe Machinist Blog, 2024
- Advanced Manufacturing, “Brushing Up on Deburring and Finishing in Tight Spaces,” 2025
- Society of Manufacturing Engineers (SME), “Deburring Processes and Challenges,” 2024
- Air Turbine Tools, “What is Deburring? Process & Guide,” 2024
- National Institute of Standards and Technology (NIST), “Advanced Deburring System Technology,” 2014
- DATRON, “Finishing Guide: What Is Deburring?,” 2024
- MSC Industrial Supply, “The Essential Guide to Deburring: Tools, Techniques and Tips,” 2025
Frequently Asked Questions
1. What is deburring CNC?
The CNC deburring process is an automated or semi-automated finishing operation that removes burrs (unwanted raised edges, fins, or sharp projections) from workpieces produced by CNC machining, turning, milling, or drilling. Unlike manual filing, CNC deburring integrates directly into the machining workflow through programmed toolpaths, robotic cells, or post-process automated systems, delivering consistent, repeatable edge quality across high-volume production runs. Left untreated, burrs compromise dimensional accuracy, assembly fit, surface integrity, and safety in the finished product.
2. What is the process of deburring?
Deburring is a multi-step finishing process that identifies burr locations on a machined part, selects the appropriate removal method based on material, geometry, and tolerance requirements, applies controlled mechanical, abrasive, thermal, chemical, or hydraulic energy to remove the burrs, and then verifies the result through inspection. The process spans methods from simple in-machine chamfering passes programmed into the CNC toolpath, to vibratory tumbling for bulk small parts, to precision electrochemical deburring for inaccessible internal features. The goal is to remove only the burr without altering the underlying part geometry or surface finish specification.
3. What are common deburring mistakes?
The most costly CNC deburring mistakes include selecting a technique that doesn’t match the part geometry (such as tumbling a part with features requiring sharp maintained edges), over-deburring (removing more material than intended and pushing dimensions out of tolerance), relying on manual deburring for production volumes (introducing operator-to-operator variability), and failing to inspect parts after deburring to confirm edge condition meets the drawing specification. A less obvious but equally damaging mistake is treating deburring as an informal, undocumented step rather than a controlled operation with defined parameters, which creates traceability gaps that fail ISO and IATF audits.
4. What is the best deburring technique?
There’s no single best technique. The optimal CNC deburring method depends on part geometry, material, batch size, and tolerance requirements. For simple turned or milled parts, programming a chamfering pass directly into the CNC toolpath is the most efficient and precise option. For complex 3D contours, robotic brushing with ceramic or abrasive-filament brushes delivers consistent results. For internal passages and cross-holes, high-pressure waterjet or electrochemical deburring outperforms mechanical methods. For very high-volume small parts with no tight edge requirements, vibratory tumbling offers the lowest cost per part. Matching the method to the specific part geometry is always the right starting point.
5. Can deburring affect part tolerances?
Yes. Aggressive or poorly controlled deburring methods can remove measurable material from functional surfaces, altering dimensions and potentially pushing a part outside its specified tolerance band. This is especially true with abrasive methods like vibratory tumbling or grinding, which don’t discriminate between burr material and base material. The CNC deburring process, when properly controlled, targets only the burr with defined parameters (media type, duration, pressure) to minimize material removal from functional surfaces. Post-deburr dimensional inspection is the verification step that confirms tolerances are maintained.
6. How does deburring fit into ISO-certified manufacturing?
Under ISO 9001:2015, ISO 13485:2016, and IATF 16949, deburring is a controlled process that must be documented, parameterized, and verified. This means defining the deburring method, media or tooling, process duration or parameters, and acceptance criteria for each part number in the process documentation. Inspection records after deburring must be maintained for traceability. Treating deburring as an informal, operator-discretion step will fail an audit. Certified manufacturers build deburring specifications directly into the part traveler and control plan, ensuring every batch receives the same treatment regardless of who runs the operation.
Conclusion
The CNC deburring process is not a minor finishing detail. It’s a critical quality step that determines whether a precision part performs as designed, passes inspection, and survives in service. Choosing the right method for the geometry, integrating deburring into the process plan from the design phase, and verifying results through documented inspection are what separate production-ready parts from costly rework cycles.
For manufacturers sourcing small precision parts, your supplier’s approach to deburring is a direct indicator of their overall quality discipline. At MFG SOLUTION, deburring is a documented, controlled step within our ISO 9001:2015, ISO 13485:2016, and IATF 16949 certified process, not an afterthought. Our team of 60+ engineering professionals selects the appropriate deburring method for each part geometry, whether that’s in-machine chamfering on our 5-axis CNC machines, automated brushing, or post-process finishing, and verifies the result before shipment. With quotes within 8 hours and parts shipped within 3 days, you get burr-free, inspection-ready components without the wait.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: