2026-09-01
6 Best Practices for Aluminum Precision Machining Success
Aluminum precision machining is the process of using CNC equipment to cut, mill, turn, or drill aluminum alloys to tight dimensional tolerances, typically for aerospace, automotive, medical, and electronics applications. Aluminum machines faster than steel, dissipates heat efficiently, and delivers an excellent strength-to-weight ratio, making it the default choice when part complexity, weight, and repeatability all matter. Choosing the right alloy, tolerances, and machining partner determines whether a project ships on time and within spec.
1. What Aluminum Precision Machining Is and Why It Matters
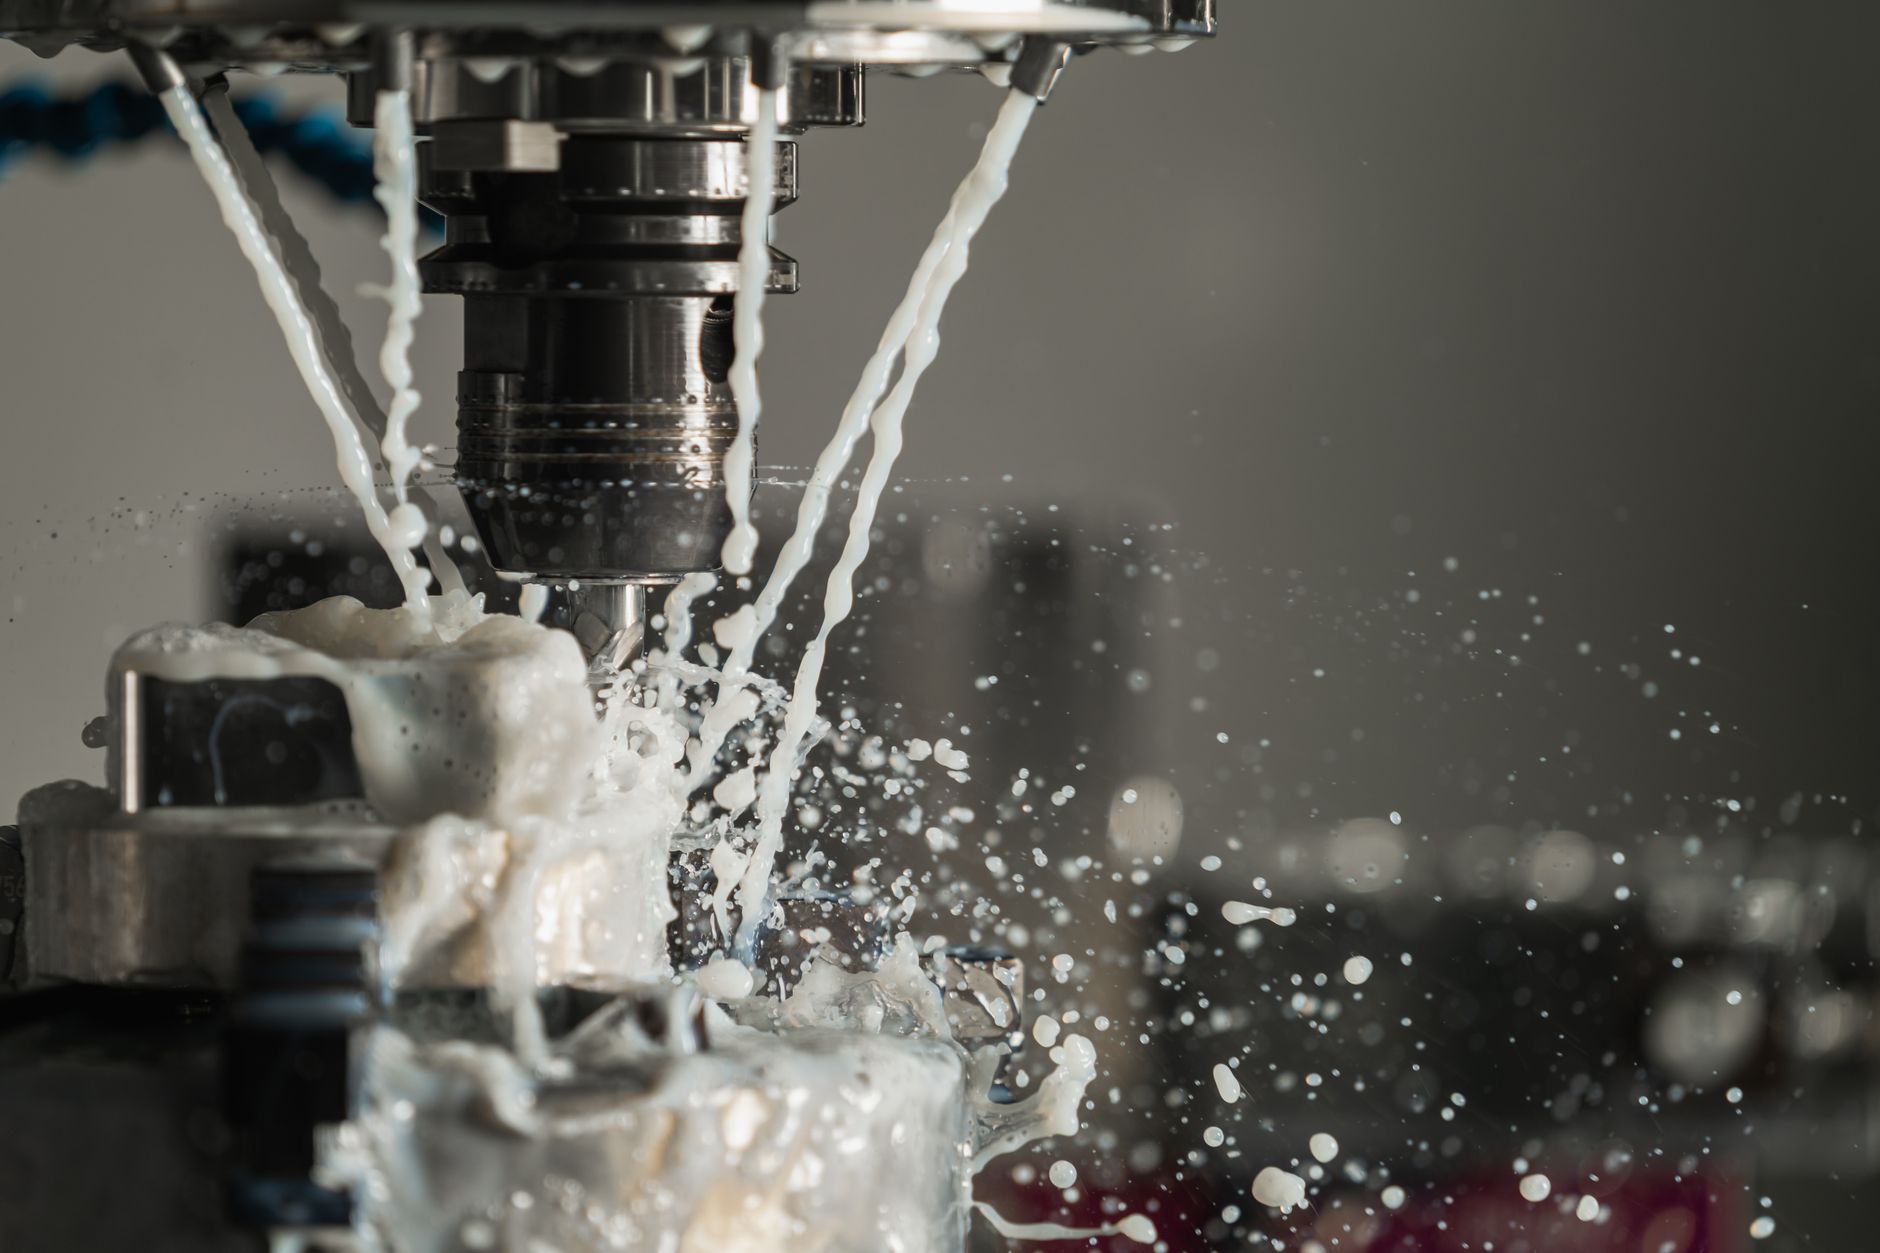
Aluminum precision machining is CNC-controlled material removal that holds tight dimensional tolerances across complex geometries, consistently, at production scale.
The process uses CNC mills, lathes, and multi-axis equipment to cut aluminum parts to exact specifications. What separates it from general fabrication is documented tolerances, process control, and full traceability at every production stage, not just cutting metal and hoping dimensions land close enough.
Why Aluminum Is Ideal for CNC Machining Compared to Other Materials
Aluminum machines roughly three to four times faster than steel and significantly faster than titanium. That speed advantage means lower tool wear, shorter cycle times, and faster delivery, without sacrificing dimensional accuracy on tight-tolerance features.
Aerospace, automotive, medical devices, electronics, and defense all depend on aluminum precision machining because the material combines a high strength-to-weight ratio with excellent corrosion resistance and consistent machinability across alloy grades. Those properties make it the default choice when weight, speed, and part quality must align simultaneously.
Common Applications Across Industries
The breadth of industries relying on aluminum precision machining reflects how versatile the material and process combination truly is. Typical applications include:
- Aerospace: Structural brackets, housings, and flight-critical components requiring tight tolerances and full traceability
- Automotive: Engine components, transmission housings, and lightweight structural parts where weight reduction drives fuel efficiency
- Medical devices: Surgical instrument bodies, implant components, and diagnostic equipment housings requiring ISO 13485-compliant manufacturing
- Electronics: Heat sinks, enclosures, and connector bodies where dimensional accuracy and thermal conductivity both matter
- Defense: Weapon system components and ruggedized enclosures where material consistency and traceability are non-negotiable
Each of these applications places different demands on alloy selection, tolerance specification, and post-processing, which is why understanding the full scope of aluminum precision machining decisions matters before a single cut is made.
2. Choosing the Right Aluminum Alloy for Precision Machining
Alloy selection is the single most consequential decision before machining begins, the wrong choice drives up tool wear, cost, and lead time regardless of shop capability.
When Should You Use 6061 Aluminum for Precision Parts?
6061-T6 is the workhorse alloy for a reason. It machines cleanly, resists corrosion well, welds without issue, and suits structural and general-purpose precision parts across electronics, automotive, and industrial applications. When no single requirement dominates, 6061 is the default starting point.
Is 7075 Aluminum Machinable and What Are Its Advantages?
7075 is machinable, but it demands more from your tooling. Its tensile strength makes it the preferred choice for aerospace and defense components where load-bearing performance is non-negotiable. The trade-off is higher tool wear and greater material cost compared to 6061, factors that compound on high-volume runs.
2024 suits fatigue-critical aerospace applications where cyclic loading is the primary design constraint. 5052 fits sheet-form or marine environments where corrosion resistance outweighs strength requirements.
The decision rule: identify the dominant requirement, strength, corrosion resistance, weight, or machinability, and let that drive alloy selection before finalizing your design. Locking in the wrong alloy mid-project adds cost and delay that no machining speed advantage recovers.
3. Tolerances and Machining Capabilities Modern Aluminum Shops Achieve
A capable aluminum precision machining shop holds tolerances in the ±0.001–0.005 inch range and delivers complex geometries in a single setup using 5-axis equipment.
5-axis CNC machines cut from multiple angles without repositioning the part. That matters because each re-fixturing step introduces potential alignment error, eliminating those steps directly improves repeatability on complex features. MFG SOLUTION operates 5-axis CNC machines alongside 20 automatic lathes, supporting tight-tolerance production runs on parts up to 38mm in diameter.
What Built-In Quality Control Methods Ensure Precision?
End-of-line inspection catches defects too late. Built-in quality control means in-process inspection at each production stage, CMM verification against the design file, and documented traceability that makes every measurement auditable. That approach, tracking conformance through the process rather than after it, is what separates certified shops from generalist job shops.
Surface finish selection also affects function, not just appearance. As-machined surfaces suit tight-fit assemblies where dimensional accuracy is the priority. Anodized finishes add corrosion and wear resistance. Bead-blasted surfaces reduce reflectivity and improve adhesion for downstream coatings. For a detailed look at managing cumulative dimensional variation across assemblies, see the site’s precision tolerance stackup guide.
4. Thin-Wall Aluminum Machining: Practical Limits and Design Rules
Thin-wall aluminum deflects under cutting forces before it fractures, making fixturing strategy and toolpath sequencing more critical than raw machine capability.
When wall thickness drops, the ratio of cutting force to material rigidity shifts. The cutter pushes the wall away rather than removing material cleanly, causing dimensional drift and surface inconsistency that thicker stock never produces. This is a physics problem, not a machine problem, and it requires a process solution.
Design Considerations for Thin-Wall Aluminum Components
Effective thin-wall strategies combine low-engagement passes, climb milling to reduce radial cutting forces, custom soft jaws that distribute clamping load without distorting the part, and strategic sequencing that leaves support material in place until final passes. Each of these decisions happens before the first cut, not during troubleshooting.
Wall geometry starts to compromise dimensional stability when thickness falls below roughly 0.040 inches for unsupported spans, though the exact threshold depends on alloy, part geometry, and clamping configuration. A design for manufacturability (DFM) review catches these issues before cutting begins, and before scrap costs accumulate. Thin-wall capability is a meaningful differentiator: ask any prospective machining partner directly whether they perform DFM review on thin-wall features before quoting.

5. Quality Certifications and Compliance Standards for Aluminum Machined Parts
The certification a shop holds determines whether its parts are legally acceptable in your supply chain, a logo on a website is not the same as a current, scoped certificate.
Each standard requires something specific in practice. ISO 9001:2015 establishes the baseline quality management system: documented processes, corrective action protocols, and management review cycles. AS9100 adds aerospace-specific traceability requirements, first article inspection, configuration control, and risk management tied to flight-critical components. ISO 13485:2016 governs medical device supply chains, requiring design controls, complaint handling, and sterility-compatible process documentation. IATF 16949 applies to automotive production, mandating statistical process control, FMEA, and production part approval (PPAP) documentation.
Which Regulated Industries Require Specific Certifications?
Aerospace primes and their Tier 1 suppliers require AS9100. Medical device OEMs sourcing machined components must work with ISO 13485-certified suppliers to satisfy FDA 21 CFR Part 820 and EU MDR requirements. Automotive OEMs and Tier 1 suppliers mandate IATF 16949 for production parts. Sourcing from an uncertified shop in any of these industries creates direct downstream risk: rejected shipments, failed supplier audits, and liability exposure if a non-conforming part reaches a regulated assembly.
MFG SOLUTION holds ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, covering medical, automotive, and general manufacturing supply chains from a single source. To verify any shop’s certification claims, request the current certificate, confirm the registrar name, check the scope statement matches your part type, and verify the expiry date. A logo on a marketing page proves nothing; a current certificate from an accredited registrar does. For deeper compliance guidance, see the site’s ISO 9001 precision machining and CNC machining quality assurance resources.
6. Lead Times and Production Timelines for Aluminum Machining Projects
Aluminum machining lead times range from 3 days for simple prototype runs to 6–8 weeks for high-volume production with post-processing, the phase that slips most is post-processing, not cutting.
A standard project moves through six phases: RFQ and quoting, DFM review, CNC programming, first-article inspection (FAI), production run, and final QC before shipment. Each phase adds time, but DFM review and FAI are where most delays originate, especially when part drawings require revision or tolerances trigger additional inspection steps.
What Turnaround Capabilities Should You Expect from Different Shop Types?
Timeline variation is driven by five factors: part complexity, alloy availability (6061 ships from stock; some 7075 variants require lead time to source), tolerance tightness, post-processing requirements such as anodizing or heat treatment, and order volume. A shop quoting a prototype in 48 hours may quote the same part at production volume with a 4-week lead time, those are structurally different commitments.
Shops that quote within hours and ship within days represent a meaningful operational difference. MFG SOLUTION quotes within 8 hours of specification submission and ships within 3 days of order approval, a turnaround that applies to production batches, not just one-off samples, backed by ISO 9001:2015 process controls that keep FAI and QC from becoming bottlenecks.
7. Cost Drivers in Aluminum Precision Machining
Part complexity and setup time are the dominant cost drivers in aluminum CNC machining, not raw material price, which is often the first number buyers check.
Four mechanisms determine per-part cost: the number of operations and fixturing changes required, tolerance tightness (tighter tolerances mean slower feeds, more tool passes, and additional inspection steps), post-processing requirements such as anodizing or heat treatment, and the total order volume that amortizes setup cost.
How Production Volume Affects Per-Part Cost Structure
Low-volume prototype runs carry the full weight of setup cost on a handful of parts. High-volume production runs spread that fixed cost across hundreds or thousands of parts, but only if the process is stable enough to run without rework. Process instability at volume erases the per-part savings quickly.
Alloy selection affects cost earlier than most buyers realize. 6061 is budget-friendly for standard-tolerance work and widely stocked. Multi-axis or tight-tolerance work moves into mid-range pricing territory. 7075 and specialty alloys carry higher material and tooling costs, harder alloys accelerate tool wear, which should factor into design decisions before an RFQ is issued, not after. Regulated medical or automotive runs requiring full traceability under ISO 13485:2016 or IATF 16949 add documentation overhead that sits in the premium tier.
8. In-House Aluminum Machining vs. Outsourcing to a Specialist Shop
Outsourcing aluminum CNC machining to a certified specialist typically delivers lower total cost and faster turnaround than in-house production for most manufacturers, unless volume is very high and parts are highly standardized.
In-house machining carries costs that rarely appear in a capital equipment proposal: operator training and retention, tooling inventory, preventive maintenance contracts, calibration, and the floor space that could otherwise run production. A 5-axis CNC machine purchase price is the starting point, not the total cost.
In-house investment makes sense in three specific situations: very high volumes of a single standardized part where setup amortization is favorable, proprietary process IP that cannot leave the facility, or supply chain security requirements that override unit economics.
Outsourcing wins when volumes vary, geometries require multi-axis equipment you don’t own, or your industry demands certified shops, medical device manufacturers need ISO 13485:2016 compliance; automotive suppliers need IATF 16949. Speed-to-market is the clearest case: a specialist shop with 60+ engineering professionals and established process controls will outrun an in-house team standing up a new capability from scratch.
The core question is whether machining is your primary value-add. If it isn’t, a certified specialist delivers better quality, faster turnaround, and lower total cost than building and maintaining that capability internally.
9. Key Factors for Choosing an Aluminum Precision Machining Partner
The four non-negotiable evaluation criteria for an aluminum machining partner are: documented equipment capability, active certifications scoped to your industry, quoting responsiveness, and confirmed scalability from prototype to production.
Start with capability checks: multi-axis CNC equipment, documented tolerance capability (not just claimed), alloy range including 6061 and 7075, and post-processing options, anodizing, heat treatment, surface finishing, handled in-house or through a controlled supply chain. A shop that subcontracts post-processing without oversight introduces quality risk at the handoff.
When evaluating potential aluminum precision machining partners, use the following checklist to structure your assessment:
- Confirmed multi-axis CNC capability (3-axis minimum; 5-axis preferred for complex geometries)
- Documented tolerance capability with CMM verification records available on request
- Active certifications scoped to your industry (ISO 9001, ISO 13485, IATF 16949, or AS9100)
- In-house or controlled post-processing (anodizing, heat treatment, surface finishing)
- DFM review offered before programming begins
- Quoting turnaround of 24 hours or less for standard parts
- Scalability from prototype quantities to full production runs on the same quality system
How Certifications Like ISO and AS9100 Impact Your Partner Choice
Certifications are a hard filter for regulated industries, not a differentiator to note and move past. Read the certificate scope carefully: ISO 9001:2015 covers general quality management; ISO 13485:2016 must explicitly cover medical device manufacturing; IATF 16949 must cover automotive production. A certificate that doesn’t name your part category or industry provides no compliance coverage for your audit trail.
Responsiveness is a reliable proxy for operational health. Shops that return quotes within hours and provide DFM feedback before programming begins have mature processes. Slow or vague quoting, “we’ll get back to you in a few days”, signals capacity constraints or communication gaps that compound at production volume.
Confirm scalability before issuing a purchase order. A partner worth committing to can handle prototype quantities and production ramp on the same quality system, without re-quoting from scratch or losing dimensional consistency as volume increases.
How to Choose the Right Aluminum Precision Machining Approach for Your Project
Match your dominant project requirement, strength, weight, corrosion resistance, cost, or regulatory compliance, to alloy and shop type first; every other decision follows from that single choice.
Step 1, Define the dominant requirement. A structural aerospace bracket and a consumer electronics enclosure are both aluminum precision machining projects, but they require different alloys, tolerances, and certifications. Naming the primary driver before selecting a supplier eliminates most mismatches.
Step 2, Qualify tolerance and geometry complexity. Standard tolerances in simple geometries open up a wider supplier pool. Tight tolerances, thin walls, or undercuts require shops with documented multi-axis capability and in-process inspection, not just claimed capability on a spec sheet.
Step 3, Match certification scope to your industry. Verify the supplier’s certificate explicitly covers your part category before issuing an RFQ. A general ISO 9001:2015 certificate does not substitute for ISO 13485:2016 in medical device supply chains or IATF 16949 in automotive.
Step 4, Evaluate total cost of ownership. Per-part price is one input. Setup amortization, post-processing, inspection documentation, and lead time cost, expedite fees, inventory carrying cost when a supplier runs late, determine the real comparison between suppliers.
Step 5, Run a pilot order. Prototype quantities reveal quoting speed, DFM feedback quality, first-article accuracy, and communication before you commit production volumes. MFG SOLUTION’s 8-hour quote and 3-day ship window makes this evaluation fast: you can assess real operational performance, not sales claims, within a week of submitting your first specification.
Frequently Asked Questions
What is the difference between aluminum CNC machining and aluminum precision machining?
Aluminum CNC machining refers to the process; aluminum precision machining describes the tolerance standard applied to that process. CNC machining uses computer-controlled tools to cut aluminum to a programmed shape. Precision machining adds the requirement that those cuts hold tight dimensional tolerances, typically ±0.005 mm or tighter, with full inspection and process control to verify every part meets spec before it ships.
Which aluminum alloy is easiest to machine?
6061-T6 is the most widely used aluminum alloy for CNC machining because it cuts cleanly, holds tight tolerances, and resists corrosion well. 7075 machines slightly harder but delivers higher strength for structural applications. For high-volume small parts, 6061 is the default starting point unless your design requires 7075’s strength-to-weight advantage.
What quality certifications should an aluminum machining shop hold for aerospace or medical parts?
For medical parts, require ISO 13485:2016; for automotive, require IATF 16949; for general industrial and aerospace supply chains, ISO 9001:2015 is the baseline. AS9100 is the aerospace-specific standard to look for when parts go directly into flight-critical assemblies. A shop holding all three, ISO 9001, ISO 13485, and IATF 16949, can serve medical, automotive, and electronics customers from a single certified quality system.
How do lead times for aluminum prototype machining compare to production run lead times?
Prototype lead times are typically shorter per part but longer per order because setup, programming, and first-article inspection dominate the schedule. Production runs spread that fixed setup cost across hundreds or thousands of parts, cutting per-unit time significantly. Shops with rapid quoting, MFG SOLUTION returns quotes within 8 hours and ships within 3 days, close that gap for small-batch production runs up to 38mm diameter.
What surface finishes are available for aluminum precision machined parts?
The most common surface finishes for aluminum precision machined parts include as-machined, anodizing (Type II and Type III hard anodize), bead blasting, chemical film (Alodine/Chromate), and powder coating. As-machined surfaces preserve the tightest dimensional tolerances. Anodizing adds corrosion and wear resistance without significantly altering dimensions. The right finish depends on the functional environment, assembly fit requirements, and any regulatory standards governing the end application.
Conclusion
Aluminum precision machining rewards preparation: alloy selection, tolerance specification, and supplier certification matter more than any single process decision. Match your alloy to your application, 6061 for general use, 7075 for high-stress environments, and confirm your shop holds the certifications your industry requires before you place an order.
For small precision parts up to 38mm diameter, the fastest concrete next step is to submit your part drawing to MFG SOLUTION for a quote. You’ll have a detailed response within 8 hours, enough information to compare against your current supplier’s lead time and cost before committing to a production run.
Recommended Articles
Explore more from our content library: