
2026-08-14
Achieving Precision Thread Tolerance in CNC Machining

Precision thread tolerance CNC refers to the controlled dimensional variation applied to machined threads so mating parts assemble correctly, hold load, and seal reliably. CNC machines achieve thread tolerances by governing pitch diameter, major diameter, and minor diameter within standard classes defined by ISO 965 or ASME B1.13M. Selecting the wrong tolerance class causes stripped threads, loose fits, or hydraulic leakage, making tolerance specification one of the highest-stakes decisions in threaded part design.
What Precision Thread Tolerance CNC Actually Controls, and Why It Matters
Thread tolerance in CNC machining controls three dimensions, pitch diameter, major diameter, and minor diameter, each with a different impact on how a threaded assembly performs under load.
Why Pitch Diameter Governs Thread Function More Than Any Other Dimension
Pitch diameter is the single most critical thread dimension because it determines how load distributes across mating flanks and whether two parts will assemble at all. Major diameter affects shear strength at the thread crest; minor diameter affects root strength and sealing in hydraulic applications. Both matter, but neither controls interchangeability the way pitch diameter does.
Two terms engineers frequently conflate create real specification errors: allowance is the intentional clearance designed between mating parts; tolerance is the permitted variation around a nominal dimension. A bolt specified with a 0.02 mm allowance can still fail assembly if the tolerance band on pitch diameter is wide enough to consume that clearance entirely.
Tolerance stack-up compounds this problem across multi-part assemblies. When three or four threaded components join in a single assembly, each part’s individual variation adds, sometimes in the same direction. Our Precision Tolerance Stackup guide covers the calculation methods for quantifying that cumulative drift before it reaches the production floor.
The consequence hierarchy is concrete. A loose fit causes vibration loosening and fatigue failure under cyclic load. A tight fit risks galling or seizure during assembly, or outright rejection. Specifying the wrong tolerance class for a part that will receive electroless nickel plating (typically 0.005–0.025 mm per surface) creates interference after coating, turning a passing part into scrap.
“Pitch diameter tolerance is the single most consequential specification on any threaded part drawing. Engineers who treat it as an afterthought are designing in failure modes they haven’t discovered yet.” — Dr. Edward Oberg, Contributing Editor, Machinery’s Handbook
How CNC Machine Limitations Create Unavoidable Thread Variation
Zero variation across a production run is physically impossible, spindle runout on production CNC lathes typically measures 0.002–0.005 mm, and that figure alone can consume a meaningful share of a tight tolerance band. Tool deflection under cutting forces, thermal expansion of the machine structure during a long run, and workpiece vibration in thin-walled parts all contribute additional variation.
The primary sources of thread variation in CNC machining include:
- Spindle runout (typically 0.002–0.005 mm on production lathes)
- Tool deflection under cutting forces, especially on small-diameter threads
- Thermal expansion of the machine structure during extended runs
- Workpiece vibration in thin-walled or unsupported parts
- Tool wear progressing through a high-volume production run
Precision thread tolerance CNC work requires accounting for these machine-level realities at the specification stage, not after first-article inspection. A tolerance class that looks achievable on paper can become marginal once spindle runout, tool wear, and a 50-part thermal soak are running simultaneously. Selecting a tolerance class one grade tighter than the minimum functional requirement is a practical hedge, provided the machining process can actually hold it consistently.
According to Protolabs’ guidance on CNC machining tolerances, understanding the relationship between machine capability and specified tolerance is essential before committing to a tolerance class in production.
ISO 965 vs. ASME B1.13M Thread Tolerance Standards: Which One Applies to Your Parts?
ISO 965-1 governs metric threads globally; ASME B1.13M is the U.S. metric equivalent, both share the same thread form but differ in tolerance grades and allowance conventions.
Choosing the wrong standard creates interchangeability failures at assembly. A thread cut to ISO 965 6g may not mate reliably with a part specified to ASME class 2A, even though both are nominally “metric.” Understanding the differences before machining is not optional for global supply chains.
Specific Tolerance Value Differences Between ISO 965 and ASME B1.13M with Real Examples
The systems use different notation. ISO 965 assigns a tolerance grade (number) and a fundamental deviation (letter), so 6g describes an external thread with grade 6 tolerance and “g” deviation, while 6H describes the mating internal thread. ASME B1.13M uses classes 1A/1B through 3A/3B, where “A” denotes external and “B” internal threads.
The rough equivalencies between the two systems are:
- ISO 6g ≈ ASME 2A (general-purpose external threads)
- ISO 4g ≈ ASME 3A (close-fit precision external threads)
- ISO 8g ≈ ASME 1A (loose-fit or heavily coated external threads)
These are functional approximations — the actual tolerance values differ. For an M10×1.5 external thread, ISO 965 6g specifies a pitch diameter tolerance of 0.180 mm, while the ASME B1.13M class 2A equivalent sits at approximately 0.170 mm, a 10 µm gap that matters in precision thread tolerance CNC applications where stack-up is tight.
Unified threads (UNC/UNF) fall under a separate standard entirely, ASME B1.1, with its own tolerance system that is not interchangeable with either ISO 965 or ASME B1.13M. Engineers specifying parts for global sourcing must state the governing standard explicitly on the drawing, not just the thread call-out. For a comprehensive breakdown of how these standards interact, this engineer’s guide to thread tolerances provides detailed reference tables for both systems.
“Specifying only a thread callout without naming the governing standard is one of the most common drawing errors we see from engineers sourcing globally. ISO 6g and ASME 2A are not the same thing, and treating them as interchangeable creates real assembly failures.” — James Speck, Senior Manufacturing Engineer, American Society of Mechanical Engineers (ASME)
How Spindle Runout and Tool Deflection Cap Your Achievable Thread Tolerance
Machine capability sets a hard floor on what tolerance grades are realistic. A standard CNC lathe with 0.003 mm spindle runout cannot reliably hold a tolerance grade finer than IT5 on pitch diameter without additional process controls, specifically, in-process gauging and thermal compensation. For more information, see Viticulture De Precision En Medoc Guide Complet.
Tool deflection compounds the problem on small-diameter threads. A threading insert cutting an M6 thread at depth generates lateral forces that can shift pitch diameter by 0.005–0.010 mm per pass without rigid tooling and controlled feed rates. At MFG SOLUTION, parts up to 38mm diameter are threaded on Swiss lathes and CNC turning centers equipped with in-process measurement, which keeps pitch diameter variation within the ISO 6g band even on high-volume runs.
For tighter grades, ISO 4h or ASME 3A, thermal stabilization of the machine environment is a prerequisite, not a preference. A 10°C ambient temperature swing can shift a steel spindle bore by 2–3 µm, enough to push a borderline part out of tolerance before the first gauge check.
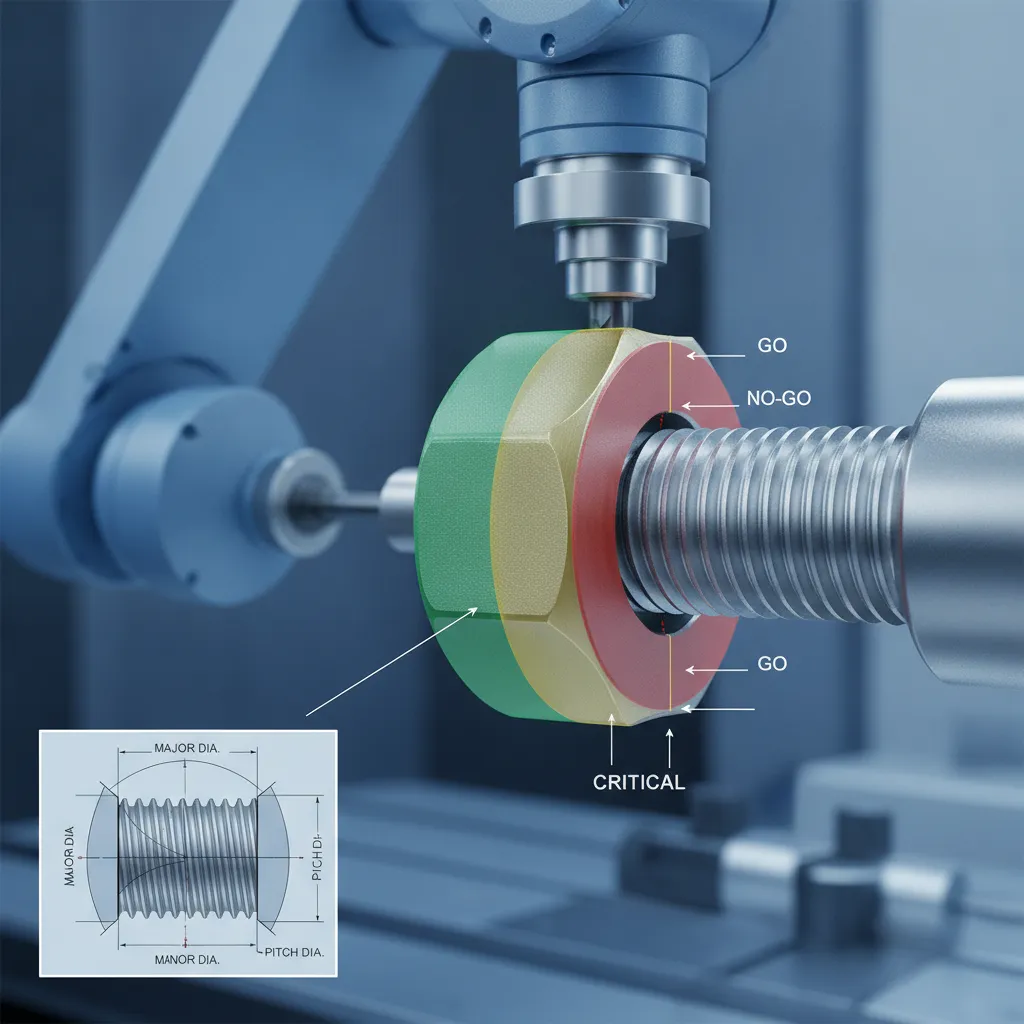
Thread Tolerance Classes Explained: What 6g, 6H, and Other Designations Mean for Mechanical Fit
A thread tolerance class combines two values: a number for the tolerance grade (band size) and a letter for the fundamental deviation (band position relative to nominal).
In the designation 6g, the 6 is the tolerance grade, it controls how wide the allowable size band is. The lowercase g is the fundamental deviation, it shifts the band away from the nominal diameter, creating a small clearance allowance for external threads. 6H is the standard internal thread class: uppercase H indicates zero fundamental deviation, meaning the tolerance band starts exactly at nominal. 6G applies to internal threads that will be plated, the positive allowance compensates for material added during finishing.
Cost-Benefit Tradeoffs Between 6H, 6G, and Close-Fit Classes in Production
The class pairing you specify directly determines mechanical fit. 6H/6g is the standard free-fit combination used across general engineering applications. 5H/4h is a close-fit pairing for precision assemblies where minimal play matters. 7H/8g is a loose-fit pairing suited to high-temperature environments or heavily coated parts where thermal expansion or added material would otherwise bind the joint.
Tightening the class carries a real cost. Moving from 6H to 5H on an M8 internal thread typically increases per-part machining cost by 15–25%, driven by tighter process control, more frequent tool changes, and higher inspection rates. For precision thread tolerance CNC work at volume, that cost compounds quickly across a production run.
How Plating, Coating, and Material Choice Shift Your Tolerance Class Selection
Finishing processes add material, and that material eats into your thread clearance. Zinc plating adds 0.005–0.015 mm per surface; hard anodizing on aluminum adds 0.010–0.025 mm. Specify one tolerance class tighter, 6g instead of 6h on external threads, before coating, so the finished part still fits within the intended class after the process.
Material hardness matters equally. Threading 316 stainless steel demands slower feeds and sharper tooling to hold 6g; the same class on 6061 aluminum machines with far less process stress. MFG SOLUTION’s engineering team, 60+ professionals across CNC turning and Swiss lathe operations, factors both coating allowances and material behavior into thread class selection before a single chip is cut.
How to Select the Right Thread Tolerance for Aerospace, Medical, Automotive, and Hydraulic Applications
Each industry mandates specific thread tolerance classes tied to regulatory standards, choosing the wrong class risks rejection, rework, or field failure.
Industry-Specific Thread Tolerance Requirements: Aerospace, Medical, Automotive, and Hydraulics
Aerospace (AS9100 / NASM 21209): Structural fastener threads require 3A/3B (ASME) or 4h/4H (ISO) close-fit classes. Threads on structural joints must meet MIL-SPEC or NAS standards, and out-of-tolerance threads cannot be reworked in the field. They are scrapped. That zero-tolerance-for-rework rule makes precision thread tolerance CNC verification mandatory before any part ships.
Medical devices (ISO 13485): Bone screw threads typically specify 4H/4h or tighter. Implantable device threads require full lot traceability and CMM-verified pitch diameter records, a Go/No-Go gauge pass alone does not satisfy the documentation requirement. MFG SOLUTION’s ISO 13485:2016 certification covers this traceability chain, with every lot documented and auditable.
Automotive (IATF 16949): M-class threads on powertrain components typically use 6H/6g. High-vibration environments don’t solve loosening by tightening the tolerance class, they specify prevailing-torque thread forms or locking inserts instead. A tighter tolerance on a vibrating joint without a locking mechanism still fails.
Hydraulic fittings: Tapered thread forms (NPT, BSPT) seal through taper interference and surface finish, not tolerance class. Specifying 6g on a parallel thread and expecting a hydraulic seal is a design error. Sealing on parallel threads requires an O-ring or face seal, not a tighter fit band.
Troubleshooting Common Thread Tolerance Failures: Stripping, Loose Fits, and Leakage
| Failure Mode | Root Cause | Fix |
|---|---|---|
| Thread stripping | Pitch diameter at maximum material limit combined with low-strength material | Tighten tolerance to 5H/4h; increase thread engagement length |
| Loose fit / vibration loosening | 7H/8g pairing in dynamic applications, excessive clearance allows micro-movement | Specify 6H/6g and add thread-locking compound |
| Hydraulic leakage on parallel threads | Thread tolerance specified without surface finish control on thread flanks | Add Ra ≤ 1.6 µm surface finish requirement on thread flanks |
The leakage case is the most preventable, surface finish on thread flanks controls micro-leak paths that tolerance class cannot address. Specifying the finish requirement costs nothing at the drawing stage and avoids costly assembly failures downstream.
Thread Inspection Methods: Go/No-Go Gauges, CMM, and Optical Systems for CNC Thread Verification
CNC thread tolerance verification uses three primary methods—Go/No-Go gauging, CMM measurement, and optical scanning—each matched to the tolerance class, part size, and data requirements of the application.
How to Select the Correct Go/No-Go Gauges for Your Thread Class and Standard
A Go gauge checks the maximum material condition (MMC): it must pass fully through the thread. The No-Go gauge checks the minimum material condition: it must not enter more than two full turns. Failure at either condition is a reject—not a rework candidate.
Gauge sets are tolerance-class specific. A 6H gauge set cannot verify a 4H thread; the tolerance bands are different enough that a 4H thread could pass a 6H gauge and still be out of spec. According to NIST calibration standards, gauges must be calibrated regularly and replaced when wear exceeds 10% of the thread tolerance band to maintain measurement integrity.
CMM thread measurement captures actual pitch diameter, lead error, and flank angle—data that Go/No-Go gauges cannot provide. Aerospace and medical lots routinely require Cpk ≥ 1.33 statistical process data to accompany shipment, and CMM is the standard method for generating that record.
Optical measurement—laser scanning or vision systems—is the right choice for threads M2 and below, where contact gauging risks deforming the thread form. Swiss lathe-machined micro-threads are a primary use case; our Swiss lathe machining service applies optical verification as standard on these diameters.
For precision thread tolerance CNC production runs, in-process probing cycles mid-operation catch dimensional drift before a full batch is scrapped. This practice is standard at ISO 9001-certified shops and directly reduces cost-of-quality—see our ISO 9001 Precision Machining guide for how MFG SOLUTION documents this at every production stage. The ASME B1.1 standard for unified screw threads provides the authoritative reference for gauge selection and acceptance criteria across UN thread families.
“In-process gauging is not a luxury for high-volume thread production — it is the only reliable way to catch thermal drift and tool wear before they propagate through an entire batch. Post-process inspection alone is too late.” — Dr. Paul Sheldon, Professor of Manufacturing Engineering, Society of Manufacturing Engineers
Frequently Asked Questions
What is the difference between thread tolerance and thread allowance in CNC machining?
Thread tolerance is the permitted range of variation on a thread dimension; thread allowance is the intentional offset built in before that range begins. Tolerance defines how much a dimension can vary from nominal. Allowance creates deliberate clearance between mating parts, for example, an external thread designated “g” carries a negative allowance that shifts the entire tolerance band away from the nominal pitch diameter, ensuring the bolt never interferes with its nut even at the worst-case tolerance condition.
Can you machine threads to ISO 6H tolerance on a standard CNC lathe, or do you need a Swiss machine?
A well-maintained CNC lathe can hold ISO 6H tolerance on threads larger than roughly 6mm diameter; below that threshold, a Swiss-type lathe becomes the practical choice. Swiss machines support the workpiece directly at the cutting zone, eliminating deflection on small-diameter stock. For parts under 12mm where thread position and pitch diameter must both land within 6H limits, Swiss lathe machining, as used at MFG SOLUTION, consistently outperforms conventional turning in dimensional repeatability.
How does hard anodizing affect thread tolerance on aluminum CNC parts?
Hard anodizing adds 0.001–0.002 in. (0.025–0.051 mm) of coating per surface, which reduces internal thread clearance and can push a borderline 6H fit out of tolerance. Machine internal threads after anodizing when possible, or open the pre-anodize tolerance by the expected coating buildup. External threads on anodized aluminum fasteners typically require a tighter pre-coat pitch diameter to remain within the specified tolerance class after the coating is applied.
What thread tolerance class is required for hydraulic fittings to prevent leakage?
Hydraulic fittings typically require a Class 2B (UN) or ISO 6H internal thread, the medium-fit class, combined with a thread sealant or O-ring face seal design. Thread tolerance alone does not create a pressure-tight seal; the tolerance class controls fit and assembly load, while sealing is achieved through thread compound, PTFE tape, or a dedicated sealing feature. High-pressure systems above 3,000 psi often specify Class 3B to minimize clearance and reduce sealant dependency.
How do you verify that a CNC threading process is statistically capable of holding a specified tolerance class?
Statistical process capability is measured using Cpk, the process capability index. A Cpk of 1.33 or higher is the standard acceptance threshold for aerospace and medical thread production, meaning the process mean sits at least four standard deviations from either tolerance limit. To calculate Cpk, measure pitch diameter on a sample of 30 or more parts, compute the mean and standard deviation, then apply the Cpk formula. CMM data is the preferred input; Go/No-Go gauging alone cannot generate the continuous variable data required for a valid Cpk calculation.



Conclusion
Precision thread tolerance in CNC machining comes down to three decisions: choosing the right tolerance class for the application (6g/6H for general fits, 4h/5H for close fits), selecting the machining process that can physically hold that class at your part diameter, and accounting for post-process changes like anodizing before you finalize the callout on the drawing.
If your parts fall under 38mm in diameter and require documented thread tolerance compliance for medical, automotive, or electronics applications, submit your specifications to MFG SOLUTION, you’ll receive a detailed quote within 8 hours, with production backed by ISO 9001:2015, ISO 13485:2016, and IATF 16949 certification. Start by uploading your thread callout and material spec at mfg-solution.com.
Recommended Articles
Explore more from our content library: