
2026-05-13
Stainless Steel Forging: Strength, Process & Applications

| Key Insight | Explanation |
|---|---|
| Forging improves mechanical properties | The compressive forging process aligns grain flow, boosting tensile strength and fatigue resistance beyond what casting can achieve. |
| Hot forging temperature range | Stainless steel is typically hot-forged between 1,700°F and 2,300°F (927°C–1,260°C) depending on the alloy grade. |
| Grade selection matters | 304 and 316 are the most commonly forged grades; 316 offers superior corrosion resistance in marine and chemical environments. |
| Forged vs. cast stainless steel | Forged parts are denser, stronger, and more reliable under cyclic loads compared to cast stainless steel components. |
| Post-forging machining is standard | Most forged stainless components require CNC machining to achieve final tolerances, surface finish, and dimensional accuracy. |
| Key industries served | Aerospace, medical devices, oil and gas, automotive, and food processing rely heavily on forged stainless steel components. |
Stainless steel forging is the process of shaping stainless steel alloys under high compressive force, typically with heat, to produce parts with superior mechanical properties. The result is a denser, stronger component with aligned grain structure. It matters because forged stainless parts outlast cast or machined-from-bar alternatives in demanding environments.
Few manufacturing decisions carry more long-term consequence than choosing how a critical component is made. In aerospace brackets, medical implants, and chemical processing valves, a forged stainless steel part isn’t just a preference. It’s an engineering requirement. The combination of corrosion resistance and enhanced strength that stainless steel forging delivers is difficult to replicate with any other process.
This article covers everything you need to know: how the forging process works, which grades perform best, the real advantages over casting, the challenges to anticipate, and the best practices that separate quality outcomes from costly failures. Whether you’re a procurement manager sourcing components or an engineer specifying materials, you’ll find practical, actionable guidance here.
What Is Stainless Steel Forging?
Stainless steel forging is a metalworking process where stainless steel billets or bars are heated and shaped using compressive dies or hammers, producing components with refined grain structure and superior mechanical performance compared to casting or machining from stock.
Definition and Core Concept
At its core, forging is about controlled deformation. You heat the metal until it’s workable, then apply force to reshape it. With stainless steel, that workable range is narrower than with carbon steel, which is part of what makes the process technically demanding.
According to the Steel Forging Association, the forging process improves both the strength and corrosion resistance of stainless steel, enabling forged grades to outlast and withstand harsher environments than their cast counterparts [1]. This isn’t just a marginal improvement. The grain refinement that occurs during forging fundamentally changes how the material responds to stress, temperature, and corrosive media.
Stainless steel itself is defined by its chromium content, typically 10.5% or higher, which forms a passive oxide layer on the surface and provides corrosion resistance. The most commonly forged grades include:
- 304 stainless steel: The workhorse grade. Excellent corrosion resistance, good formability, widely available.
- 316 stainless steel: Adds molybdenum for superior resistance to chlorides and acidic environments. Preferred for marine and chemical applications.
- 410 stainless steel: A martensitic grade that can be heat-treated for high hardness. Used in valves and fasteners.
- 17-4 PH stainless steel: A precipitation-hardening grade offering very high strength with good corrosion resistance. Common in aerospace.
Why It Matters in Modern Manufacturing
As of 2026, demand for forged stainless components continues to grow across medical devices, energy infrastructure, and automotive electrification. The Nickel Institute has published technical guidance on forging austenitic stainless steels, noting their suitability for cryogenic, high-temperature, and corrosive service conditions [2].
Understanding this strategy isn’t just academic. It directly affects part reliability, supply chain decisions, and total cost of ownership for anyone specifying or sourcing precision components.
How Stainless Steel Forging Works
this approach works by heating a billet to a specific temperature range, then applying compressive force through dies or hammers to shape it, refine its grain structure, and eliminate internal voids.
The Forging Process Step by Step
- Material selection: Choose the appropriate stainless grade based on the service environment, required mechanical properties, and post-forging machinability needs.
- Billet preparation: Cut stock to the correct weight and volume for the finished part, accounting for flash and trimming losses.
- Heating: Heat the billet to the forging temperature. According to GL Forge’s technical guide, stainless steel is hot-forged between 1,700°F and 2,300°F (927°C–1,260°C) depending on the grade [3].
- Die forging or open-die forging: Place the heated billet in the press or hammer and apply force. Closed-die (impression-die) forging produces near-net shapes; open-die forging is used for larger, simpler geometries.
- Trimming: Remove flash (excess material squeezed out between die halves) using trim dies.
- Heat treatment: Anneal or solution treat to relieve residual stresses and restore corrosion resistance, especially for austenitic grades that may sensitize during forging.
- Inspection: Conduct dimensional checks, non-destructive testing (NDT), and mechanical property verification per applicable standards.
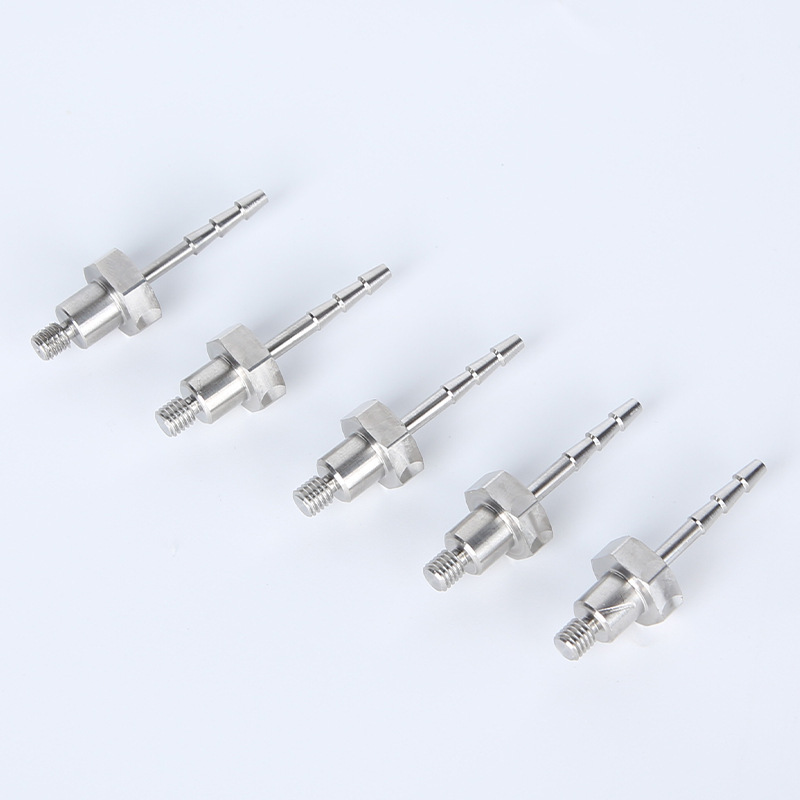
- CNC machining: Finish the forging to final dimensions and surface finish using CNC turning, milling, or Swiss lathe operations.
Forging Methods Compared
The ASM International Handbook on Bulk Forming describes several forging methods applicable to stainless steels, including open-die, closed-die, and rolled-ring forging [4]. Each suits different part geometries and production volumes.
Rolled-ring forging, for example, is ideal for flanges, rings, and bearing races. Open-die forging handles large, custom shapes. Closed-die forging is the standard for high-volume, near-net-shape production of smaller components.
Pro Tip: Keep stainless steel within its forging temperature window. Working it too cool increases the risk of cracking; working it too hot risks grain growth that weakens the final part. Use calibrated furnaces and monitor soak times carefully for each grade.
One limitation worth noting: stainless steel’s low thermal conductivity means it heats and cools unevenly compared to carbon steel. Thick sections require longer soak times to achieve uniform temperature throughout the billet before forging begins.
Key Benefits of Stainless Steel Forging
this delivers superior tensile strength, fatigue resistance, and corrosion performance compared to cast or machined-from-bar alternatives, making it the preferred manufacturing method for safety-critical components.
Mechanical and Structural Advantages
The most significant benefit is grain flow control. When stainless steel is forged, the grain structure aligns with the part’s contour rather than being cut through (as in machining from bar stock). This produces what engineers call “favorable grain flow,” which directly improves:
- Tensile strength: Forged stainless steel consistently achieves higher ultimate tensile strength than cast equivalents.
- Fatigue resistance: Aligned grain flow resists crack initiation and propagation under cyclic loading.
- Impact toughness: The refined, dense microstructure absorbs energy more effectively, critical in aerospace and automotive crash-safety applications.
- Corrosion resistance: Forging eliminates the porosity and inclusions common in castings, removing pathways for corrosive media to penetrate the material.
Research published in PMC (National Institutes of Health) on 316L stainless steel confirms that hot forging transforms columnar grain morphology into equiaxed grains, significantly increasing both yield strength and ultimate tensile strength [5]. This is particularly relevant for medical implant and surgical instrument applications.
Trenton Forging notes that the continuous grain flow created during forging improves mechanical properties throughout the component, not just at the surface [6]. That’s a critical distinction from surface hardening or coating processes.
Economic and Application Benefits
Beyond raw performance, it offers practical economic advantages:
- Longer service life: Stronger, denser parts fail less often, reducing replacement and downtime costs.
- Near-net-shape production: Closed-die forging minimizes material waste compared to machining from solid bar.
- Consistent quality at volume: Once dies are qualified, forging produces highly repeatable parts batch after batch.
- Reduced post-processing: Forged parts often require less machining than castings because they’re closer to final geometry and have no porosity to address.
Industry analysts suggest that for high-volume production runs of critical components, the per-part cost of forging is often lower than machining from solid bar once tooling costs are amortized. Results will vary depending on part complexity, volume, and material grade.
Forged vs. Cast Stainless Steel: A Direct Comparison
Forged stainless steel is stronger, denser, and more fatigue-resistant than cast stainless steel; cast parts are better suited to complex geometries that would be impractical to forge.
Side-by-Side Performance Data
| Property | Forged Stainless Steel | Cast Stainless Steel |
|---|---|---|
| Tensile Strength | Higher (aligned grain flow) | Lower (random grain structure) |
| Fatigue Resistance | Excellent | Moderate |
| Porosity | Minimal to none | Common without HIP treatment |
| Corrosion Resistance | Superior (no inclusions/voids) | Good but can be compromised by porosity |
| Geometric Complexity | Limited by die design | Highly complex shapes possible |
| Tooling Cost | Higher upfront (dies) | Lower upfront (molds) |
| Best For | High-stress, safety-critical parts | Complex, lower-stress components |
According to Titan Fittings, forging enhances both strength and ductility through compressive deformation, while casting’s random solidification can introduce internal defects that reduce mechanical performance under load [7].
When to Choose Forging Over Casting
Choose forging when:
- The part will experience cyclic or impact loading
- Corrosion resistance must be consistent through the cross-section
- The application is safety-critical (medical, aerospace, pressure vessels)
- Production volume justifies die costs
Choose casting when the geometry is too complex for practical die design, or when production volumes are too low to amortize forging tooling. In practice, many finished components combine both: a forged blank that’s subsequently CNC-machined to final tolerances.
Common Challenges in Stainless Steel Forging for 2026
this method presents specific challenges including narrow working temperature windows, rapid die wear, sensitization risk, and demanding post-forging heat treatment requirements that don’t apply to carbon steel.
Material and Process Challenges
Stainless steel is significantly harder to forge than low-carbon steel. The work-hardening rate of austenitic grades like 304 and 316 is high, meaning the material resists deformation and can crack if worked outside its temperature window. As contributors on I Forge Iron note, stainless steel requires forging at a near-white heat and demands much greater impact force for metal movement compared to mild steel [8].
Common challenges include:
- Sensitization: Heating austenitic stainless steels in the 800°F–1,500°F (427°C–816°C) range causes chromium carbide precipitation at grain boundaries, reducing corrosion resistance. Proper solution annealing after forging is essential.
- Die wear: The high strength and abrasiveness of stainless steel accelerates die wear significantly compared to forging carbon steel. Die material selection and lubrication are critical.
- Toxic byproducts: Grinding and finishing stainless forgings generates chromium oxide particles. Proper ventilation, PPE, and waste handling are required per OSHA and EPA guidelines.
- Scale formation: Stainless steel forms tenacious oxide scale during heating that must be removed before die contact to prevent surface defects.
- Thermal conductivity: Low thermal conductivity means large billets heat unevenly, requiring careful furnace management to avoid hot and cold spots.
Common Mistakes to Avoid
A common mistake is forging stainless steel at temperatures appropriate for carbon steel. This produces surface cracking and internal stress concentrations. Another pitfall is skipping post-forging annealing on austenitic grades, leaving the part sensitized and vulnerable to intergranular corrosion in service.
Pro Tip: Always specify solution annealing after forging austenitic stainless grades (304, 316). Heat to 1,900°F–2,050°F (1,040°C–1,120°C) and water quench. This dissolves chromium carbides and restores full corrosion resistance. Skipping this step is one of the most costly mistakes in stainless forging.
From experience working with precision component suppliers, one pitfall that consistently causes problems is inadequate die lubrication. Stainless steel’s tendency to gall (cold-weld to tooling surfaces) makes proper glass-based or graphite lubricants non-negotiable for hot forging operations.
Best Practices and Expert Tips for 2026
Best practices for this strategy in 2026 center on precise temperature control, grade-specific die design, mandatory post-forging heat treatment, and integrating CNC machining for final dimensional accuracy.
Process Optimization Guidelines
Industry analysts consistently highlight temperature management as the single most important variable in this approach quality. Scot Forge, one of the established names in open-die and rolled-ring forging, produces stainless components for acidic, high-temperature, and cryogenic environments, underscoring the breadth of applications where process discipline matters [9].
Key best practices include:
- Grade matching: Select the grade based on service environment, not just availability. 316L (low-carbon variant) is preferred for welded assemblies; 17-4 PH suits high-strength aerospace applications.
- Controlled heating: Use calibrated induction or gas furnaces. Monitor billet temperature with contact pyrometers or thermal cameras before each forging stroke.
- Die design for stainless: Use larger draft angles and more generous radii than you’d use for carbon steel. This reduces die stress and the risk of cold shuts (surface folding defects).
- Lubrication selection: Use glass-based lubricants for temperatures above 2,000°F; graphite-in-water emulsions work well at lower forging temperatures.
- Post-forging inspection: Apply dye penetrant testing (DPT) or fluorescent penetrant inspection (FPI) to detect surface-breaking defects before machining.
- CNC finish machining: Most stainless forgings require precision machining to achieve final tolerances. Swiss lathe and CNC turning operations are standard for small-diameter forged components.
Quality Standards and Certifications
As of 2026, quality management for forged stainless components is governed by several key frameworks:
- ISO 9001:2015: General quality management system standard covering process control and traceability.
- ISO 13485:2016: Medical device quality management, required when forged components go into surgical instruments or implants.
- IATF 16949: Automotive quality standard, mandating zero-defect processes and full supply chain traceability.
- ASTM A668 / A181: Specifications for carbon and alloy steel forgings for general industrial use, often referenced alongside stainless-specific requirements.
At MFG SOLUTION, we’ve found that customers sourcing forged stainless components for medical and automotive applications consistently prioritize suppliers who hold ISO 13485 and IATF 16949 certifications. These aren’t just credentials. They represent documented process control, where every step is tracked, auditable, and verifiable.
Pro Tip: When qualifying a stainless steel forging supplier, request first article inspection (FAI) reports and material certifications (mill certs) for every heat lot. These documents confirm the material meets specified chemistry and mechanical property requirements before you commit to a production run.
Our team at MFG SOLUTION recommends pairing cold forging or precision CNC machining with forged blanks for small stainless components under 38mm diameter. This combination delivers the structural benefits of forging with the dimensional precision that medical and automotive customers require, all within a 3-day ship window for qualified parts.
Sources & References
- Steel Forging Association, “Stainless Steel Forging,” 2024
- Nickel Institute, “Forgings: Stainless Steel Technical Guide,” 2023
- GL Forge, “Guide to Stainless Steel Forgings: 304 and 316 SS Forging,” 2024
- ASM International, “Forging of Stainless Steels,” Metalworking: Bulk Forming Handbook
- PMC/NIH, “Laser Powder Bed Fusion and Hot Forging of 316L Stainless Steel,” 2025
- Trenton Forging, “Stainless Steel Forging: Benefits,” 2024
- Titan Fittings, “Forged vs Cast Stainless Steel: Understanding the Differences,” 2024
- I Forge Iron, “Forging Stainless Steel: Experts Please,” Community Discussion
- Scot Forge, “Stainless Steel Forgings,” 2024
Frequently Asked Questions
1. What is stainless steel forging and how does it differ from casting?
this uses compressive force to shape heated stainless steel billets, producing parts with aligned grain flow and superior mechanical properties. Casting pours molten metal into molds, which can introduce porosity and random grain structure. Forged parts are stronger and more fatigue-resistant; cast parts handle more complex geometries. For safety-critical applications, forging is almost always the preferred method.
2. What temperature is stainless steel forged at?
Stainless steel is hot-forged between 1,700°F and 2,300°F (927°C–1,260°C) depending on the specific grade. Austenitic grades like 304 and 316 are typically forged in the upper portion of this range. Working below the minimum temperature risks cracking; working above the maximum causes grain growth that weakens the finished part. Precise temperature control is non-negotiable for quality stainless forgings.
3. Which stainless steel grades are best for forging?
304 and 316 are the most commonly forged stainless grades due to their good ductility and wide availability. 316L (low-carbon) is preferred for welded or corrosive-environment applications. 17-4 PH is used where very high strength is needed, particularly in aerospace. Martensitic grades like 410 are forgeable but require careful heat treatment to achieve target hardness without cracking.
4. Does stainless steel forging require post-forging heat treatment?
Yes, in most cases. Austenitic stainless grades (304, 316) should be solution annealed after forging to dissolve chromium carbides that form during the forging cycle. This restores full corrosion resistance. Precipitation-hardening grades like 17-4 PH require age hardening. Skipping post-forging heat treatment is one of the most common and costly errors in stainless forging production.
5. What industries use forged stainless steel components?
Forged stainless steel components are used across aerospace (structural brackets, engine components), medical devices (surgical instruments, implant hardware), oil and gas (valves, flanges, pump shafts), automotive (exhaust and drivetrain components), food processing (hygienic fittings), and marine applications. Any industry requiring a combination of high strength, corrosion resistance, and long service life is a natural fit for it.
6. How does CNC machining relate to stainless steel forging?
Most this methods require CNC machining after forging to achieve final dimensional tolerances, surface finish, and feature details that dies cannot produce. CNC turning, Swiss lathe operations, and mill-turn processes are standard post-forging steps. The forging provides the structural integrity; CNC machining delivers the precision. For small components under 38mm diameter, this combination is particularly cost-effective for high-volume production.
7. Is stainless steel forging more expensive than machining from bar stock?
It depends on volume and part geometry. Forging involves upfront die costs that can be significant. For low volumes, machining from bar stock is often more economical. At higher volumes, forging reduces material waste and machining time, lowering per-part cost. For safety-critical parts where mechanical properties matter, the performance advantages of forging often justify the cost premium regardless of volume. Results vary by application.
8. What quality certifications should a stainless steel forging supplier hold?
For general industrial use, ISO 9001:2015 is the baseline. Medical device applications require ISO 13485:2016. Automotive supply chains demand IATF 16949. Aerospace applications typically require AS9100D. Always request material certifications (mill certs), first article inspection (FAI) reports, and non-destructive testing records from any forging supplier, regardless of their certification status.
this strategy remains one of the most reliable manufacturing processes for producing high-strength, corrosion-resistant components in demanding service environments. The process demands technical discipline, from precise temperature management to mandatory post-forging heat treatment, but the performance payoff is substantial. Forged stainless parts simply outlast and outperform alternatives in the applications that matter most.
For procurement managers and engineers sourcing small precision stainless components, the practical path forward often combines forged blanks with precision CNC machining. That’s exactly where MFG SOLUTION operates. With ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, 60+ engineering professionals, and a 3-day ship window backed by an 8-hour quote turnaround, we deliver the this approach and precision machining capability your supply chain needs without the lead times that slow your program down. Submit your specifications and get a quote within 8 hours.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: