
2026-05-11
Quick Turn Machining: A Complete How-To Guide

| Key Insight | Explanation |
|---|---|
| Speed is the core value | Quick turn machining compresses lead times from weeks to days, letting teams respond faster to product launches and supply disruptions. |
| File readiness determines turnaround | Submitting complete, toleranced drawings in accepted formats (STEP, DXF, PDF) is the single biggest factor in how fast your quote and production begin. |
| Process selection affects cost and speed | Choosing CNC turning, Swiss lathe, or automatic lathe based on part geometry directly impacts per-unit cost and how quickly a batch can ship. |
| Certifications matter for regulated industries | Medical, automotive, and aerospace buyers must verify ISO 9001:2015, ISO 13485:2016, or IATF 16949 compliance before approving a supplier. |
| Tolerance defines process choice | Parts requiring ±0.005mm or tighter typically need Swiss lathe or 5-axis CNC mill-turn operations rather than standard CNC turning. |
| Batch size shapes economics | Small prototype runs (1–50 pieces) and production batches (500–10,000 pieces) have different optimal processes and pricing structures. |
You need 500 small stainless steel connectors machined to ±0.01mm tolerance. Your current supplier quoted four weeks. Your product launch is in ten days. This is exactly the scenario where quick turn machining becomes essential. Quick turn machining refers to an expedited precision manufacturing workflow in which CNC-machined parts are quoted, produced, and shipped within days rather than weeks. For electronics manufacturers, automotive Tier-1 suppliers, and medical device teams, this capability isn’t a luxury. It’s a supply chain requirement.
This guide walks you through every stage of the process: from preparing your design files to validating finished parts on your floor. You’ll learn which machining processes suit different geometries, what certifications to verify, and how to avoid the most common mistakes that slow down fast-turn orders. Estimated time to work through this guide: 20 minutes. Difficulty level: intermediate (some familiarity with engineering drawings is helpful).
What Is Quick Turn Machining?
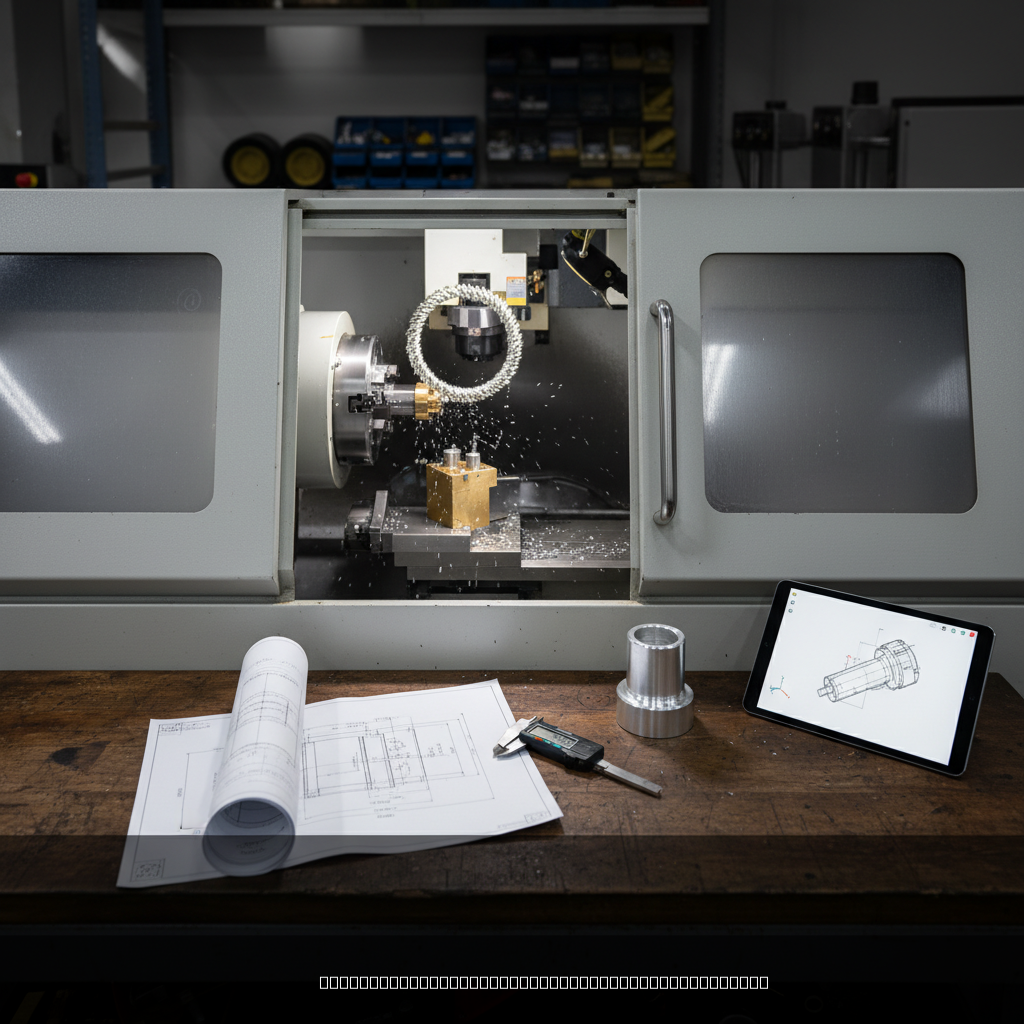
Quick turn machining is a precision manufacturing approach that prioritizes speed at every stage, from quoting through shipping, without sacrificing dimensional accuracy or material integrity. Standard job shop lead times in the industry range from two to six weeks. Quick turn machining compresses that window to as little as one to three days for straightforward parts, and five to seven days for more complex geometries.
How It Differs from Standard CNC Machining
The underlying cutting processes are identical. What changes is everything around the cutting: how fast a quote is generated, how quickly materials are staged, and how production is scheduled. Quick turn suppliers maintain in-stock material inventories, dedicate machine capacity for expedited orders, and use streamlined digital quoting systems rather than manual RFQ workflows.
According to industry analysts, the shift toward digital quoting platforms has cut average quote response times from 48–72 hours down to under 8 hours for standard part geometries as of 2026 [1]. That compression at the front end is what makes the rest of the timeline possible.
Who Uses Quick Turn Machining?
The users are typically engineers and procurement managers under deadline pressure. Common scenarios include:
- New product launches requiring rapid prototype iterations before tooling is committed
- Supply chain disruptions forcing emergency sourcing from an alternative vendor
- ISO certification audits that reveal a quality gap requiring immediate replacement parts
- Competitive pressure to accelerate time-to-market on a new device or component
- Bridge production runs while long-lead tooling or casting dies are being made
The Southwest Research Institute (SwRI) notes that quick-turnaround precision machining is particularly valuable for prototype fabrication where design iterations are frequent and waiting weeks for each revision is cost-prohibitive [2].
| Attribute | Standard CNC Machining | Quick Turn Machining |
|---|---|---|
| Typical lead time | 2–6 weeks | 1–7 days |
| Quote turnaround | 2–5 business days | Under 8 hours |
| Material staging | Ordered per job | Pre-stocked inventory |
| Scheduling | Standard queue | Dedicated expedited capacity |
| Premium cost | Base rate | 10–30% above base (varies) |
What You’ll Need Before You Start
Before submitting a quick turn machining order, you need four things ready: complete design files, defined tolerances, material specification, and a supplier with verified capacity and certifications.
Technical Prerequisites
Incomplete documentation is the number-one cause of delays in quick turn orders. Have these ready before you contact any supplier:
- 3D CAD files in STEP (.stp) or IGES format for solid geometry
- 2D engineering drawings (PDF or DXF) with all tolerances, surface finish callouts, and GD&T (geometric dimensioning and tolerancing) annotations
- Material specification including alloy grade (e.g., 303 stainless, 6061-T6 aluminum, C360 brass)
- Quantity broken down by prototype and production run if applicable
- Surface finish requirements (Ra value in micrometers or microinches)
- Thread callouts for any tapped or turned threads, including standard (e.g., M6×1.0 or 1/4-20 UNC)
Supplier Qualification Checklist
Not every machine shop can deliver true quick turn machining. Verify these supplier attributes before committing:
- ISO 9001:2015 certification for general quality management
- ISO 13485:2016 if parts go into medical devices
- IATF 16949 if parts are used in automotive applications
- Stated quote turnaround time (8 hours or less is achievable with modern systems)
- Documented ship window (3 days is the benchmark for truly expedited service)
- Equipment capable of your required tolerances (5-axis CNC for complex geometries, Swiss lathe for long slender parts)
Pro Tip: Always request a sample inspection report or first-article inspection (FAI) documentation from a prospective quick turn supplier before placing a production order. This confirms they have measurement capability (CMM or optical comparator) that matches your tolerance requirements.
Step 1: Prepare Your Design Files
Preparing complete, clean design files is the most time-sensitive step you control. Errors or omissions here cause rework requests that can add 24–48 hours to any this approach timeline.
How to Create Production-Ready Files
- Export your 3D model as a STEP file from your CAD software (SolidWorks, Fusion 360, CATIA, or equivalent). Verify the file opens cleanly without missing faces or geometry errors.
- Generate a 2D drawing with at minimum: part dimensions, critical tolerances (ISO 2768 fine or custom GD&T callouts), surface finish (Ra), and material specification in the title block.
- Mark critical features explicitly. Don’t rely on the machinist to infer which dimensions are functional. Use a feature control frame or a separate notes section.
- Specify thread standards clearly. State whether threads are metric (ISO) or unified (UNC/UNF), and include class of fit (e.g., 6H for metric internal threads).
- Include a revision number on every drawing. This prevents the supplier from machining an outdated version if you’ve iterated the design.
In practice, the most common file issue we see is missing tolerance callouts on bore diameters and shaft fits. A drawing that says “Ø8mm” without a tolerance forces the machinist to apply a general tolerance, which may not match your assembly requirements.
Pro Tip: Use ISO 2768-m (medium) as a general tolerance standard for non-critical features, and call out tighter tolerances only where functionally required. This reduces machining cost and speeds up production without compromising part performance.
Step 2: Select the Right Machining Process
Selecting the correct machining process for your part geometry and volume is the single biggest lever on both cost and turnaround time in this.
Matching Process to Part Geometry
Different processes have different setup times, cycle times, and cost profiles. Here’s a practical breakdown:
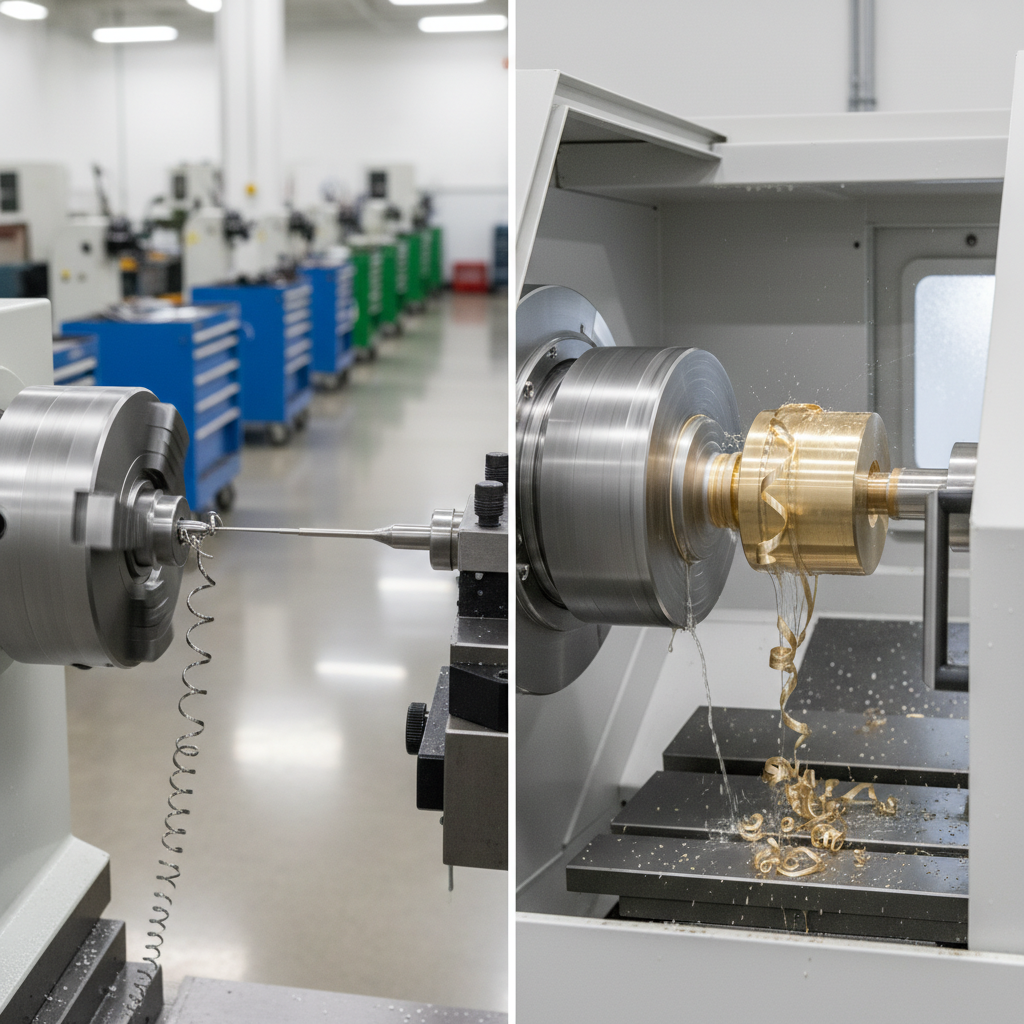
- CNC Turning: Best for cylindrical or rotationally symmetric parts. Fast cycle times, low per-unit cost at medium to high volumes. Suitable for shafts, bushings, connectors, and fittings up to 38mm diameter.
- Swiss Lathe (Swiss Screw Machining): Optimal for long, slender parts (high length-to-diameter ratio) requiring tight tolerances. The guide bushing supports the workpiece close to the cutting tool, minimizing deflection. Common in medical device pins, dental components, and miniature fasteners.
- CNC Mill & Turn: Used when a part has both rotational and prismatic features (e.g., a shaft with a milled flat or cross-hole). Eliminates secondary operations by combining turning and milling in one setup.
- Automatic Lathe: High-volume production of simple turned parts. Very low cycle times once set up. Economical for runs of 1,000 pieces or more.
- Cold Forging (Cold Heading): Near-net-shape forming for high-volume fasteners and small structural components. Reduces material waste and machining time significantly compared to cutting from bar stock.
According to OGB CNC’s analysis of quick turn CNC machining selection criteria, matching the process to the part’s geometric complexity is the primary decision variable, followed by batch size and tolerance requirements [1].
Process Selection by Volume and Tolerance
| Process | Best For | Typical Tolerance | Volume Sweet Spot |
|---|---|---|---|
| CNC Turning | Cylindrical parts, shafts, bushings | ±0.01–0.05mm | 10–10,000 pcs |
| Swiss Lathe | Slender, high-precision parts | ±0.003–0.01mm | 50–50,000 pcs |
| CNC Mill & Turn | Complex multi-feature parts | ±0.005–0.02mm | 5–5,000 pcs |
| Automatic Lathe | Simple turned parts, high volume | ±0.02–0.05mm | 1,000–100,000 pcs |
| Cold Forging | Fasteners, structural small parts | ±0.05–0.1mm (pre-finish) | 10,000+ pcs |
Step 3: Submit Your RFQ and Review the Quote
Submitting a well-structured request for quotation (RFQ) directly determines how quickly you receive a usable quote and how accurately it reflects your actual requirements.
What to Include in Your RFQ
- Attach all files prepared in Step 1: STEP file, 2D drawing PDF, and any reference documents (material data sheets, applicable standards).
- State your required ship date explicitly. Don’t say “as soon as possible.” Give a specific date. This lets the supplier confirm feasibility rather than assume.
- Specify quantity tiers if you want pricing for both a prototype run and a production run. Many buyers get quotes for 10, 100, and 1,000 pieces simultaneously.
- List any post-machining operations you need: anodizing, passivation, plating, heat treatment, or assembly. These add lead time and must be quoted separately.
- State your quality documentation requirements: certificate of conformance (CoC), first-article inspection (FAI) report, material certification (mill cert), or PPAP (Production Part Approval Process) for automotive buyers.
How to Evaluate the Quote
A credible it quote should include unit price, setup charge (if applicable), lead time from approval, and any notes about design for manufacturability (DFM). If the quote comes back with DFM flags, pay attention. These are usually legitimate concerns that will affect part quality if ignored.
At MFG SOLUTION, we’ve found that buyers who respond to DFM feedback within two hours of receiving a quote consistently see their parts ship on the fastest possible timeline. Delays in DFM approval are the second most common cause of missed ship dates, after incomplete initial files.
Step 4: Approve Production and Monitor Quality
Approving production and maintaining quality oversight during a this method run requires clear communication upfront and defined inspection checkpoints.
What Happens During Production
Once you approve the quote, the supplier stages material, programs the CNC equipment, and begins machining. In a certified facility, quality control runs in parallel with production, not after it. This is what ISO 9001:2015 “full process control” actually means: every step is tracked, documented, and auditable for compliance.
Key quality events during production include:
- First-off inspection: The first part machined is measured against the drawing before the batch continues. Deviations are corrected at the program level before full production runs.
- In-process inspection: Periodic dimensional checks during the run, typically every 50–100 pieces depending on batch size and tolerance criticality.
- Final inspection: Full dimensional verification against the drawing for a statistically representative sample, per AQL (Acceptable Quality Level) sampling plans.
Certifications to Verify
For regulated industries, confirm that your supplier’s certifications are current as of 2026. ISO certifications are audited annually and must be renewed on a three-year cycle. Request the certificate with the expiration date visible. Relevant standards include:
- ISO 9001:2015 for general quality management systems
- ISO 13485:2016 for medical device component manufacturing
- IATF 16949 for automotive supply chain quality
The Lighthouse for the Blind’s precision machining division notes that quick-turn capability is most effective when paired with rigorous in-process quality checks rather than relying solely on final inspection [3].
Pro Tip: For your first order with a new quick turn supplier, request a first-article inspection (FAI) report with actual measured values (not just pass/fail) for all critical dimensions. This gives you a baseline to compare against future batches and confirms their measurement capability.
Step 5: Receive, Inspect, and Validate Parts
Receiving and validating incoming this strategy parts correctly protects your assembly line and your quality records, especially in regulated industries.
Incoming Inspection Protocol
- Check packaging integrity before opening. Damage in transit can affect part dimensions, especially for tight-tolerance components.
- Verify quantity against packing list. Count the parts and confirm the lot number matches the documentation.
- Review all quality documents included with the shipment: certificate of conformance, material certifications, and FAI report if requested.
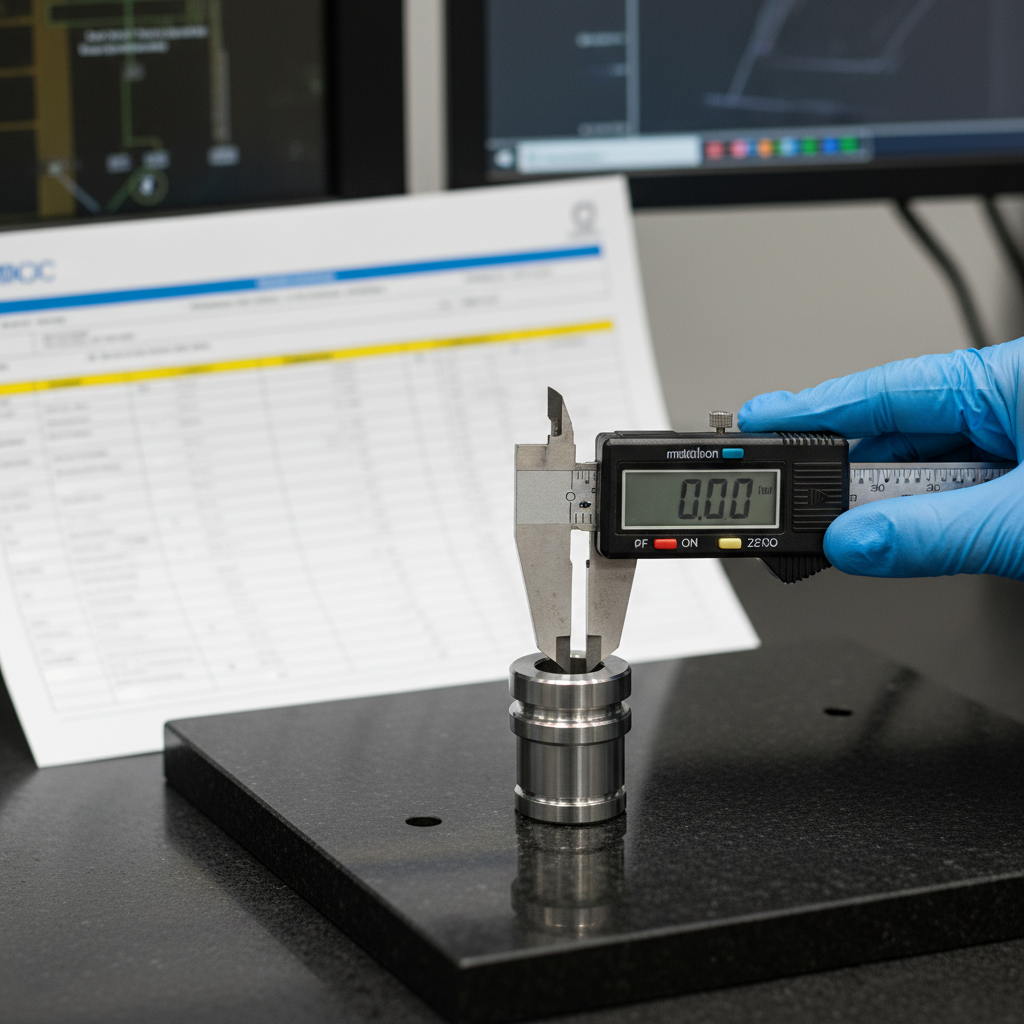
- Perform incoming dimensional inspection on a sample per your internal AQL plan. For critical parts, a 100% inspection may be warranted on first orders.
- Record results in your quality management system and link them to the supplier’s lot number. This traceability is required for ISO 13485 and IATF 16949 compliance.
What to Do If Parts Are Out of Specification
Nonconforming parts happen, even with certified suppliers. The correct response is to quarantine the parts, issue a nonconformance report (NCR) with specific dimensional data, and contact the supplier immediately with photos and measurement records. A competent this approach partner will respond with a corrective action report (CAR) and replacement parts on an expedited timeline.
From experience, most nonconformances in quick turn orders trace back to an ambiguous tolerance callout on the drawing rather than a machining error. This reinforces the importance of Step 1.
Quick Turn Machining Best Practices for 2026
As of 2026, the most effective this programs share a set of practices that consistently reduce lead times and improve first-pass quality rates.
Design for Manufacturability (DFM) Principles
DFM (design for manufacturability) is the practice of designing parts with the manufacturing process in mind, reducing setup complexity and machining time. Key DFM principles for it include:
- Avoid unnecessarily tight tolerances on non-functional features. Every tighter-than-standard tolerance adds inspection time and cost.
- Design internal corner radii to match standard end mill sizes (e.g., R0.5, R1.0, R2.0mm). Non-standard radii require special tooling that adds lead time.
- Minimize the number of setups required. Parts that can be machined complete in one chucking are faster and cheaper than those requiring multiple fixture changes.
- Use standard thread sizes and pitches wherever possible. Non-standard threads require special taps or thread mills that may not be in stock.
- Specify surface finish only as tight as functionally required. An Ra 0.8µm finish takes significantly longer to achieve than Ra 3.2µm.
Supplier Relationship Practices
Our team at MFG SOLUTION recommends establishing a preferred supplier relationship rather than spot-quoting every order. Suppliers who know your part families, materials, and quality requirements can quote faster and machine more accurately because they’ve built institutional knowledge of your specifications.
Parts Badger’s expedited manufacturing guidelines also emphasize that pre-approved part libraries and standing material agreements are the most reliable way to sustain consistent this method performance across multiple order cycles [4].
Common Mistakes to Avoid
Most delays and quality failures in this strategy are preventable. These are the pitfalls that consistently cause problems, drawn from hands-on experience across hundreds of expedited orders.
File and Documentation Errors
- Submitting 3D files without 2D drawings. A STEP file alone doesn’t communicate tolerances, surface finish, or thread specifications. Always include a fully annotated 2D drawing.
- Using outdated drawing revisions. A common mistake is submitting a revised STEP file but forgetting to update the 2D drawing. The machinist follows the 2D drawing. Mismatches cause scrapped parts.
- Leaving tolerance callouts to general standards without flagging exceptions. If one bore is critical and others aren’t, mark it. Don’t expect the machinist to identify which features matter most.
- Not specifying material grade. “Stainless steel” is not a specification. 303, 304, 316, and 17-4 PH stainless all machine differently and have different corrosion and strength properties.
Process and Scheduling Mistakes
- Requesting quick turn machining for parts that need long-lead finishing operations. If your part requires hard chrome plating or black oxide coating from a third-party finisher, the machining lead time is irrelevant. Plan the full supply chain, not just the machining step.
- Approving production without reviewing DFM feedback. One pitfall to watch for: suppliers flag a potential issue, the buyer approves anyway to save time, and the parts arrive nonconforming. DFM feedback exists to protect your timeline, not slow it down.
- Underestimating first-order setup time. A new part on a new supplier’s machines always takes longer than a repeat order. Budget for a slightly longer lead time on first articles and use that run to validate the process.
- Not confirming shipping method. Quick turn machining gets parts ready in three days, but standard ground freight adds another five. Confirm express shipping is included or budgeted if your deadline is tight.
Sources and References
- OGB CNC, “How to Choose Quick Turn CNC Machining for Your Manufacturing Needs,” 2026
- Southwest Research Institute (SwRI), “Precision Machining & Prototype Fabrication,” 2026
- The Lighthouse for the Blind, Inc., “Precision Machining,” 2026
- Parts Badger, “Quick Turn CNC Machining | Expedited Manufacturing,” 2026
- Quick Turn Machining LLC (QTM), “Manufacturing Machined Parts,” 2026
Frequently Asked Questions
1. What is quick turn machining and how fast is it?
this approach is an expedited CNC manufacturing service that compresses the full production cycle from quote to shipment into days rather than weeks. Depending on part complexity and supplier capacity, lead times range from one to seven business days. Quote turnaround at capable facilities is under 8 hours from the time a complete file package is submitted.
2. How much does quick turn machining cost compared to standard lead times?
Expedited machining typically carries a premium of 10–30% over standard pricing, depending on how aggressively the lead time is compressed and how much dedicated machine capacity the supplier must allocate. For production volumes (500+ pieces), the per-unit premium is smaller because setup cost is amortized. Results vary by supplier, material, and complexity.
3. What file formats do I need to submit for a quick turn machining order?
Most this suppliers accept STEP (.stp) or IGES files for 3D geometry, and PDF or DXF for 2D engineering drawings. Always submit both. The 3D file defines the geometry; the 2D drawing communicates tolerances, surface finish, threads, and material. Submitting only one of the two is the most common cause of quoting delays.
4. Which materials are best suited for quick turn machining?
Aluminum (6061-T6, 7075), brass (C360), and stainless steel (303, 304) are the fastest-machinable materials and are almost always in stock at quick turn facilities. Titanium, Inconel, and hardened steels are machinable but require more tool changes and slower feeds, which adds time. Material availability in your supplier’s inventory is a key factor in actual lead time.
5. Can quick turn machining meet medical and automotive quality standards?
Yes, provided the supplier holds the relevant certifications. For medical device components, look for ISO 13485:2016 certification. For automotive parts, IATF 16949 is the required standard. ISO 9001:2015 covers general quality management for all other industries. Always request a current certificate with visible expiration date before placing a regulated-industry order.
6. What is the maximum part size for quick turn machining?
This depends on the supplier’s equipment. Many quick turn specialists focus on small parts (under 38mm diameter) because they can be produced on automatic lathes and Swiss lathe equipment at high speed and low cost. Larger parts typically require machining centers with longer setup times, which reduces the speed advantage of quick turn services.
7. How do I find a reliable quick turn machining supplier?
Verify certifications (ISO 9001, ISO 13485, or IATF 16949 as applicable), confirm stated quote and ship windows are contractually backed, and request references or sample inspection reports from previous orders. A supplier who can provide a detailed quote within 8 hours of receiving your files has demonstrated the organizational capability that it actually requires.
8. What tolerances can quick turn machining achieve?
Standard this method on CNC turning centers achieves ±0.01–0.05mm on most features. Swiss lathe operations can hold ±0.003–0.01mm on slender parts. 5-axis CNC mill-turn operations handle complex geometries with tolerances down to ±0.005mm. Tighter tolerances require more inspection time, which should be factored into the quoted lead time.
Conclusion
this strategy is a structured, repeatable process. The difference between an order that ships in three days and one that takes three weeks almost always comes down to preparation: complete files, clear tolerance callouts, correct process selection, and a certified supplier with genuine expedited capacity.
To summarize the steps covered in this guide:
- Prepare complete design files with tolerances, material spec, and surface finish callouts
- Select the right machining process (CNC turning, Swiss lathe, mill-turn, automatic lathe, or cold forging) based on geometry and volume
- Submit a complete RFQ with required ship date and quality documentation requirements
- Approve production after reviewing DFM feedback and verify the supplier’s certifications
- Receive, inspect, and document incoming parts against your quality records
MFG SOLUTION delivers this approach with quotes within 8 hours and shipments within 3 days, backed by ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications. With 60+ engineering professionals, 5-axis CNC machines, 20 automatic lathes, and Swiss lathe capability, we machine precision parts up to 38mm diameter for electronics, automotive, and medical device manufacturers worldwide. If you have a tight deadline and a file ready to review, submit your specifications and receive a detailed quote before the end of your business day.