
2026-05-11
Machining Aluminum Parts: A Complete 2026 Guide

| Key Insight | Explanation |
|---|---|
| Aluminum is highly machinable | Aluminum alloys machine 3–5× faster than mild steel, reducing cycle times and tooling costs significantly. |
| Alloy choice drives outcomes | 6061-T6 and 7075-T6 are the most common CNC-machined alloys; each suits different strength and weight requirements. |
| Coolant strategy matters | Proper coolant or compressed air prevents built-up edge (BUE) on cutting tools, protecting surface finish and dimensional accuracy. |
| Cost varies widely | Part price depends on geometry complexity, tolerances, batch size, and finishing requirements — not just raw material cost. |
| Quality certifications reduce risk | ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications ensure traceable, auditable quality for medical and automotive applications. |
| Multiple processes available | CNC turning, Swiss lathe, milling, and cold forging each offer distinct advantages depending on part geometry and volume. |
Machining aluminum parts is the process of using subtractive manufacturing techniques — CNC milling, turning, Swiss lathe, and related operations — to cut raw aluminum stock into precise, finished components. Aluminum’s low density, excellent thermal conductivity, and outstanding machinability make it the preferred metal for industries ranging from aerospace to medical devices. This guide covers alloy selection, cutting parameters, cost drivers, common pitfalls, and the best practices that separate high-quality production runs from costly rework.
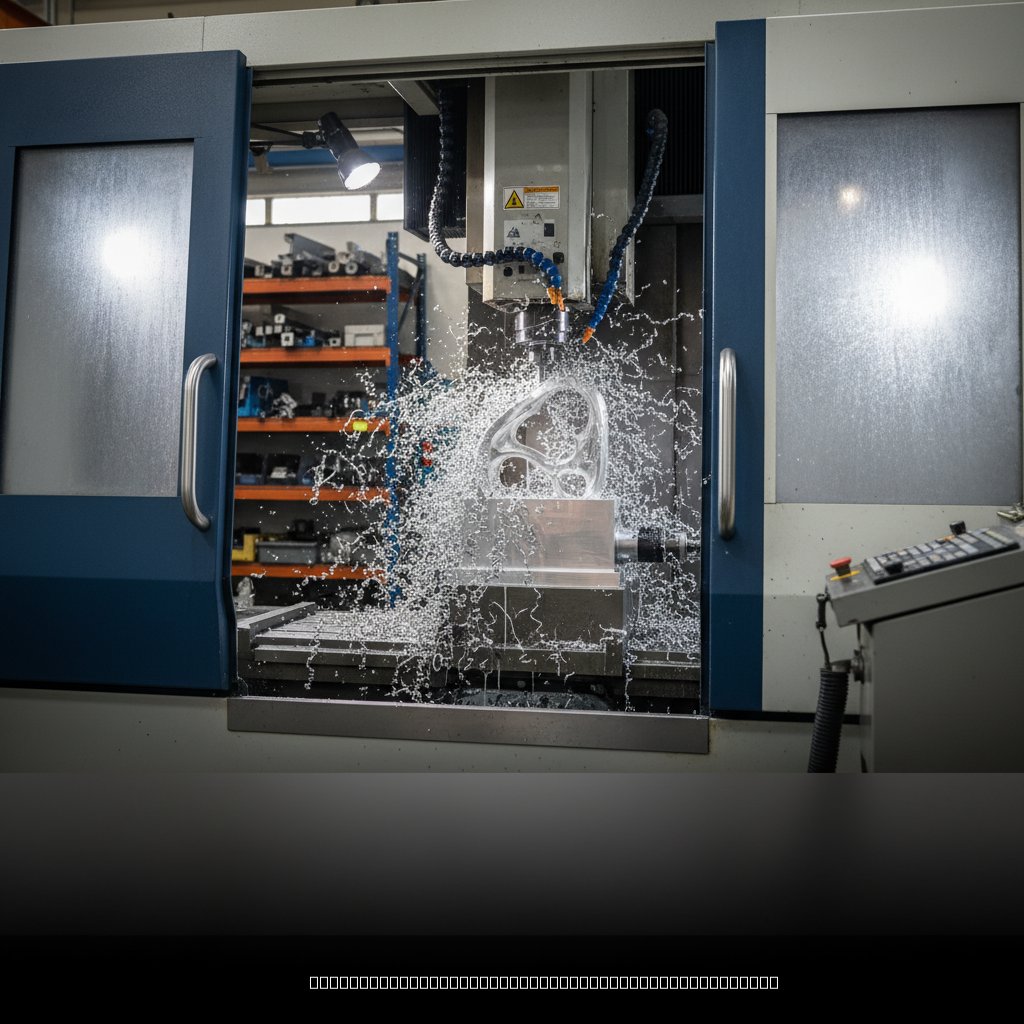
What Is Machining Aluminum Parts?
Machining aluminum parts refers to subtractive manufacturing processes that shape aluminum alloy stock into dimensionally accurate components using cutting tools, rotating spindles, and computer-controlled motion systems.
Aluminum is one of the most widely machined metals in the world. According to the ASM International Handbook on machining, aluminum alloys offer a superior combination of low cutting forces, excellent chip formation, and high surface finish quality compared to most other structural metals [1]. That’s why it dominates precision part production across automotive, electronics, and medical sectors.
Why Aluminum Is the Go-To Material
The material has a density of roughly 2.7 g/cm³ — about one-third that of steel — yet certain alloys achieve tensile strengths exceeding 570 MPa. This strength-to-weight ratio is hard to match. Pair that with natural corrosion resistance (from a self-forming oxide layer) and excellent thermal/electrical conductivity, and you have a material that suits a remarkably broad range of applications [2].
Common aluminum alloys used in CNC machining include:
- 6061-T6: The workhorse alloy. Good strength, excellent corrosion resistance, widely available, and easy to anodize.
- 7075-T6: Higher strength, favored for aerospace and structural applications where weight savings are critical.
- 2024-T3: Excellent fatigue resistance; common in aircraft fuselage components.
- 5052-H32: Superior corrosion resistance in marine environments; often used for enclosures and panels.
- 6063-T5: Preferred for extruded profiles and architectural components with smooth surface requirements [3].
Where Machined Aluminum Parts Are Used
The application range is broad. You’ll find machined aluminum parts in:
- Automotive components: valve bodies, brackets, sensor housings
- Medical devices: surgical instrument handles, implant tooling, diagnostic equipment enclosures
- Electronics: heat sinks, connector bodies, PCB standoffs
- Aerospace: structural brackets, fluid fittings, actuator components
- Consumer products: camera bodies, bicycle components, precision hardware
Industry analysts suggest the global CNC machining market for aluminum components will continue expanding through 2026 and beyond, driven by lightweighting trends in electric vehicles and miniaturization in consumer electronics [4].
How Machining Aluminum Parts Works
Machining aluminum parts follows a defined sequence: material selection, CAD/CAM programming, fixturing, cutting operations, finishing, and quality inspection — each stage directly affecting final part accuracy and cost.
The Core Machining Processes
Several distinct processes are used, often in combination, depending on part geometry and required tolerances:
- CNC Turning: The workpiece rotates while a stationary cutting tool removes material. Ideal for cylindrical parts like shafts, bushings, and connectors. Tolerances of ±0.01 mm are routinely achievable.
- CNC Milling: The cutting tool rotates and moves across a stationary or indexed workpiece. Used for flat surfaces, slots, pockets, and complex 3D profiles. 5-axis milling handles undercuts and compound angles in a single setup.
- Swiss Lathe Machining: A specialized form of CNC turning where the workpiece is guided through a collet bushing, providing exceptional rigidity for long, slender parts. Swiss lathe (also called Swiss screw machining) delivers tolerances as tight as ±0.005 mm on parts up to 38 mm in diameter.
- Automatic Lathe: High-volume bar-fed turning for simpler rotational geometries. Extremely cost-effective for large production runs.
- CNC Mill & Turn: Combines milling and turning in one machine setup, reducing handling time and maintaining positional accuracy across multiple features [5].
Pro Tip: For small aluminum parts under 38 mm diameter with tight tolerances, Swiss lathe machining typically delivers the best combination of dimensional accuracy and cycle time efficiency. If your part has both turned and milled features, a CNC mill & turn center eliminates the positional error introduced by re-fixturing between separate machines.
Cutting Parameters for Aluminum
Aluminum machines best at higher cutting speeds than steel. According to NIST’s technical reference on machining aluminum alloys, recommended surface speeds for high-speed steel (HSS) tooling range from 200 to 600 m/min, while carbide tooling can run at 600 to 3,000 m/min depending on alloy and operation [1].
| Alloy | Cutting Speed (Carbide) | Feed Rate | Coolant Recommendation |
|---|---|---|---|
| 6061-T6 | 600–1,500 m/min | 0.05–0.30 mm/rev | Flood coolant or compressed air |
| 7075-T6 | 500–1,200 m/min | 0.05–0.25 mm/rev | Flood coolant preferred |
| 2024-T3 | 400–900 m/min | 0.04–0.20 mm/rev | Flood coolant required |
| 5052-H32 | 300–800 m/min | 0.04–0.18 mm/rev | Mist or flood coolant |
Chip evacuation is critical. Aluminum produces long, stringy chips that can re-cut against the workpiece surface if not cleared promptly. High-pressure coolant directed at the cutting zone, combined with chip conveyors on CNC turning centers, keeps the work zone clear and protects surface finish [6].
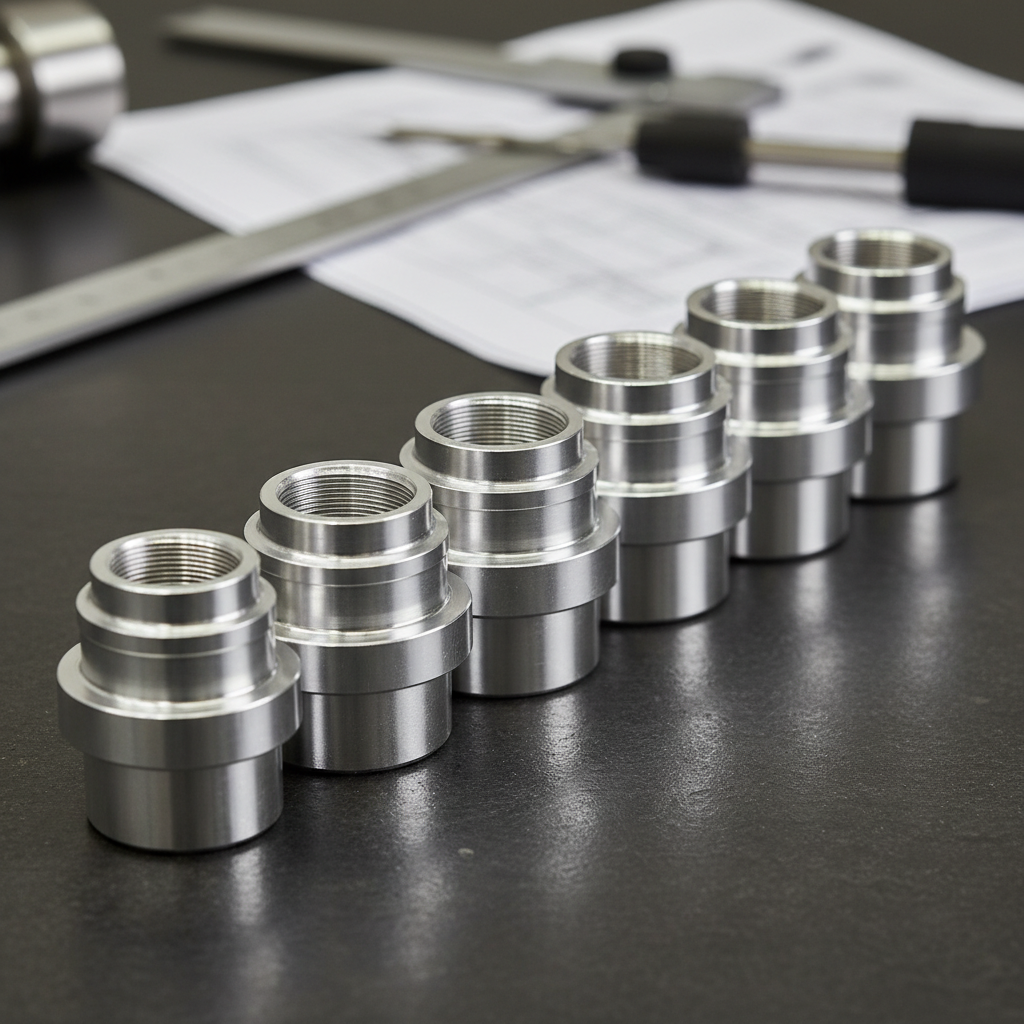
Key Benefits of Machining Aluminum Parts
Machining aluminum parts offers faster cycle times, lower tooling wear, and a broader range of post-process finishing options than most other metals — making it the cost-effective choice for both prototypes and high-volume production runs.
Performance and Production Advantages
The practical benefits are significant and well-documented:
- High machinability rating: Aluminum alloys score 300–1,500% on the machinability index relative to AISI B1112 steel (rated at 100%). This directly translates to faster cycle times and lower per-part cost [1].
- Reduced tool wear: Softer than steel or titanium, aluminum causes far less abrasive wear on carbide inserts and end mills. Tool life extends significantly, reducing consumable costs in production runs.
- Tight tolerances achievable: With proper fixturing and thermal management, tolerances of ±0.005 mm are routinely achievable on Swiss lathe and precision CNC turning operations.
- Excellent surface finish: Aluminum accepts fine surface finishes (Ra 0.4 µm or better) without specialized tooling, important for sealing surfaces and optical applications.
- Lightweight output: Parts weigh roughly one-third of equivalent steel components, reducing shipping costs and improving product performance in weight-sensitive assemblies [2].
- Finishing versatility: Machined aluminum parts accept anodizing, hard-coat anodizing, chromate conversion coating, powder coating, and electropolishing — covering virtually every functional and cosmetic requirement [7].
Economic Benefits for Production Runs
From a procurement standpoint, aluminum’s machinability directly reduces cost. A one-minute operation on aluminum might take three to five minutes on stainless steel, with proportionally higher tooling consumption. For high-volume runs of small precision parts, this difference compounds quickly.
A precision machining client in the electronics sector recently faced a sourcing challenge: they needed 50,000 aluminum connector housings per quarter with ±0.01 mm tolerances and a 5-day delivery window. By switching to a supplier with automatic lathe and Swiss lathe capacity — rather than conventional CNC milling — they reduced per-part cost by approximately 35% while meeting the tolerance requirement. The key was matching the process to the geometry, not defaulting to a single machining method.
Pro Tip: Don’t specify a machining process in your RFQ — specify the geometry, tolerance, and volume. A capable supplier with multiple process options (CNC turning, Swiss lathe, automatic lathe) will select the most cost-efficient method for your part. Locking in a process prematurely often adds 20–40% to part cost unnecessarily.
Research from the Aluminum Extruders Council confirms that precision cutting and CNC machining of aluminum extrusions and billets is the dominant fabrication method for structural and functional components across North American manufacturing [3].
Common Challenges in Machining Aluminum Parts
Machining aluminum parts presents specific challenges including built-up edge on cutting tools, part distortion from thermal expansion, and work-hardening in certain alloys — all of which require deliberate process controls to avoid scrapped parts.
Built-Up Edge and Surface Quality Issues
Built-up edge (BUE) is the most common problem machinists encounter with aluminum. It occurs when aluminum welds itself to the cutting tool’s rake face at elevated temperatures, creating a false cutting edge that degrades surface finish and dimensional accuracy. Prevention strategies include:
- Using sharp, polished carbide or PCD (polycrystalline diamond) tooling with high positive rake angles
- Maintaining adequate cutting speeds to keep temperatures in the optimal range
- Applying flood coolant or high-pressure mist to the cutting zone
- Selecting TiN or TiAlN-coated tools for high-volume runs where BUE is a recurring issue [5]
A common mistake is running aluminum at speeds optimized for steel. In practice, too-slow cutting speeds increase the likelihood of BUE formation. Running faster — within the machine’s spindle capability — often produces better surface results, not worse.
Thermal Distortion and Fixturing Problems
Aluminum’s coefficient of thermal expansion (23.1 µm/m·°C) is roughly twice that of steel. In high-speed machining, heat generated during cutting can cause measurable dimensional changes in the workpiece. For tight-tolerance parts (±0.01 mm or tighter), this is a real risk.
- Thin-wall distortion: Walls thinner than 1.5 mm can flex under cutting forces, causing chatter and out-of-tolerance dimensions. Proper fixturing and reduced depth-of-cut in finishing passes mitigate this.
- Residual stress: Certain alloys (notably 7075 and 2024) carry internal residual stresses from heat treatment. Aggressive material removal can release these stresses, causing the part to warp after machining. Rough machining followed by a stress-relief step before finishing is the accepted solution [1].
- Fixturing marks: Aluminum’s softness means clamps leave marks easily. Soft jaws, vacuum fixtures, and low-contact workholding solutions protect cosmetic surfaces.
One pitfall to watch for in procurement: suppliers who quote fast but don’t ask about residual stress or wall thickness. These are the details that separate a supplier who ships conforming parts from one who ships parts that look right but fail incoming inspection.
Best Practices for Machining Aluminum Parts in 2026
The most effective approach to machining aluminum parts in 2026 combines alloy-specific cutting parameters, validated toolpath strategies, rigorous in-process inspection, and supplier certifications that ensure traceability from raw material to finished part.
Process Selection and Design for Manufacturability
Design for Manufacturability (DFM) is the single highest-leverage activity before a single chip is cut. At MFG SOLUTION, we’ve found that DFM reviews catch tolerance conflicts, unnecessary surface finish requirements, and suboptimal feature geometries that would otherwise add 15–30% to part cost with no functional benefit.
Key DFM principles for aluminum parts:
- Maintain wall thickness above 1.5 mm wherever possible; 2.0 mm is the practical minimum for tight-tolerance features
- Specify tolerances only where functionally required — every ±0.01 mm tolerance zone adds inspection time and cost
- Design internal corners with the largest practical radius (at least 1/3 of cavity depth) to allow standard end mill geometries
- Avoid unnecessary thread depth; standard thread engagement of 1.5× diameter is sufficient for aluminum in most structural applications
- Consolidate features to minimize setups — each setup introduces potential positional error and adds handling time [8]
Quality Assurance and Certification Standards
For machining aluminum parts destined for regulated industries, quality certification isn’t optional. As of 2026, the three most relevant standards are:
- ISO 9001:2015: General quality management system covering process control, documentation, and continuous improvement. The baseline requirement for most industrial customers.
- ISO 13485:2016: Medical device quality management. Requires full traceability, validated processes, and controlled environments for parts used in medical applications.
- IATF 16949: Automotive quality management, building on ISO 9001 with additional requirements for production part approval (PPAP), measurement system analysis (MSA), and statistical process control (SPC).
Our team at MFG SOLUTION recommends requesting a supplier’s current certificates — not just claims — before committing to a production order. Certificates should be current (valid as of 2026), issued by an accredited certification body, and scope-specific to the processes you’re using.
Pro Tip: When evaluating a machining supplier for aluminum parts, ask specifically about their Statistical Process Control (SPC) implementation. A supplier running SPC on critical dimensions can provide Cpk data — a measure of process capability — that tells you objectively whether their process can hold your tolerance, not just whether their last batch happened to pass inspection.
According to Precision Steel Services, CNC machining of aluminum extrusions and billets requires careful attention to fixturing consistency and tool path validation to maintain dimensional repeatability across production runs [6]. This is especially true for batch sizes above 500 pieces, where even a 0.5% nonconformance rate generates significant rework cost.
Sources & References
- NIST Materials Data Repository, “Machining of Aluminum and Aluminum Alloys,” ASM International, 2026 (archival)
- ASM International Handbooks Online, “Machining of Aluminum and Aluminum Alloys,” Chapter Abstract, 2026
- Aluminum Extruders Council, “Cutting/Forming,” AEC.org, 2026
- JLCCNC, “A Complete Guide to Aluminum CNC Machining,” 2026
- CNCRush, “Best Practices for CNC Machining Aluminum Parts,” 2026
- Precision Steel Services, “CNC Machining for Aluminum Extrusions,” PrecisionSteel.org, 2026
- Protolabs, “Aluminum CNC Machining Service | Custom Parts | Anodizing,” 2026
- MakerVerse, “The Guide to CNC Machined Aluminum Parts,” 2026
Frequently Asked Questions
1. Does aluminum parts require machining?
Not all aluminum parts require machining, but most precision components do. Aluminum can be cast, extruded, forged, or stamped into near-net shapes, but machining aluminum parts is necessary when tight dimensional tolerances (typically ±0.05 mm or tighter), specific surface finishes, or complex geometries are required. CNC turning, milling, and Swiss lathe operations are the most common machining methods used to achieve these outcomes. For high-volume simple shapes, cold forging or extrusion followed by light finish machining often delivers the best cost-per-part.
2. How much does it cost to get aluminum machined?
Machining aluminum parts costs vary significantly based on part complexity, tolerance requirements, batch size, and the specific process used. For simple turned parts in volumes of 1,000 or more, per-part costs can fall below $2–$5. Complex milled components with tight tolerances and multiple setups can range from $20 to $200+ per part at low volumes. Machining time rates for aluminum typically run $0.50–$3.00 per minute, but the real cost driver is setup time, fixturing, and inspection — which are amortized across the batch. Larger production runs lower unit costs substantially.
3. Do you need coolant when milling aluminum?
Coolant is strongly recommended when milling aluminum, though the type matters more than the volume. Flood coolant (water-soluble cutting fluid) is the standard approach for most CNC milling operations, as it prevents built-up edge (BUE) formation on the tool, evacuates chips from the cut zone, and controls workpiece temperature to maintain dimensional accuracy. Compressed air alone works for light finishing passes and thin-wall features where liquid coolant could cause thermal shock. Avoid dry milling aluminum at high material removal rates — the combination of heat and chip re-cutting degrades surface finish and tool life rapidly.
4. Does aluminum have good machinability?
Yes — aluminum is one of the most machinable metals available. Most aluminum alloys score 300–1,500% on the standard machinability index (relative to AISI B1112 steel at 100%), meaning they can be machined 3–15 times faster than steel with less tool wear. This translates directly to lower cycle times, lower tooling costs, and more competitive part pricing. The 6061-T6 alloy is considered the benchmark for machinability among structural aluminum grades, while free-machining alloys like 2011 offer even higher ratings. The main trade-off is that aluminum’s softness makes it prone to built-up edge if cutting parameters aren’t optimized.
5. What is the best aluminum alloy for CNC machining?
6061-T6 is the most widely used alloy for this method due to its excellent balance of strength, corrosion resistance, machinability, and cost. It machines cleanly, holds tight tolerances, and accepts anodizing well. For higher-strength applications — aerospace brackets, high-load structural components — 7075-T6 is the preferred choice, though it’s slightly more challenging to machine and costs more per kilogram. If maximum machinability is the priority (for high-volume automatic lathe production, for example), the 2011 free-machining alloy delivers the highest chip-breaking performance but with reduced corrosion resistance.
6. How do I find a reliable supplier for custom aluminum machined parts?
Look for suppliers who hold current ISO 9001:2015 certification at minimum, and ISO 13485:2016 or IATF 16949 if your application is medical or automotive. Verify that their certificate scope covers the specific processes you need (CNC turning, milling, Swiss lathe). Request a sample order or first-article inspection (FAI) report before committing to full production volumes. Evaluate their quoting responsiveness — a supplier who takes more than 24 hours to quote a standard part likely has capacity or communication issues that will show up in production. For global sourcing, prioritize suppliers who offer digital quoting, traceable quality records, and fast ship windows.
Conclusion
this strategy remains one of the most cost-effective, versatile, and technically accessible manufacturing approaches available in 2026. The combination of aluminum’s outstanding machinability, broad alloy selection, and compatibility with multiple production processes — from Swiss lathe to CNC mill & turn — gives engineers and procurement teams genuine flexibility to optimize for cost, precision, or throughput.
The key decisions that determine outcome are alloy selection, process matching, cutting parameter discipline, and supplier quality certification. Get those right, and aluminum machining delivers tight tolerances, excellent surface finish, and competitive unit economics at scale.
MFG SOLUTION specializes in precision this approach up to 38 mm in diameter, with quotes returned within 8 hours and orders shipped within 3 days. Backed by ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, and supported by 60+ engineering professionals operating 5-axis CNC machines, Swiss lathes, and 20 automatic lathes, the team handles everything from prototype quantities to high-volume production runs for electronics, automotive, and medical device customers worldwide.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.