
2026-05-20
Forging Components: A Complete Guide for 2026

| Key Insight | Explanation |
|---|---|
| Forging produces stronger parts than casting | The compressive force aligns metal grain flow, yielding superior tensile strength and fatigue resistance compared to cast equivalents. |
| Four primary forging methods exist | Impression die (closed die), open die, cold forging, and seamless rolled ring forging each suit different part geometries and production volumes. |
| Cold forging is ideal for small precision parts | It shapes metal at room temperature, achieving tight tolerances, smooth surface finishes, and minimal material waste — perfect for high-volume runs under 38mm diameter. |
| Forged components serve critical industries | Automotive, aerospace, medical, and electronics sectors all rely on forging for load-bearing, safety-critical parts that can’t afford failure. |
| Quality certification matters for forged parts | ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications ensure full process control and traceability — essential for medical and automotive supply chains. |
| Design choices affect cost significantly | Draft angles, parting line placement, and tolerancing decisions made at the design stage can reduce tooling costs and scrap rates substantially. |
Forging components are metal parts shaped under high compressive force while the material remains in a solid state, producing parts with superior grain structure, strength, and fatigue resistance compared to other manufacturing methods. The process doesn’t melt the metal — it compresses and shapes it, which is exactly why forged parts outperform cast or machined-from-bar alternatives in demanding applications. If you’re sourcing precision parts for automotive, medical, or electronics applications, understanding forging components is essential to making smart material and process decisions.
This guide covers everything you need to know: what forging components are, how they’re manufactured, which types suit which applications, the real benefits and trade-offs, common pitfalls to avoid, and practical sourcing advice for 2026.
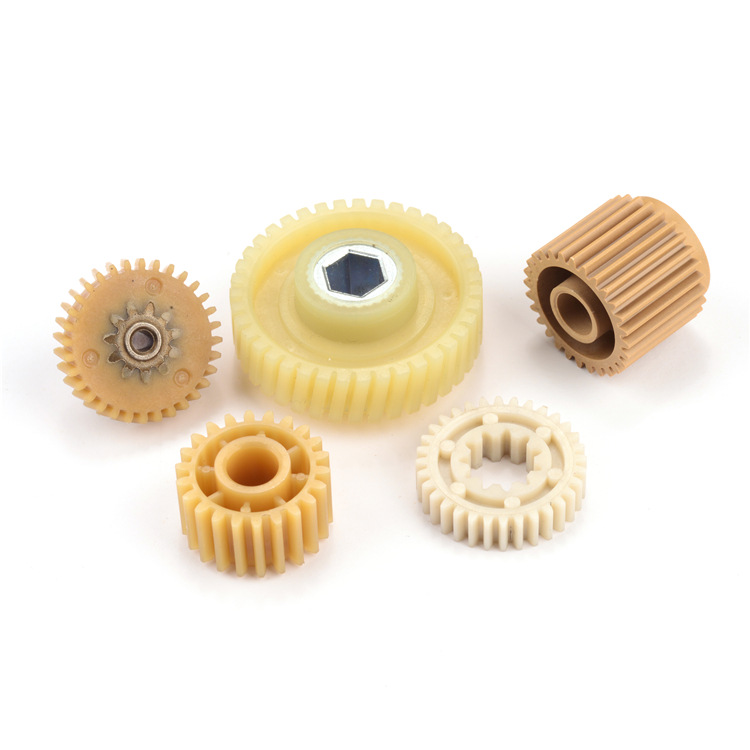
What Are Forging Components?
Forging components are precision-engineered metal parts produced by applying localized compressive forces to a metal workpiece, shaping it into a desired geometry while maintaining solid-state structure throughout the process. Unlike casting, no melting occurs — the metal’s crystalline grain structure is preserved and refined, which directly improves mechanical properties.
Definition and Core Characteristics
According to the Forging Industry Association, forging is “a manufacturing process where metal is pressed, pounded, or squeezed under great pressure into high-strength parts known as forgings” [1]. That definition captures the core principle: force, not heat alone, is what shapes the part.
Forging components share several defining characteristics:
- Continuous grain flow: The metal’s internal grain structure follows the contour of the part, rather than being cut across during machining. This dramatically improves fatigue strength.
- High density: Compressive forming eliminates internal voids and porosity that commonly appear in castings.
- Dimensional repeatability: Die-based forging produces consistent part geometry across large production runs.
- Material efficiency: Cold forging in particular generates minimal scrap compared to subtractive machining methods.
What Counts as a Forged Component?
Typical forged configurations include bars, blanks, connecting rods, cylinders, discs, rings, shafts, and sleeves [2]. In practice, any metal part that has been shaped through compressive force qualifies as a forged component, regardless of whether additional machining is applied afterward.
The distinction matters for procurement teams. A “forged and machined” part has gone through forging first to establish grain structure and near-net shape, then through CNC machining to achieve final tolerances and surface finish. This combination is common in automotive and medical device manufacturing, where both structural integrity and dimensional precision are non-negotiable.
Pro Tip: When reviewing supplier quotes for forging components, always ask whether the quoted part is forged-only or forged-plus-machined. The difference affects lead time, cost, and the tolerance grades you can realistically expect.
As of 2026, the global forging market continues to expand, driven by demand from electric vehicle (EV) platforms, medical implant manufacturing, and aerospace structural components. Industry analysts estimate that automotive applications alone account for roughly 35-40% of global forging output, a figure that has remained stable even as EV architectures shift part geometries and material requirements.
How Forging Components Are Made
Forging components are made by heating (or not, in the case of cold forging) a metal billet, then applying compressive force through dies or hammers to shape the part into its final or near-final geometry.
The Core Forging Process
The manufacturing sequence for most forged components follows these steps:
- Billet preparation: Raw metal stock (steel, aluminum, titanium, brass, or other alloys) is cut to the correct weight and volume for the part.
- Heating (for hot/warm forging): The billet is heated to a specified temperature. For steel, this is typically 1,100–1,250°C for hot forging, or 650–900°C for warm forging.
- Die placement: The heated billet is positioned in the lower die cavity.
- Compression: The upper die closes under hydraulic, mechanical, or hammer force, compressing the metal into the die cavity.
- Flash removal (trimming): Excess material squeezed out at the die parting line (called flash) is trimmed away.
- Heat treatment: Many forged parts undergo annealing, quenching, or tempering to optimize final mechanical properties.
- Finishing: CNC machining, grinding, or surface treatment brings the part to final dimensional specifications.
Cold Forging: A Special Case for Small Parts
Cold forging (also called cold heading or cold forming) shapes metal at or near room temperature. Cornell Forge notes that cold forging produces parts with excellent surface finish and tight dimensional tolerances without the scaling and decarburization that hot forging can introduce [3].
For small precision components under 38mm diameter, cold forging is particularly attractive because:
- Material utilization approaches 100% with minimal scrap
- Surface hardness increases through work hardening, often eliminating secondary heat treatment
- Cycle times are fast, supporting high-volume production economics
- Dimensional consistency across thousands of parts is excellent
At MFG SOLUTION, we’ve found that combining cold forging with CNC turning or Swiss lathe finishing delivers the best balance of structural performance and dimensional precision for small fasteners, connectors, and shaft components. The cold forging step establishes grain structure and near-net shape; the CNC step achieves the final tolerances your design requires.
Pro Tip: For high-volume runs of small forging components (10,000+ pieces), cold forging combined with automatic lathe finishing typically delivers the lowest cost-per-part compared to machining from bar stock alone. Ask your supplier to model both process routes before committing to tooling investment.
According to Trenton Forging, roll forging is another method used for elongated parts like engine bearings, wheel bearings, flanges, and gears, where the metal is shaped by passing it between two rotating dies [4]. This expands the range of geometries achievable through forging well beyond simple axisymmetric shapes.
Types of Forging Components and Their Applications
Forging components are categorized by the forging method used to produce them, and each method suits a different combination of part geometry, material, production volume, and tolerance requirement.
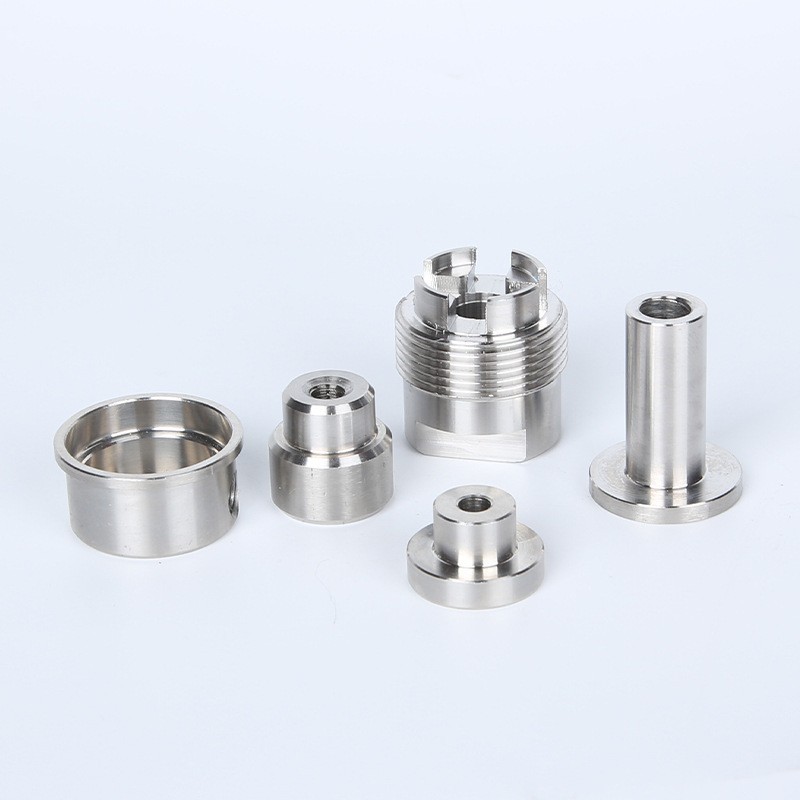
The Four Main Types of Forging
| Forging Type | Temperature | Best For | Typical Applications |
|---|---|---|---|
| Impression Die (Closed Die) | Hot (1,100–1,250°C) | Complex shapes, high volume | Connecting rods, crankshafts, hand tools |
| Open Die Forging | Hot | Large parts, low volume | Shafts, cylinders, large discs |
| Cold Forging | Room temperature | Small precision parts, high volume | Fasteners, pins, connectors, small shafts |
| Seamless Rolled Ring | Hot | Annular shapes | Bearing races, flanges, gear blanks |
Industry-Specific Applications of Forged Components
The Forging Industry Association documents a wide range of applications across sectors [2]:
- Automotive: Connecting rods, crankshafts, steering knuckles, wheel hubs, transmission gears, and suspension components. According to Aerostar Manufacturing, farm implements and engine/transmission components also rely heavily on forged parts including gears, shafts, levers, and spindles [5].
- Aerospace: Turbine discs, landing gear components, structural brackets, and engine mounts where strength-to-weight ratio is critical.
- Medical devices: Orthopedic implants, surgical instrument handles, and prosthetic joint components where biocompatibility and fatigue life are paramount.
- Electronics: Connector housings, heat sink bases, and precision fasteners for PCB assemblies.
- Oil and gas: Valve bodies, pipe fittings, flanges, and pressure vessel components rated for extreme conditions.
- Defense and ordnance: Structural frames, weapon components, and vehicle drive train parts requiring certified material traceability.
The breadth of these applications explains why forging components remain a foundational manufacturing method in 2026, even as additive manufacturing and advanced casting techniques continue to evolve.
Key Benefits of Forging Components in 2026
Forging components offer superior mechanical properties, dimensional consistency, and long-term reliability compared to cast or machined-from-bar alternatives, making them the preferred choice for safety-critical and high-cycle applications.
Mechanical and Structural Advantages
The structural case for forging is strong. Compressive forming aligns the metal’s grain flow to the part’s contour, which is fundamentally different from a casting where grain structure is random, or a machined part where grain is cut across. The Steel Founders’ Society of America acknowledges that forged components demonstrate advantages in applications with high cyclic loading — though they also note that casting can be economically competitive for complex geometries at sufficient volumes [6].
- Tensile strength: Forged steel typically achieves 10–15% higher tensile strength than equivalent cast steel of the same alloy.
- Fatigue resistance: The continuous grain flow structure resists crack initiation under cyclic stress, extending component service life.
- Impact toughness: Forged parts absorb impact energy more effectively, critical for automotive crash-safety components.
- Reduced porosity: Internal voids present in castings are eliminated through compressive forming, improving pressure-tightness.
Economic and Operational Benefits
Beyond raw mechanical performance, forging components offer practical economic advantages for production environments:
- Material efficiency: Cold forging especially produces near-net-shape parts, reducing material waste and machining time.
- Consistency at scale: Die-based processes produce highly repeatable parts across large batches, reducing inspection burden and scrap rates.
- Lower total cost of ownership: Longer part life and fewer field failures offset higher upfront tooling costs over the production run.
- Compatibility with post-processing: Forged blanks accept CNC machining, grinding, plating, and heat treatment predictably, simplifying process planning.
Industry analysts suggest that for production volumes above 5,000 pieces, forging typically delivers a lower cost-per-part than machining from solid bar stock, once tooling amortization is factored in. Results vary depending on part complexity, material, and tolerance requirements.
Pro Tip: Don’t evaluate forging components solely on piece price. Calculate total cost including tooling amortization, scrap rate, secondary machining time, and field failure rates. In our experience, the total-cost picture often favors forging over machining from bar for runs above 5,000 pieces, even when the per-piece forging price looks higher initially.
Common Challenges and Mistakes in Forging
Forging components can develop defects or cost overruns when design, material selection, or process parameters aren’t properly controlled. Knowing the most common failure points helps you avoid them early.
Common Forging Defects
A common mistake is assuming that forging automatically produces defect-free parts. In practice, several defect types can occur if the process isn’t carefully managed:
- Laps and folds: Metal folds back on itself during forming, creating a surface discontinuity that looks like a crack. Usually caused by improper die design or insufficient material flow.
- Cold shuts: Two metal streams meet without fully bonding, leaving an internal seam. Often results from incorrect temperature or die fill sequence.
- Underfill: Insufficient material in the die cavity leaves incomplete features on the part. Caused by under-weight billets or inadequate forging pressure.
- Flash-line cracks: Cracks propagating from the flash trim line into the part body. Typically a trimming die geometry or temperature issue.
- Internal bursts: Internal cracking caused by excessive tensile stress during forging, often from too-rapid deformation of certain alloys.
Design and Sourcing Mistakes to Avoid
According to GS Forgings, size, complexity, and draft angle are the three design variables that most directly affect forging cost and quality [7]. One pitfall to watch for: engineers sometimes specify machined-part tolerances on forged drawings without accounting for the inherent dimensional variation of the forging process itself, leading to unnecessarily expensive secondary machining.
- Insufficient draft angles: Parts with no draft (vertical walls) are difficult to eject from the die, causing tool damage and surface defects. A minimum 3–5° draft is standard practice.
- Ignoring parting line placement: A poorly placed parting line complicates die construction and increases flash volume, adding cost.
- Over-specifying tolerances: Applying CNC-machining tolerances (±0.01mm) to forged surfaces that will later be machined anyway adds cost without benefit. Specify forging tolerances only where the forged surface is the functional surface.
- Wrong material selection: Some alloys (high-carbon steels, certain titanium grades) have narrow forging temperature windows. Selecting a material without verifying its forgeability can lead to cracking or incomplete fill.
- Inadequate supplier qualification: Sourcing forging components from uncertified suppliers without documented process control creates audit risk, especially in medical and automotive supply chains where IATF 16949 or ISO 13485 compliance is required.
A precision machining client once approached our team after receiving a batch of cold-forged connectors with consistent underfill on one feature. The root cause was a billet weight specification that was 4% below the die cavity volume — a small oversight in the design documentation that caused 100% rejection of the batch. Proper first-article inspection (FAI) protocols, documented under ISO 9001:2015, would have caught this before full production.
Best Practices for Sourcing Forging Components in 2026
Sourcing forging components successfully in 2026 requires a structured approach that covers design optimization, supplier qualification, quality verification, and supply chain risk management.
Supplier Qualification and Certification Requirements
Not all forging suppliers are equal. For components destined for regulated industries, certification is non-negotiable:
- ISO 9001:2015: The baseline quality management system standard. Confirms the supplier has documented processes, traceability, and corrective action procedures.
- IATF 16949: The automotive-specific quality standard. Required by most Tier-1 and Tier-2 automotive OEMs for forged and machined components.
- ISO 13485:2016: The medical device quality management standard. Essential for forged implant components, surgical instruments, and device housings.
- Material certification (Mill Certs): Every forged component should be traceable to a certified material heat with documented chemical composition and mechanical properties.
Our team at MFG SOLUTION recommends requesting a copy of the supplier’s current quality certificates, their last internal audit report, and a sample first-article inspection (FAI) report before committing to a production order. This takes one email and saves significant rework risk downstream.
Design for Forgeability: Key Guidelines
The 7 Essentials for Forging Components Manufacturers framework outlines that a capable forging supplier should maintain integrated engineering design, toolroom capability, cutting shop, forging shop, heat treatment, and finishing operations under one roof [8]. When evaluating suppliers, confirm they control these steps rather than outsourcing critical operations.
Practical design guidelines for forging components:
- Add 3–7° draft angles to all vertical walls to ensure clean die release.
- Specify generous corner radii (minimum 1.5mm internal, 3mm external) to promote smooth metal flow and extend die life.
- Place the parting line at the largest cross-section of the part to minimize die depth and flash volume.
- Avoid abrupt cross-section changes; use tapers and fillets to guide metal flow progressively.
- Identify which surfaces will be machined after forging and apply forging tolerances only to non-machined functional surfaces.
- Confirm material forgeability with your supplier before finalizing alloy selection, especially for high-strength or exotic alloys.
| Sourcing Factor | What to Check | Why It Matters |
|---|---|---|
| Quality Certifications | ISO 9001, IATF 16949, ISO 13485 | Confirms documented process control and audit readiness |
| Material Traceability | Mill certificates per heat/batch | Required for aerospace, medical, and automotive compliance |
| First Article Inspection | Dimensional report against drawing | Catches tooling and process issues before full production run |
| Lead Time | Quote turnaround + production + shipping | Directly impacts your product launch and inventory planning |
| Post-Forging Capability | CNC machining, heat treatment, plating | Single-source finishing reduces handling risk and lead time |
Sources & References
- Forging Industry Association, “What is Forging,” 2026
- Forging Industry Association, “Common Applications of Forgings,” 2026
- Cornell Forge Co., “Understanding Forging & Forged Parts,” 2026
- Trenton Forging, “Metal Forging Methods Explained,” 2026
- Aerostar Manufacturing, “The Role of Forging in Automotive and Aerospace Industries,” 2026
- Steel Founders’ Society of America, “Castings or Forgings? A Realistic Evaluation,” 2026
- GS Forgings, “Design Considerations for Forging,” 2026
- LinkedIn, “7 Essentials for Forging Components Manufacturer,” 2026
Frequently Asked Questions
1. What are forging components?
Forging components are metal parts shaped by applying compressive force to a solid metal billet using dies, hammers, or presses, without melting the material. This process refines the metal’s internal grain structure along the part’s contour, producing superior tensile strength, fatigue resistance, and impact toughness compared to cast or machined-from-bar equivalents. Common examples include connecting rods, shafts, flanges, fasteners, and gear blanks used across automotive, aerospace, and medical applications.
2. What are the 4 types of forging?
The four primary forging types are: (1) impression die (closed die) forging, where metal is shaped between two die halves for complex, high-volume parts; (2) open die forging, where unrestricted dies shape large, simple geometries; (3) cold forging, which forms metal at room temperature for small precision parts with tight tolerances and excellent surface finish; and (4) seamless rolled ring forging, which produces annular shapes like bearing races and flanges. Each method suits different combinations of part size, geometry, material, and production volume.
3. What are the components of a forge (the equipment setup)?
An industrial forging setup includes the forging press or hammer (the primary force-generating machine, ranging from mechanical crank presses to hydraulic presses rated in thousands of tons), the die set (upper and lower tooling that defines part geometry), a furnace or induction heater for hot and warm forging, a billet shear or saw for stock preparation, trimming dies for flash removal, and a conveyor or robotic handling system for high-volume production. For cold forging, the furnace is replaced by a cold heading or cold forming machine operating at room temperature.
4. Why is borax used on metal during forging?
Borax (sodium tetraborate) acts as a flux during forge welding operations. It dissolves and removes iron oxide scale (mill scale) from the heated metal surface, lowers the effective melting point of the oxide layer, and creates a liquid slag that protects the clean metal from re-oxidizing before the weld is struck. This ensures intimate metal-to-metal contact during the forge weld, producing a sound bond. In modern industrial forging, borax-based fluxes are primarily relevant to blacksmithing and forge welding rather than production press forging.
5. How do forging components compare to castings?
Forging components generally outperform castings in tensile strength, fatigue resistance, and impact toughness because the grain structure is continuous and directional rather than random. Castings, however, can achieve more complex internal geometries (hollow sections, undercuts) that forging cannot produce without secondary machining. The Steel Founders’ Society of America notes that at higher production volumes with simpler configurations, forged components can become economically convertible to castings. The right choice depends on your specific load case, geometry, volume, and cost target.
6. What materials are commonly used for forging components?
Carbon steel and alloy steel account for the majority of forged components globally, valued for their strength, forgeability, and cost. Aluminum alloys (6061, 7075) are widely forged for aerospace and automotive parts where weight reduction is critical. Stainless steel forgings serve medical and food-processing applications. Titanium alloys are forged for aerospace structural parts and orthopedic implants. Brass and copper alloys are cold-forged for electrical connectors and precision fasteners. Material selection should always be confirmed with your forging supplier for forgeability at the required production temperature.
Conclusion
this practice remain one of the most reliable ways to produce metal parts with consistent mechanical performance, especially for safety-critical applications in automotive, medical, and aerospace sectors. The process has been refined over decades, and as of 2026, it continues to evolve with tighter process controls, improved die materials, and better integration with CNC finishing operations.
Choosing the right forging method, designing for forgeability, and qualifying your supplier properly are the three decisions that most directly determine whether your this method project succeeds or creates costly rework. Cold forging combined with precision CNC machining delivers the best economics for small parts under 38mm diameter at production volumes.
MFG SOLUTION specializes in exactly this combination: cold forging, CNC turning, Swiss lathe, and mill-turn finishing, all under ISO 9001:2015, ISO 13485:2016, and IATF 16949 certification. Our team of 60+ engineering professionals can quote your this strategy within 8 hours and ship completed parts within 3 days. If you’re sourcing small precision this approach and need a certified, fast, and cost-effective manufacturing partner, we’re ready to help.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: