
2026-05-28
Custom Steel Forged Parts: A Complete Buyer’s Guide

| Key Insight | Explanation |
|---|---|
| Forging outperforms casting in strength | The compressive forging process aligns steel’s grain structure, producing parts that are significantly stronger and more fatigue-resistant than cast equivalents. |
| Three main forging methods exist | Hot forging, warm forging, and cold forging each suit different part geometries, tolerances, and production volumes. Choosing the right method directly affects cost and quality. |
| Material selection is critical | Carbon steel, alloy steel, and stainless steel each offer different trade-offs in strength, corrosion resistance, and machinability that affect part performance and price. |
| Certifications protect buyers | ISO 9001:2015, IATF 16949, and ISO 13485:2016 certifications signal documented process control, reducing quality risk for automotive, medical, and electronics applications. |
| Cold forging suits small precision parts | For parts under 38mm diameter, cold forging delivers tight tolerances and excellent surface finish with minimal post-processing, making it highly cost-effective at volume. |
| Rapid sourcing is now achievable | Modern certified suppliers can quote within 8 hours and ship within 3 days, compressing traditional 4–6 week lead times to days without sacrificing quality. |
Custom steel forged parts are components shaped from steel billets or bars through controlled compressive force, produced to a buyer’s exact dimensional and material specifications. The forging process realigns the steel’s internal grain structure, creating parts that are measurably stronger and more fatigue-resistant than machined or cast alternatives. Whether you’re sourcing fasteners for an automotive assembly line, structural connectors for heavy machinery, or precision fittings for a medical device, understanding how forging works, which method fits your application, and what to demand from a supplier can save you significant time and money.
This guide covers everything procurement managers and engineers need to know: the core forging processes, material choices, real-world benefits, common sourcing mistakes, and the best practices shaping the market as of 2026.
What Are Custom Steel Forged Parts?
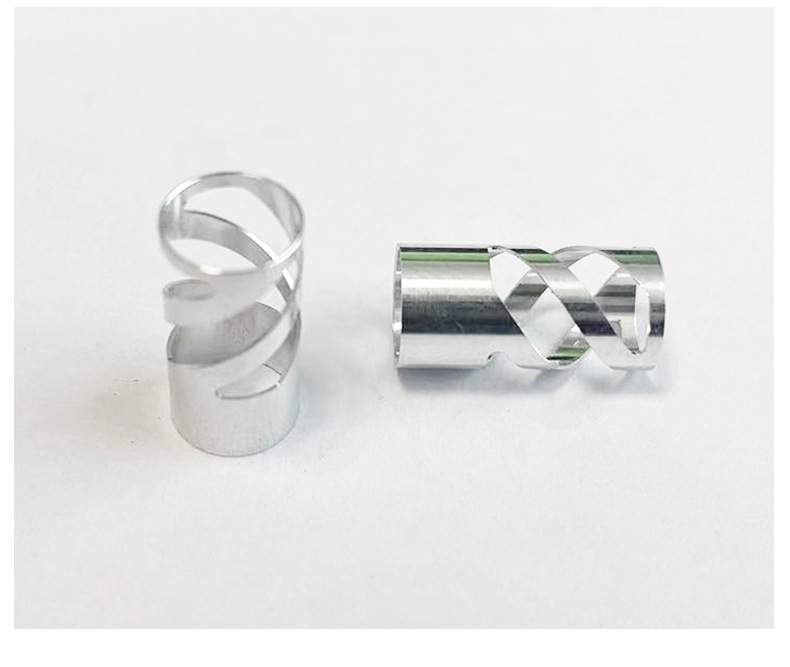
Custom steel forged parts are steel components manufactured by applying compressive force, via hammer, press, or die, to shape heated or room-temperature steel into a specific geometry defined by the customer. Unlike standard off-the-shelf forgings, custom parts are produced to print, meaning every dimension, tolerance, and material grade is specified by the buyer [1].
Why Forging Differs from Other Manufacturing Methods
Forging isn’t just another way to shape metal. The compressive force used in forging causes plastic deformation that refines and aligns the steel’s grain flow along the contours of the part. This is fundamentally different from casting, where molten metal is poured into a mold and solidifies with a random grain structure, or from machining, which cuts away material without influencing internal grain at all.
The result? Forged parts consistently outperform cast or machined equivalents in tensile strength, impact resistance, and fatigue life. According to the Forging industry overview on Wikipedia, forged components can achieve strength levels that would require significantly heavier castings to match, making forging the preferred choice wherever weight-to-strength ratio matters [1].
Where Custom Steel Forgings Are Used
The applications are broad. Industries that rely heavily on custom steel forged parts include:
- Automotive: Connecting rods, crankshafts, steering knuckles, and wheel hubs
- Aerospace: Structural brackets, landing gear components, and turbine discs
- Oil and gas: Valve bodies, flanges, and pipe fittings
- Heavy machinery: Gears, shafts, and coupling hubs
- Medical devices: Surgical instrument bodies and implant components
- Electronics manufacturing: Precision housings and connector bodies
Industry analysts note that demand for custom forgings in automotive and medical sectors has grown steadily through 2024–2026, driven by tightening performance requirements and supply chain consolidation pressures [2].
| Manufacturing Method | Grain Structure | Typical Strength | Best For |
|---|---|---|---|
| Forging | Aligned, continuous | Highest | High-stress, fatigue-critical parts |
| Casting | Random, isotropic | Moderate | Complex shapes, low-stress applications |
| Machining from bar stock | Unmodified bar grain | Good | Low-volume, tight-tolerance parts |
| Powder metallurgy | Sintered, porous | Moderate to good | Complex near-net shapes, high volume |
How Custom Steel Forged Parts Are Made
The production of this practice follows a defined sequence, from material selection through final inspection, with each step directly influencing the part’s mechanical properties and dimensional accuracy.
The Three Core Forging Methods
Not all forging is the same. The three primary methods differ in temperature, tooling, and the types of parts they produce best [3]:
- Hot forging: Steel is heated above its recrystallization temperature (typically 1,100–1,250°C for carbon steel) before forming. This makes the metal highly malleable, allowing complex shapes with less force. Hot forging is the most common method for large structural parts.
- Warm forging: Performed between 650–950°C. It offers better dimensional accuracy than hot forging and lower energy consumption, making it suitable for medium-complexity parts requiring tighter tolerances.
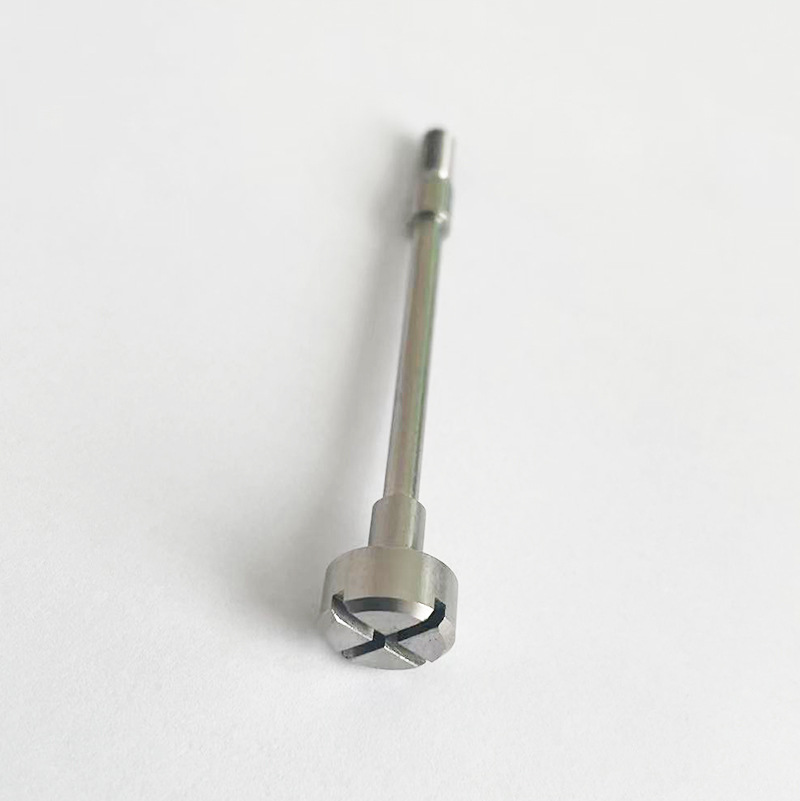
- Cold forging (cold heading): Performed at or near room temperature. The steel work-hardens during forming, resulting in excellent surface finish and very tight tolerances, often eliminating the need for secondary machining. Cold forging is ideal for small, high-volume parts such as fasteners, pins, and connector bodies.
Pro Tip: For small precision parts under 38mm diameter produced in high volumes, cold forging almost always delivers the best cost-per-part outcome. The near-net-shape output means less machining time and less material waste, both of which reduce unit cost significantly at scale.
Step-by-Step: The Custom Forging Production Process
- Design review and DFM (Design for Manufacturability): Engineers review the customer’s drawing to assess forgeability, identify undercuts or draft angles, and recommend material grades.
- Die design and fabrication: Custom dies (the tooling that shapes the part) are machined from tool steel. Die quality directly determines part consistency across a production run.
- Billet preparation: Steel bar stock is cut to precise weight, ensuring consistent volume for each forging cycle.
- Heating (for hot/warm forging): Billets are heated in controlled furnaces to the target temperature range for the alloy being used.
- Forging: The heated (or room-temperature, for cold forging) billet is placed in the die and struck or pressed into shape. Closed-die forging, used for custom parts, confines the metal completely within the die cavity for dimensional consistency [4].
- Trimming: Flash (excess metal squeezed out between die halves) is trimmed away.
- Heat treatment: Processes such as annealing, normalizing, or quench-and-temper are applied to achieve the specified mechanical properties.
- Secondary machining: CNC turning, milling, or Swiss lathe operations bring critical features to final tolerance.
- Inspection and testing: Dimensional checks, hardness testing, and non-destructive testing (NDT) verify conformance to specification.
According to CFS Forge’s technical documentation, closed-die forging is the dominant method for this method because it produces consistent, near-net-shape components with minimal material waste [5].
Key Benefits of Custom Steel Forged Parts
this strategy deliver a combination of mechanical performance, design flexibility, and long-term cost efficiency that few other manufacturing methods can match. Here’s why engineers and procurement teams consistently specify them for demanding applications.
Mechanical and Structural Advantages
- Superior strength-to-weight ratio: The aligned grain structure produced by forging means parts can be designed lighter while meeting the same load requirements as heavier cast equivalents.
- Higher fatigue resistance: Forged parts handle cyclic loading far better than castings, which can harbor internal porosity that initiates fatigue cracks.
- Consistent mechanical properties: Every part in a batch shares the same grain refinement and heat treatment history, reducing property variation across a production run.
- Excellent impact toughness: Critical in automotive crash structures and heavy equipment where sudden load spikes are common.
- Reliability in extreme environments: Forged steel parts maintain structural integrity under high temperature, pressure, and corrosive conditions [6].
Research from industry sources indicates that forged steel components can exhibit tensile strength values 20–30% higher than equivalent cast parts, depending on alloy and heat treatment [7].
Economic and Supply Chain Benefits
- Near-net-shape output: Less material removal means lower machining costs and shorter cycle times.
- Long die life: Quality forging dies can produce tens of thousands of parts, spreading tooling cost across high volumes.
- Reduced scrap rates: Closed-die forging produces consistent geometry, cutting the reject rate compared to casting.
- Single-source consolidation: A capable forging supplier with secondary machining capability can deliver a finished part, reducing vendor count and coordination overhead.
In practice, manufacturers that switch from cast-then-machine workflows to forge-then-finish often report 15–25% reductions in total part cost for medium-to-high volume runs. Results vary depending on part complexity, volume, and material grade.
For those working on special events or branded projects that require custom-made components, it’s worth noting that the same attention to detail applied in precision manufacturing extends to other customized products. For example, custom presentation packaging like Custom Wax Seal Stamp Kits Events demonstrate how bespoke manufacturing thinking applies across industries, from metal parts to branded accessories.
Pro Tip: When evaluating total cost of ownership for a forged part, don’t just compare the per-piece price. Factor in scrap rate, secondary machining time, and the cost of field failures. Forged parts’ lower failure rates often justify a higher unit price over the product’s service life.
Common Challenges and Mistakes to Avoid
Sourcing this approach isn’t without pitfalls. Even experienced procurement teams make avoidable mistakes that result in delayed shipments, rejected parts, or unexpected costs. Here are the most common issues, and how to sidestep them.
Design and Specification Errors
- Insufficient draft angles: Draft angles (the slight taper on vertical surfaces) are required for the forged part to release cleanly from the die. Designs without adequate draft create tooling problems and surface defects. A minimum of 3–5 degrees is standard for most closed-die forgings [8].
- Unrealistic tolerance expectations: Forging produces near-net shapes, not finished dimensions. Specifying machined tolerances (±0.01mm) on forged surfaces that will be machined anyway wastes inspection resources. Reserve tight tolerances for features that truly need them.
- Wrong material grade for the application: Specifying a high-alloy steel when carbon steel would meet the load requirements is a common cost inflation error. Conversely, under-specifying material in corrosive environments leads to premature failure.
- Missing heat treatment requirements: Forgings supplied without a specified heat treatment condition (annealed, normalized, quench-and-tempered) will have unpredictable hardness and strength. Always define the required mechanical property range.
A manufacturing client we worked with recently submitted drawings for a small steel connector without specifying draft angles or heat treatment. The result was a first-article rejection and a two-week delay while the design was revised. That’s a preventable setback with proper upfront DFM review.
Supplier Selection Mistakes
- Choosing on price alone: The lowest quoted price often reflects missing inspection steps, inferior raw material, or unqualified tooling. A part that fails in service costs far more than the savings on unit price.
- Not verifying certifications: As of 2026, any supplier claiming ISO 9001:2015 or IATF 16949 compliance should be able to provide current, auditable certification documents. Don’t accept verbal assurances.
- Ignoring secondary machining capability: If your forged part requires CNC turning or milling to final dimensions, a supplier without in-house secondary machining will add lead time and coordination risk by outsourcing that work.
- Overlooking capacity constraints: A forge shop with limited press tonnage may not be able to handle your geometry, even if their price is competitive. Always confirm that the supplier’s equipment matches your part’s forming requirements [9].
Best Practices for Sourcing Custom Steel Forged Parts in 2026
The sourcing landscape for the practice has shifted meaningfully through 2024–2026. Supply chain resilience pressures, tighter quality mandates from automotive and medical OEMs, and the rise of digital quoting platforms have all changed what “best practice” looks like. Here’s what works now.
Qualification and Documentation Standards
- Require a First Article Inspection Report (FAIR): A FAIR documents that the first production part meets every requirement on the drawing. It’s the baseline for production approval and should be non-negotiable for any new part number.
- Specify material traceability: Require mill certificates (also called material test reports) for every heat of steel used. This documents the chemical composition and mechanical properties of the raw material, which is mandatory for aerospace, automotive Tier-1, and medical device supply chains.
- Mandate process control documentation: Certified suppliers under ISO 9001:2015 or IATF 16949 maintain documented control plans, inspection records, and non-conformance reports. Request these as part of your supplier qualification process.
- Conduct periodic supplier audits: Even with strong certifications, annual or biannual audits of your forging supplier’s facility and quality system reduce long-term risk.
Industry analysts at Scot Forge emphasize that large-precision metal parts in demanding applications require open-die or closed-die forging manufacturers with documented quality systems, not just claimed capabilities [10].
Optimizing Cost Without Sacrificing Quality
- Consolidate to a supplier with multiple manufacturing methods. A partner offering cold forging, CNC turning, Swiss lathe, and automatic lathe services can optimize the process for your specific part geometry, rather than forcing every part into one method.
- Design for the process early. Involve your forging supplier during the design phase. Small geometry changes, like adding a draft angle or adjusting a fillet radius, can dramatically reduce die complexity and unit cost.
- Order in economical batch sizes. Forging economics improve significantly with volume. Work with your supplier to understand the break-even point between tooling amortization and per-piece cost.
- Use rapid quoting to compare options quickly. Suppliers that can return a detailed quote within 8 hours allow procurement teams to compare multiple sourcing options without extending the project timeline.
- Validate with small initial batches. Before committing to a full production run, order a small qualification batch and perform incoming inspection. This limits exposure if the supplier’s first production run has issues.
Pro Tip: At MFG SOLUTION, we’ve found that procurement teams who share full drawings with GD&T callouts (Geometric Dimensioning and Tolerancing, the standardized system for defining part geometry) during the quoting stage receive far more accurate quotes, with fewer change orders downstream. Incomplete drawings are the single biggest driver of quote revisions and schedule delays.
Our team at MFG SOLUTION recommends that buyers sourcing this practice for automotive or medical applications always request a copy of the supplier’s current IATF 16949 or ISO 13485:2016 certificate, not just a claim of compliance. Certificates have expiry dates and audit cycles; an expired certificate is a red flag.
The paper manufacturing sector offers a useful parallel: as Paper360 reports, paper mills rely on complex forged parts including rings, discs, hubs, and shafts where dimensional consistency and material integrity are non-negotiable for continuous operation [11]. The same principle applies across any industry where downtime is expensive.
Sources & References
- Wikipedia, “Forging,” 2026
- Walker Forge, “Custom Forged Parts – Custom Metal Forgings,” 2026
- Deeco Metals, “Custom Steel Forged Parts,” 2026
- Trinity Forge, “Custom Forging,” 2026
- CFS Forge, “Forging Tooling, Forging Dies | Steel Forging,” 2026
- Canton Drop Forge, “High-Quality Custom Forging & Precision Forged Parts,” 2026
- GL Forge, “Custom Forged Parts | Stainless Steel Forging | CNC Milling,” 2026
- Modern Group USA, “Custom Forge Manufacturing – Custom Metal Forging Services,” 2026
- R&M Forge and Fittings, “Custom Metal Forgings Manufacturer,” 2026
- Scot Forge, “Blog – Customer Stories,” 2026
- Paper360 / TAPPI, “Paper Mills Forge Ahead with Complex Forged Parts,” 2024
Frequently Asked Questions
1. What is the difference between custom steel forged parts and standard forgings?
Standard forgings are produced to generic dimensions and sold from stock. this method are manufactured to a specific customer drawing, with defined dimensions, tolerances, material grade, and mechanical property requirements. Custom parts are produced to print, meaning every specification is buyer-defined rather than catalog-defined. This allows exact fit for the application but requires tooling investment upfront.
2. Which steel grades are most commonly used for custom forged parts?
The most common grades include carbon steels (1018, 1045), alloy steels (4140, 4340), and stainless steels (304, 316, 17-4 PH). Carbon steels offer good strength at low cost. Alloy steels provide higher hardenability and toughness for demanding structural applications. Stainless grades add corrosion resistance for food processing, medical, and marine environments. Grade selection depends on load requirements, environment, and budget.
3. How long does it take to produce custom steel forged parts from a new drawing?
Lead time depends on part complexity, die requirements, and batch size. For new tooling, die fabrication typically adds 2–6 weeks before production begins. Once tooling is qualified, repeat orders can be quoted within 8 hours and shipped within 3 days for small precision parts. Buyers should plan for longer initial lead times when introducing a new part number requiring custom dies.
4. Is cold forging better than hot forging for small precision parts?
For small parts under approximately 38mm diameter in high volumes, cold forging generally delivers better dimensional accuracy, superior surface finish, and lower per-piece cost. The work-hardening effect also increases surface strength. Hot forging is preferred for larger or more complex geometries where the material needs to flow further. The right choice depends on part size, shape complexity, required tolerances, and annual volume.
5. What certifications should I require from a custom steel forged parts supplier?
At minimum, require ISO 9001:2015 for general quality management. For automotive applications, IATF 16949 is the industry standard. Medical device components require ISO 13485:2016. Always request current, dated certificates, not just claims of compliance. Suppliers should also provide material traceability (mill certificates) and First Article Inspection Reports (FAIR) for new part numbers.
6. Can forged steel parts be welded after manufacturing?
Yes. Forged steel behaves similarly to wrought mild steel in welding. For thicker sections or high-alloy grades, pre-heat and post-weld heat treatment are recommended to prevent cracking and maintain weld strength. The dense, refined grain structure of forged steel actually provides a good base for welding, with fewer porosity-related issues than cast parts. Always specify the steel grade to your welding engineer before procedure qualification.
7. What is the minimum order quantity for custom steel forged parts?
Minimum order quantities vary by supplier and part size. Cold forging for small parts typically becomes cost-effective at volumes of 1,000 pieces or more, where tooling cost is amortized across enough units to bring per-piece cost down. Some suppliers accept smaller prototype runs at higher per-piece cost. For high-volume precision parts, batch production runs significantly reduce unit cost compared to low-volume machining from bar stock.
8. How do I find reliable custom steel forged parts manufacturers?
Look for suppliers with verifiable ISO certifications, in-house secondary machining capability, documented quality systems, and a track record in your industry. Request references from customers in similar applications. Evaluate their quoting responsiveness as a proxy for operational efficiency. Suppliers who can return detailed quotes within 8 hours and ship within 3 days typically have the process control and capacity to support demanding production schedules.
Conclusion
this strategy remain one of the most reliable ways to achieve high strength, dimensional consistency, and long service life in demanding applications. The process, whether cold, warm, or hot forging, fundamentally improves steel’s mechanical properties by aligning its grain structure in ways that casting and machining simply can’t replicate.
Choosing the right supplier matters as much as choosing the right process. Verified certifications, in-house secondary machining, documented process control, and fast quoting turnaround are the markers of a supplier you can rely on. Cutting corners on any of these criteria tends to surface as quality escapes or schedule failures later in the supply chain.
MFG SOLUTION specializes in high-precision small machined parts, including cold forged components up to 38mm in diameter, with quotes returned within 8 hours and shipments dispatched within 3 days. Backed by ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, and supported by 60+ engineering professionals with 5-axis CNC machines and cold heading equipment, MFG SOLUTION is built for procurement teams and engineers who need this approach delivered fast, right, and at a cost that makes sense.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: