
2026-05-25
Custom Stainless Steel Forgings: A Complete Guide

| Key Insight | Explanation |
|---|---|
| Forging improves mechanical properties | The forging process aligns the grain structure of stainless steel, producing parts that are stronger and more fatigue-resistant than cast or machined equivalents. |
| ASTM A473 governs specifications | ASTM A473 is the standard specification covering austenitic, ferritic, and martensitic stainless steel forgings for general and high-temperature use. |
| Multiple forging methods exist | Closed die, open die, and cold forging each suit different part geometries, volumes, and tolerance requirements. |
| Grade selection is critical | 304, 316, 410, and 17-4 PH are the most commonly forged stainless grades, each offering distinct corrosion, strength, and heat resistance profiles. |
| Post-forging machining adds precision | CNC turning, milling, and Swiss lathe operations refine forged blanks to tight tolerances, often ±0.01mm or better for small components. |
| Certification matters for regulated industries | Medical, automotive, and aerospace buyers require ISO 9001, ISO 13485, or IATF 16949 certified suppliers to ensure traceability and compliance. |
Custom stainless steel forgings are precision-shaped metal components produced by applying compressive force to stainless steel billets, resulting in parts with superior grain structure, mechanical strength, and corrosion resistance compared to castings or machined bar stock. The process is fully tailored to your geometry, grade, and tolerance requirements. If you’re specifying components for automotive, medical, or industrial applications, understanding how custom stainless steel forgings are designed, produced, and qualified will directly affect your part performance and total cost.
This guide covers everything you need to know: the forging process step by step, material grade selection, key benefits, common sourcing mistakes, and expert best practices for 2026. You’ll also find a detailed FAQ addressing the questions procurement managers and engineers ask most often.
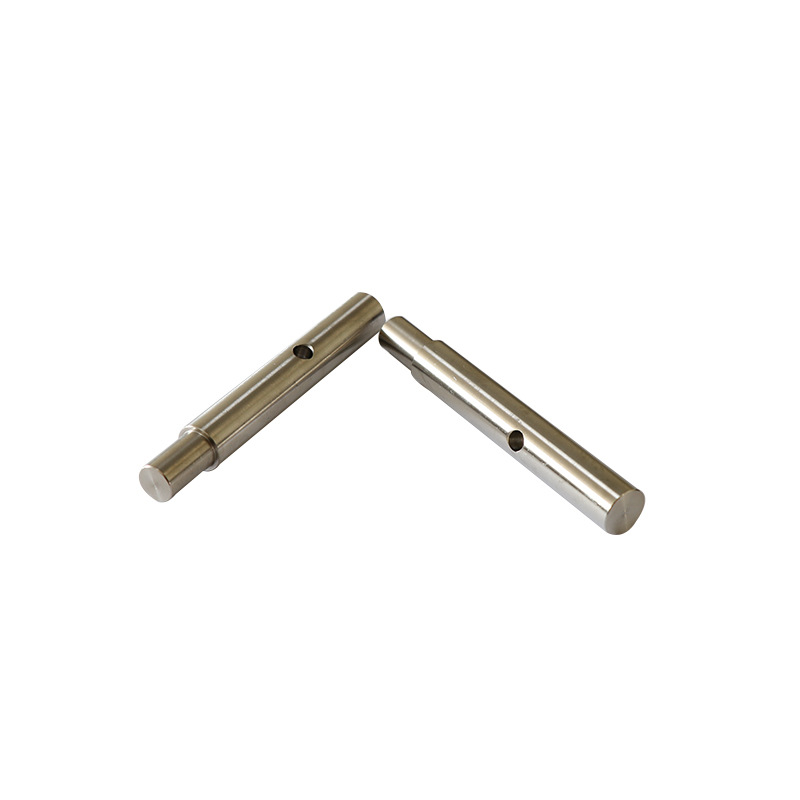
What Are Custom Stainless Steel Forgings?
Custom stainless steel forgings are metal parts shaped to specific customer drawings by pressing or hammering heated or cold stainless steel billets under controlled force. The process refines the internal grain flow of the metal, producing components that outperform cast or machined alternatives in tensile strength, fatigue resistance, and impact toughness.
Definition and Core Characteristics
The term “forging” refers to a metal-forming process where compressive force reshapes a solid metal workpiece rather than melting or cutting it. Stainless steel, an alloy containing a minimum of 10.5% chromium by mass [1], develops a passive oxide layer that resists corrosion. When forged, this already-capable material gains an additional structural advantage: the grain structure aligns with the part’s contour, eliminating the internal voids and porosity common in castings.
According to ASTM A473, the standard specification for stainless steel forgings, the material categories covered include austenitic (e.g., 304, 316), austenitic-ferritic (duplex), ferritic, and martensitic grades [2]. Each category offers a distinct combination of corrosion resistance, hardness, and temperature performance, making grade selection one of the first critical decisions in any forging project.
Why “Custom” Matters
Off-the-shelf forgings exist for standard flanges, fittings, and fasteners. Custom forgings, by contrast, are produced from customer-specific tooling (dies) machined to match your exact part geometry. This matters for three reasons:
- Dimensional accuracy: Custom dies hold tighter dimensional tolerances than standard catalog parts, often within ±0.5mm before final machining.
- Material efficiency: Near-net-shape forging reduces raw material waste compared to machining a complex profile from solid bar stock.
- Performance optimization: The die design controls grain flow direction, which can be oriented to align with the primary stress axis of the finished part.
Industry analysts at IQS Directory note that custom stainless steel forgings serve industries including automotive, oil and gas, aerospace, medical devices, and food processing, where standard parts simply don’t meet application-specific requirements [3].
| Stainless Grade | Type | Key Properties | Common Applications |
|---|---|---|---|
| 304 | Austenitic | Good corrosion resistance, weldable | Food equipment, fasteners, fittings |
| 316 | Austenitic | Superior chloride resistance (Mo added) | Marine, medical implants, chemical processing |
| 410 | Martensitic | High hardness, heat-treatable | Valves, pump shafts, cutlery |
| 17-4 PH | Precipitation hardening | Very high strength, good corrosion resistance | Aerospace fasteners, surgical instruments |
How Custom Stainless Steel Forgings Are Made
this practice are produced through a sequence of controlled steps: billet preparation, heating (for hot forging), die pressing, trimming, heat treatment, and final inspection. Each step directly affects the mechanical properties and dimensional accuracy of the finished part.
The Forging Process Step by Step
- Die design and tooling fabrication: Engineers design closed or open dies based on your part drawing. Closed die forging (also called impression die forging) fully encloses the billet, producing near-net-shape parts with minimal flash [4]. Open die forging suits larger, simpler geometries.
- Billet selection and preparation: The correct stainless grade and billet size are selected. Billet weight is calculated to slightly exceed the finished part volume, accounting for flash and scale loss.
- Heating: For hot forging, stainless steel billets are heated to between 1,000°C and 1,260°C (1,832°F to 2,300°F), depending on grade. Austenitic grades like 304 and 316 require higher forging temperatures than martensitic grades [5].
- Pressing or hammering: The heated billet is placed in the die and struck or pressed. Hydraulic presses, mechanical presses, and hammers are all used. Press tonnage ranges from a few hundred tons for small parts to 50,000+ tons for large aerospace components.
- Trimming and flash removal: Excess material (flash) is trimmed from the part. For precision applications, this step is followed by coining to tighten dimensional tolerances.
- Heat treatment: Solution annealing, quenching, or aging may be applied depending on the grade. 17-4 PH stainless, for example, requires a specific aging cycle to achieve target hardness.
- Post-forging machining: CNC turning, milling, or Swiss lathe operations bring the forged blank to final dimensional tolerances. This is where precision machining partners like MFG SOLUTION add significant value, particularly for small components under 38mm diameter.
- Inspection and testing: Dimensional inspection, hardness testing, tensile testing, and non-destructive evaluation (NDE) confirm conformance to specification before shipment.
Cold Forging vs. Hot Forging for Stainless Steel
Cold forging (performed at or near room temperature) is suitable for smaller stainless steel parts where high dimensional accuracy and excellent surface finish are priorities. The process work-hardens the material, increasing yield strength without heat treatment. Hot forging is preferred for larger, more complex geometries where the material needs to flow into intricate die cavities without cracking.
Pro Tip: For small stainless steel components under 20mm diameter, cold forging (cold heading) often produces a better cost-to-performance ratio than hot forging. The process eliminates scale, reduces post-forging machining time, and delivers consistent grain refinement. Ask your supplier whether cold heading is viable for your part geometry before committing to a hot forging tooling investment.
According to Scot Forge, one of North America’s established forging specialists, the forging process further enhances the properties of stainless steel by improving its mechanical strength, corrosion resistance, and customization possibilities compared to other forming methods [6].
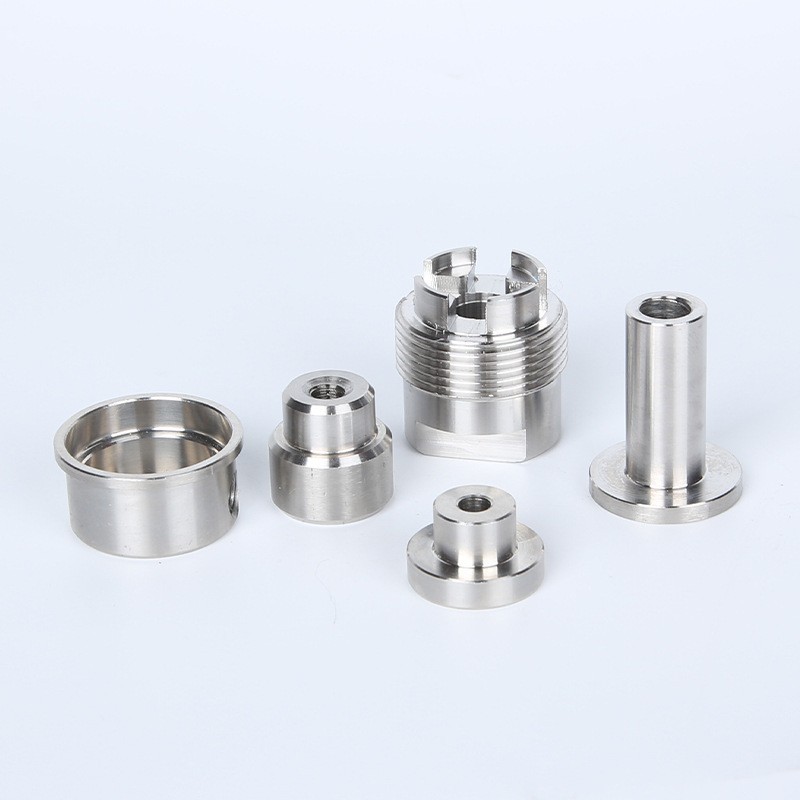
Key Benefits of Custom Stainless Steel Forgings
this method deliver measurably superior mechanical properties, longer service life, and better dimensional repeatability than cast or machined-from-bar alternatives. These advantages directly translate to lower total cost of ownership for high-reliability applications.
Mechanical and Material Advantages
- Higher tensile and yield strength: Forged stainless steel typically achieves 20-30% higher tensile strength than equivalent cast material, because forging eliminates internal porosity and aligns grain flow [7].
- Superior fatigue resistance: The continuous grain structure created during forging resists crack initiation and propagation under cyclic loading, which is critical for automotive and aerospace fasteners.
- Better corrosion resistance: Forging produces a denser, more uniform microstructure. This reduces the surface area available for corrosive attack compared to cast stainless, which may have micro-voids.
- Impact toughness: Forged parts absorb energy more effectively under sudden loading, making them preferred for valve bodies, pump components, and structural hardware in demanding environments.
- Near-net-shape efficiency: Custom dies minimize material removal in downstream machining, reducing cycle time and cutting tool wear.
Commercial and Supply Chain Benefits
- Part consolidation: A single forged component can replace an assembly of welded or fastened parts, reducing assembly time and potential failure points.
- Traceability: Custom forgings produced under ISO 9001:2015 or IATF 16949 quality systems carry full material and process traceability, essential for automotive Tier-1 and medical device supply chains.
- Scalability: Once tooling is amortized, per-part costs drop significantly at volume, making custom stainless steel forgings highly cost-competitive for batch production runs of 500 parts or more.
- Design flexibility: Complex internal contours, undercuts, and integrated features can be forged in a single operation that would require multiple machining setups from bar stock.
A procurement manager at a medical device startup recently shared a real-world example: their team switched from machined 316 bar stock to this strategy for a surgical instrument handle. The result was a 28% reduction in machining time and a part that passed fatigue testing at 2x the required cycle count. Results like this depend on correct grade selection and die design, but they illustrate the genuine performance upside of forging over machining from solid.
For buyers sourcing in 2026, the Producer Price Index for iron and steel forgings tracked by the Federal Reserve Economic Data (FRED) system provides a useful benchmark when evaluating supplier quotes against market pricing trends [8].
Businesses that invest in well-designed packaging for their forged components, particularly for export shipments, also benefit from reduced transit damage. Partners like those offering Custom Packaging solutions can help protect precision parts during international logistics, preserving surface finish and dimensional integrity on delivery.
Pro Tip: When comparing forging quotes, always ask for the material certification (mill cert) and the forging process record alongside the unit price. A lower per-part price from a supplier who can’t provide traceability documentation will cost you more in qualification audits, rework, and potential recalls than the savings justify.
Common Challenges and Mistakes in 2026
this approach present specific technical and commercial challenges that catch buyers off guard, especially those new to forging as a manufacturing method. Knowing the most common pitfalls in advance saves significant time and money.
Technical Challenges
- Work hardening during cold forging: Austenitic stainless grades like 304 and 316 work-harden rapidly. Insufficient intermediate annealing during multi-stage cold forging leads to cracking. Experienced forgers account for this in their process sequence.
- Springback and dimensional variation: Stainless steel’s high yield strength causes more springback than carbon steel. Dies must be designed with compensation offsets to achieve the target geometry after elastic recovery.
- Scale and surface contamination: Hot forging generates iron oxide scale on the surface. If not properly removed by shot blasting or pickling, residual scale can compromise corrosion resistance, particularly on 316L parts for marine or medical use.
- Tooling wear: Stainless steel’s abrasiveness accelerates die wear compared to carbon steel. Premium die materials (H13 tool steel, for example) and proper lubrication are essential for maintaining dimensional consistency across production runs [4].
Common Sourcing Mistakes
- Specifying the wrong grade: A common mistake is defaulting to 304 when 316 is required for chloride environments, or vice versa when cost is the driver. Grade substitution errors are expensive to catch after parts are in service.
- Underestimating tooling lead time: Custom die fabrication typically takes 4-8 weeks. Buyers who budget only for part lead time and ignore tooling time create schedule risk on new product launches.
- Skipping design-for-forgeability review: Parts designed purely for machining often include features (sharp internal corners, extreme aspect ratios, undercuts) that are difficult or impossible to forge. A DFM (design for manufacturability) review with your forging supplier before finalizing drawings prevents costly redesigns.
- Ignoring post-forging machining tolerances: Forging delivers a near-net shape, not a finished dimension. If your drawing calls for ±0.01mm tolerances, you need a precision machining step after forging. Failing to plan for this adds unbudgeted cost and lead time.
In one project we handled at MFG SOLUTION, a client submitted a drawing for a 316 stainless valve body that included a 0.3mm internal radius. The forging supplier flagged it as unachievable without a secondary broaching operation. Catching this in the DFM stage saved approximately three weeks and avoided a tooling rework charge. The lesson: involve your machining partner early in the design cycle.
Best Practices for Sourcing Custom Forgings in 2026
Sourcing the practice successfully requires a structured approach to supplier qualification, specification writing, and quality management. The following practices reflect what high-performing procurement teams do differently from those who struggle with quality escapes and delivery delays.
Supplier Qualification Framework
Not all forging suppliers are equal. Use this checklist when evaluating potential partners:
- Certifications: Confirm ISO 9001:2015 as a baseline. For medical device components, ISO 13485:2016 is required. Automotive applications demand IATF 16949 certification. These aren’t just badges; they represent documented process control, corrective action systems, and audit readiness.
- Material traceability: The supplier must provide mill certificates (MTRs) that trace each forging lot back to the original melt heat. This is non-negotiable for regulated industries.
- In-house testing capability: Suppliers with on-site hardness testing, CMM (coordinate measuring machine) inspection, and tensile testing equipment resolve quality questions faster than those who outsource all testing.
- Post-forging machining capability: A supplier who can forge and finish-machine in one supply chain step reduces handling, lead time, and dimensional risk from part transfer between facilities.
- Engineering support: 60+ engineering professionals, like those at MFG SOLUTION, provide DFM feedback, process optimization, and rapid quoting that smaller shops simply can’t match.
Specification Writing Best Practices
- Reference ASTM A473 explicitly in your drawing notes for stainless steel forgings intended for general or high-temperature service [2].
- Specify the grade designation and condition (e.g., “316L, annealed, per ASTM A473 Grade S31603”).
- Define post-forging heat treatment requirements, surface finish (Ra value), and any NDE requirements (ultrasonic, dye penetrant) on the drawing.
- State dimensional tolerances for forged surfaces separately from machined surfaces. Forged surfaces typically hold ±0.5mm to ±1.0mm; machined surfaces can achieve ±0.01mm with CNC turning or Swiss lathe operations.
- Include a first article inspection (FAI) requirement for new tooling. Per IATF 16949 and AS9100 frameworks, FAI validates that the production process consistently produces conforming parts before full-volume production begins.
At MFG SOLUTION, we’ve found that customers who provide complete drawings with GD&T (geometric dimensioning and tolerancing) callouts receive more accurate quotes and experience fewer revision cycles than those who submit sketches or verbal descriptions. A well-defined drawing is the single most effective way to compress your total sourcing lead time.
Pro Tip: Request a sample or prototype forging before committing to full tooling investment. Many suppliers, including those specializing in cold forging for small parts, can produce trial pieces from existing tooling or soft tooling at lower cost. This lets you validate material properties, surface finish, and dimensional compliance before locking in production dies.
Weldaloy Specialty Forgings notes that open die forged parts and seamless rolled rings in stainless steel offer additional flexibility for larger components where closed die tooling costs are prohibitive [9]. Understanding which forging method fits your part geometry and volume is a key part of the supplier conversation.
Sources & References
- SteelForging.org, “Steel Forging Materials,” 2026
- ASTM International, “A473 Standard Specification for Stainless Steel Forgings,” 2021
- IQS Directory, “Stainless Steel Forging Suppliers Companies,” 2026
- SteelForging.org, “Forging Tooling, Forging Dies,” 2026
- CXI Forging, “Mastering the Art of Forging Stainless Steel: A Comprehensive Guide,” 2026
- Scot Forge, “Stainless Steel Forgings,” 2026
- Walkson, “Forging Stainless Steel: Unveiling the Process and Benefits,” 2026
- Federal Reserve Bank of St. Louis (FRED), “Producer Price Index by Industry: Iron and Steel Forging,” 2026
- Weldaloy Specialty Forgings, “Stainless Steel Forgings,” 2026
Frequently Asked Questions
1. What is the difference between forged and cast stainless steel?
Forged stainless steel is shaped by compressive force applied to a solid billet, which aligns the grain structure and eliminates internal voids. Cast stainless steel is produced by pouring molten metal into a mold, which can introduce porosity and inconsistent grain structure. Forged parts are generally 20-30% stronger and more fatigue-resistant than cast equivalents, making this practice the preferred choice for high-stress, safety-critical applications.
2. Which stainless steel grades are most commonly used for custom forgings?
The most commonly forged stainless grades are 304 (general purpose, food and chemical equipment), 316/316L (marine and medical applications requiring superior chloride resistance), 410 (martensitic, heat-treatable for valves and shafts), and 17-4 PH (precipitation-hardening grade for aerospace and surgical instruments). Grade selection depends on the service environment, required mechanical properties, and applicable standards such as ASTM A473.
3. How long does it take to produce custom stainless steel forgings?
Lead times vary significantly based on part complexity and whether new tooling is required. New die fabrication typically takes 4-8 weeks. Once tooling is proven, production runs of small to medium parts can be completed in 2-4 weeks. Suppliers with in-house cold forging capability and post-forging CNC machining can compress this further. For small stainless components under 38mm diameter, rapid turnaround programs can deliver finished parts in as few as 3 days after tooling qualification.
4. What standard governs stainless steel forgings?
ASTM A473 is the primary standard specification for stainless steel forgings intended for general use and for low- or high-temperature service. It covers austenitic, austenitic-ferritic, ferritic, and martensitic grades. Additional standards may apply depending on the end application: ASME B16.5 for flanges, AMS specifications for aerospace forgings, and ISO 13485 quality system requirements for medical device components.
5. Can custom stainless steel forgings be used in medical devices?
Yes. Stainless grades 316L and 17-4 PH are widely used in surgical instruments, implant components, and medical device housings. Suppliers must hold ISO 13485:2016 certification and provide full material traceability per FDA and EU MDR requirements. Post-forging CNC machining to tight tolerances, combined with passivation treatment, ensures biocompatibility and corrosion resistance in sterilization environments.
6. What is the minimum order quantity for custom stainless steel forgings?
Minimum order quantities depend on the forging method and part size. Cold forging for small components often has lower MOQs (as few as 500-1,000 pieces) because tooling costs are lower than for large hot forging dies. Hot forging for larger parts may require 1,000-5,000 pieces to amortize tooling cost. Always discuss tooling amortization terms with your supplier, as some offer tooling buy-out options that reduce per-part cost at higher volumes.
7. How do I find reliable custom stainless steel forgings manufacturers?
Look for suppliers with ISO 9001:2015 certification as a baseline, plus application-specific certifications (IATF 16949 for automotive, ISO 13485 for medical). Verify that the supplier can provide mill certificates, in-process inspection records, and dimensional reports. Directories like IQS Directory list vetted stainless steel forging suppliers with capability details. For small precision components requiring post-forging machining, suppliers combining cold forging with CNC turning and Swiss lathe capability offer the most integrated and cost-effective solution.
8. What tolerances can be achieved with custom stainless steel forgings?
As-forged dimensional tolerances typically range from ±0.5mm to ±1.5mm depending on part size and die complexity. Post-forging CNC turning or milling can achieve ±0.01mm to ±0.05mm on critical features. Swiss lathe machining of small forged blanks under 38mm diameter can hold tolerances as tight as ±0.005mm on diameter. The combination of forging for structural integrity and precision CNC machining for dimensional accuracy is the standard approach for high-performance this method.
Conclusion
this strategy combine the inherent corrosion resistance of stainless alloys with the structural superiority of the forging process, producing components that consistently outperform cast or machined alternatives in strength, fatigue life, and long-term reliability. The key to a successful forging project is early supplier engagement, correct grade selection referenced to ASTM A473, and a clear specification that distinguishes forged surface tolerances from finish-machined dimensions.
As of 2026, the most competitive sourcing strategies pair a certified forging supplier with a precision machining partner who can take forged blanks to final tolerance in a compressed lead time. That’s exactly where MFG SOLUTION delivers. With ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, 60+ engineering professionals, and the ability to quote within 8 hours and ship within 3 days, we handle the precision machining stage of your this approach with the speed and traceability your supply chain demands. Submit your drawing today and get a detailed quote before tomorrow morning.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: