2026-05-26
Custom Metal Forgings: Strength, Process & Selection

| Key Insight | Explanation |
|---|---|
| Forging Produces Superior Grain Structure | Compressive force aligns the metal’s grain flow to the part’s shape, producing stronger, more fatigue-resistant components than castings or machined bar stock. |
| Multiple Forging Methods Exist | Open-die, closed-die, and cold forging each suit different part sizes, volumes, and tolerance requirements. Choosing correctly drives cost efficiency. |
| Material Choice Is Critical | Steel, aluminum, titanium, and brass are common forging materials. Each offers distinct trade-offs in strength, weight, corrosion resistance, and cost. |
| Certifications Signal Quality | ISO 9001:2015 and IATF 16949 certification at your forging supplier ensures documented process control, traceability, and compliance for automotive and medical applications. |
| Cold Forging Excels for Small Parts | Cold forging at room temperature delivers tight tolerances and excellent surface finish for small precision components, reducing secondary machining costs significantly. |
| Lead Time Varies Widely by Supplier | Traditional forging suppliers quote 4–6 week lead times. Certified rapid-turnaround partners can quote within 8 hours and ship within 3 days for small parts. |
You need 50,000 small steel connectors. They have to handle 200,000 fatigue cycles without cracking. Your current supplier machines them from bar stock, and the reject rate keeps climbing. The answer, in many cases, is custom metal forgings. Custom metal forgings are parts shaped under high compressive force, producing a refined grain structure that machined or cast components simply can’t match. This article covers how forging works, which method fits your application, what mistakes to avoid, and how to find a supplier who won’t add six weeks to your timeline.
What Are Custom Metal Forgings?
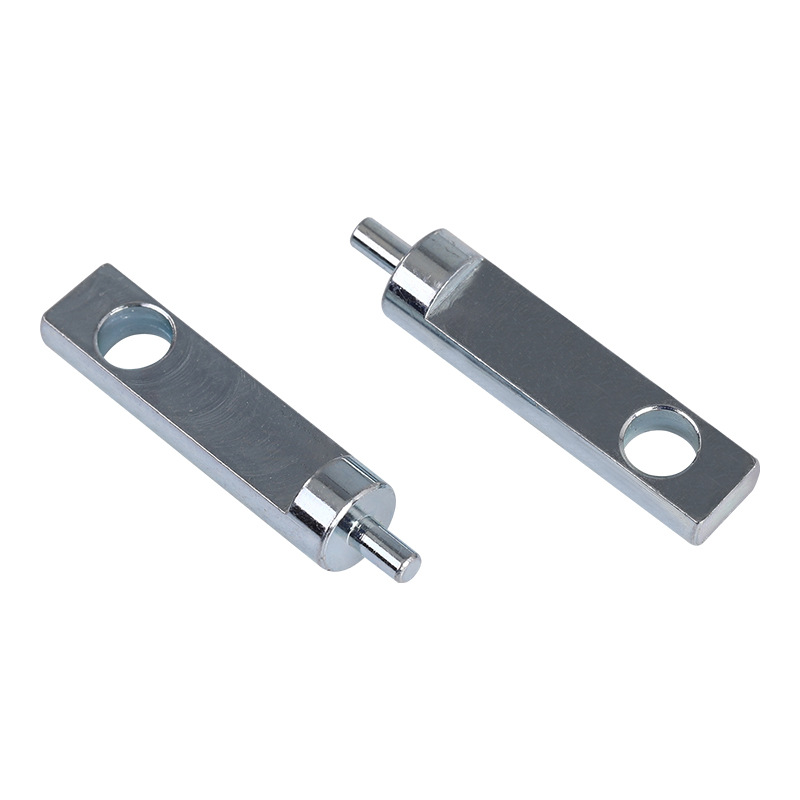
Custom metal forgings are metal parts produced by applying localized compressive forces to a workpiece, shaping it into a specific geometry defined by the customer’s design. The process refines grain structure, eliminates porosity, and delivers mechanical properties that exceed those of equivalent cast or machined parts.
The Core Definition
According to Wikipedia’s engineering reference on forging, forging is a manufacturing process involving the shaping of metal using localized compressive forces, delivered by a hammer or die [1]. The word “custom” means the part geometry, material, and tolerances are specified by the buyer rather than selected from a standard catalog.
This distinction matters. Off-the-shelf forgings are produced in standard shapes and sizes. Custom metal forgings are built to print, meaning every dimension, alloy grade, and surface condition is defined by the customer’s engineering drawing.
Why Industries Rely on Forged Parts
Forged components appear across nearly every demanding industry. The Contract Manufacturing Companies resource on castings and forgings notes that common forged products include automotive crankshafts, bearing caps, axle carriers, valve bodies, turbine housings, splines, and suspension components [2]. Medical implants, aerospace fasteners, and hydraulic fittings are other frequent applications.
The reason is straightforward. Forging produces a continuous, unbroken grain flow aligned to the part’s shape. This gives forged parts higher tensile strength, better fatigue resistance, and greater impact toughness compared to castings of the same material [1]. For safety-critical parts, that’s not a nice-to-have. It’s a requirement.
- Automotive: Crankshafts, connecting rods, gear blanks, steering knuckles
- Aerospace: Structural brackets, landing gear components, turbine discs
- Medical: Orthopedic implant components, surgical instrument handles
- Industrial: Flanges, rings, valves, hydraulic fittings
- Electronics: Heat sinks, connector bodies, precision housings
Pro Tip: Before specifying a forged part, confirm that the strength improvement justifies the tooling cost. For low-stress components produced in small volumes, machining from bar stock may be more economical. Forging’s advantages are most pronounced in high-cycle, high-load, or safety-critical applications.
How Custom Metal Forgings Work
Custom metal forgings are produced by heating or pressing metal into a die cavity under controlled force, then finishing the part to final dimensions through trimming, heat treatment, and machining as needed.
The Main Forging Methods
Three primary methods cover the vast majority of custom forging applications. Each has a distinct operating principle, cost profile, and part-size range.
- Open-Die Forging: The workpiece is shaped between flat or simple-contour dies without enclosing it completely. This suits very large parts. R&M Forge produces open-die forgings up to 250 inches in diameter and 50,000 pounds [3]. Material utilization is lower, and secondary machining is typically required.
- Closed-Die (Impression-Die) Forging: The metal is pressed into a die cavity that defines the final shape. Trinity Forge describes closed-die forging as the standard for built-to-print components where dimensional consistency across high volumes is essential [4]. Tooling costs are higher, but per-part costs drop significantly at volume.
- Cold Forging: Metal is shaped at or near room temperature, without preheating. This method produces excellent surface finish and tight dimensional tolerances, making it ideal for small precision parts. Material hardness increases through work hardening, which can eliminate additional heat treatment steps.
The Step-by-Step Production Sequence
- Design & Tooling: The customer’s CAD drawing is reviewed for forgeability. Die geometry is designed, and tooling is machined.
- Material Selection & Preparation: Billet or bar stock is cut to the correct weight. For hot forging, the billet is heated to forging temperature (typically 1,100–1,250°C for steel).
- Forging: The heated or cold billet is placed in the die and struck or pressed to shape. Multiple blows or press strokes may be required.
- Trimming: Flash (excess material squeezed out of the die) is removed by a trimming die or CNC machining.
- Heat Treatment: Normalizing, annealing, or quench-and-temper cycles are applied to achieve the specified mechanical properties.
- Finishing & Inspection: Parts are machined to final tolerances, surface-treated if required, and inspected against the engineering drawing.
| Method | Typical Part Size | Tolerance Range | Best For |
|---|---|---|---|
| Open-Die Forging | Large (up to 50,000 lbs) | ±1.5 mm or more | Low-volume, large structural parts |
| Closed-Die Forging | Small to medium (grams to ~50 kg) | ±0.2–0.5 mm | High-volume, complex geometry |
| Cold Forging | Small (under 38 mm typical) | ±0.05–0.1 mm | Precision small parts, high volume |
| Rolled Ring Forging | Rings up to 250″ diameter | ±0.5–2.0 mm | Flanges, bearings, pressure vessels |
Key Benefits of Custom Metal Forgings
Custom metal forgings deliver higher mechanical strength, better fatigue life, and reduced material waste compared to cast or machined alternatives, making them the preferred choice for load-bearing and safety-critical components.
Mechanical and Structural Advantages
The grain refinement produced by forging is the primary mechanical advantage. According to the U.S. International Trade Commission’s competitive assessment of the forging industry, forged components consistently outperform cast equivalents in tensile strength, yield strength, and impact resistance [5]. This is why crankshafts, axles, and connecting rods are forged rather than cast in virtually every automotive application.
Industry analysts note that forged steel parts can achieve tensile strengths 20–30% higher than equivalent castings, depending on alloy and processing conditions. That difference translates directly into longer service life, lower warranty costs, and the ability to design lighter parts that still meet load requirements.
- Superior fatigue resistance: Continuous grain flow resists crack initiation and propagation under cyclic loading.
- No internal porosity: Unlike castings, forgings have no voids or shrinkage defects that weaken the part.
- Consistent mechanical properties: Every part in a production run has the same grain structure and properties.
- Better surface integrity: Cold forging in particular produces a work-hardened surface that resists wear.
Economic and Supply Chain Benefits
Tengco’s forging resource points out that custom metal forging yields parts that are strong enough to eliminate the need for expensive high-alloy materials [6]. A standard carbon steel forging can replace a more costly alloy steel casting while meeting the same performance specification. That’s real cost reduction, not a marketing claim.
Material utilization is another factor. Cold forging, in particular, produces near-net-shape parts with minimal machining allowance. Less scrap means lower material cost per part. For high-volume production runs of small components, this compounds quickly.
A procurement manager at an electronics connector manufacturer recently shared that switching from machined bar stock to cold forgings for a brass terminal reduced per-part cost by 18% at a volume of 200,000 pieces annually. The savings came from reduced machining time and lower scrap rates, not from compromising on quality.
Pro Tip: When evaluating forging versus machining, calculate total cost of ownership rather than just piece price. Include material scrap rates, secondary machining operations, heat treatment, and expected reject rates. Cold forging often wins at volumes above 10,000 pieces even when the initial tooling cost seems high.
For businesses that need customer support during the quoting or design-for-manufacturability phase, working with suppliers who offer dedicated Customer Support resources can significantly reduce specification errors and rework costs before production begins.
Common Challenges and Mistakes to Avoid
The most common mistakes in custom metal forging projects involve incorrect method selection, inadequate die design review, and underestimating the lead time required for tooling fabrication.
Design and Specification Errors
One pitfall to watch for is specifying tolerances tighter than the forging process can reliably hold. Closed-die forging typically holds ±0.2–0.5 mm. If your drawing calls for ±0.05 mm on a forged surface, you’re paying for secondary machining whether you planned for it or not. Align your tolerance callouts with the process capability from the start.
Another common mistake is designing parts with undercuts or re-entrant features that are impossible to release from a forging die. In practice, a design-for-forgeability (DFF) review before tooling is cut saves significant rework cost. Most experienced forging suppliers offer this review as part of the quoting process. If yours doesn’t, that’s a red flag.
GL Forge, with over six decades of custom metal forging experience, emphasizes that die design is where most project problems originate [7]. Draft angles, parting line placement, and fillet radii all affect whether the part releases cleanly and whether die life is acceptable.
Supplier and Quality Risks
Not all forging suppliers are equal in process control. The USITC forging industry assessment notes that quality consistency is a persistent differentiator between certified and uncertified suppliers [5]. Suppliers operating without ISO 9001:2015 or IATF 16949 certification may lack the documented process controls needed to guarantee repeatability across production runs.
- Inconsistent heat treatment: Inadequate temperature control produces parts that don’t meet hardness or tensile specifications.
- Die wear not monitored: As dies wear, dimensional variation increases. Without statistical process control (SPC), this goes undetected until parts fail incoming inspection.
- Material traceability gaps: For medical and automotive applications, material certificates and heat number traceability are mandatory. Confirm this before placing an order.
- Overlooking post-forging machining: Many forged parts require CNC finishing to achieve final dimensions. Budget for this in your cost model.
From experience, a medical device startup once sourced forged titanium housings from a supplier without ISO 13485:2016 certification. The parts passed dimensional inspection but failed biocompatibility documentation requirements during an FDA audit. The project was delayed by four months while a certified supplier was qualified. Certification isn’t bureaucracy. It’s risk management.
Best Practices for Sourcing Custom Forgings in 2026
Sourcing this approach effectively in 2026 requires aligning your part requirements with the right forging method, verifying supplier certifications, and building rapid-iteration capability into your supply chain.
Selecting the Right Process and Supplier
Start with your part’s geometry, volume, and mechanical requirements. Small parts under 38 mm in diameter with tight tolerances and volumes above 10,000 pieces are strong candidates for cold forging. Larger structural components with complex geometry suit closed-die hot forging. Very large, low-volume parts go to open-die forging. Getting this decision right before tooling is cut saves substantial cost.
According to Modern Group’s forging resource, suppliers with over 100 years of combined experience bring pattern recognition that prevents common design mistakes before they become production problems [8]. Look for suppliers who ask detailed questions about your application, not just your drawing dimensions.
As of 2026, the global forging market is increasingly segmented between suppliers who offer digital quoting and rapid turnaround and those who still operate on 4–6 week lead times. Ensun’s 2026 directory of custom metal forging manufacturers lists over 100 active suppliers globally, reflecting a competitive market where buyers have real choice [9].
Quality Assurance Framework
At MFG SOLUTION, we’ve found that buyers who specify their quality requirements upfront, including required certifications, inspection methods, and documentation, consistently receive better outcomes than those who address quality after production begins. Build your quality requirements into your RFQ, not your rejection procedure.
- Require ISO 9001:2015 certification as a minimum for any production forging supplier.
- For automotive parts, require IATF 16949 certification and an approved supplier audit.
- For medical components, require ISO 13485:2016 and material traceability to heat number.
- Request first-article inspection (FAI) reports before approving production quantities.
- Specify statistical process control (SPC) requirements for critical dimensions on high-volume runs.
Laube’s the practice resource describes a best-practice approach where the supplier partners with the client from ideation to final delivery, producing forgings that exceed expectations through early design involvement [10]. This collaborative model reduces late-stage engineering changes, which are the most expensive kind.
Pro Tip: Request a design-for-manufacturability (DFM) review before finalizing your forging drawing. A good supplier will flag draft angle issues, wall thickness problems, and tolerance conflicts before tooling is cut. This 30-minute conversation can save weeks of rework and thousands in tooling revisions.
Our team at MFG SOLUTION recommends that buyers sourcing small forged parts also evaluate whether cold forging combined with CNC finishing can meet their requirements. This combination often delivers the tight tolerances of machining with the material strength of forging, at a lower total cost than either process alone for volumes above 5,000 pieces.
Sources & References
- Wikipedia, “Forging,” 2026
- Contract Manufacturing Companies, “Casting and Forgings,” 2026
- R&M Forge, “Custom Metal Forgings Manufacturer,” 2026
- Trinity Forge, “Custom Forging,” 2026
- U.S. International Trade Commission, “Competitive Assessment of the U.S. Forging Industry,” 2026
- Tengco, “Custom Forging Hot-Formed Metal Parts,” 2026
- GL Forge, “Custom Metal Forging Services,” 2026
- Modern Group, “Custom Metal Forging Services,” 2026
- Ensun, “Top 100 Custom Metal Forging Manufacturers in 2026,” 2026
- Laube, “Custom Metal Forgings: Delivering Strength,” 2026
Frequently Asked Questions
1. What are custom metal forgings used for?
this practice are used in automotive (crankshafts, connecting rods, steering components), aerospace (structural brackets, turbine discs), medical (implant components, instrument handles), and industrial applications (flanges, valves, hydraulic fittings). Any application requiring high fatigue strength, impact resistance, or structural integrity is a strong candidate for forged components rather than cast or machined alternatives.
2. How do custom metal forgings differ from castings?
Forgings are shaped by compressive force, which refines the metal’s grain structure and eliminates internal porosity. Castings are produced by pouring molten metal into a mold, which can introduce voids, shrinkage defects, and a coarser grain structure. As a result, this method typically offer 20–30% higher tensile strength and significantly better fatigue life than equivalent castings of the same material.
3. What materials can be used in custom metal forgings?
The most common materials are carbon steel, alloy steel, stainless steel, aluminum, titanium, and brass. Carbon and alloy steels dominate automotive and industrial applications. Aluminum forgings are preferred where weight reduction is critical. Titanium is used in aerospace and medical implants. Brass and copper alloys suit electrical connectors and plumbing fittings. Material choice affects forging temperature, die wear, and final mechanical properties.
4. What tolerances can custom metal forgings achieve?
Tolerance capability depends on the forging method. Open-die forgings typically hold ±1.5 mm or more and require secondary machining for precision features. Closed-die forgings achieve ±0.2–0.5 mm. Cold forging delivers the tightest tolerances, typically ±0.05–0.1 mm, making it suitable for small precision parts where minimal secondary machining is desired. Final CNC finishing after forging can achieve tolerances tighter than ±0.01 mm where required.
5. How long does it take to produce custom metal forgings?
Lead time depends on part complexity, volume, and supplier capability. Tooling fabrication for closed-die or cold forging typically takes 3–6 weeks. Once tooling is approved, production runs of small parts can be completed in days. Some rapid-turnaround suppliers can quote within 8 hours of receiving a specification and ship completed small forged parts within 3 days for standard geometries. Traditional suppliers often quote 4–6 week total lead times.
6. Is cold forging better than hot forging for small precision parts?
For small parts under 38 mm in diameter, cold forging generally offers better dimensional accuracy, superior surface finish, and work-hardened surfaces without a separate heat treatment step. Hot forging is better suited to larger, more complex geometries where the material needs to be softened for shaping. Results may vary depending on material type and part geometry, so a DFM review with your supplier is the best way to confirm the right method.
7. What certifications should a custom forging supplier have?
At minimum, look for ISO 9001:2015 certification, which confirms a documented quality management system. For automotive parts, IATF 16949 is required by most OEMs and Tier-1 suppliers. For medical device components, ISO 13485:2016 ensures compliance with medical manufacturing standards. Suppliers holding all three certifications offer the broadest compliance coverage and the most rigorous process documentation, which is essential for regulated industries.
8. Can custom metal forgings be combined with CNC machining?
Yes, and this combination is very common. Forging produces the near-net shape and the superior grain structure; CNC machining then achieves final dimensional tolerances, threaded features, and surface finishes that forging alone cannot deliver. For small precision parts, cold forging followed by CNC turning or Swiss lathe finishing often delivers the best combination of mechanical strength, dimensional accuracy, and cost efficiency at production volumes.
Conclusion
this strategy remain one of the most reliable ways to produce strong, fatigue-resistant metal parts at scale. The process delivers mechanical properties that casting and machining from bar stock simply can’t replicate, and the economics improve significantly at production volumes where tooling costs are amortized across many parts.
Choosing the right forging method, material, and supplier is where most projects succeed or fail. Cold forging excels for small precision parts. Closed-die forging suits complex geometries at high volume. Certification matters more than price for regulated industries. And lead time is no longer an acceptable excuse: suppliers with modern quoting systems and production infrastructure can turn around small forged parts far faster than the industry’s historical 4–6 week standard.
MFG SOLUTION specializes in cold forging and precision CNC finishing for small parts up to 38 mm in diameter. We hold ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, employ 60+ engineering professionals, and operate advanced cold heading equipment alongside 5-axis CNC machines. We quote within 8 hours and ship within 3 days. If you’re sourcing this approach and need a certified, rapid-turnaround partner, MFG SOLUTION is built for exactly that.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: