
2026-05-03
CNC Threading Services: A Complete Guide for 2026

| Key Insight | Explanation |
|---|---|
| Three primary threading methods | CNC threading services use tapping, thread milling, or single-point turning depending on part geometry, material, and tolerance requirements. |
| Cost range in 2026 | Threading costs typically add $5–$40 per part depending on thread size, material, method, and batch volume. High-volume runs significantly reduce per-part cost. |
| Thread milling vs. tapping | Thread milling offers greater flexibility and is safer in hard materials; tapping is faster and more cost-effective for standard thread sizes in softer materials. |
| Quality standards matter | ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications ensure threading quality for medical, automotive, and electronics applications. |
| Internal vs. external threads | Both thread types serve distinct fastening functions; internal threads (nuts, bores) and external threads (bolts, studs) require different tooling and programming approaches. |
| Rapid turnaround is achievable | Specialized CNC machining suppliers can quote within 8 hours and ship precision-threaded parts within 3 days for qualifying batch sizes. |
Precision-threaded parts hold the modern manufacturing world together, quite literally. CNC threading services are the process of using computer-controlled machine tools to cut, mill, or form helical grooves (threads) into a workpiece, enabling reliable mechanical fastening and assembly. The method delivers consistent geometry, tight tolerances, and repeatability that manual threading simply can’t match. Whether you’re sourcing connectors for medical devices, fasteners for automotive assemblies, or fittings for electronics enclosures, understanding how CNC threading services work will help you specify parts correctly, control costs, and avoid costly rework.
This guide covers every major aspect: the core methods, practical benefits, real-world challenges, 2026 best practices, and honest answers to the questions engineers and procurement managers ask most often.
What Is CNC Threading?
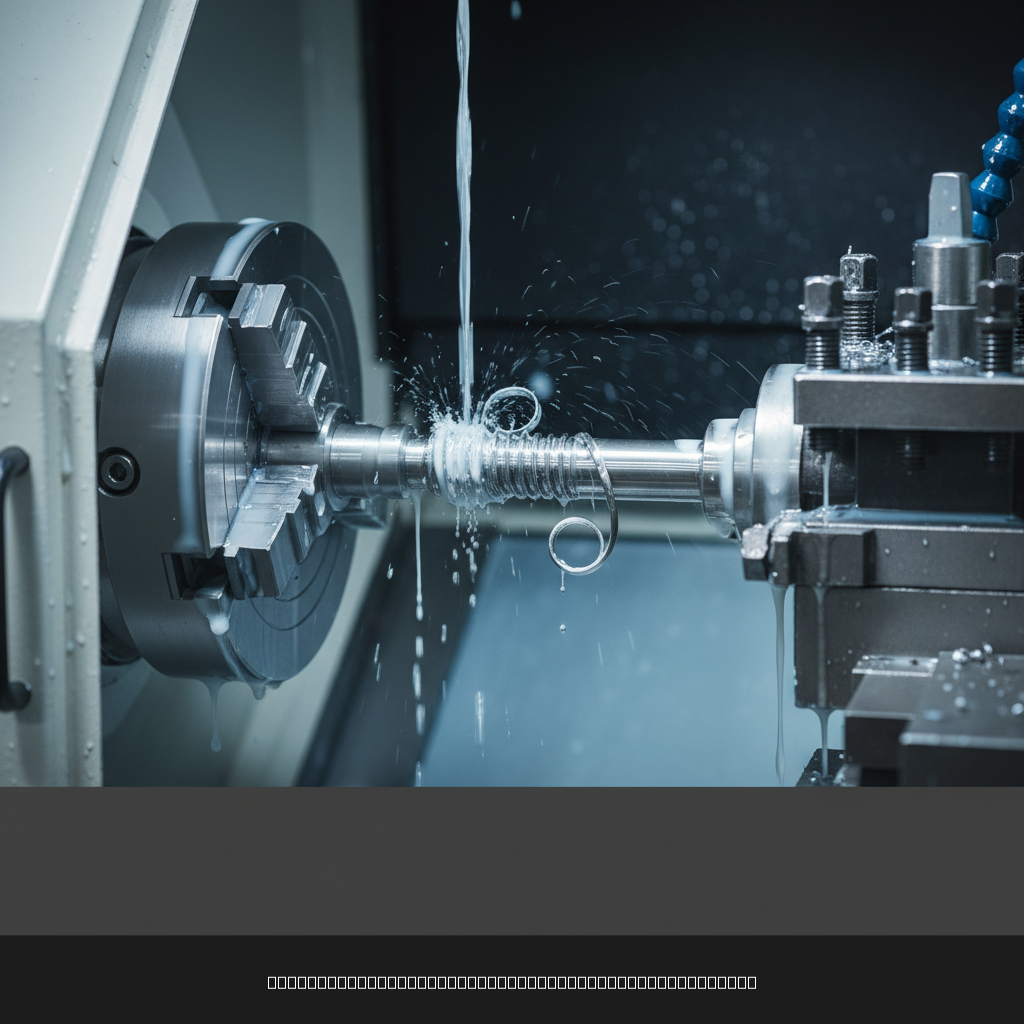
CNC threading services use computer-controlled lathes, mills, or dedicated threading machines to produce accurate helical grooves on cylindrical or conical workpieces. The process is programmable, repeatable, and capable of holding tolerances tighter than ±0.01mm on thread pitch diameter.
Definition and Core Concepts
A thread is a continuous helical ridge wrapped around a cylinder (external thread) or cut inside a bore (internal thread). Threads serve one primary function: converting rotational motion into linear clamping force. That’s why they appear in everything from M2 screws in smartphone housings to 2-inch NPT fittings in industrial pipelines.
CNC threading differs from manual threading in one critical way: the machine’s controller synchronizes spindle rotation with axial tool movement to the exact pitch specified in the part program. There’s no reliance on operator feel or hand pressure. According to PartMFG’s guide to CNC threading, the process encompasses tapping, thread milling, single-point turning, and thread rolling, each suited to different materials and geometries [1].
Why Thread Geometry Matters
Thread geometry is defined by several parameters that engineers must specify correctly:
- Pitch: The distance between adjacent thread crests, measured in millimeters (metric) or threads per inch (imperial)
- Major diameter: The largest diameter of the thread, used for nominal size designation
- Minor diameter: The smallest diameter, which determines root strength
- Thread angle: Typically 60° for unified (UN) and metric (M) threads, 55° for Whitworth (BSW)
- Thread class: Fit tolerance designation (e.g., 6H/6g for metric, 2A/2B for unified) defining how tightly mating parts fit together
- Lead: The axial distance traveled per full rotation, relevant for multi-start threads
Getting these parameters right before machining prevents the most expensive outcome in threading: a part that fails gauge inspection and must be scrapped. As noted by Protolabs’ design guide for CNC machined parts, thread callouts in CAD files must match the machining method to avoid ambiguity during quoting and production [2].
| Thread Standard | Common Uses | Angle | Designation Example |
|---|---|---|---|
| Metric (ISO) | Electronics, automotive, general industrial | 60° | M8×1.25 |
| Unified (UNC/UNF) | Aerospace, North American industrial | 60° | 1/4-20 UNC |
| NPT (Pipe) | Fluid/gas fittings, oilfield | 60° | 1/2-14 NPT |
| ACME / Trapezoidal | Lead screws, power transmission | 29° / 30° | 3/4-6 ACME |
| Whitworth (BSW/BSP) | UK industrial, hydraulic fittings | 55° | G1/4 BSP |
How CNC Threading Works: Processes and Methods
CNC threading is performed through four main methods: single-point turning, tapping, thread milling, and thread rolling. Each method uses different tooling and machine motion to produce threads, and the right choice depends on material, thread size, batch size, and required accuracy.
The Four Core Threading Methods
Understanding each method helps you specify parts correctly and avoid over-engineering your threading requirements.
- Single-point thread turning: A single-point cutting tool mounted on a CNC lathe traces the helical path of the thread in multiple passes. The controller synchronizes spindle RPM with Z-axis feed to achieve the specified pitch. This method excels for large-diameter external threads and custom thread profiles. It’s commonly used for ACME, stub ACME, and API pipe threads.
- Tapping (rigid tapping): A tap, a fluted cutting tool shaped like the finished thread, is driven into a pre-drilled hole at a feed rate exactly matching the thread pitch. Modern CNC machining centers use synchronized spindle-feed tapping (often called rigid tapping) to eliminate the need for a floating tap holder. Tapping is fast and economical for standard metric and unified threads in aluminum, brass, and mild steel. According to eMachineShop’s CNC threading resource, tapping remains the most common method for internal threads in production runs [3].
- Thread milling: A multi-tooth thread mill follows a helical interpolation path around the bore or OD. The cutter rotates on its own axis while the machine interpolates the circular path. Thread milling works in virtually any material, including hardened steels above 50 HRC, and produces excellent surface finish. It also allows one tool to cut multiple thread sizes by adjusting the interpolation diameter.
- Thread rolling (form threading): A hardened roll die displaces material radially to form threads without cutting. No chips are produced. The result is a stronger thread with better fatigue resistance because the grain structure flows along the thread profile rather than being severed. Thread rolling is standard for high-volume fastener production and is frequently used in Swiss lathe operations for small-diameter parts.
The Purdue University Fabrication Lab notes that CNC lathes are recommended for turning, grooving, O.D. and I.D. threading, drilling, and knurling, confirming the versatility of CNC turning platforms for threading operations [4].
Machine Types Used for CNC Threading
Different machine platforms support different threading methods:
- CNC turning centers: Ideal for external and internal threads on rotational parts; single-point turning and live-tool tapping are standard
- Swiss-type CNC lathes: Excellent for small-diameter parts (under 32mm); the guide bushing provides superior rigidity for fine-pitch threads on long, slender parts
- CNC machining centers (mills): Used for thread milling and tapping in prismatic parts; 5-axis machines can thread on compound angles
- Dedicated thread rolling machines: High-volume production of cold-formed external threads on fasteners and connectors
Pro Tip: For small-diameter parts under 20mm with fine-pitch threads (e.g., M3×0.5 or M4×0.7), specify thread milling or Swiss lathe single-point turning rather than tapping. Tap breakage in small bores is a leading cause of part scrap and production delays, especially in stainless steel and titanium.
Key Benefits of Professional CNC Threading Services
Professional CNC threading services deliver tighter tolerances, higher repeatability, and broader material capability than manual or semi-automated threading, making them the preferred choice for precision assemblies in demanding industries.
Precision, Repeatability, and Compliance
The core advantage of CNC threading is consistency. Every part in a batch receives the same programmed thread geometry, regardless of whether you’re running 50 pieces or 50,000. That consistency is critical for assembly-line production where mating parts from different suppliers must fit together without adjustment.
- Tolerance control: CNC threading routinely holds pitch diameter tolerances within ±0.005mm for metric fine threads, far tighter than manual die threading
- Surface finish: Thread milling and single-point turning produce Ra values of 0.8–1.6 µm on thread flanks, ensuring reliable sealing in fluid fittings
- Material versatility: CNC threading works across aluminum, brass, stainless steel, titanium, Inconel, PEEK, and engineering plastics. Ehren-Haus Industries highlights that specialized CNC threading services extend to custom plastic parts for industrial applications [5]
- Thread form variety: From standard M2 micro-threads in electronics to large-diameter API oilfield connections, CNC threading services handle the full range
- Traceability: ISO 9001:2015-certified shops document every operation, providing audit trails that medical and automotive customers require
Industry analysts consistently note that certified CNC threading services reduce assembly reject rates compared to manually threaded parts. Research from quality management literature suggests that process-controlled CNC threading can reduce thread-related non-conformances by 60–80% compared to manual methods, depending on the thread class and material.
Economic Advantages at Scale
Cost efficiency improves substantially with volume. CNC threading services amortize setup costs across the batch, so per-part threading cost drops sharply as quantities increase.
- Setup time for a standard tapping operation on a CNC turning center: 15–30 minutes
- Cycle time per thread (M6 internal, 10mm deep, aluminum): typically under 8 seconds with rigid tapping
- Thread rolling on a Swiss lathe adds minimal cycle time for external threads on turned parts
- Combining threading with turning in a single setup eliminates secondary operations and reduces handling cost
At MFG SOLUTION, we’ve found that integrating threading into our CNC turning and Swiss lathe operations, rather than treating it as a secondary process, typically reduces total part cost by 15–25% for small precision components. Our 60+ engineering professionals review each job to select the most economical threading method before quoting.
Pro Tip: Always request that threading be performed in the same setup as turning or milling when possible. Repositioning a part for a secondary threading operation introduces datum shift errors and adds cost. A capable CNC turning center or Swiss lathe can complete both operations in one clamping.
Common Challenges and Mistakes in CNC Threading
CNC threading failures typically stem from incorrect tool selection, inadequate thread design, or poor material-method matching. Recognizing these pitfalls before production starts saves significant time and money.
Design and Specification Errors
The most common mistake engineers make is under-specifying threads on drawings. A callout that simply reads “M6 thread” leaves the machinist guessing about thread class, depth, and whether a through or blind hole is intended. In practice, incomplete callouts cause quoting delays and, worse, parts that pass visual inspection but fail functional assembly.
Common specification mistakes include:
- Omitting thread class (tolerance grade), leading to loose or tight fits that cause assembly problems
- Specifying thread depth too shallow, resulting in insufficient thread engagement for the required clamp load
- Calling out a thread standard that doesn’t match the mating component’s country of manufacture (e.g., mixing metric and unified threads in the same assembly)
- Placing threaded holes too close to part edges, leaving insufficient wall thickness and risking thread stripping
- Requesting fine-pitch threads in materials prone to galling, such as austenitic stainless steel, without specifying a thread lubricant or surface treatment
According to Protolabs’ threading design guide, engineers should always specify the thread standard, class, major diameter, pitch, and minimum thread depth on the drawing or in the 3D model’s PMI (Product and Manufacturing Information) annotations [2].
Tooling and Process Mistakes
Even with correct specifications, process errors cause threading failures. A precision machining client we worked with recently submitted a batch of M3×0.5 stainless steel connectors with blind holes. Their previous supplier had used standard taps, which broke repeatedly in the blind holes due to chip packing. Switching to a spiral-flute tap with through-coolant and a 20% reduction in tap engagement depth solved the problem entirely.
Other process-level pitfalls:
- Incorrect cutting speed: Too fast causes tap breakage; too slow produces poor surface finish and built-up edge on the tool
- Insufficient coolant: Threading generates concentrated heat at the tool tip; inadequate coolant accelerates tool wear and degrades thread surface finish
- Wrong tap geometry for the material: Spiral-point taps work well in through-holes; spiral-flute taps are required for blind holes to evacuate chips upward
- Skipping thread gauging: Not every part needs to be gauged, but statistical sampling with go/no-go gauges is mandatory for production runs destined for automotive or medical assemblies
GBF Enterprises, specialists in precision thread cutting for over 40 years, emphasizes that matching the tap geometry to both the material and the hole type (through vs. blind) is the single most impactful decision in preventing tap breakage [6].
Best Practices for CNC Threading Services in 2026
As of 2026, the best CNC threading operations combine digital process control, smart tooling, and supplier qualification standards to deliver zero-defect threaded parts consistently and cost-effectively.
Process Control and Quality Frameworks
The most reliable threading results come from shops that treat threading as a controlled process, not just a machining step. Best-in-class CNC threading services apply the following practices:
- Define thread specifications completely in the CAD model or drawing, including standard, class, depth, and surface finish requirement. Use ISO 286 for metric fits and ASME B1.13M for metric thread tolerances.
- Select the threading method based on material hardness and hole type. Use thread milling for hardened materials above 45 HRC, spiral-flute tapping for blind holes in softer materials, and thread rolling for external threads on high-volume production parts.
- Validate tool life limits and enforce tool change intervals. Worn taps and thread mills produce oversized or undersized threads before they visibly fail. Setting a maximum number of holes per tool based on material and thread size prevents this.
- Use in-process gauging or probing where cycle time allows. On modern CNC turning centers, in-spindle probing can verify thread depth and position without removing the part from the chuck.
- Implement first-article inspection (FAI) per AS9102 or PPAP (Production Part Approval Process) for automotive parts. FAI documents confirm that the first part produced matches the drawing before the full batch runs.
- Maintain traceability records for medical and automotive parts. ISO 13485:2016 and IATF 16949 both require documented evidence that threading parameters were within specification for every production lot.
The Energy Technology Manufacturing and Threading (ETMT) facility demonstrates how advanced CNC equipment and rigorous process control enable premium threading services across demanding oilfield applications, a model applicable to any high-stakes threading environment [7].
Supplier Selection Criteria for 2026
Choosing a CNC threading services provider requires evaluating more than just price. Consider these criteria:
- Certifications: ISO 9001:2015 is the baseline. For medical parts, require ISO 13485:2016. For automotive, require IATF 16949. These certifications mean every step is tracked, documented, and auditable for compliance.
- Equipment capability: Confirm the supplier has live-tool turning centers or Swiss lathes for small-diameter parts, and 5-axis capability if your parts have compound-angle threaded features
- Turnaround time: Suppliers who can quote within 8 hours and ship within 3 days for standard batch sizes provide a meaningful supply chain advantage over shops with 3–6 week lead times
- Engineering support: A supplier with 60+ engineering professionals on staff can identify design-for-manufacturability (DFM) issues before cutting starts, preventing costly revisions
- Gauge inventory: Confirm the supplier stocks go/no-go gauges for the thread standards you use, including metric, unified, pipe, and any special profiles
As noted in Metoree’s 2026 review of threading service companies, the top providers combine CNC Swiss machining, thread rolling, and turning in a single facility to minimize handling and reduce lead time [8].
Pro Tip: When evaluating a new CNC threading services supplier, request a sample run of 10–20 parts before committing to a full production order. Measure thread pitch diameter, minor diameter, and surface finish against your drawing callouts. A supplier confident in their process will welcome this step, not resist it.
Sources & References
- PartMFG, “What Is CNC Threading? Types of Threading Processes,” 2026
- Protolabs, “A Guide to Adding Threading to CNC Machined Parts,” 2026
- eMachineShop, “CNC Threading,” 2026
- Purdue University Fabrication Lab, “CNC Lathe Details,” 2026
- Ehren-Haus Industries, “Plastic Threading and CNC Threading Services,” 2026
- GBF Enterprises, “Precision Thread Cutting,” 2026
- ETMT, “The Most Diverse Range of Oilfield Threading Services,” 2026
- Metoree, “15 Threading Service Companies in 2026,” 2026
- Vescio Manufacturing, “Thread Cutting & Grinding,” 2026
- Beta Manufacturing, “Precision CNC Machining,” 2026
Frequently Asked Questions
1. How much does CNC service cost?
CNC machining service costs vary widely based on machine type, part complexity, material, and batch size. As of 2026, hourly machine rates range from $50–$80 for standard CNC turning to $150–$300 per hour for 5-axis machining centers. For most small precision parts in production quantities, per-part costs fall between $2 and $50. High-volume runs, tight tolerances, and difficult materials all push costs higher. Suppliers offering rapid quoting within 8 hours help you compare options quickly without committing to a full RFQ cycle.
2. Can CNC do threads?
Yes. CNC threading services produce both internal and external threads using four main methods: single-point turning on CNC lathes, rigid tapping on machining centers, thread milling via helical interpolation, and thread rolling for cold-formed external threads. Each method suits different materials, thread sizes, and production volumes. CNC threading achieves tighter tolerances and better repeatability than manual methods, making it the standard for precision assemblies in automotive, medical, and electronics manufacturing.
3. What is the average cost of CNC threading?
For machined metal parts, CNC threading typically adds $5–$40 per part depending on thread size, material, method, and batch volume. A standard M6 tapped hole in aluminum adds minimal cost (under $2 per part at volume), while a custom ACME thread in stainless steel on a one-off part may add $30–$60. Thread rolling for high-volume external threads on connectors can reduce per-part threading cost to fractions of a cent at scale. Always request itemized quotes to understand threading cost separately from turning and finishing.
4. Is thread milling better than tapping?
It depends on your specific situation. Thread milling is superior for hard materials (above 45 HRC), blind holes where chip evacuation is difficult, large thread diameters, and situations where one tool must produce multiple thread sizes. Tapping is faster and more cost-effective for standard thread sizes in aluminum, brass, and mild steel, particularly for through-holes. In practice, most CNC threading services use rigid tapping for standard production threads and switch to thread milling for challenging materials, tight tolerances, or non-standard profiles. eMachineShop’s threading guide confirms that both methods are standard in professional CNC threading services [3].
5. What materials can be CNC threaded?
CNC threading services work across a broad material range, including aluminum alloys (6061, 7075), brass and copper alloys, stainless steels (303, 304, 316), carbon and alloy steels, titanium (Grades 2 and 5), Inconel and other nickel superalloys, and engineering plastics such as PEEK, Delrin, and nylon. Material selection affects tool choice, cutting speed, coolant type, and thread form. Gummy materials like pure aluminum and austenitic stainless steel require specific tap geometries and coatings to prevent built-up edge and galling.
6. What thread standards are most commonly used in CNC machining?
The most common thread standards in CNC threading services are ISO metric (M series) for global industrial and consumer products, Unified National Coarse (UNC) and Fine (UNF) for North American and aerospace applications, NPT and NPTF for pipe and fluid fittings, and ACME/stub ACME for power transmission screws. Medical device parts often require metric fine threads per ISO 965, while automotive fasteners follow metric coarse threads per ISO 261. Specifying the correct standard on your drawing is essential to avoid costly mismatches with mating components.
Conclusion
this method are a foundational capability in precision manufacturing. The right threading method, correctly specified and executed by a certified supplier, determines whether your assembly functions reliably or fails at the fastening point. From Swiss lathe thread rolling on M2 connectors to single-point turning of large-diameter pipe threads, the choice of process matters as much as the machine that runs it.
The key takeaways are straightforward: specify threads completely on your drawings, match the threading method to your material and geometry, and partner with a supplier whose certifications and equipment back up their quality claims. As of 2026, the best this strategy combine ISO 9001:2015 process control, rapid quoting, and integrated threading-in-turning capability to cut lead times from weeks to days.
MFG SOLUTION delivers exactly that. With ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, 60+ engineering professionals, and the ability to quote within 8 hours and ship within 3 days, we handle this approach for electronics, automotive, and medical device manufacturers who can’t afford quality compromises or long lead times. Our parts go up to 38mm diameter, and our team will recommend the most cost-effective threading method for your specific application before the first chip falls.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: