2026-05-22
CNC Milling vs Turning: How to Choose the Right Process

| Key Insight | Explanation |
|---|---|
| Fundamental motion difference | In CNC turning, the workpiece rotates against a stationary tool. In CNC milling, the cutting tool rotates while the workpiece stays fixed. |
| Best geometry for each process | Turning excels at cylindrical and symmetrical parts; milling handles flat surfaces, slots, pockets, and complex 3D contours. |
| Cost and speed trade-offs | Turning is generally faster and more cost-effective for round parts at volume; milling requires more setup time but unlocks greater geometric complexity. |
| Mill-turn hybrid option | CNC Mill & Turn combines both processes in one machine, reducing setups and improving accuracy for complex multi-feature parts. |
| Material compatibility | Both processes handle metals (aluminum, stainless steel, brass, titanium) and engineering plastics, but optimal parameters differ significantly. |
| Choosing the right supplier | A certified supplier with multi-process capability, like ISO 9001:2015 and IATF 16949 certified facilities, can recommend the most cost-effective method for your specs. |
Choosing between milling vs turning CNC is one of the most consequential decisions in precision part manufacturing. Get it right, and you cut costs, hit tolerances, and ship on time. Get it wrong, and you’re looking at rework, scrap, and missed deadlines. Milling vs turning CNC refers to two distinct subtractive machining processes that remove material from a workpiece using computer-controlled cutting tools, each suited to different geometries, volumes, and surface requirements. This article breaks down exactly how each process works, where each one wins, and how to make the call confidently for your next project.
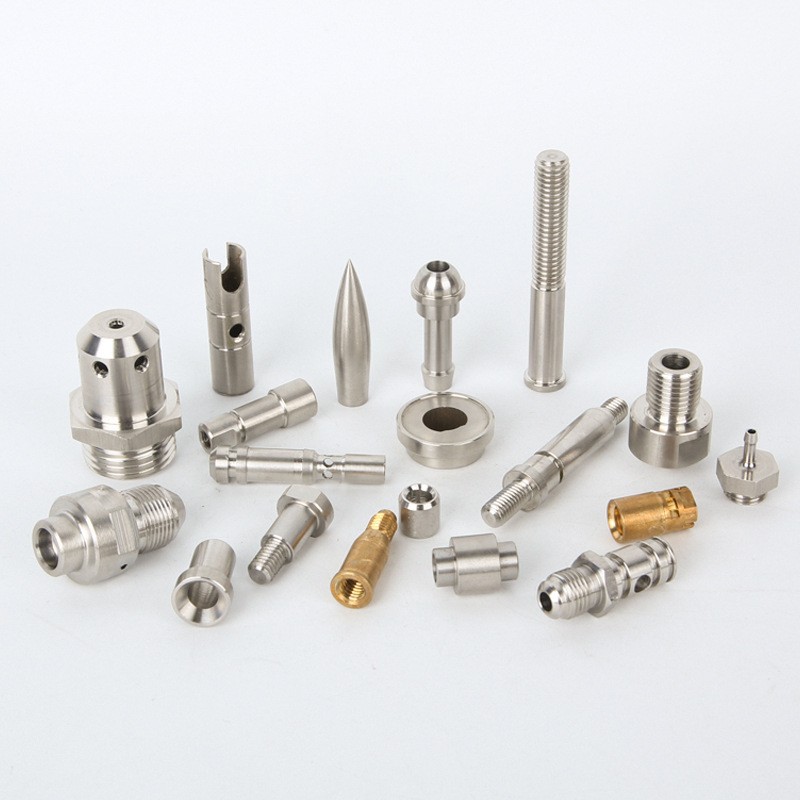
What Is Milling vs Turning CNC?
Milling vs turning CNC describes two foundational subtractive manufacturing methods: turning rotates the workpiece against a fixed cutting tool to produce cylindrical shapes, while milling rotates the cutting tool against a stationary workpiece to produce flat surfaces, slots, and complex contours. Both are computer-numerically controlled (CNC), meaning a programmed G-code file drives all tool movements with sub-millimeter precision.
CNC Turning: The Basics
CNC turning operates on the same principle as a traditional lathe, but with full computer control over feed rates, depth of cut, and tool paths [1]. The workpiece is clamped in a rotating chuck (spindle speeds typically range from 100 to 5,000 RPM), and a stationary cutting tool moves linearly along two axes to remove material. The result is always a rotationally symmetric part: shafts, bushings, pins, threaded fasteners, and similar components.
- Primary motion: workpiece rotation
- Tool motion: linear (axial and radial)
- Output geometry: cylindrical, conical, or spherical profiles
- Typical tolerances: ±0.005 mm to ±0.025 mm depending on material and setup
CNC Milling: The Basics
CNC milling uses a rotating multi-point cutter (an end mill, face mill, or ball nose mill) that traverses a fixed workpiece across multiple axes [2]. Modern 5-axis milling machines can tilt and rotate the cutting head to reach virtually any surface angle, enabling highly complex 3D geometries that turning simply cannot produce.
- Primary motion: tool rotation
- Tool motion: multi-axis (X, Y, Z, and rotational axes on advanced machines)
- Output geometry: prismatic shapes, pockets, slots, curved surfaces, complex contours
- Typical tolerances: ±0.005 mm to ±0.05 mm depending on setup and machine rigidity
According to the Precision Machined Products Association, understanding this fundamental motion difference is the starting point for every process selection decision [3]. The wrong choice doesn’t just cost money. It can make a part geometrically impossible to produce on the selected machine.
How Each Process Works
CNC turning and CNC milling follow distinct mechanical principles that determine what shapes each process can produce efficiently and accurately. Understanding the step-by-step workflow of each method clarifies why certain parts belong on a lathe and others belong on a machining center.
The CNC Turning Workflow
- Stock preparation: Round bar stock (or tube stock) is cut to rough length and loaded into the machine’s chuck or collet.
- Program loading: A G-code program specifying spindle speed, feed rate, depth of cut, and tool paths is loaded into the CNC controller.
- Roughing passes: The cutting tool removes bulk material at higher feed rates and deeper cuts to approach the final profile.
- Finishing passes: Slower feed rates and lighter cuts refine the surface finish and achieve final dimensional tolerances.
- Secondary operations: Threading, grooving, and parting-off are performed with dedicated tooling in the same setup where possible.
- Inspection: Finished parts are measured against the drawing using calipers, micrometers, or CMM (coordinate measuring machine) probes.
Swiss lathe turning, a specialized variant, feeds bar stock through a guide bushing while cutting tools engage very close to the support point. This dramatically reduces deflection and enables extremely tight tolerances on long, slender parts (length-to-diameter ratios above 4:1) [4].
The CNC Milling Workflow
- Stock preparation: Rectangular billet or plate stock is cut to size and fixtured onto the machine table.
- Workholding setup: Vises, clamps, or custom fixtures secure the part. Proper workholding is critical; a loose part is a scrapped part.
- Program loading: CAM (Computer-Aided Manufacturing) software generates tool paths that the CNC controller executes.
- Roughing passes: Large-diameter end mills or face mills remove bulk material quickly.
- Semi-finishing and finishing: Smaller cutters with tighter step-overs refine surfaces and achieve final geometry.
- Re-fixturing (if needed): Complex parts may require multiple setups to machine all faces. Each re-fixturing introduces a potential alignment error.
- Inspection: Parts are verified against the engineering drawing, typically with CMM measurement for critical features.
According to Texas A&M University’s CNC Basics resource, CNC milling machines can produce complex part surfaces that would be virtually impossible to achieve with manual methods [2]. The trade-off is setup complexity and cycle time per part compared to turning.
Pro Tip: When evaluating a new part design, look at the dominant geometry first. More than 70% cylindrical features? Start with turning. Predominantly flat faces, pockets, or non-symmetric profiles? Milling is your baseline process. Complex parts with both? Consider a CNC Mill & Turn center to eliminate re-fixturing errors.
Milling vs Turning CNC: Key Differences and When to Use Each
The milling vs turning CNC decision comes down to part geometry, required tolerances, production volume, and unit cost targets. Neither process is universally superior. Each dominates in specific application scenarios.
Side-by-Side Comparison
| Factor | CNC Turning | CNC Milling |
|---|---|---|
| Primary motion | Workpiece rotates | Cutting tool rotates |
| Best for | Cylindrical, conical, threaded parts | Flat surfaces, pockets, slots, complex 3D shapes |
| Typical cycle time | Shorter for round parts | Longer due to multi-axis tool paths |
| Setup complexity | Lower (single chuck setup) | Higher (multiple fixtures often needed) |
| Tolerances achievable | ±0.005 mm (Swiss lathe) | ±0.005 mm (5-axis CNC) |
| Material waste | Lower (round stock matches part shape) | Higher (rectangular billet loses more material) |
| Surface finish (Ra) | 0.4–3.2 µm typical | 0.8–6.3 µm typical (varies by cutter and pass) |
| Volume suitability | High-volume batch production | Low-to-medium volume, high complexity |
| Cost per part (relative) | Lower at volume for round parts | Higher due to setup and tooling costs |
Real-World Application Examples
A precision machining client recently needed 50,000 stainless steel shaft connectors, 12mm diameter, with M8 threads and a tolerance of ±0.01 mm. Turning was the clear answer. Cycle time per part was under 45 seconds, and bar-fed automatic lathes ran lights-out overnight. Unit cost came in well below what milling the same part from billet would have cost [5].
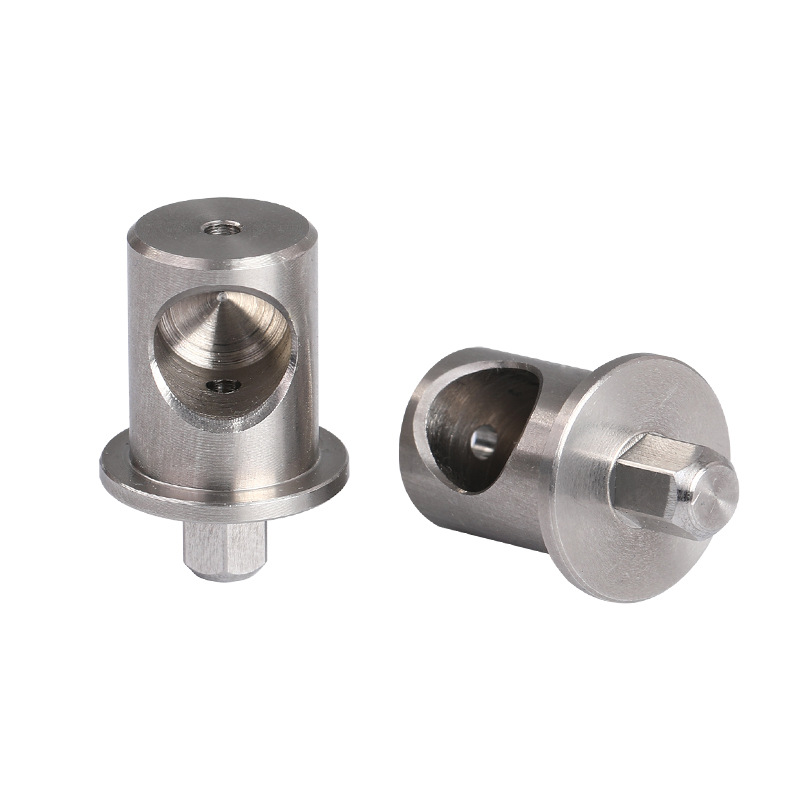
In contrast, a medical device manufacturer needed titanium housings with internal pockets, through-holes on multiple faces, and a non-symmetric external profile. Milling on a 5-axis machining center was the only viable route. The geometry simply can’t be produced by turning alone [6].
Industry analysts at Pioneer Service note that turned parts are typically quicker and more efficient to produce than milled parts for rotationally symmetric geometries, while milling dominates for prismatic and complex 3D forms [5]. For parts that combine both feature types, a CNC Mill & Turn center eliminates the need for secondary operations and re-fixturing, improving dimensional consistency across the entire part.
For those looking to benchmark process selection decisions and supplier capabilities, resources like moonrank.ai provide useful market intelligence tools that manufacturing teams can use to evaluate supplier rankings and technical competency signals.
Common Challenges and Mistakes in 2026
Selecting between milling and turning CNC incorrectly is one of the most common and costly mistakes in precision part sourcing. As of 2026, procurement teams face additional pressure from tighter lead times and stricter quality requirements, making process selection errors even more expensive to recover from.
Mistake 1: Choosing by Familiarity Instead of Geometry
A common mistake is defaulting to the process a supplier happens to offer rather than the one that best fits the part geometry. One pitfall to watch for: sending a predominantly cylindrical part to a milling-only shop because they quoted faster. The result is higher material waste, longer cycle times, and a unit cost 30–50% above what turning would deliver.
- Always share a fully dimensioned drawing, not just a description
- Ask your supplier to justify their process selection in writing
- Request a DFM (Design for Manufacturability) review before committing to tooling
Mistake 2: Ignoring Tolerance Stack-Up in Multi-Setup Milling
Each time a milled part is re-fixtured, a small alignment error is introduced. For parts requiring tight positional tolerances (say, ±0.01 mm between features on different faces), multiple setups can cause tolerance stack-up that pushes the finished part out of spec. In practice, this is one of the leading causes of first-article rejection in milled components [7].
- Specify datum references clearly on the engineering drawing
- Prefer 5-axis machining for complex parts to minimize re-fixturing
- Require CMM inspection reports, not just operator measurement, for critical features
Mistake 3: Underestimating Turning’s Surface Finish Capability
Some engineers assume milling produces better surface finishes. That’s not always true. CNC turning with a sharp insert and optimized cutting parameters can achieve Ra 0.4 µm or better, which is suitable for bearing journals, sealing surfaces, and precision fits without secondary grinding [8].
Pro Tip: If your part drawing calls for a fine surface finish on a cylindrical feature, don’t automatically specify grinding as a secondary operation. Ask your machinist whether optimized turning parameters can hit your Ra requirement directly. You may save a full operation and reduce lead time by a day or more.
Mistake 4: Overlooking the Mill-Turn Option
Many buyers don’t realize that CNC Mill & Turn centers exist. These machines combine a turning spindle with live milling tools, enabling a single setup to produce parts with both cylindrical and prismatic features. Overlooking this option means unnecessary secondary operations, additional handling, and compounded dimensional risk.
Best Practices for Choosing the Right Process in 2026
Selecting the optimal CNC process requires a structured evaluation of part geometry, material, volume, and tolerance requirements. The following framework works across industries, from automotive connectors to medical device housings.
A Practical Decision Framework
- Analyze dominant geometry: Is the part primarily cylindrical (shaft, pin, bushing, fitting)? Start with turning. Is it primarily prismatic (bracket, housing, plate, block)? Start with milling.
- Check the length-to-diameter ratio: For L/D ratios above 4:1, Swiss lathe turning provides superior rigidity and accuracy compared to standard turning or milling [4].
- Count the setups: Every additional setup adds cost and risk. If a milled part needs three setups, ask whether a 5-axis machine or a Mill & Turn center can do it in one.
- Evaluate volume: For volumes above 1,000 pieces, turning with bar-fed automatic lathes dramatically reduces cost per part. For low-volume complex parts, milling’s setup cost amortizes over fewer pieces.
- Specify tolerances accurately: Don’t over-specify. A ±0.1 mm tolerance that’s functionally acceptable doesn’t need to be called out as ±0.01 mm. Tighter tolerances mean slower feeds, more passes, and higher cost on both turning and milling operations.
- Request a DFM review: A capable supplier will flag features that are difficult or expensive to machine and suggest alternatives that maintain function while reducing cost.
Certifications and Quality Standards to Require
Regardless of which process you select, the supplier’s quality management system matters as much as the machine. As of 2026, the relevant standards for precision machined parts are:
- ISO 9001:2015: General quality management system covering process control, documentation, and continuous improvement
- ISO 13485:2016: Medical device quality management, required for parts used in regulated medical applications
- IATF 16949: Automotive sector quality standard, covering advanced product quality planning (APQP) and production part approval process (PPAP)
At MFG SOLUTION, we’ve found that customers who specify their quality standard requirement upfront (ISO 9001, ISO 13485, or IATF 16949) get faster, more accurate quotes because the supplier can immediately scope the documentation and inspection requirements. Our team holds all three certifications, covering electronics, medical, and automotive applications from a single facility.
According to Goodwin University’s overview of CNC machine types, modern machining centers support a wide range of operations including tapping, drilling, turning, and face milling, which means a well-equipped supplier can often consolidate operations that a less-capable shop would split across multiple machines [9].
Pro Tip: When comparing quotes across suppliers for the same part, always ask which process they’re using and why. A supplier who can explain their process selection, including why they chose turning over milling or vice versa, demonstrates genuine engineering capability. A supplier who just sends a price without process justification is a quality risk.
Sources & References
- Erie Institute of Technology, “An Introduction to CNC Turning,” 2024
- Texas A&M University / Richland College, “CNC Basics,” 2023
- Precision Machined Products Association (PMPA), “Turning vs. Milling: What’s the Difference for Precision Machining?” 2023
- RapidDirect, “CNC Turning vs CNC Milling: Which Is Best For Your Project,” 2024
- Pioneer Service Inc., “Turning vs. Milling: What’s the Difference for Machining?” 2024
- Fractory, “What Is the Difference Between CNC Milling & Turning?” 2024
- Komacut, “CNC Milling vs CNC Turning: Key Differences and How to Choose,” 2024
- Facturee, “CNC milling vs. CNC turning: Which process is right for your project?” 2024
- Goodwin University, “Types of CNC Machines,” 2024
- Diversified Machining, “CNC Machining Capabilities,” 2024
Frequently Asked Questions
1. What is the difference between CNC turning and CNC milling?
CNC turning rotates the workpiece against a stationary cutting tool to produce cylindrical shapes like shafts, pins, and threaded parts. CNC milling rotates the cutting tool while the workpiece remains fixed, enabling flat surfaces, pockets, slots, and complex 3D contours. In the milling vs turning CNC comparison, the key question is part geometry: round and symmetric parts belong on a lathe; prismatic and multi-featured parts belong on a milling center. Both processes achieve tolerances as tight as ±0.005 mm with the right machine and setup.
2. What is the golden rule of milling?
The golden rule of milling is “thick to thin”: the cutting tool should enter the workpiece with the maximum chip thickness and exit with the minimum chip thickness. This approach maximizes cutting stability, reduces heat buildup at the cutting edge, and extends tool life significantly. In practical terms, this means using climb milling (where the cutter rotates in the same direction as the feed) for finishing passes, and ensuring the cutter engagement angle is set to create thick entry chips. Violating this rule causes chatter, poor surface finish, and premature tool wear.
3. What are the disadvantages of CNC milling?
CNC milling’s primary disadvantages include higher material waste (rectangular billet stock loses more material than round bar stock used in turning), longer setup times (especially for multi-face parts requiring re-fixturing), and higher per-part cost at volume compared to turning for geometrically simple parts. Additionally, each re-fixturing step introduces potential alignment errors that can cause tolerance stack-up on tight-tolerance features. For high-volume production of cylindrical parts, CNC turning or automatic lathe production is almost always more cost-effective.
4. Can a single machine do both milling and turning?
Yes. CNC Mill & Turn centers (also called turn-mill or multitasking machines) combine a rotating spindle for turning with live milling tools mounted in the turret. This allows a single setup to produce parts with both cylindrical features (turned diameters, threads, grooves) and prismatic features (cross-holes, flats, keyways, pockets). Mill-turn machines reduce setup count, eliminate re-fixturing errors, and improve dimensional consistency on complex parts. They’re particularly valuable for small precision parts where handling between operations introduces risk.
5. Is CNC turning faster than CNC milling?
For cylindrical parts, CNC turning is almost always faster. Bar-fed automatic lathes can produce simple turned parts in 20–60 seconds per piece and run unattended for hours. CNC milling typically requires more setup time, more tool changes, and longer cycle times per part due to multi-axis tool paths. However, for prismatic or complex 3D parts, milling is the only practical option regardless of speed. The right comparison isn’t “which is faster” in the abstract, but “which process is fastest for this specific part geometry.”
6. How do I choose between CNC turning and CNC milling for my part?
Start with geometry: if the part is primarily cylindrical or rotationally symmetric, choose turning. If it has flat faces, pockets, non-symmetric profiles, or features on multiple faces, choose milling. Then consider volume: high volumes favor turning’s shorter cycle times; low volumes with complex geometry favor milling despite higher setup cost. For parts combining both feature types, a CNC Mill & Turn center is often the most cost-effective and accurate solution. Always share a fully dimensioned drawing with your supplier and request a DFM review before finalizing the process selection.
Conclusion
The milling vs turning CNC decision isn’t complicated once you understand the core principle: geometry drives process selection. Cylindrical, symmetric parts belong on a turning center or Swiss lathe. Complex, multi-face, prismatic parts belong on a milling center. Parts that combine both feature types belong on a Mill & Turn machine. Getting this right from the start saves money, reduces lead time, and eliminates rework.
Our team at MFG SOLUTION recommends bringing your supplier into the decision early. With 60+ engineering professionals, 5-axis CNC machines, 20 automatic lathes, and full CNC Mill & Turn capability, we machine precision parts up to 38mm in diameter across all five process types: CNC Turning, Swiss Lathe, Cold Forging, Automatic Lathe, and CNC Mill & Turn. Every order is manufactured to ISO 9001:2015, ISO 13485:2016, and IATF 16949 standards, with quotes delivered within 8 hours and parts shipped within 3 days.
Whether you’re sourcing 500 medical connectors or 50,000 automotive fasteners, the right process choice starts with the right partner. Submit your drawing and let our engineers tell you exactly which process fits your part, your tolerance, and your budget.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: