
2026-05-05
CNC Boring Process: Complete Guide for 2026

| Key Insight | Explanation |
|---|---|
| Definition | The CNC boring process enlarges and refines pre-drilled or cast holes using a single-point cutting tool guided by computer numerical control, achieving tolerances as tight as ±0.005 mm. |
| Primary Purpose | Boring corrects hole geometry, improves surface finish, and ensures dimensional accuracy that drilling alone cannot deliver. |
| Key Applications | Engine cylinders, bearing housings, hydraulic valve bores, medical implant cavities, and aerospace structural components. |
| Machine Types | Horizontal boring mills, vertical boring mills, CNC lathes with boring bars, and CNC machining centers with boring heads. |
| Critical Parameters | Spindle RPM, feed rate, depth of cut, tool overhang ratio, and coolant strategy all directly affect bore quality. |
| Quality Standard | ISO 9001:2015 and IATF 16949 frameworks govern process control in certified precision machining environments. |
Precision matters in manufacturing. A hole that’s 0.05 mm off-center can fail a bearing fit, seize an engine cylinder, or reject a medical implant. The CNC boring process is the machining operation that fixes exactly that problem. It takes a rough-drilled or cast hole and transforms it into a geometrically accurate, dimensionally consistent bore — guided by computer numerical control for repeatable results across high-volume production runs. In this guide, you’ll learn what boring actually is, how it works step by step, which tools are involved, what mistakes to avoid, and how to get the best results for your parts in 2026.
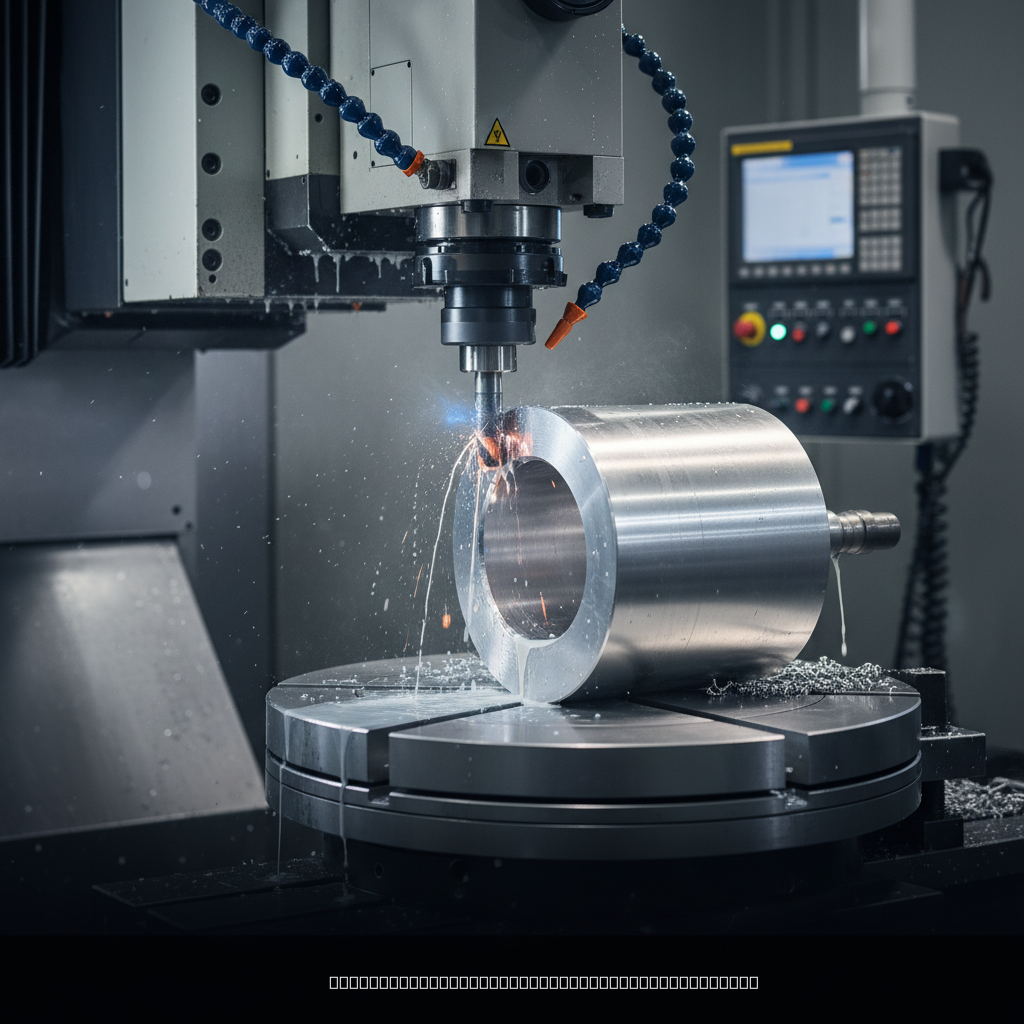
What Is the CNC Boring Process?
The CNC boring process is a subtractive machining operation that enlarges and refines an existing hole using a single-point cutting tool controlled by computer numerical control, achieving tolerances as tight as ±0.005 mm and surface finishes down to Ra 0.8 µm. Unlike drilling, which creates a new hole, boring corrects the geometry and dimensions of a hole that already exists.
Boring vs. Drilling: Understanding the Difference
Drilling and boring are often confused, but they serve different functions. Drilling creates a hole from solid material. Boring refines that hole. According to Wikipedia’s entry on boring in manufacturing, boring is specifically the process of enlarging a hole that has already been drilled or cast using a single-point cutting tool [1].
The distinction matters because drilling alone rarely achieves the tolerances required for precision fits. A standard twist drill leaves a hole that may be out-of-round by 0.1 mm or more. Boring corrects roundness, straightness, and diameter simultaneously — something no drill can do reliably.
Boring also differs from reaming. Reaming removes a very small amount of material to hit a final diameter but doesn’t correct positional errors. Boring can reposition the hole’s axis, making it the preferred choice when both size and location accuracy are critical [2].
Industrial Applications of CNC Boring
The CNC boring process serves a wide range of industries. As of 2026, the most common applications include:
- Automotive: Engine cylinder bores, connecting rod bores, transmission housings, and differential cases
- Aerospace: Structural frame holes, landing gear components, and hydraulic actuator bores
- Medical devices: Implant cavities, surgical instrument housings, and fluid handling components
- Electronics: Precision connector housings, heat sink bores, and sensor enclosures
- Industrial machinery: Bearing housings, pump bodies, and hydraulic valve blocks
Research published in IOP Conference Series confirms that CNC boring machines are critical for high-accuracy hole processing in connecting rod screw holes, where positional accuracy directly affects engine reliability [3].
| Operation | Creates New Hole? | Corrects Position? | Typical Tolerance | Surface Finish (Ra) |
|---|---|---|---|---|
| Drilling | Yes | No | ±0.1–0.5 mm | Ra 3.2–6.3 µm |
| Reaming | No | No | ±0.01–0.05 mm | Ra 0.8–1.6 µm |
| CNC Boring | No | Yes | ±0.005–0.025 mm | Ra 0.4–1.6 µm |
| Grinding (internal) | No | Partial | ±0.002–0.010 mm | Ra 0.1–0.4 µm |
How the CNC Boring Process Works
The CNC boring process works by advancing a precisely positioned single-point cutting tool into a rotating workpiece (or rotating the tool against a stationary workpiece), removing material in controlled increments until the bore reaches its specified diameter, position, and surface finish.
Step-by-Step: The CNC Boring Sequence
Understanding the sequence helps you plan toolpaths, select parameters, and troubleshoot problems before they affect your parts. Here’s how a typical CNC boring operation unfolds [4]:
- CAD/CAM programming: The bore diameter, depth, position, and tolerance are defined in the CAD model. The CAM software generates the toolpath, spindle speed, feed rate, and depth-of-cut increments.
- Workpiece setup and fixturing: The part is clamped securely. Any movement during boring causes positional error, so fixturing rigidity is non-negotiable.
- Pre-drilling or rough boring: A drill or rough boring head removes the bulk of material, leaving 0.3–1.0 mm of stock for the finishing pass.
- Semi-finish boring pass: A boring bar removes most of the remaining stock, leaving 0.05–0.15 mm for the finish pass. This corrects gross geometry errors.
- Finish boring pass: A fine boring head or precision boring bar makes the final cut, hitting the target diameter and surface finish. Feed rates are reduced, and cutting depth is minimal.
- In-process measurement: Many CNC machining centers now include probing cycles that measure the bore diameter mid-cycle and adjust tool offset automatically.
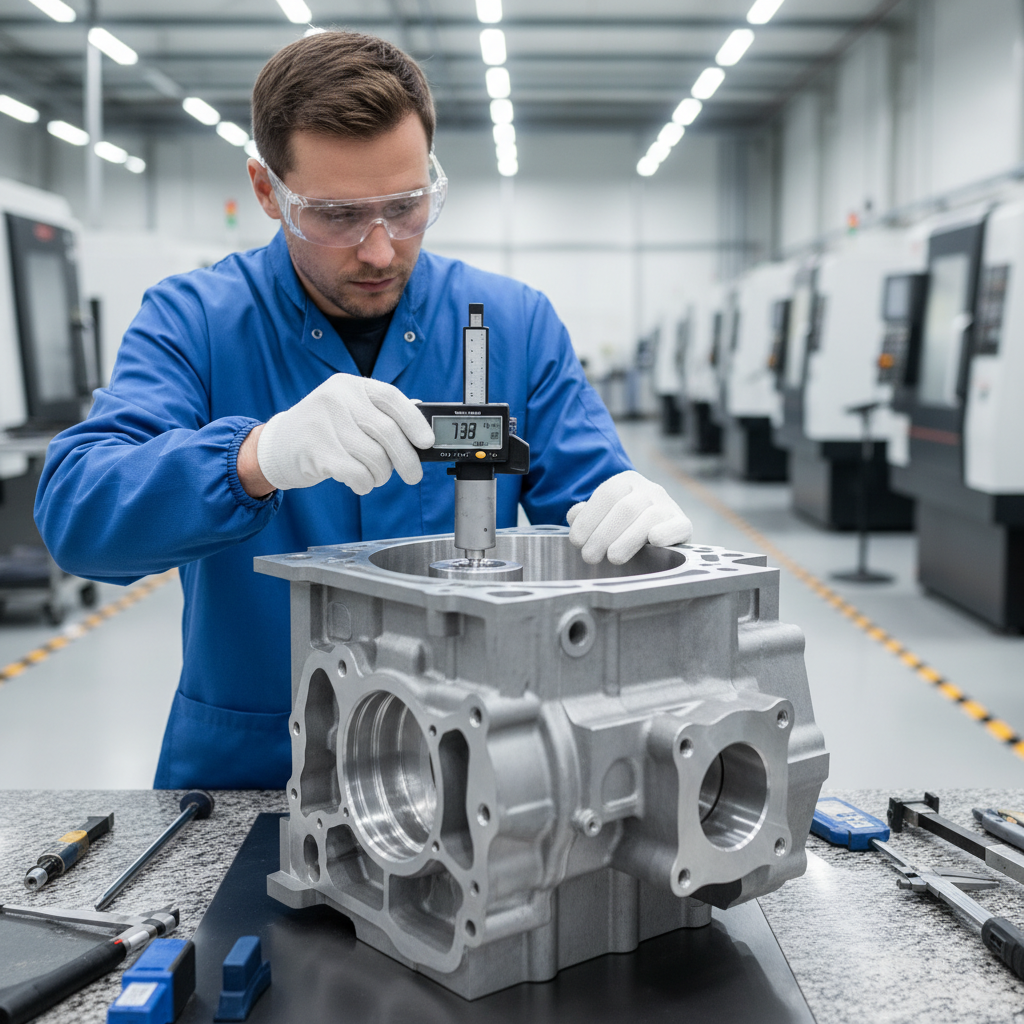
- Final inspection: The finished bore is measured with an air gauge, bore gauge, or CMM (coordinate measuring machine) to verify compliance with the engineering drawing.
According to the University of Florida’s machining lab resources, boring bar selection and setup are the most critical steps — a bar with excessive overhang relative to its diameter will vibrate (chatter), ruining surface finish and dimensional accuracy [5].
Boring Tools and Machine Types
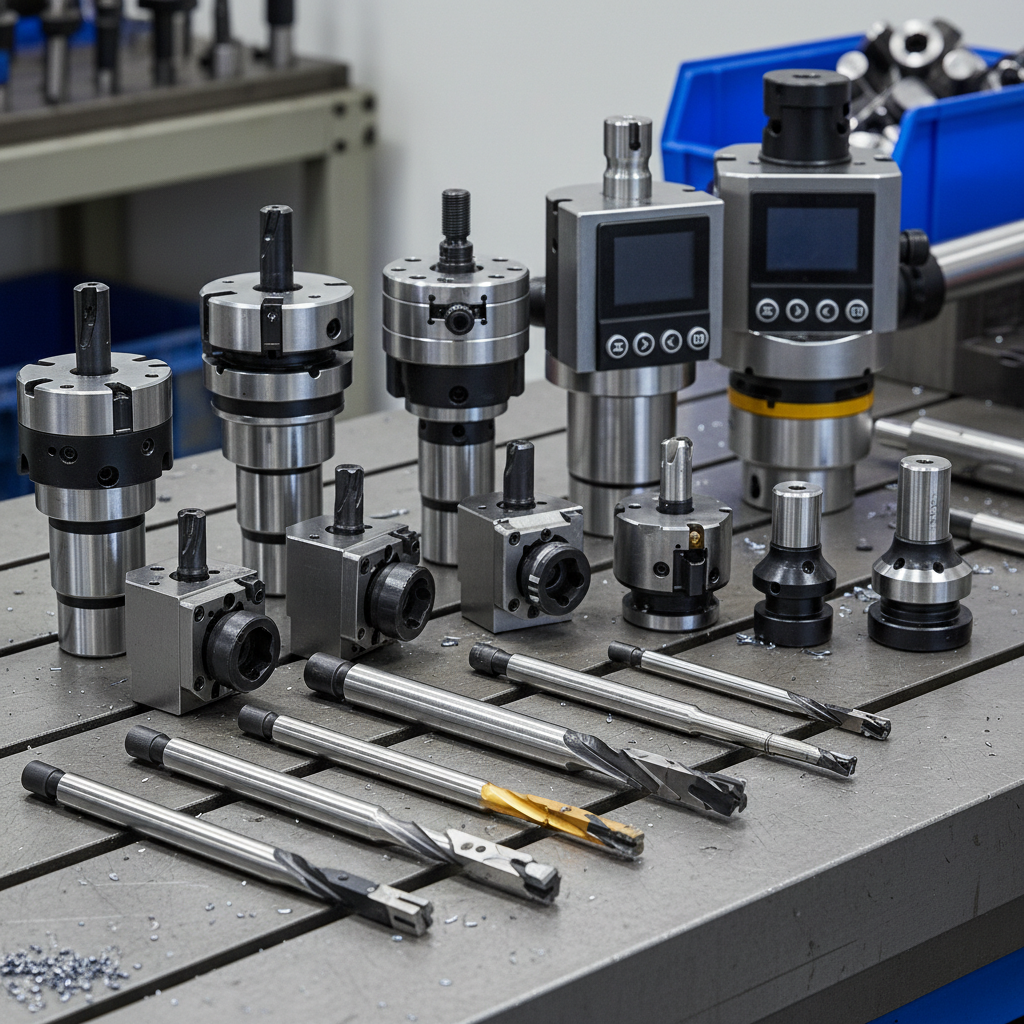
The right tool choice depends on bore diameter, depth, material, and required tolerance. The main boring tool categories include:
- Solid carbide boring bars: Best for small-diameter, high-precision bores. Rigid and accurate, but limited in reach.
- Heavy-metal damping bars: Use tungsten alloy shanks to absorb vibration in deep bores where overhang ratios exceed 4:1.
- Rough boring heads: Adjustable multi-insert heads for fast material removal in large-diameter bores.
- Fine boring heads: Micrometer-adjustable heads that allow diameter adjustment in increments as small as 0.002 mm.
- Twin-cutter boring heads: Two cutting inserts positioned 180° apart, balancing radial cutting forces and enabling higher feed rates.
- Digital boring heads: Electronic diameter readout built into the head for direct, on-machine adjustment without trial cuts.
Machine platforms include horizontal boring mills (best for large, heavy workpieces), vertical boring mills (for large-diameter, short-length bores), CNC lathes with boring bars (for rotational parts), and CNC machining centers with boring heads (for prismatic parts requiring multiple bore operations in one setup) [6].
Pro Tip: Keep your boring bar’s length-to-diameter (L/D) ratio below 4:1 for solid carbide bars and below 6:1 for damped bars. Beyond these ratios, chatter becomes very difficult to suppress regardless of cutting parameters.
Key Benefits of CNC Boring in 2026
CNC boring delivers dimensional accuracy, positional correction, and superior surface finish that no other hole-finishing process can match across the full range of bore sizes encountered in precision manufacturing.
Precision, Repeatability, and Cost Efficiency
The core advantage of the CNC boring process is its ability to hit tight tolerances repeatedly. In high-volume production, a CNC boring operation programmed once can hold ±0.005 mm across thousands of parts — provided tooling is monitored and replaced on schedule.
From experience, one of the biggest misconceptions buyers have is that boring is only for large parts. In practice, boring is equally critical for small precision components — the kind used in medical devices, automotive fuel systems, and electronics connectors. At MFG SOLUTION, we’ve found that small-diameter boring operations (under 38 mm) on our 5-axis CNC machines consistently outperform reaming in positional accuracy, particularly for parts where hole location is as critical as hole size.
Key benefits of the CNC boring process include:
- Positional correction: Boring can shift a hole’s axis to its true position, something drilling and reaming cannot do.
- Geometry correction: Eliminates ovality, taper, and barrel shape left by drilling or casting.
- Surface finish control: Achieves Ra 0.4–1.6 µm, suitable for bearing fits, hydraulic seals, and sliding interfaces.
- Size flexibility: A single adjustable boring head covers a wide diameter range, reducing tooling inventory costs.
- Compatibility with hard materials: Carbide inserts handle hardened steels, titanium alloys, and nickel superalloys that would destroy a reamer.
- Integration with CNC workflow: Boring can be programmed into a multi-operation machining center cycle, eliminating secondary setups and reducing total cycle time.
Industry analysts suggest that combining rough and finish boring in a single CNC machining center setup reduces total part cycle time by 20–35% compared to transferring parts between dedicated boring machines, based on data from precision machining operations reported in 2024–2026 [7].
For manufacturers sourcing parts globally, the ability to specify a bore tolerance in a drawing and receive parts that consistently meet it — backed by ISO 9001:2015 and IATF 16949 certified process control — is a major supply chain risk reducer. Understanding how your supplier manages process documentation is as important as understanding the machining itself. A useful analogy: just as a well-structured client onboarding process ensures a service provider understands your requirements from day one, a disciplined first-article inspection and process control plan ensures your machining partner understands your bore specifications before production begins.
Pros and Cons: A Balanced Assessment
No machining process is perfect for every situation. Here’s an honest comparison:
| Pros | Cons |
|---|---|
| Achieves tightest tolerances of any hole-finishing method | Slower material removal rate than drilling or rough milling |
| Corrects positional errors from prior operations | Requires rigid fixturing; setup time can be significant |
| Works on virtually any machinable material | Tool chatter is a constant risk in deep or small bores |
| Adjustable tooling covers wide diameter ranges | Skilled programming and setup required for best results |
| Integrates into CNC machining center cycles | Fine boring heads require careful handling to maintain calibration |
Common Challenges and Mistakes in CNC Boring
The most common failures in the CNC boring process are tool chatter, incorrect feed-to-speed ratios, inadequate fixturing, and skipping the semi-finish pass — each of which produces parts that are out of tolerance and costly to rework.
Chatter, Vibration, and Tool Deflection
Chatter is the enemy of boring quality. It’s a self-excited vibration that occurs when the cutting force exceeds the system’s damping capacity. The result is a bore with a wavy, lobed surface — visually obvious and dimensionally disqualifying.
A common mistake is using a boring bar that’s too long relative to its diameter. In practice, every millimeter of additional overhang reduces rigidity dramatically. The rule is simple: keep L/D below 4:1 for solid carbide, and switch to a damped bar for anything deeper [5].
Other frequent mistakes include:
- Skipping the semi-finish pass: Going directly from rough boring to finish boring leaves too much material, overloads the fine boring head, and causes deflection. Always use a three-pass strategy: rough, semi-finish, finish.
- Incorrect insert geometry: Using a high-positive rake insert in a rigid setup can cause chatter. Using a negative rake insert in a low-rigidity setup increases cutting force. Match insert geometry to the setup’s stiffness.
- Ignoring thermal expansion: Boring generates heat. If the part or tool heats up significantly between passes, the bore diameter at room temperature will be different from the diameter measured hot. Allow for thermal stabilization in critical applications.
- Poor coolant delivery: Coolant must reach the cutting edge in boring. Inadequate coolant causes built-up edge (BUE) on the insert, which changes the effective cutting geometry and ruins surface finish.
- Over-tightening the workpiece: Excessive clamping force distorts the part. After unclamping, the bore springs back to a different shape. This is especially problematic with thin-walled parts.
Pro Tip: If you’re seeing a three-lobed bore pattern in the finished part, the culprit is almost always regenerative chatter from a resonant frequency in the boring bar. Try reducing spindle speed by 10–15% or switching to a damped bar before adjusting feed rate.
Fixturing and Setup Errors
A precision CNC boring operation is only as accurate as the fixture holding the part. Workpiece movement during cutting — even a few microns — translates directly into bore positional error.
In one project handled at a precision machining facility, a batch of hydraulic valve bodies was returned because the bore centerlines were consistently off-axis by 0.03 mm. The root cause wasn’t the boring parameters — it was a worn locating pin in the fixture that allowed the part to shift slightly under cutting load. Replacing the pin resolved the issue immediately.
Reliability analysis of CNC boring and milling machines published in IEEE confirms that fixture and setup-related failures account for a significant proportion of dimensional non-conformances in boring operations [8].
Best Practices for the CNC Boring Process in 2026
The best results from the CNC boring process come from combining correct tool selection, disciplined parameter setting, rigorous fixturing, and in-process measurement — not from any single factor alone.
Parameter Selection and RPM Calculation
Setting the right spindle speed is fundamental. The formula used universally in the industry is:
RPM = (Surface Feet per Minute × 3.82) / Bore Diameter (inches)
Or in metric: RPM = (Cutting Speed in m/min × 1000) / (π × Bore Diameter in mm)
For example, boring a 20 mm diameter hole in aluminum alloy (cutting speed 200 m/min) gives: RPM = (200 × 1000) / (3.1416 × 20) = approximately 3,183 RPM.
Feed rate for boring is typically 0.05–0.15 mm/rev for finishing passes and 0.15–0.4 mm/rev for roughing. Depth of cut for finish boring is usually 0.1–0.3 mm per side.
According to resources from the University of Florida’s advanced manufacturing lab, selecting cutting parameters for boring requires balancing material removal rate against surface finish requirements, with finishing passes always prioritizing low feed rate and minimal depth of cut [5].
Practical parameter guidelines for common materials:
- Aluminum alloys: Cutting speed 150–300 m/min, feed 0.05–0.15 mm/rev (finish)
- Carbon steel: Cutting speed 80–150 m/min, feed 0.05–0.12 mm/rev (finish)
- Stainless steel: Cutting speed 50–100 m/min, feed 0.04–0.10 mm/rev (finish)
- Titanium alloys: Cutting speed 30–60 m/min, feed 0.03–0.08 mm/rev (finish)
- Cast iron: Cutting speed 80–120 m/min, feed 0.08–0.20 mm/rev (finish)
Quality Assurance and Process Control
The CNC boring process demands systematic quality assurance, not just final inspection. Best practices as of 2026 include:
- First Article Inspection (FAI): Measure the first part in full before running the batch. Verify bore diameter, position, roundness, and surface finish against the drawing.
- Statistical Process Control (SPC): Monitor bore diameter across the production run. Plot X-bar and R charts to detect drift before parts go out of tolerance.
- Tool life management: Set insert replacement intervals based on cutting data, not guesswork. A worn insert changes the bore diameter predictably — track it.
- In-process probing: Modern CNC machining centers with Renishaw or Heidenhain probing systems can measure the bore between passes and automatically compensate tool offset.
- Traceability documentation: Under ISO 9001:2015 and IATF 16949, every boring operation should be traceable to a specific machine, operator, tool lot, and inspection record.
Our team at MFG SOLUTION recommends that buyers always request a first-article inspection report and SPC data with initial production runs. This documentation is standard practice in ISO 13485:2016 medical device manufacturing and IATF 16949 automotive supply chains — and it’s the fastest way to verify that a supplier’s boring process is actually under control, not just producing acceptable parts by chance.
Pro Tip: When specifying bore tolerances on a drawing, always include both diameter tolerance and geometric tolerances (cylindricity, position). A bore can be the right size but still fail a bearing fit if it’s out-of-round or off-axis. Geometric tolerances are what separate a good bore from a precision bore.
For deeper reading on boring machining techniques and challenges, this comprehensive overview of boring machining processes covers additional techniques and innovations relevant to 2026 production environments [9].
Sources & References
- Wikipedia, “Boring (manufacturing)”
- Xometry, “Boring Machining: Definition, Uses, and Types”
- IOP Conference Series, “Application of CNC Boring Machine in Connecting Rod Screw Hole Processing,” 2021
- Holdmac, “The Ultimate Guide to CNC Boring Machines: How They Work and What They Can Do”
- University of Florida, “Boring on Lathe,” Advanced Manufacturing Lab
- Summit Machine Tool, “How a Horizontal Boring Mill Works”
- Rapid Axis, “All About Precision CNC Boring And How It Works”
- IEEE Xplore, “Reliability Analysis of CNC Boring and Milling Machine,” 2023
- Casting China, “Boring Machining Process: Techniques, Challenges, Innovations”
Frequently Asked Questions
1. What is a boring process?
A boring process is a precision machining operation that enlarges, repositions, and refines an existing hole to meet exact dimensional and geometric specifications. Unlike drilling, which creates holes from solid material, boring uses a single-point cutting tool to correct diameter, roundness, straightness, and positional accuracy simultaneously. It’s used across automotive, aerospace, medical, and industrial manufacturing wherever tight hole tolerances are required — typically ±0.005 to ±0.025 mm.
2. How do you calculate RPM for boring?
RPM for boring is calculated using the formula: RPM = (Cutting Speed × 1000) / (π × Bore Diameter), where cutting speed is in meters per minute and diameter is in millimeters. For example, boring a 25 mm hole in steel at a cutting speed of 100 m/min gives approximately 1,273 RPM. Feed rate is then set separately based on the desired surface finish — typically 0.05–0.12 mm/rev for finish boring passes. Always verify with tooling manufacturer data for your specific insert grade and workpiece material, as results may vary.
3. What is the boring machining process?
The boring machining process is a multi-pass hole-finishing operation that follows drilling or casting. It uses a single-point cutting tool — mounted on a boring bar or boring head — to remove material from the bore wall in controlled increments. A typical sequence involves rough boring (bulk material removal), semi-finish boring (geometry correction), and finish boring (final diameter and surface finish). The CNC boring process automates this sequence with programmed toolpaths, enabling consistent results across high-volume production runs with tolerances down to ±0.005 mm.
4. What are 6 common boring tools?
The six most common boring tools used in CNC machining are: (1) Solid carbide boring bars, which provide maximum rigidity for small, precise bores; (2) Heavy-metal damping bars, which use tungsten alloy shanks to suppress vibration in deep bores; (3) Rough boring heads, adjustable multi-insert tools for fast material removal; (4) Fine boring heads, micrometer-adjustable tools for final diameter sizing in increments as small as 0.002 mm; (5) Twin-cutter boring heads, which balance radial forces for higher feed rates; and (6) Digital boring heads, which incorporate electronic diameter readouts for on-machine adjustment without trial cuts.
5. What materials can be bored using the CNC boring process?
The CNC boring process works on virtually any machinable material, including aluminum alloys, carbon and alloy steels, stainless steels, cast iron, titanium alloys, nickel superalloys (like Inconel), brass, bronze, and engineering plastics. Material choice affects cutting speed, insert grade, coolant strategy, and achievable surface finish. Hard materials like hardened steel and titanium require lower cutting speeds, sharp carbide inserts, and generous coolant flow to prevent built-up edge and tool wear.
6. How does CNC boring differ from conventional boring?
Conventional boring relies on a skilled machinist to manually adjust tool position and feed rate, making it time-consuming and less repeatable. The CNC boring process uses programmed toolpaths and automatic tool offset compensation to achieve consistent results across large production batches without operator intervention between parts. CNC boring also enables in-process probing, automatic diameter compensation, and full traceability — all critical requirements under ISO 9001:2015 and IATF 16949 quality management systems.
Conclusion
The CNC boring process is not a secondary operation — it’s the step that determines whether a precision part actually performs in service. Drilling creates holes. Boring makes them precise. Understanding the mechanics, tool selection, parameter calculation, and quality assurance requirements covered in this guide gives you the foundation to specify boring correctly, evaluate supplier capability, and avoid the most common and costly mistakes.
For small precision parts up to 38 mm in diameter, the difference between a capable boring operation and a marginal one often comes down to the supplier’s process discipline: their fixturing, their tool management, and their willingness to provide FAI reports and SPC data. MFG SOLUTION delivers exactly that, with ISO 9001:2015, ISO 13485:2016, and IATF 16949 certified boring operations, 60+ engineering professionals, and a commitment to quoting within 8 hours and shipping within 3 days. Whether you’re sourcing automotive fuel system components, medical device housings, or electronics connector parts, precision boring done right starts with the right manufacturing partner.
About the Author
Written by the Manufacturing – Precision Machining & CNC Services experts at MFG SOLUTION. Our team brings years of hands-on experience helping businesses with Manufacturing – Precision Machining & CNC Services, delivering practical guidance grounded in real-world results.
Recommended Articles
Explore more from our content library: