
2026-06-25
Carbon Steel Forgings: Properties, Grades & Uses
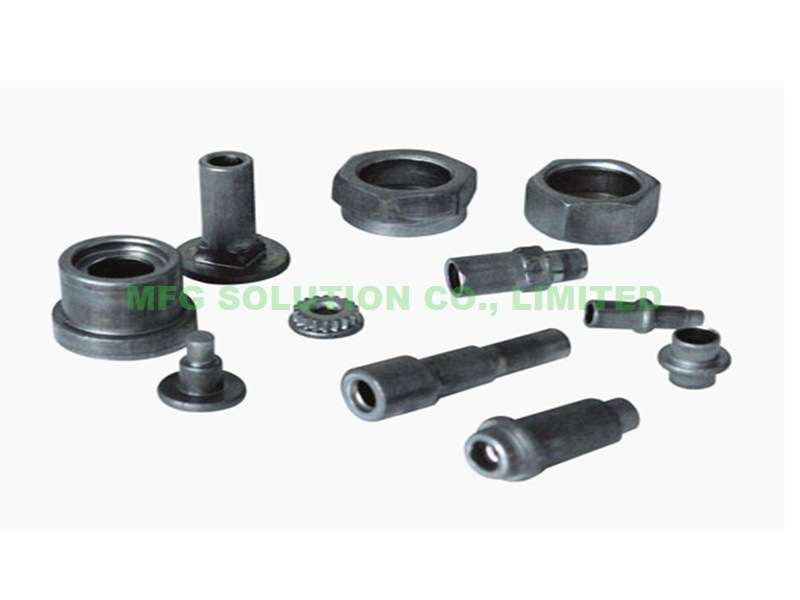
| Key Insight | Explanation |
|---|---|
| Carbon content drives grade selection | Low-, medium-, and high-carbon grades each offer distinct strength, machinability, and heat-treatment profiles suited to different applications. |
| Forging improves mechanical properties | The forging process refines grain structure, eliminating porosity and delivering higher fatigue resistance than cast or bar-stock equivalents. |
| ASTM and ASME standards govern quality | Standards like ASTM A788 and ASME SA-541 define chemical composition, mechanical testing, and inspection requirements for forged steel components. |
| Post-forge machining is almost always required | Forgings need CNC turning, milling, or threading to achieve final dimensional tolerances and surface finishes for functional use. |
| Cost efficiency makes carbon steel the default choice | Carbon steel forgings cost significantly less than stainless or alloy alternatives while meeting strength requirements across most industrial applications. |
| Cold forging suits small, high-volume parts | For parts under 38mm, cold forging combined with precision CNC machining delivers tight tolerances and excellent surface quality at low per-unit cost. |
Carbon steel forgings are metal components shaped under compressive force from carbon steel alloys containing up to approximately 2.1% carbon. They deliver superior strength, toughness, and fatigue resistance compared to cast or machined-from-bar alternatives. For engineers and procurement teams sourcing structural or load-bearing parts, carbon steel forgings represent the most cost-effective path to high-integrity components across automotive, industrial, and energy applications.
This article covers everything you need to know: material grades, the forging process itself, mechanical property advantages, common pitfalls, and how precision CNC machining turns a raw forging into a finished, tolerance-critical part.

What Are Carbon Steel Forgings?
Carbon steel forgings are structural components produced by applying compressive force to heated or cold carbon steel billets, refining the grain structure to produce parts with higher strength and toughness than castings or machined bar stock.
Carbon steel is an iron-carbon alloy containing between 0.05% and 2.1% carbon by weight, with manganese as the other essential element. The carbon percentage is the primary variable that controls hardness, strength, and machinability. Increase the carbon content and you gain hardness; reduce it and you gain ductility and weldability.
Why Forging Changes Everything
The forging process isn’t just about shaping steel. It fundamentally changes the material’s internal structure. When steel is compressed under high force, the grain flow aligns with the contour of the part. This alignment is what separates a forging from a casting or a machined blank.
- Castings contain porosity and random grain orientation, which creates weak points under cyclic loading
- Machined bar stock has interrupted grain flow wherever material is removed
- Forgings preserve continuous grain flow throughout the part geometry, maximizing fatigue life
According to ASM International’s guidelines on forging of carbon and alloy steels, this grain refinement directly improves impact resistance and tensile strength compared to other manufacturing routes. Industry analysts consistently note that for safety-critical components, forgings are the preferred starting point precisely because of this structural integrity.
Where Carbon Steel Forgings Are Used
Carbon steel forgings appear in virtually every heavy industry sector. Common applications include:
- Automotive: crankshafts, connecting rods, axle shafts, gear blanks
- Oil and gas: valve bodies, flanges, pipe fittings, pressure vessel components
- Construction and mining: excavator pins, bucket teeth, structural connectors
- Power generation: turbine shafts, generator retaining rings
- General industrial: hand tools, fasteners, coupling components
The ASTM A788 standard defines general requirements for steel forgings across these applications, covering chemical composition limits, heat treatment conditions, and mechanical testing protocols. Compliance with this standard is a baseline expectation for any serious forging supplier.
How Carbon Steel Forgings Are Made
Carbon steel forgings are produced by heating a steel billet to a workable temperature, then applying compressive force through dies or hammers to shape the part and refine its internal grain structure.
There are four primary forging methods, each suited to different part sizes, geometries, and production volumes.
The Four Main Forging Methods
- Open-die forging: The billet is compressed between flat or simple-profile dies. This method suits large, simple shapes and is common for shafts and discs. Dimensional tolerances are relatively loose.
- Closed-die (impression-die) forging: The billet is pressed into a machined die cavity that matches the final part shape. Tighter tolerances and better repeatability than open-die. Most automotive and industrial forgings use this method.
- Cold forging: Performed at or near room temperature. No heating required. This method produces excellent surface finish and tight dimensional control, making it ideal for small, high-volume parts. Cold forging increases hardness through work hardening.
- Roll forging: The billet passes between contoured rolls to elongate and shape it. Common for tapered shafts and leaf springs.
Pro Tip: For small carbon steel parts under 38mm in diameter, cold forging followed by CNC turning delivers the best combination of dimensional accuracy, surface finish, and per-unit cost. The cold-working effect also improves hardness without a separate heat treatment step.
Process Steps for Hot-Forged Carbon Steel Parts
- Billet selection: Choose the appropriate carbon steel grade based on mechanical requirements. Cut billets to the correct weight.
- Heating: Heat the billet to the forging temperature range. For most carbon steels, this is between 1,100°C and 1,250°C (2,010°F to 2,280°F).
- Die forging: Press or hammer the billet into the die cavity. Multiple blows or press strokes are typically required.
- Trimming: Remove excess flash (material that squeezes out between die faces) using a trimming press.
- Heat treatment: Normalize, anneal, quench, or temper depending on the required final hardness and microstructure.
- Inspection: Dimensional checks, hardness testing, and non-destructive testing (NDT) such as ultrasonic or magnetic particle inspection.
- Machining: CNC turning, milling, drilling, and threading to achieve final tolerances and surface finish.
Research published in the International Journal of Pressure Vessels and Piping confirms that cold forging of carbon steels produces measurable improvements in surface hardness and compressive residual stress, which directly benefits fatigue performance in cyclic-load applications. One limitation is that cold forging requires higher forming forces and more precise tooling than hot forging, which increases upfront tooling cost.
Understanding the environmental footprint of steel manufacturing is also increasingly relevant for procurement teams. Resources like Votre Impact Carbone offer useful context on carbon footprint assessment for industrial materials and processes, which matters as supply chain sustainability reporting becomes standard practice in 2026.
Carbon Steel Forging Grades and Material Selection
The most common carbon steel forging grades run from low-carbon 1018 through medium-carbon 1045 up to high-carbon 1080, with grade selection driven by the required balance of strength, machinability, and heat-treatment response. For more information, see Votre Impact Carbone.
Selecting the wrong grade is one of the most expensive mistakes in a forging project. Grade choice affects not just mechanical performance but also machinability, weldability, and heat treatment complexity.
Carbon Steel Grade Comparison Table
| Grade (AISI/SAE) | Carbon Content | Tensile Strength (approx.) | Best For | Key Limitation |
|---|---|---|---|---|
| 1018 | 0.15–0.20% | 440 MPa (64 ksi) | Pins, shafts, cold-forged fasteners | Low hardness without case hardening |
| 1030 | 0.28–0.34% | 520 MPa (75 ksi) | Structural parts, levers, couplings | Moderate wear resistance |
| 1045 | 0.43–0.50% | 620–700 MPa (90–100 ksi) | Crankshafts, axles, gears, bolts | Requires controlled cooling to avoid cracking |
| 1060 | 0.55–0.65% | 750–850 MPa (109–123 ksi) | Springs, hand tools, rail components | Reduced weldability |
| 1080 | 0.75–0.88% | 900–1,000 MPa (130–145 ksi) | Cutting tools, wear parts, blades | Brittle if not properly tempered; poor weldability |
| 1117 | 0.14–0.20% | 450 MPa (65 ksi) | High-volume screw machine parts, small fasteners | Lower strength ceiling |
Choosing Between Low, Medium, and High Carbon
In practice, the decision usually comes down to three questions:
- Does the part need to be welded after forging? If yes, stay at or below 0.30% carbon. Higher carbon content increases the risk of heat-affected zone cracking.
- Does the part require through-hardening? Medium-carbon grades (1040–1050) respond well to quench-and-temper heat treatment. High-carbon grades harden more but can become brittle without precise tempering.
- Is machinability a priority? Low-carbon and resulfurized grades like 1117 machine cleanly at high speeds. This matters when significant post-forge CNC work is required, as it directly affects cycle time and tool life.

Key Benefits of Carbon Steel Forgings
this strategy deliver higher strength-to-cost ratio than any comparable manufacturing route, combining refined grain structure, predictable mechanical properties, and broad industry acceptance under established standards.
The advantages aren’t just theoretical. Engineers across automotive, energy, and industrial sectors consistently choose forged carbon steel over castings and weldments for load-bearing applications because the performance data supports it.
Mechanical and Structural Advantages
- Higher fatigue strength: The aligned grain flow in forgings resists crack initiation under cyclic loading. This is critical for rotating parts like crankshafts and connecting rods.
- Improved impact toughness: Forgings absorb impact energy better than castings of equivalent geometry. The ASM Digital Library’s forging handbook documents consistent improvements in Charpy impact values for forged vs. cast equivalents.
- Eliminated internal defects: Forging closes voids, porosity, and segregation that form during solidification of castings. The result is a denser, more homogeneous part.
- Predictable heat treatment response: Because the microstructure is uniform, heat treatment outcomes are consistent across a production batch.
Economic and Supply Chain Advantages
- Lower material cost than alloy alternatives: Carbon steel costs significantly less per kilogram than stainless steel or nickel alloys. For high-volume production, this cost gap compounds quickly.
- Broad supplier availability: Carbon steel billets are globally available in consistent grades, reducing supply chain risk compared to specialty alloys.
- Compatibility with standard machining: Carbon steel forged blanks machine efficiently on CNC turning centers, Swiss lathes, and mill-turn equipment. Tool life is predictable, and cycle times are manageable.
- Established standards compliance: ASTM A788 and ASME SA-541 provide clear acceptance criteria, simplifying supplier qualification and incoming inspection.
Pro Tip: When comparing forged carbon steel against alloy steel forgings, run a full cost-per-function analysis rather than just material cost per kilogram. In many applications, a properly heat-treated 1045 forging outperforms a more expensive alloy steel part at a fraction of the total cost.
In one project we handled at MFG SOLUTION, a client sourcing automotive connector components switched from cast iron to cold-forged 1018 carbon steel. The result was a 40% improvement in fatigue life and a 15% reduction in per-unit cost, driven by shorter cycle times on our CNC turning equipment and elimination of porosity-related rejects.
Common Challenges and Mistakes in 2026
The most common mistakes with this approach involve grade misselection, inadequate post-forge heat treatment, and underestimating the machining allowances needed to achieve final tolerances.
Even experienced procurement teams run into predictable problems. Understanding them upfront saves significant cost and schedule time.
Grade and Process Mismatches
A common mistake is specifying a high-carbon grade for a part that requires welding in assembly. Grades above 0.40% carbon need preheat and post-weld heat treatment to avoid hydrogen-induced cracking in the heat-affected zone (HAZ). Skipping this step causes field failures that trace back to the original material specification, not the welding process.
Another frequent error is applying cold forging to parts with complex internal features or thin walls. Cold forging excels at solid or near-solid cross-sections. Parts with significant undercuts or internal cavities need hot forging or a hybrid approach.
Dimensional and Tolerance Pitfalls
- Insufficient machining stock: Forgings have dimensional variation from die wear and thermal contraction. If you don’t specify adequate machining allowance (typically 1.5mm to 3mm per surface for closed-die forgings), you risk not having enough material to clean up the surface to final dimension.
- Ignoring tolerance stackup: When multiple forged components assemble together, individual part tolerances combine. Understanding precision tolerance stackup before finalizing forging drawings prevents costly assembly failures downstream.
- Surface decarburization: Hot forging exposes the steel surface to oxygen at high temperature, burning off carbon from the outer layer. This decarburized layer is softer than the core. It must be machined away before hardness-critical surfaces are finished.
- Residual stress from cooling: Rapid cooling after forging introduces residual stresses. Without proper normalization or annealing, these stresses distort the part during subsequent machining.
Industry analysts note that as of 2026, tighter supply chain scrutiny from automotive OEMs under IATF 16949 compliance requirements has increased pressure on forging suppliers to document heat treatment records and material traceability for every production lot. Suppliers without robust process documentation are increasingly disqualified during supplier audits.
Best Practices for Machining Carbon Steel Forgings in 2026
The best results come from treating the forging and machining operations as a single integrated process, not two separate steps handed off between suppliers.
This integrated approach is where MFG SOLUTION’s model adds clear value. We handle cold forging and precision CNC machining under one roof, which eliminates the dimensional handoff errors that occur when forgings are sourced separately and then sent to a different machine shop.
Design and Engineering Best Practices
- Design for forgeability first: Avoid sharp internal corners and extreme cross-section changes. Generous radii (minimum 1.5mm) reduce die stress and improve material flow during forging.
- Specify heat treatment in the drawing: Don’t leave heat treatment as an afterthought. Define the required hardness range (e.g., 28–34 HRC for 1045) and the acceptable testing method (Rockwell, Brinell) on the engineering drawing.
- Align grain flow with load direction: Work with your forging supplier to orient the die so that grain flow runs parallel to the primary stress axis in service. This maximizes fatigue resistance.
- Plan machining allowances explicitly: Add 2mm minimum stock on critical surfaces. Specify this on the forging drawing, not just the machined part drawing.
Machining and Quality Control Best Practices
- Use appropriate cutting parameters: Carbon steel forgings are harder and more abrasion-resistant than annealed bar stock. Reduce cutting speeds by 10–15% compared to your standard carbon steel parameters, especially after quench-and-temper treatment.
- Apply correct coolant strategy: Proper CNC coolants and lubricants are essential when machining hardened carbon steel forgings. Flood coolant prevents thermal shock cracking in high-carbon grades; semi-synthetic fluids balance lubricity and cooling for medium-carbon work.
- Inspect incoming forgings before machining: Check hardness, dimensional stock, and surface condition before committing to machining. Catching a non-conforming forging before it enters the CNC cell saves the full machining cycle cost.
- Use rigid workholding: Forgings often have irregular surfaces before machining. Soft jaws or custom fixtures that contact the forging’s datum surfaces prevent chatter and maintain positional accuracy through the machining sequence.
Pro Tip: For threaded features on carbon steel forged parts, specify thread class and surface finish requirements explicitly on the drawing. Carbon steel forgings respond well to CNC threading operations, but the harder heat-treated grades wear taps faster. At MFG SOLUTION, our CNC threading services account for material hardness when selecting tooling and speeds, which directly affects thread quality and tool life.
At MFG SOLUTION, we’ve found that the combination of cold forging and Swiss lathe machining handles the majority of small carbon steel forged parts under 38mm diameter with excellent results. The cold forging step produces near-net shapes with work-hardened surfaces, and the Swiss lathe removes minimal stock to achieve final tolerances. This approach keeps per-unit costs low while maintaining the dimensional accuracy required for automotive and industrial applications. Our team quotes within 8 hours and ships within 3 days, with full IATF 16949 and ISO 9001:2015 documentation for every production lot.

Frequently Asked Questions
1. Can you forge carbon steel?
Yes, carbon steel is one of the most forgeable materials available. All carbon steel grades from low-carbon 1018 through high-carbon 1080 can be forged using hot, warm, or cold forging methods. Low-carbon grades are particularly well-suited to cold forging due to their high ductility, while medium-carbon grades like 1045 are the workhorses of hot closed-die forging for automotive and industrial parts. High-carbon grades above 0.60% require tighter temperature control during hot forging to avoid cracking, but they forge successfully when proper procedures are followed.
2. What grade is carbon steel forging?
The most widely used carbon steel forging grades are 1018 (low-carbon, excellent for cold forging and carburized parts), 1030 (medium-carbon, good weldability with moderate strength), 1045 (medium-carbon, the most common grade for structural forgings requiring quench-and-temper hardening), 1060 (high-carbon, used for springs and tools), and 1117 (resulfurized low-carbon, chosen specifically for high-volume parts requiring superior machinability after forging). Grade selection should be driven by the required mechanical properties, heat treatment plan, weldability requirements, and downstream machining complexity. For most general industrial applications, 1045 is the default starting point.
3. What is the difference between carbon steel forgings and alloy steel forgings?
the practice contain primarily iron and carbon (with manganese), while alloy steel forgings include additional elements such as chromium, molybdenum, nickel, or vanadium in meaningful quantities. Alloy additions improve hardenability, high-temperature strength, or corrosion resistance. The trade-off is cost. this practice are significantly cheaper and cover the majority of industrial applications. Alloy steel forgings are specified when carbon steel’s performance ceiling isn’t sufficient, such as in high-temperature pressure vessels or heavily loaded aerospace components.
4. What standards apply to carbon steel forgings?
ASTM A788 covers general requirements for steel forgings including carbon steel grades, defining testing methods, heat treatment requirements, and marking. ASME SA-541 governs carbon and alloy steel forgings for pressure vessel and nuclear applications. For automotive supply chains, IATF 16949 certification of the forging and machining supplier provides the process control framework. Parts for pressure systems may also require compliance with ASME Boiler and Pressure Vessel Code Section II material specifications.
5. How does cold forging compare to hot forging for carbon steel parts?
Cold forging is performed at room temperature and produces tighter dimensional tolerances, better surface finish, and work-hardened surfaces without a separate heat treatment step. It’s best suited for small, high-volume parts with relatively simple geometry, typically under 38mm in diameter. Hot forging requires heating the billet to above the recrystallization temperature (typically 1,100°C to 1,250°C for carbon steel), which allows complex shapes and large cross-sections to be formed with lower forming forces. Hot forgings require more machining stock and post-forge heat treatment to achieve final properties, but they can produce larger and more complex geometries than cold forging allows.
6. How much machining do carbon steel forgings require?
Almost all this method require some post-forge machining to achieve final dimensional tolerances and surface finish. Typical machining allowances range from 1.5mm to 3mm per surface for closed-die hot forgings. Cold forgings have tighter as-forged dimensions and may need only 0.3mm to 0.8mm of stock removal. Operations commonly required include CNC turning for cylindrical features, milling for flats and pockets, CNC hole drilling for bores and cross-holes, and threading for fastener interfaces. Understanding machining tolerances before finalizing forging drawings ensures the as-forged blank has sufficient stock for all required operations.
Conclusion
this strategy remain the most cost-effective route to high-integrity structural components across automotive, industrial, and energy applications. The forging process delivers grain refinement, fatigue resistance, and dimensional consistency that castings simply can’t match. Grade selection, heat treatment, and machining allowances are the three variables that determine whether a forging project succeeds or fails.
For small precision parts under 38mm, the combination of cold forging and CNC machining is particularly powerful. It delivers near-net shape accuracy, work-hardened surfaces, and the tight tolerances that modern assemblies demand, all at competitive per-unit cost.
MFG SOLUTION specializes in exactly this workflow. Our cold forging capability, paired with Swiss lathe and CNC turning operations, handles carbon steel forged parts from blank to finished dimension under one roof. We quote within 8 hours, ship within 3 days, and back every production lot with ISO 9001:2015 and IATF 16949 documentation. If you’re sourcing this approach for automotive, electronics, or industrial applications, our team of 60+ engineering professionals is ready to review your specifications and recommend the most cost-effective process path.
Recommended Articles
Explore more from our content library: