
2026-06-05
A Complete Guide to the Types of Forging Processes

| Key Insight | Explanation |
|---|---|
| Four core types of forging | Open die, closed die (impression die), cold forging, and seamless rolled ring forging cover the vast majority of industrial applications. |
| Temperature matters | Forging is classified as hot, warm, or cold depending on the workpiece temperature relative to the metal’s recrystallization point. |
| Cold forging excels for small parts | Cold forging (including cold heading) produces high-volume, tight-tolerance small components with minimal material waste and superior surface finish. |
| Material grain flow is key | Forging aligns the metal’s grain structure to the part geometry, producing stronger, more fatigue-resistant parts than casting or machining from bar stock. |
| Wide material compatibility | Steel, aluminum, titanium, brass, copper, and high-temperature alloys are all routinely forged, each requiring different process parameters. |
| Process selection drives cost | Choosing the right forging method for your part geometry, volume, and tolerance requirements directly determines unit cost and lead time. |
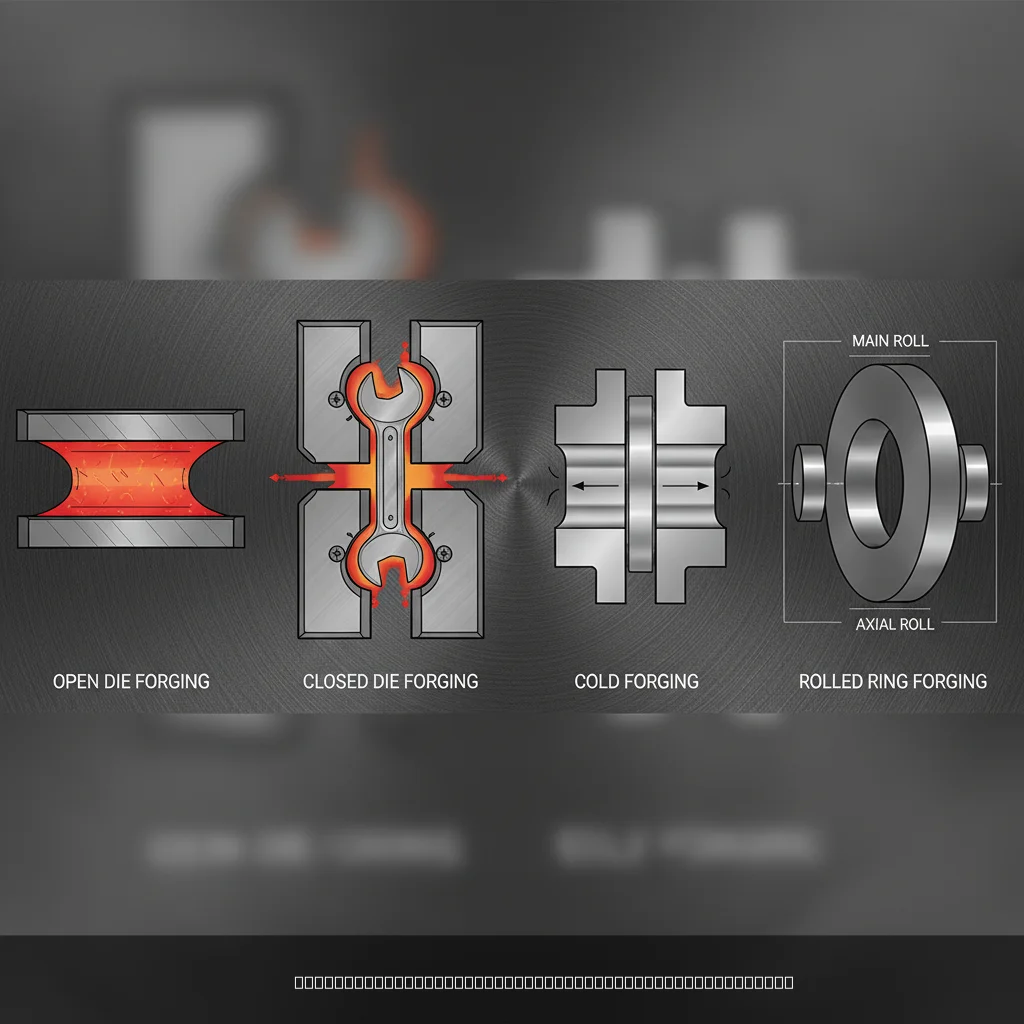
The main types of forging are open die forging, closed die (impression die) forging, cold forging, and seamless rolled ring forging. Each method shapes metal through compressive force, but they differ in tooling, temperature, and the part geometries they produce best. Understanding which type suits your application determines both part quality and production cost. This guide covers every major forging process, the metals used, and the practical trade-offs engineers and procurement teams need to know when selecting a method.
What Is Forging?
Forging is a bulk metal-forming process that shapes workpieces by applying compressive forces through hammers, presses, or dies. It can be performed at cold, warm, or hot temperatures and produces parts with superior mechanical properties compared to casting or machining from bar stock.
Definition and Core Principles
According to the Forging Industry Association, forging is a bulk forming process where metal is deformed into shaped components, and it can be performed cold, warm, or hot [1]. The process works by applying force that exceeds the material’s yield strength, permanently deforming the workpiece into the desired shape without removing material.
What separates forging from other metalworking methods is grain flow. When metal is forged, the internal grain structure aligns with the contour of the finished part. This produces higher tensile strength, impact resistance, and fatigue life than a cast or machined equivalent. The Engineering Choice notes that forging involves shaping metal through hammering, pressing, or rolling using compressive forces [2].
Why Forging Matters in Modern Manufacturing
Forged parts appear in virtually every critical application: automotive drivetrain components, aerospace structural members, medical implants, and industrial fasteners. The process is valued not just for shape creation, but for the mechanical integrity it imparts to the final part.
- Forged parts typically exhibit 20-30% higher fatigue strength than equivalent cast parts
- The process produces near-net-shape components, reducing downstream machining
- Forging supports high-volume production with consistent, repeatable quality
- It works across a wide range of metals, from mild steel to exotic nickel alloys
As of 2026, global demand for precision-forged components continues to grow, driven by lightweighting requirements in electric vehicles and tighter tolerance demands in medical device manufacturing.
Types of Forging: A Complete Breakdown
The primary types of forging are open die, closed die, cold forging, and seamless rolled ring forging, with additional methods including upset forging, press forging, roll forging, and drop forging used for specialized applications.
The Four Core Forging Categories
GL Forge identifies four principal forging processes that cover the majority of industrial production: impression die (closed die) forging, open die forging, cold forging, and seamless rolled ring forging [3]. Each serves a distinct niche based on part size, geometry, material, and volume requirements.
| Forging Type | Temperature | Best For | Typical Tolerance | Tooling Cost |
|---|---|---|---|---|
| Open Die | Hot | Large, simple shapes; shafts; discs | ±1.5–3mm | Low |
| Closed Die (Impression) | Hot or Warm | Complex, high-volume parts | ±0.3–1mm | High |
| Cold Forging | Room temperature | Small, precise, high-volume parts | ±0.05–0.2mm | Medium |
| Seamless Rolled Ring | Hot | Rings, flanges, bearing races | ±0.5–2mm | Medium |
| Upset Forging | Hot or Cold | Fasteners, bolts, flanged ends | ±0.1–0.5mm | Low–Medium |
| Press Forging | Hot or Cold | Precise, large structural parts | ±0.2–1mm | High |
Additional Forging Methods Worth Knowing
Beyond the four core types, several specialized processes serve niche applications. Fractory lists drop forging, press forging, upset forging, automatic hot forging, and roll forging as distinct methods within the broader forging classification [4].
- Drop forging: Uses a falling hammer (gravity or powered) to strike the workpiece against a die; subdivided into open and closed die variants
- Press forging: Applies slow, continuous pressure rather than impact, giving better dimensional control and deeper deformation
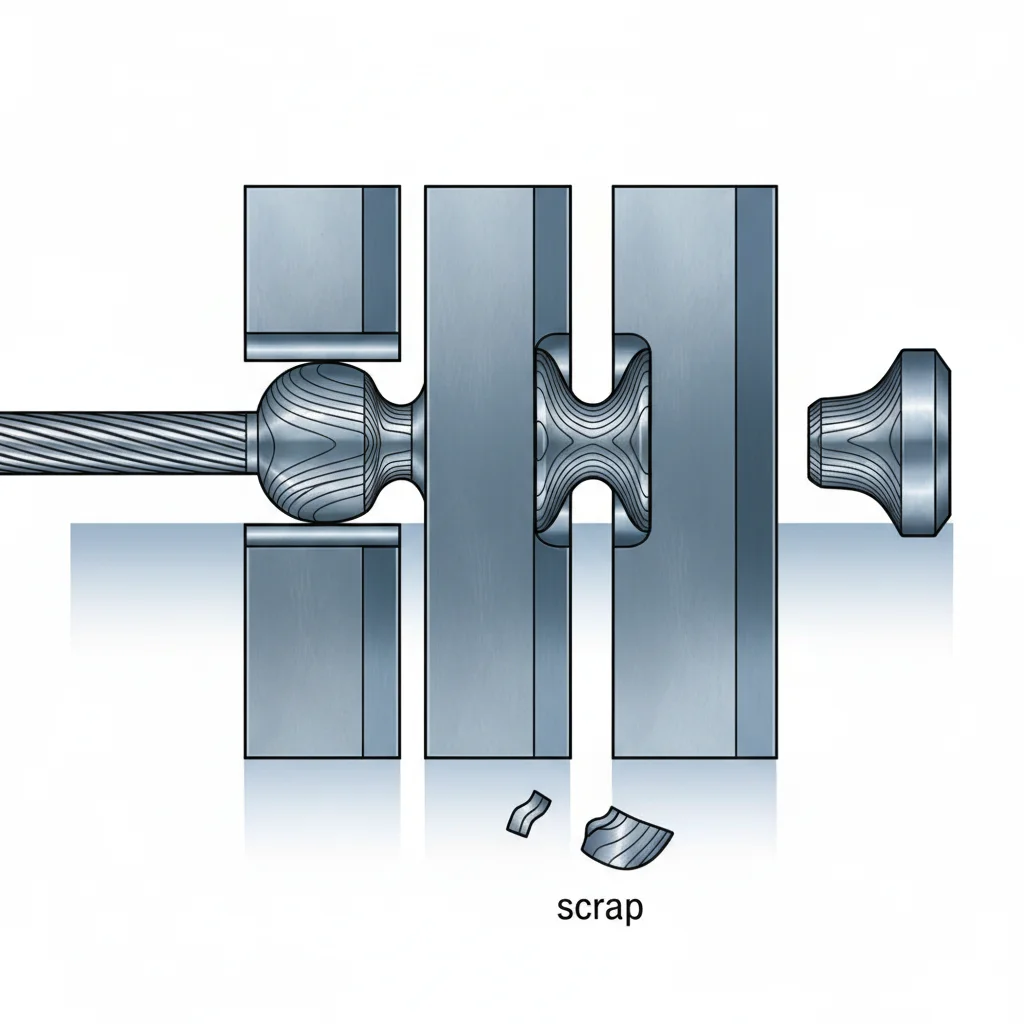
- Upset forging: Increases the cross-section of a workpiece by compressing its length; standard for producing bolt heads and flanges
- Roll forging: Passes the workpiece between two driven rolls with grooved dies to reduce cross-section and elongate the part
- Automatic hot forging: Combines induction heating and multi-stage die sequences for high-volume, near-net-shape production
Pro Tip: Don’t default to closed die forging just because your part looks complex. For small, high-volume components under 38mm in diameter, cold forging often delivers tighter tolerances, better surface finish, and lower per-unit cost — with no heating energy required.
How Each Forging Process Works
Each forging process applies compressive force differently: open die uses flat or simple tooling with manual repositioning, closed die uses matched cavities to fill a precise shape, cold forging deforms metal at room temperature through progressive dies, and rolled ring forging expands a pierced disc between driven rollers.
Open Die and Closed Die Forging Mechanics
Open die forging (also called smith forging or free forging) places the workpiece between two flat or simply shaped dies. The operator repositions the part between blows to achieve the desired shape. According to IQS Directory, open die forging is suited for large, simple geometries like shafts, cylinders, and discs, and it’s the method closest to traditional blacksmithing [5].
Closed die forging (impression die forging) confines the workpiece inside a matched pair of dies. As the dies close, metal flows to fill every cavity. Flash, the thin excess metal that squeezes out at the die parting line, is later trimmed. Cornell Forge explains that closed die forging enables complex geometries and tight dimensional repeatability, making it the standard for automotive and aerospace structural parts [6].
- Billet or preform is cut to a calculated weight
- The workpiece is heated to forging temperature (typically 900–1250°C for steel)
- The preform is placed in the die cavity
- The hammer or press closes the dies under force
- Flash is trimmed in a separate trimming die
- The forging is heat-treated, inspected, and finished
Cold Forging and Seamless Rolled Ring Mechanics
Cold forging (including cold heading, cold extrusion, and cold drawing) deforms metal at or near room temperature. No heating is required. The metal work-hardens during deformation, which actually increases its strength. Wikipedia’s forging entry notes that cold forging produces excellent surface finish and dimensional accuracy, making it ideal for fasteners, pins, and small precision components [7].
Cold heading, a subset of cold forging, is particularly relevant for small parts manufacturing. It feeds wire stock into a die and uses a punch to form heads, flanges, or other features in a single stroke. At MFG SOLUTION, we’ve found that cold heading for parts up to 38mm diameter consistently delivers tolerances in the ±0.05–0.1mm range with minimal secondary machining required.
Seamless rolled ring forging starts with a pierced disc (a donut shape) that is placed over a driven roll. An idler roll applies pressure from the outside while the ring expands in diameter and its cross-section reduces. This produces rings with continuous grain flow around the circumference, ideal for bearing races, flanges, and gear blanks.
Forging Materials: What Metals Are Commonly Forged?
Nearly any metal can be forged, but the most commonly forged materials are carbon and alloy steels, stainless steels, aluminum alloys, titanium, brass, copper, and high-temperature nickel or cobalt alloys. Material choice directly affects which forging process is practical.
Steel, Aluminum, and Titanium
Steel is the most widely forged metal. Carbon steels (AISI 1018–1045), alloy steels (4130, 4340), and stainless steels (304, 316, 17-4 PH) are all routinely forged across all major process types. The Copper Development Association notes that forging terms and processes apply across copper, brass, and steel families, reflecting the process’s broad material compatibility [8].
Aluminum alloys (6061, 7075, 2024) are the second most common forging material. Aluminum forgings are standard in aerospace structures, automotive wheels, and bicycle components. They require lower forging temperatures (400–480°C) and produce excellent strength-to-weight ratios.
Titanium is forged for aerospace and medical implant applications where high strength and biocompatibility are both required. Titanium forging is technically demanding because of the metal’s narrow forging temperature window and reactivity with oxygen at high temperatures.
Copper, Brass, and High-Temperature Alloys
- Brass and copper: Forged for electrical connectors, plumbing fittings, and marine hardware; copper’s excellent forgeability allows intricate closed die shapes at relatively low temperatures
- Nickel superalloys (Inconel, Waspaloy): Forged for jet engine components and industrial turbines; require hot forging at very high temperatures and specialized die materials
- Cobalt alloys: Used in medical implants and cutting tools; forged in small volumes with precise thermal control
- Tool steels (H13, D2, M2): Forged to produce dies, cutting tools, and heavy-duty components requiring extreme hardness
Pro Tip: For small precision parts in brass or stainless steel under 38mm diameter, cold forging (specifically cold heading) is almost always more cost-effective than hot closed die forging. You eliminate heating energy, scale removal, and much of the post-forge machining — all of which add cost and lead time.
Industry analysts suggest that the choice of forging material and process together account for roughly 60–70% of the total part cost, according to research published by the Forging Industry Association [1]. Getting both decisions right early in the design phase is far less expensive than correcting them during production.
Key Benefits and Common Challenges of Forging
Forging’s primary advantages are superior mechanical properties, excellent grain structure, and high production repeatability. Its main challenges are high tooling costs for closed die processes, limited geometric complexity compared to casting, and the need for precise process control to avoid defects.
Why Forged Parts Outperform Cast or Machined Alternatives
The mechanical advantages of forging are well-documented. General Kinematics notes that forged parts exhibit superior strength, toughness, and reliability compared to cast or machined alternatives because the forging process refines and aligns the grain structure [9].
- Grain flow continuity: Forging follows the part contour, eliminating the random grain orientation of castings
- No internal porosity: Unlike casting, forging produces fully dense parts with no shrinkage voids
- Work hardening (cold forging): Cold forging increases surface hardness and fatigue resistance without heat treatment
- Material efficiency: Near-net-shape forging wastes far less material than machining from solid bar stock
- Consistency at volume: Die-based processes produce identical parts across large production runs
Common Challenges and How to Avoid Them
From experience, the most common mistake procurement teams make is selecting closed die forging for low-volume runs without accounting for die amortization. Die costs for closed die forging can range from $5,000 to $50,000 or more, and those costs must be spread across the production run. For volumes under a few thousand pieces, open die or cold forging often makes more economic sense.
A precision machining client we worked with recently faced exactly this issue: they’d specified a closed die hot forging process for a stainless steel connector component produced in batches of 500 pieces. Switching to cold heading reduced their per-unit cost by over 40% and cut lead time from three weeks to five days.
- Die cracking: Caused by incorrect die material selection or inadequate preheating; avoid by following recommended die steel grades for each forging temperature
- Underfill: Occurs when insufficient metal volume is placed in the die cavity; resolved by accurate billet weight calculation
- Laps and folds: Surface defects from improper metal flow; prevented by optimizing preform geometry
- Dimensional drift: Die wear over long runs causes gradual tolerance degradation; controlled by regular die inspection intervals
Best Practices for Choosing a Forging Process in 2026
Selecting the right forging process in 2026 requires matching part geometry, production volume, tolerance requirements, and material to the process that minimizes total cost per part, not just tooling cost.
A Framework for Process Selection
Our team at MFG SOLUTION recommends a structured decision framework when evaluating forging options for new part programs. The framework considers five variables in sequence:
- Part size and geometry: Parts under 38mm diameter with rotational symmetry are strong candidates for cold forging or upset forging; larger complex shapes favor closed die hot forging
- Annual volume: Under 5,000 pieces, open die or cold forging minimizes tooling amortization; above 50,000 pieces, closed die becomes cost-competitive
- Tolerance requirement: Tolerances tighter than ±0.2mm are most reliably achieved with cold forging or precision closed die; looser tolerances open up lower-cost hot forging options
- Material: Confirm the material’s forgeability rating and required forging temperature before committing to a process
- Secondary operations: Account for post-forge machining, heat treatment, and surface finishing when comparing total part cost across processes
Quality Standards and Certification Requirements
As of 2026, forged components for automotive, medical, and aerospace applications must meet specific quality management standards. The three most relevant are:
- ISO 9001:2015: General quality management system standard applicable to all forging suppliers
- IATF 16949: Automotive-specific quality standard requiring documented process control, PPAP (Production Part Approval Process), and statistical process control (SPC)
- ISO 13485:2016: Medical device manufacturing standard requiring full traceability, risk management, and validated processes
The Crucible describes the four fundamental stages of any forging process as heating, holding, hitting, and shaping [10]. In a certified manufacturing environment, each of these stages requires documented process parameters, inspection checkpoints, and traceability records.
Pro Tip: Always request a PPAP (Production Part Approval Process) package from your forging supplier, even for non-automotive parts. It forces the supplier to document control plans, measurement system analysis, and process capability studies — giving you hard evidence that the process is in control before you commit to a production run.
According to research referenced by IQS Directory, forging processes are most effectively categorized by both die configuration (open vs. closed) and temperature regime (hot, warm, cold), since these two variables together determine the part’s final mechanical properties and dimensional accuracy [5].
Sources & References
- Forging Industry Association, “Forging 101”, 2023
- The Engineering Choice, “What Is Forging? Definition, Process, and Types”, 2024
- GL Forge, “Types of Forging Processes: Guide to Metal Forging Methods”, 2024
- Fractory, “Forging: Process, Classification & Methods”, 2024
- IQS Directory, “Types, Process, and Uses of Forging”, 2024
- Cornell Forge Co., “Understanding the Different Forging Processes”, 2024
- Wikipedia, “Forging”, 2026
- Copper Development Association, “Forging Guide Glossary of Terms”, 2024
- General Kinematics, “Different Metal Forging Methods”, 2024
- The Crucible, “16 Blacksmithing Techniques”, 2024
Frequently Asked Questions
1. What are the four types of forging?
The four primary types of forging are open die forging, closed die (impression die) forging, cold forging, and seamless rolled ring forging. Open die uses simple flat tooling for large shapes; closed die uses matched cavities for complex, high-volume parts; cold forging deforms metal at room temperature for small precision components; and seamless rolled ring forging expands a pierced disc into rings and flanges. Most industrial parts fall into one of these four categories, though specialized methods like upset forging, press forging, and roll forging serve additional niche applications.
2. What metals are commonly forged?
The most commonly forged metals are carbon steels, alloy steels, stainless steels, aluminum alloys, titanium, brass, copper, and high-temperature nickel and cobalt superalloys. Steel accounts for the largest share of global forging volume, while aluminum is standard in aerospace and automotive lightweighting applications. Titanium and nickel superalloys are forged in smaller volumes for critical aerospace, medical, and energy applications where extreme strength and temperature resistance are required. Each material requires specific forging temperature ranges and die materials to achieve optimal results.
3. What is the difference between hot forging and cold forging?
Hot forging heats the metal above its recrystallization temperature (typically 900–1250°C for steel), making it easier to deform but producing a rougher surface finish and requiring post-forge scale removal. Cold forging works at room temperature, producing tighter dimensional tolerances (±0.05–0.2mm), better surface finish, and higher surface hardness through work hardening. Cold forging is preferred for small, high-volume precision parts; hot forging is used for large, complex geometries where the material needs to flow freely into intricate die cavities.
4. What is upset forging used for?
Upset forging compresses a workpiece along its length to increase its cross-sectional area, most commonly used to form bolt heads, flanges, and other enlarged-end features on rod or wire stock. It’s one of the most efficient types of forging for high-volume fastener production. The process can be performed hot or cold and is well-suited to automatic forging machines that feed wire stock and produce finished upset forms in a single or multi-stroke sequence.
5. How does forging compare to casting for part strength?
Forged parts are generally 20–30% stronger in fatigue than equivalent cast parts because forging aligns the metal’s grain structure to the part geometry and eliminates internal porosity and shrinkage voids that are inherent in casting. Casting allows more complex internal geometries (like hollow sections) that forging cannot produce, so the choice depends on the specific strength, geometry, and volume requirements of the application. For high-stress structural components, forging is almost always the preferred process.
6. What is the most cost-effective forging process for small parts?
For small parts (under 38mm diameter) produced in high volumes, cold forging and cold heading are typically the most cost-effective types of forging processes. They eliminate heating energy costs, produce excellent surface finish that reduces secondary machining, and achieve tight tolerances in a single or multi-stroke operation. Tooling costs are moderate, and per-unit costs drop significantly at volumes above 5,000–10,000 pieces, making cold forging the standard choice for precision fasteners, connectors, and small structural components.
Conclusion
The types of forging span a wide range of processes, from the simplicity of open die hammer work to the precision of cold heading and seamless ring rolling. Each method has a specific role: open die for large, simple shapes; closed die for complex, high-volume parts; cold forging for small, tight-tolerance components; and rolled ring for annular parts requiring circumferential grain continuity. The right choice depends on your part geometry, production volume, material, and tolerance requirements.
For engineers and procurement teams sourcing small precision components, cold forging deserves serious consideration. It delivers superior surface finish, excellent dimensional accuracy, and lower per-unit cost at volume, without the energy and scale-removal overhead of hot processes.
MFG SOLUTION operates cold heading equipment alongside 5-axis CNC machines, Swiss lathes, and automatic lathes to cover the full spectrum of small precision part manufacturing. With ISO 9001:2015, ISO 13485:2016, and IATF 16949 certifications, 60+ engineering professionals, and a quote-to-ship window of 8 hours to 3 days, we’re equipped to help you select the most cost-effective forging or machining process for your specific application. Submit your specifications and get a detailed quote within 8 hours.
Recommended Articles
Explore more from our content library: